

 EN

 English
 русский
 Français
 Español
 عربى
Reinforcing Steel Aluminum Strand: High-Strength Conductors for Reliable Power Transmission
Content
- 1 1. What Is Reinforcing Steel Aluminum Strand?
- 2 2. Why the Aluminum-and-Steel Design Is Advantageous
- 3 3. Product Specifications and Engineering Selection
- 4 4. Manufacturing Process and Quality Control
- 5 5. Performance Features Under Operating Conditions
- 6 6. Applications in Power Transmission and Distribution
- 7 7. Advantages Compared with Competing Conductor Options
- 8 8. Installation and Maintenance Recommendations
- 9 9. Why Manufacturing Capability Matters to Buyers
- 10 10. Recommended Purchasing Checklist
- 11 11. Frequently Asked Questions
- 11.1 Q1: What is the main purpose of the steel core?
- 11.2 Q2: Is reinforcing steel aluminum strand the same as an all-aluminum conductor?
- 11.3 Q3: How should the conductor size be selected?
- 11.4 Q4: Can this product be used in coastal environments?
- 11.5 Q5: What is the typical conductivity of the product?
- 11.6 Q6: What delivery length is available?
- 11.7 Q7: Is the product suitable for high-tension distribution lines?
- 11.8 Q8: Can it be used as a ground or shield wire?
- 11.9 Q9: What fittings should be used?
- 11.10 Q10: What makes the manufacturer suitable for customized projects?
- 12 12. Conclusion
- 13 References
- 14 Product: Reinforcing Steel Aluminum Strand
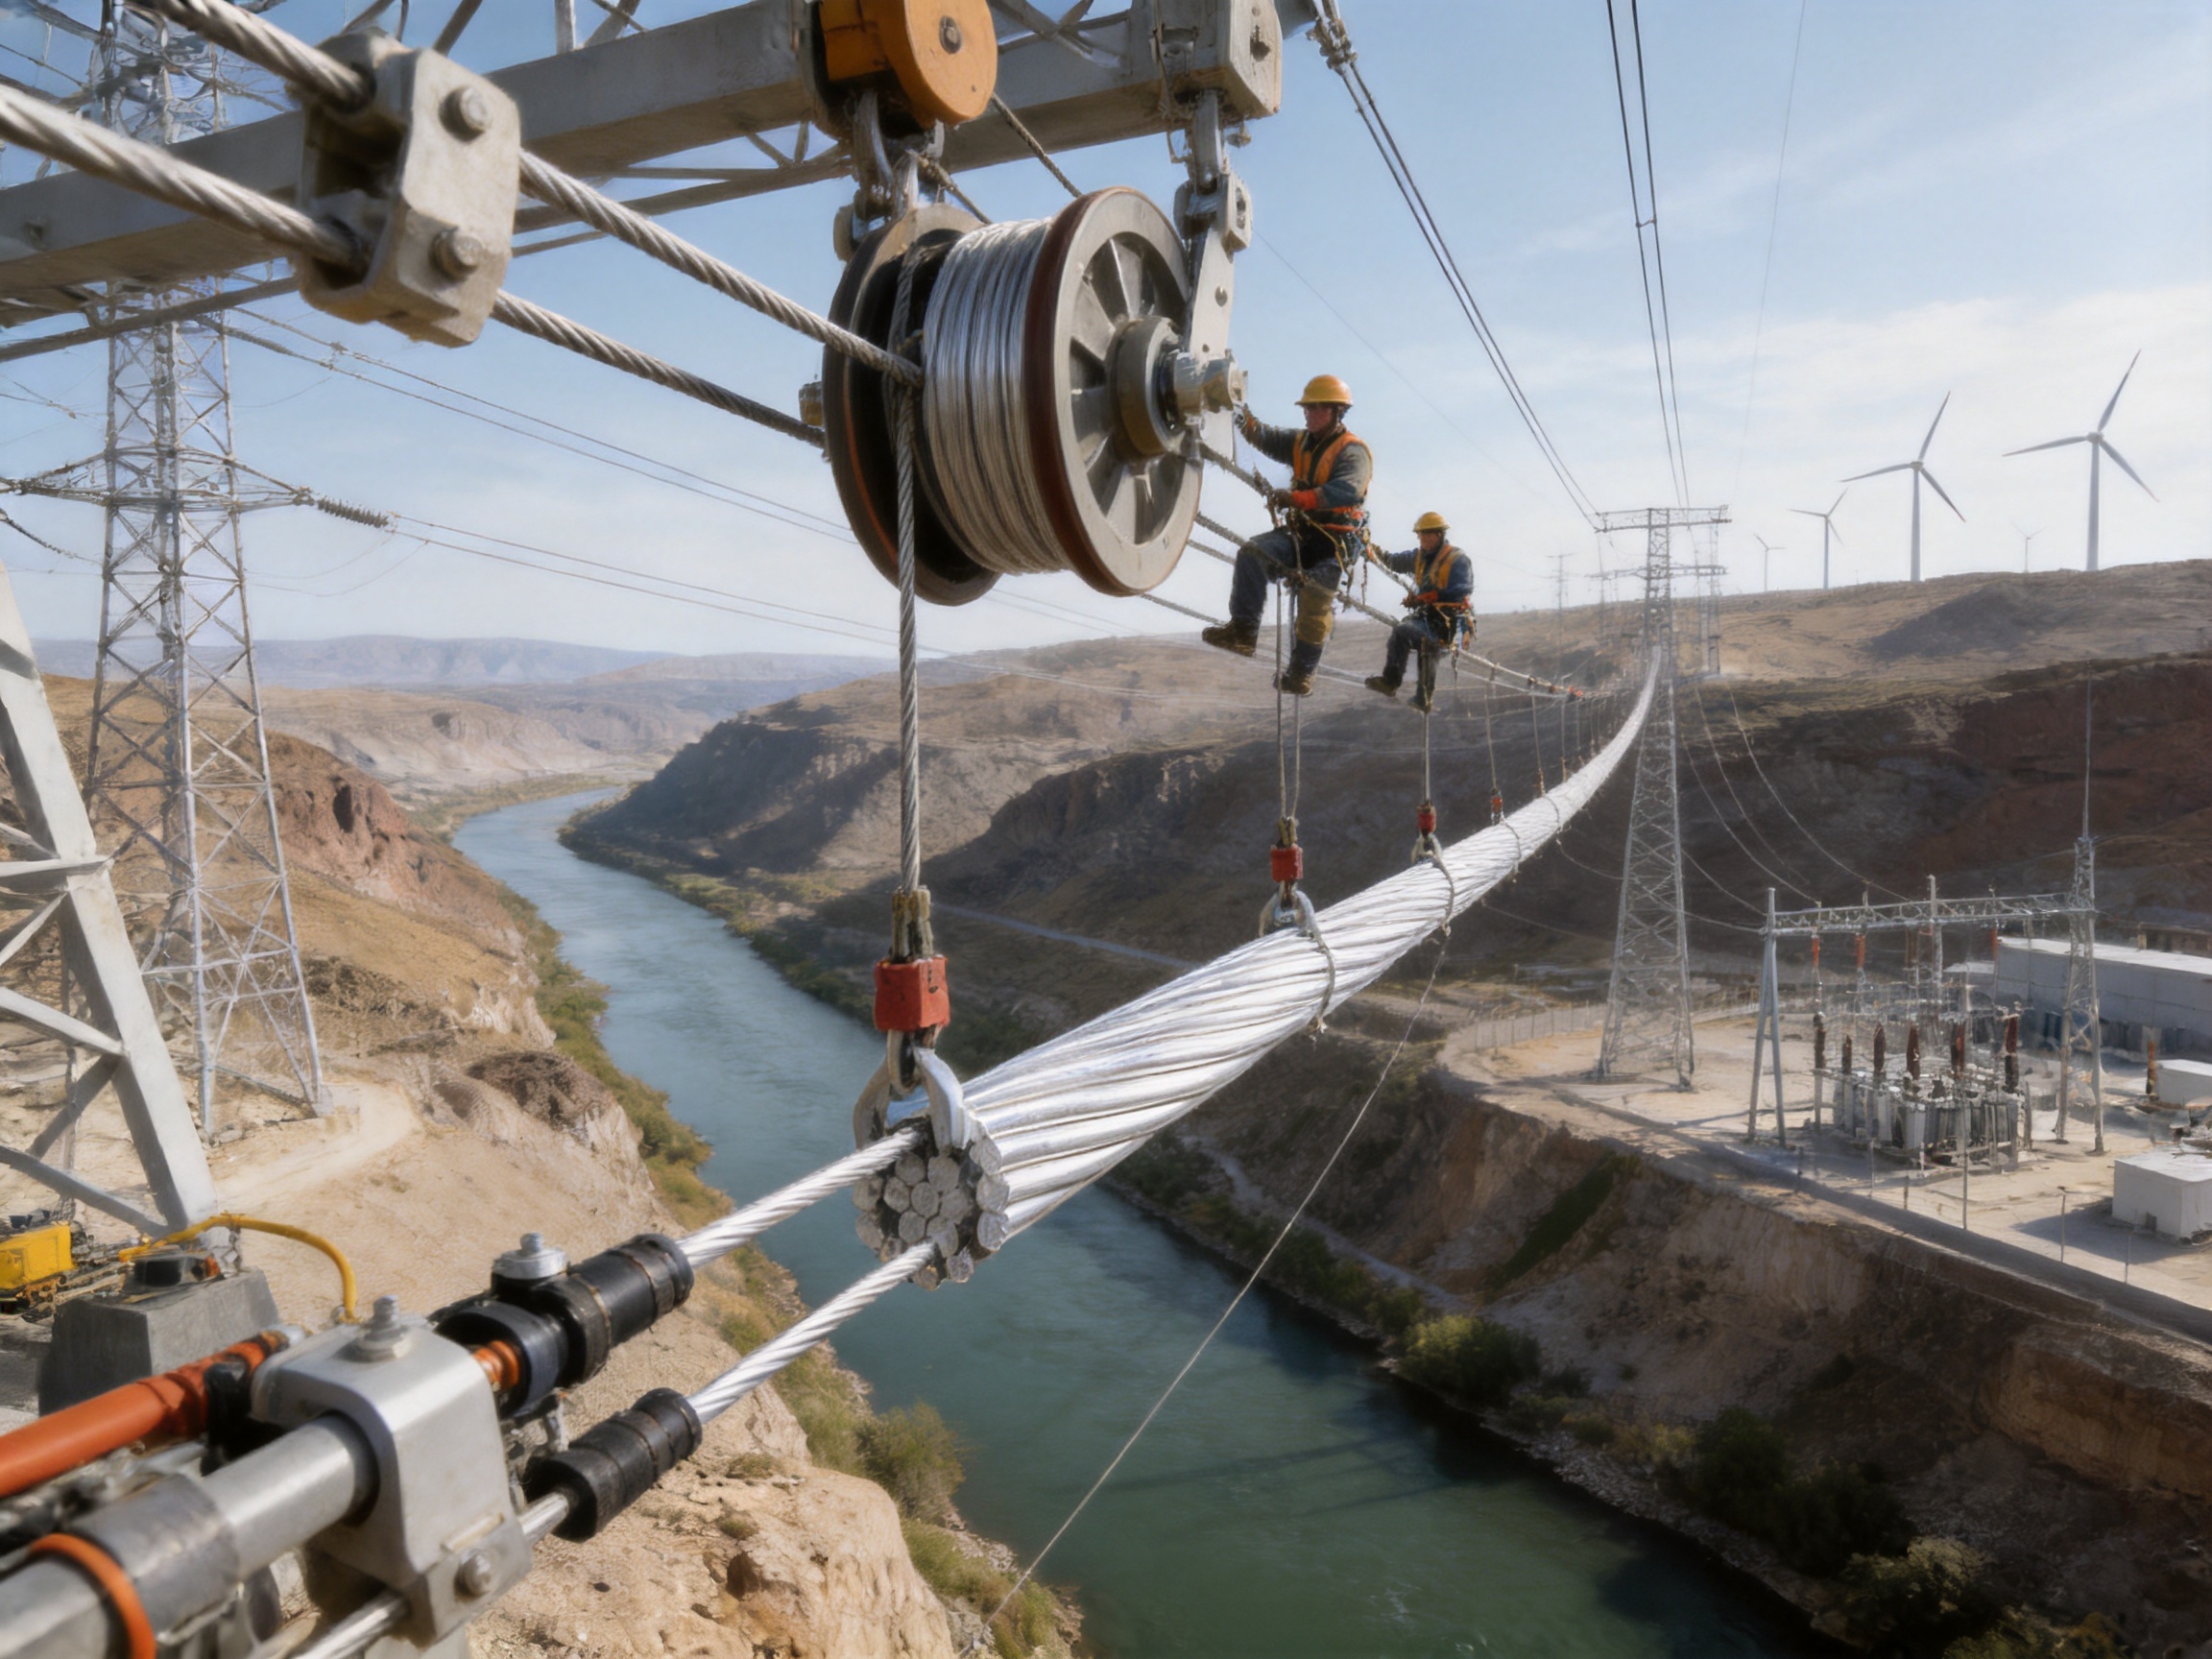
Reinforcing steel aluminum strand is a composite stranded conductor designed to combine the electrical conductivity of aluminum with the mechanical strength of a steel core. This combination makes it suitable for overhead transmission lines, high-tension distribution networks, grounding and shielding applications, and specialized hardware connections where both current-carrying capability and mechanical stability are required.
The product described in this article is manufactured according to the GB1179-83 standard and is available in nominal cross-sectional combinations ranging from 10/2 mm² to 240/30 mm². The first value generally represents the nominal aluminum area, while the second value represents the nominal steel-core area. Depending on the selected construction, the conductor may contain 6 to 30 aluminum strands surrounding 1 to 7 steel-core strands.
For modern power infrastructure, conductor selection is rarely based on conductivity alone. A conductor must also withstand tension, wind, ice, vibration, temperature variation, installation stress, and long-term environmental exposure. Reinforcing steel aluminum strand addresses these requirements through a layered aluminum-and-steel construction that offers a practical balance between electrical performance, tensile strength, weight, and installation efficiency.
Jiangsu Wopeng Power Technology Co., Ltd. supplies reinforcing steel aluminum strand as part of its wider power-transmission and busbar product portfolio. With engineering capabilities covering low-voltage systems through 35kV applications, the company combines standardized conductor production with expertise in tubular busbars, cast-resin busbar systems, wind-power busbars, compact busbars, and sliding contact line systems. This broader manufacturing background supports an application-oriented approach to conductor design, inspection, and customer service.
Reinforcing Steel Aluminum Strand
1. What Is Reinforcing Steel Aluminum Strand?
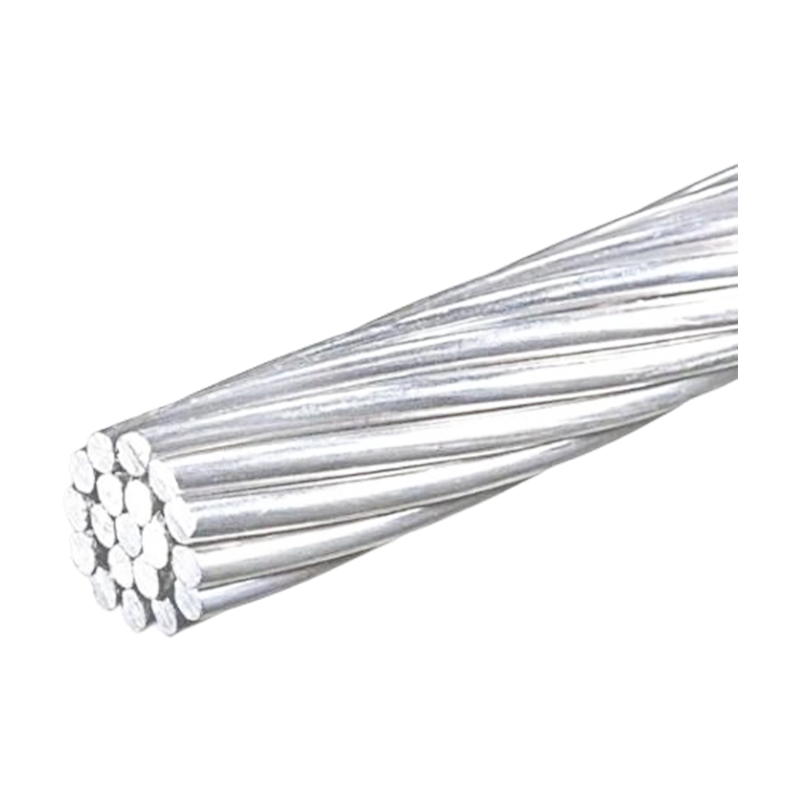
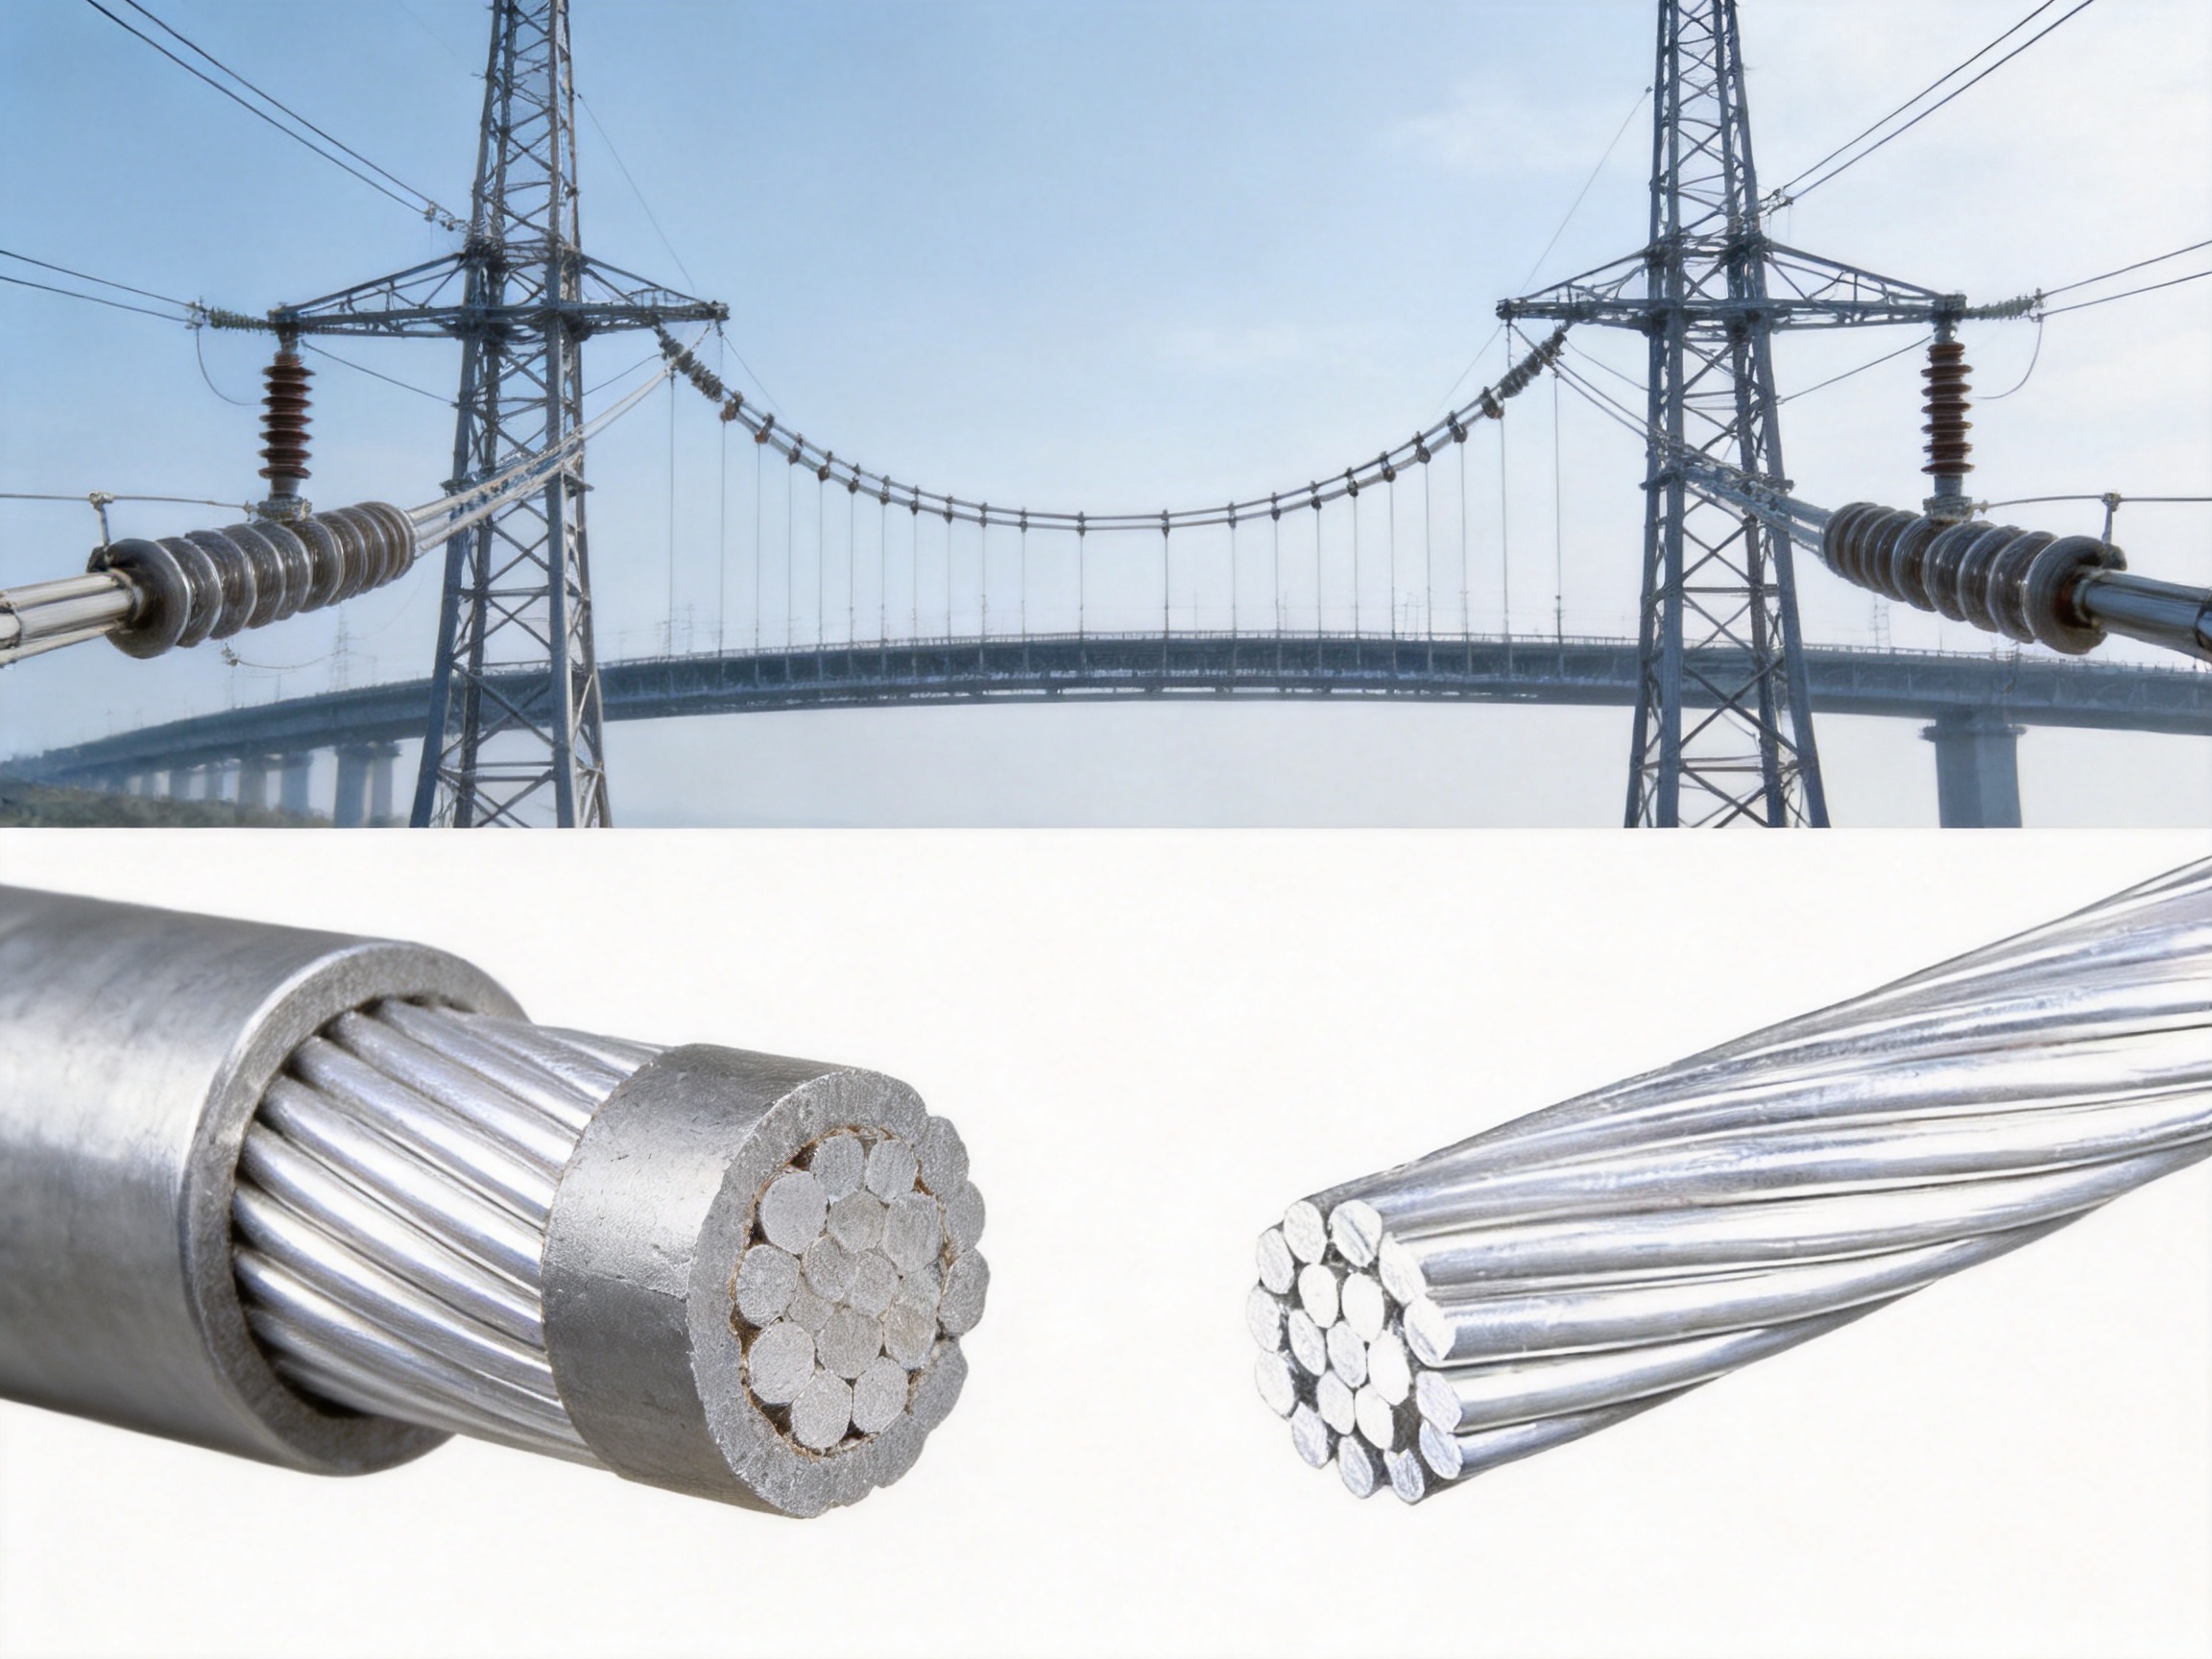
Reinforcing steel aluminum strand is a stranded composite conductor consisting of conductive aluminum wires placed around a central steel core. The aluminum portion forms the primary current-carrying path, while the steel portion provides tensile strength and structural support. The two materials perform different functions, but their combined construction allows the conductor to meet the requirements of demanding overhead power applications.
Aluminum is used for the outer conducting layers because it offers good electrical conductivity at a lower density than copper. It is also naturally resistant to many atmospheric conditions and can be formed into wires suitable for compact, concentric stranding. However, aluminum alone has lower tensile strength than steel. Long spans, high installation tensions, wind loads, ice accumulation, and conductor vibration can create mechanical demands that an all-aluminum conductor may not handle as efficiently.
The steel core compensates for this limitation. It supports a significant portion of the mechanical load and helps the conductor maintain its designed sag and tension characteristics. The result is a conductor capable of covering longer spans and operating under more severe mechanical conditions without excessive elongation, breakage, or loss of clearance.
The product is commonly associated with steel-reinforced aluminum conductors used in overhead networks. It can also be supplied for specific damping-wire and hardware-connection applications, including damping-type end caps. In these applications, the conductor’s combination of flexibility, tensile strength, conductivity, and compatibility with suitable connection hardware is particularly valuable.
1.1 Composite Construction
The conductor is formed through a controlled stranding process. Steel-core strands are placed at the center, and aluminum strands are helically wrapped around them in one or more layers. The number and diameter of the individual wires determine the final cross-sectional area, outside diameter, weight, resistance, and tensile strength.
Typical constructions include combinations of 1 to 7 steel-core strands with 6 to 30 aluminum strands. Aluminum wire diameters may range from approximately 1.50 mm to 4.72 mm, while steel-core wire diameters may range from approximately 1.50 mm to 3.60 mm. This range allows engineers to select a construction appropriate for the required current capacity, span length, mechanical load, and installation method.
The aluminum strands provide the main conductive area. The steel core is not intended to replace aluminum as the current-carrying material; instead, it reinforces the conductor mechanically. Because the electrical and mechanical functions are distributed between different materials, the conductor can achieve a stronger performance balance than a single-material alternative.
1.2 Standardized Product Range
The nominal cross-section range extends from 10/2 mm² to 240/30 mm². Across this range, calculated cross-sectional areas may extend from approximately 12.37 mm² to 275.96 mm². Outer diameters may range from approximately 4.50 mm to 21.60 mm, depending on the selected construction.
Calculated direct-current resistance values are listed from no more than approximately 2.706 Ω/km at the smaller end of the range to approximately 0.1410 Ω/km for larger constructions. Calculated tensile strength may range from approximately 4,012 N to 91,120 N, while calculated weight may range from approximately 42.9 kg/km to 964.2 kg/km.
These values are important during engineering selection. Resistance influences power loss and voltage performance. Tensile strength influences span capability, installation tension, and weather-load performance. Weight affects tower loading, stringing equipment, transportation, and structural design. Outside diameter influences fittings, clamps, clearances, and compatibility with existing line hardware.
2. Why the Aluminum-and-Steel Design Is Advantageous
The main advantage of reinforcing steel aluminum strand is functional separation. Aluminum supplies current-carrying capacity and environmental resistance, while steel supplies mechanical reinforcement. This design avoids relying on one material to perform every function and gives engineers greater flexibility in matching a conductor to actual operating conditions.
2.1 Higher Mechanical Strength Than All-Aluminum Conductors
Compared with a standard all-aluminum conductor of similar general size, a steel-reinforced construction can provide higher tensile strength. This is especially important when a line must cross a long distance between towers, pass through areas with severe wind, or withstand ice loading.
Higher tensile strength helps maintain conductor geometry during installation and operation. It can reduce excessive sag, preserve electrical clearances, and improve the stability of the line under changing weather conditions. In suitable designs, longer spans may be achieved with fewer support structures, potentially reducing tower foundations, land requirements, construction labor, and associated project costs.
Mechanical strength is also important during stringing. Conductors are pulled through sheaves and tensioning equipment during installation. The steel core gives the conductor greater resistance to installation tension, provided that the stringing procedure remains within the approved mechanical limits and does not exceed the elastic range of the conductor or its fittings.
2.2 Efficient Electrical Performance
The aluminum strands constitute the primary current path and provide a favorable conductivity-to-weight ratio. The supplied product information identifies electrical-grade aluminum with a purity of at least 99.7% and conductivity above 61% IACS after controlled annealing. Actual conductor performance depends on the construction, temperature, surface condition, and applicable test method, so project-specific data should be confirmed against the purchase specification.
Although steel has lower electrical conductivity than aluminum, the steel core occupies a relatively limited portion of the total cross-section. The surrounding aluminum layers therefore carry most of the current. Depending on the construction and material grade, typical conductivity may be described within a range of approximately 52.5% to 61% IACS for the complete conductor or its aluminum component, subject to the relevant calculation basis.
Low direct-current resistance helps limit resistive losses during continuous operation. For larger cross-sections, the resistance is significantly lower than that of smaller constructions, allowing the conductor to carry higher current with improved transmission efficiency. The conductor’s electrical characteristics should always be evaluated together with operating temperature, allowable current, ambient conditions, and installation geometry.
2.3 Favorable Strength-to-Weight Ratio
Steel is stronger than aluminum but substantially denser. The composite design uses steel only where mechanical reinforcement is needed and aluminum where conductivity and low mass are valuable. This produces a practical strength-to-weight ratio for overhead lines.
A favorable strength-to-weight ratio can simplify transportation and installation compared with a conductor that would require a much larger quantity of a heavy material to achieve the same tensile performance. It can also help control the vertical and horizontal loads imposed on towers, crossarms, insulators, clamps, and foundations.
2.4 Resistance to Atmospheric Exposure
Aluminum forms a thin, adherent oxide layer that provides natural protection against many atmospheric environments. This makes aluminum conductors suitable for outdoor installations exposed to humidity, industrial pollutants, and coastal air. The supplied product information also identifies galvanized steel-core protection, with zinc coating weight stated as complying with a minimum value of 300 g/m².
The aluminum outer layers help protect the steel core from direct exposure. In coastal or chemically aggressive environments, however, product selection should still consider salt concentration, pollution severity, drainage, connector design, and inspection requirements. Correct installation and compatible fittings are necessary to preserve the conductor’s long-term performance.
2.5 Suitability for Long-Span Applications
Long-span transmission lines place greater demands on tensile strength, sag control, vibration resistance, and tower loading. The steel core enables the conductor to handle greater mechanical loads than many all-aluminum alternatives. This can be beneficial for river crossings, mountainous terrain, open industrial sites, and areas where tower placement is restricted.
Longer spans can reduce the number of towers required, but span design must not rely on tensile strength alone. Engineers must also consider maximum operating temperature, creep, wind pressure, ice thickness, terrain elevation, conductor spacing, galloping risk, and the dynamic behavior of the entire line system.
3. Product Specifications and Engineering Selection
Selecting the correct reinforcing steel aluminum strand requires more than choosing a nominal cross-section. The conductor must be matched to the electrical load, mechanical span, environmental conditions, support structure, hardware, and applicable national or international standards.
| Parameter | Available or Stated Range | Engineering Significance |
| Nominal cross-section | 10/2 mm² to 240/30 mm² | Defines the approximate aluminum and steel-core areas |
| Aluminum strand count | 6 to 30 strands | Influences conductive area, flexibility, diameter, and surface arrangement |
| Steel-core strand count | 1 to 7 strands | Influences tensile strength and core configuration |
| Aluminum wire diameter | Approximately 1.50 mm to 4.72 mm | Determines layer geometry and contributes to total conductive area |
| Steel wire diameter | Approximately 1.50 mm to 3.60 mm | Contributes to mechanical reinforcement and core dimensions |
| Calculated cross-sectional area | Approximately 12.37 mm² to 275.96 mm² | Supports electrical and mechanical calculations |
| Outer diameter | Approximately 4.50 mm to 21.60 mm | Important for fittings, clearances, and line hardware |
| DC resistance | Approximately 2.706 Ω/km to 0.1410 Ω/km maximum, depending on size | Used to estimate voltage drop and resistive loss |
| Calculated tensile strength | Approximately 4,012 N to 91,120 N | Supports span, tension, sag, and weather-load design |
| Calculated weight | Approximately 42.9 kg/km to 964.2 kg/km | Influences transportation, tower loading, and installation equipment |
| General delivery length | Normally less than 2,000 m | Supports project logistics and reel planning |
3.1 Electrical Load Requirements
The first selection consideration is the required continuous current. Engineers should calculate the expected load, future capacity requirements, ambient temperature, solar radiation, wind speed, installation altitude, and allowable conductor temperature. A larger cross-section generally offers lower resistance and greater current-carrying capability, but it also increases weight, diameter, and material consumption.
For distribution systems, the conductor may be selected according to current demand, voltage class, line length, allowable voltage drop, and network expansion plans. For transmission systems, power-transfer requirements must be considered together with thermal limits and stability requirements.
Short-circuit conditions also require evaluation. The supplied information identifies a short-circuit thermal capacity of 150 kA²·s for the product description. Because short-circuit withstand is affected by conductor size, initial temperature, final temperature, duration, and connection hardware, the actual value must be confirmed for the selected construction and project design.
3.2 Mechanical and Environmental Requirements
Mechanical design should consider the maximum working tension, everyday tension, installation tension, elastic behavior, creep, wind pressure, ice load, and vibration. The supplied technical information states that creep deformation is controlled within 0.05% under long-term operating loads and that the construction has been evaluated through a two-million-cycle wind-induced vibration fatigue test.
These performance statements indicate the importance of controlled stranding and pre-twisting. Nevertheless, line designers should use certified test reports and project-specific calculations rather than relying solely on general product descriptions.
Environmental requirements can include temperatures from -40°C to +80°C, ice coating up to 30 mm, salt-spray exposure, ultraviolet aging, and repeated thermal cycling. The supplied product information reports stable thermal expansion behavior within the stated temperature range, retention of more than 95% tensile strength after 5,000 hours of salt-spray testing, and no significant surface degradation after 5,000 hours of UV aging.
3.3 Hardware Compatibility
Conductor performance depends on the quality and compatibility of clamps, compression connectors, suspension fittings, dead-end fittings, spacers, vibration dampers, and grounding accessories. Aluminum-to-steel composite conductors require fittings designed for their construction. Using inappropriate hardware may cause local crushing, oxidation, electrical resistance increase, strand damage, or premature mechanical failure.
Compression connectors intended for aluminum-to-steel transitions should be selected where required. Installation crews must follow the specified stripping length, die sequence, compression force, connector orientation, and inspection procedure. Joint surfaces should be clean and prepared according to the fitting manufacturer’s instructions.
4. Manufacturing Process and Quality Control
The performance of reinforcing steel aluminum strand depends heavily on manufacturing precision. A conductor may meet its nominal material specification yet perform poorly if the wire diameters, lay lengths, tension balance, surface condition, or core alignment are inconsistent. Jiangsu Wopeng Power Technology Co., Ltd. emphasizes standardized production, controlled processing, engineering supervision, and inspection throughout the manufacturing cycle.
4.1 Raw Material Control
Production begins with the selection and verification of aluminum and steel materials. Electrical-grade aluminum must meet the required purity, conductivity, chemical composition, and mechanical characteristics. Steel-core wire must provide the specified tensile strength, dimensional accuracy, surface condition, and coating performance.
Incoming inspection may include dimensional measurement, surface examination, conductivity testing, tensile testing, coating verification, and documentation review. Raw materials are identified and managed so that different grades or batches are not unintentionally mixed during production.
For galvanized steel-core material, zinc coating quality is particularly important. The coating must be continuous and sufficiently bonded to protect the steel from atmospheric corrosion. The stated minimum zinc coating weight of 300 g/m² provides a reference point for quality control, while the final requirement should be confirmed against the applicable standard and order specification.
4.2 Aluminum Wire Drawing and Annealing
Aluminum rod is processed through drawing operations to achieve the specified wire diameter. Drawing must be controlled carefully because excessive deformation, poor lubrication, damaged dies, or unstable line speed can affect surface quality and mechanical properties.
After drawing, controlled annealing may be used to adjust the aluminum’s conductivity, ductility, and flexibility. The annealing cycle must balance electrical performance with the mechanical requirements of stranding. Excessive annealing can reduce strength, while insufficient annealing can produce a wire that is too hard or insufficiently ductile for stable stranding.
Advanced production management uses controlled temperature, residence time, line speed, and cooling conditions. Conductivity and tensile properties are checked after processing to verify that the wire is suitable for the next manufacturing stage.
4.3 Steel-Core Preparation
The steel core is prepared through processes that ensure correct diameter, surface condition, coating integrity, and tensile performance. The galvanized surface must remain free from severe scratches, flaking, contamination, and other defects that could reduce corrosion resistance or impair contact with the surrounding aluminum strands.
Core wires are arranged according to the required construction. For multi-wire cores, the individual steel wires must be balanced and aligned to create a stable central structure. The core must remain centered during the subsequent aluminum stranding operation.
4.4 Concentric Stranding
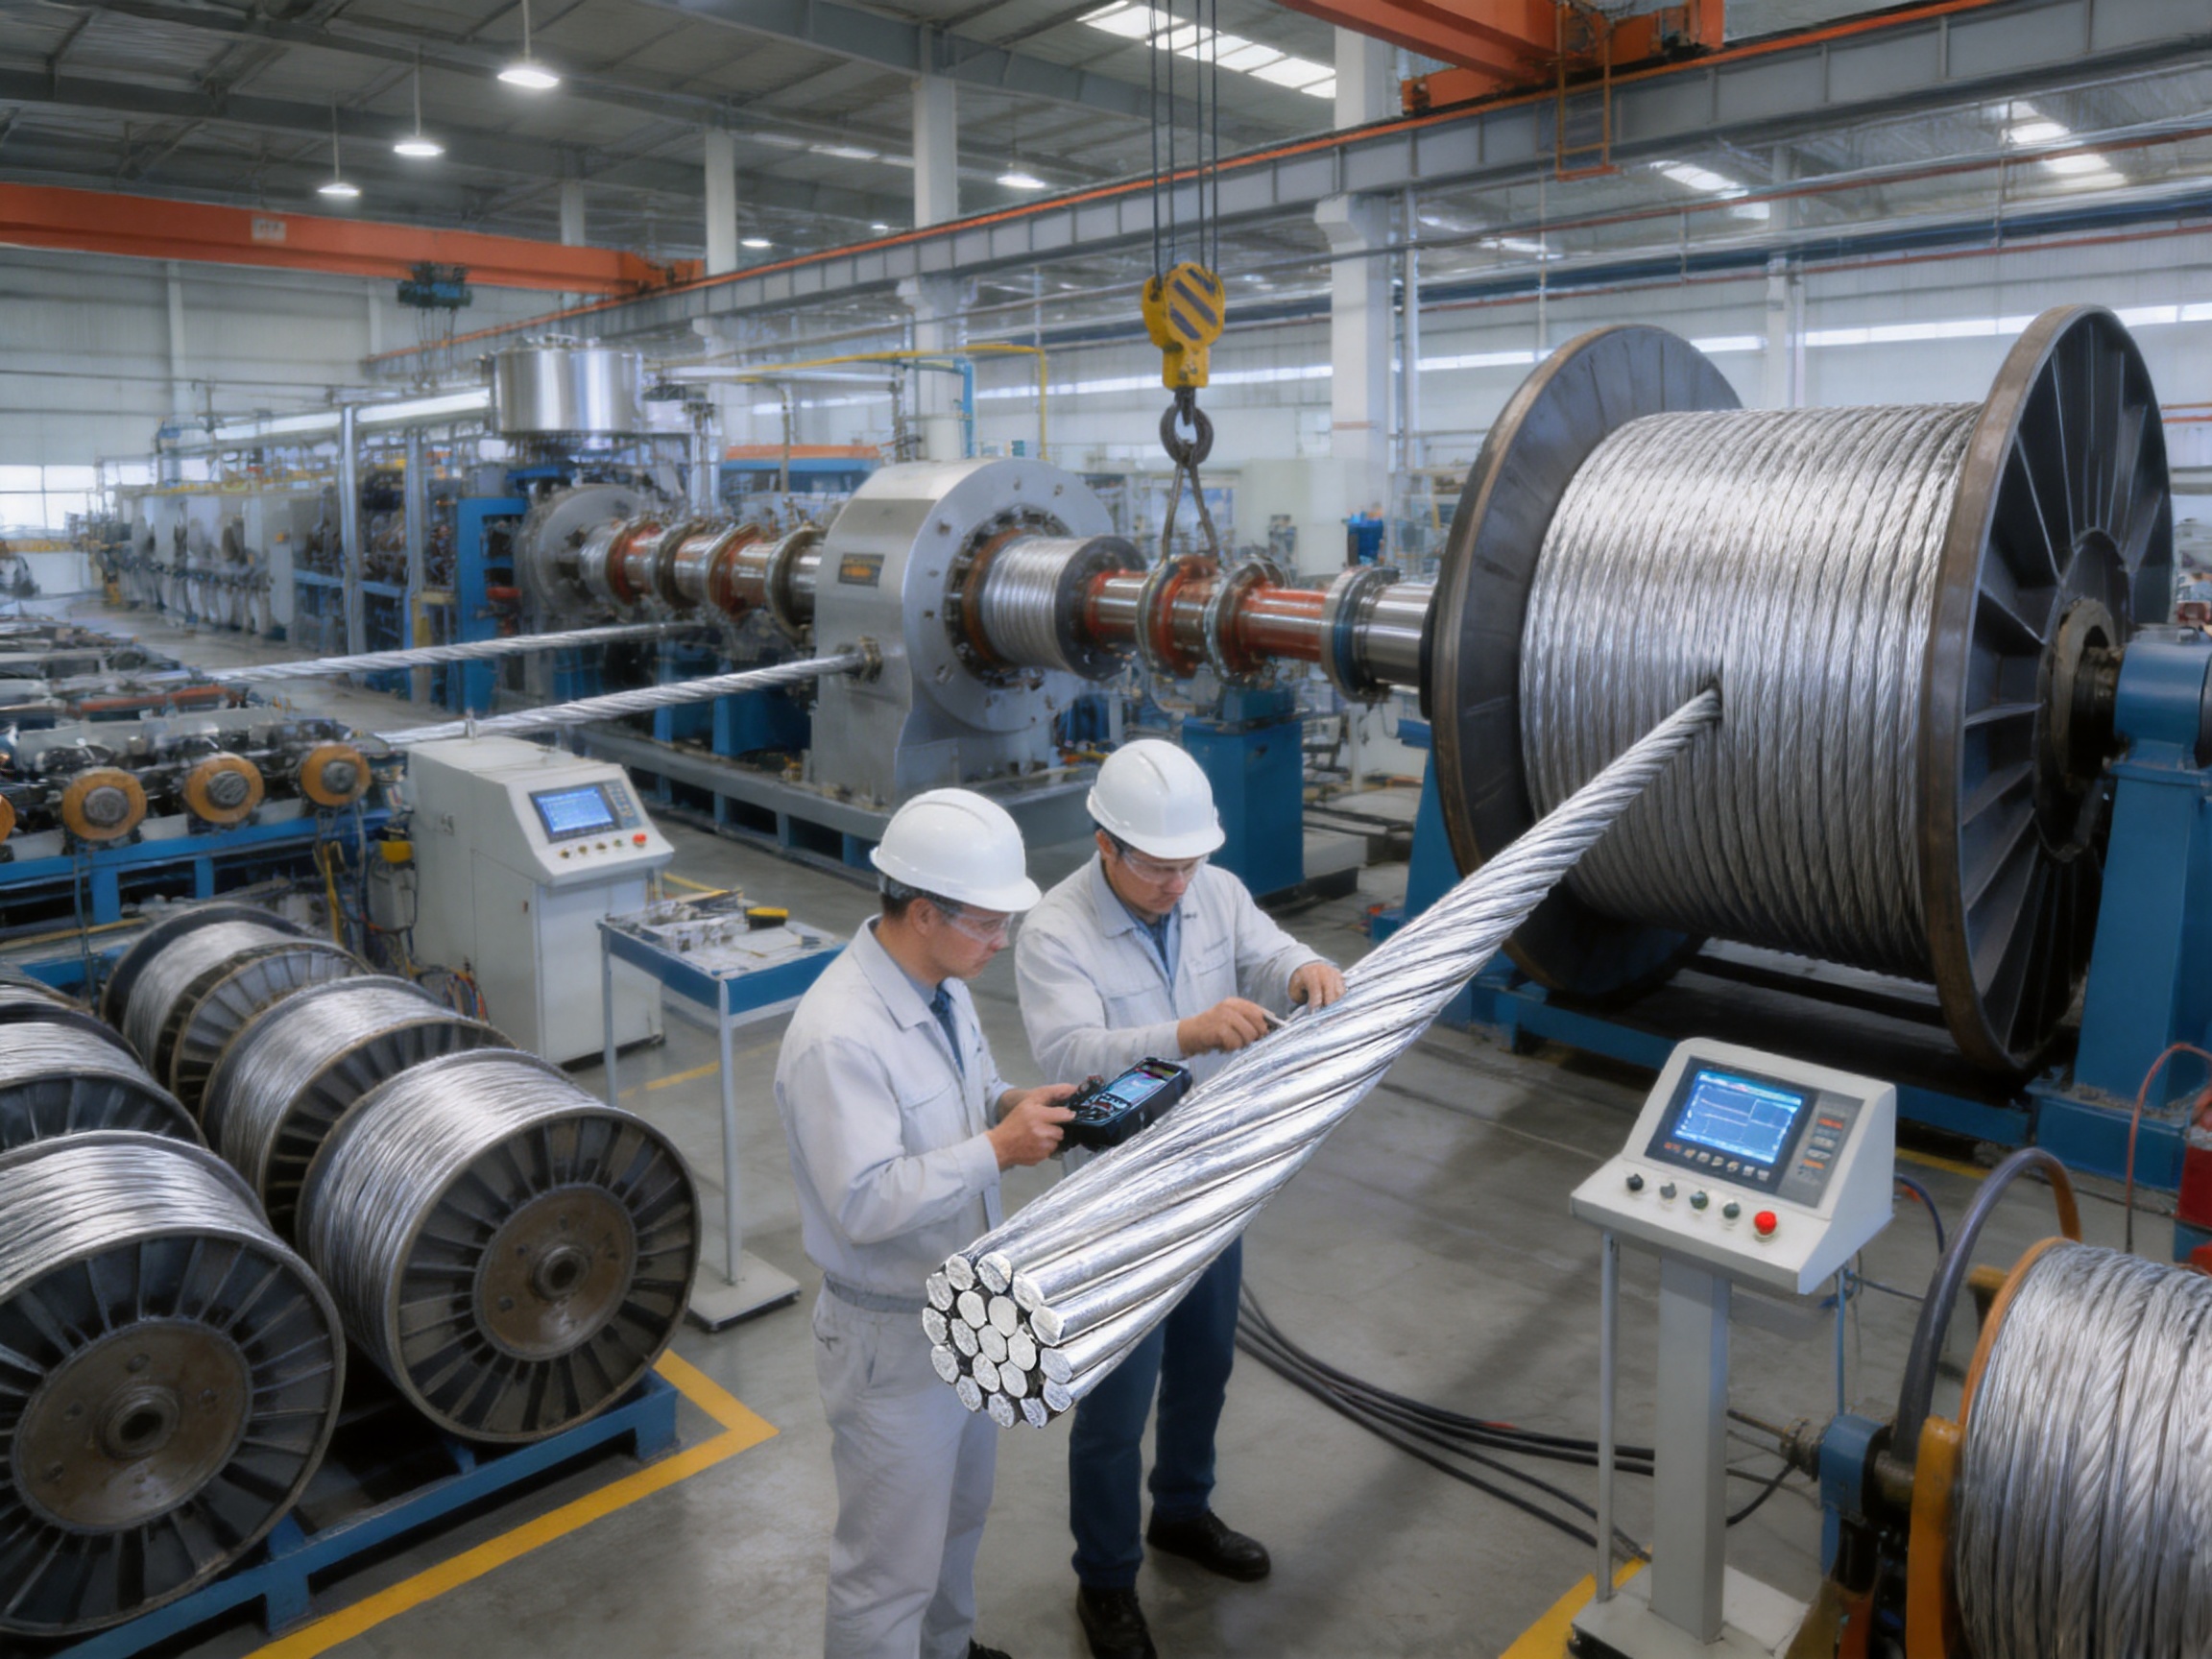
Stranding is one of the most important manufacturing stages. Aluminum wires are laid helically around the steel core in controlled layers. The lay length, direction, tension, pitch ratio, and layer arrangement determine the final diameter, flexibility, surface uniformity, and mechanical behavior of the conductor.
Scientifically designed stranding pitch ratios help distribute stress more uniformly among the wires. Balanced wire tension prevents some strands from carrying excessive load while others remain relatively loose. A stable and uniform lay also improves compatibility with clamps and compression fittings.
During production, operators and quality personnel monitor outside diameter, lay direction, pitch, strand positioning, surface condition, and reel winding. Automated or semi-automated equipment can improve repeatability and reduce variation between production batches.
4.5 Pre-Twisting and Strand Stability
Pre-twisting is used to reduce the tendency of the conductor to loosen after cutting or handling. Without adequate control, residual stress can cause strands to spring apart, shift position, or form localized irregularities. These conditions may complicate installation and reduce the reliability of fittings.
A controlled pre-twisting process helps maintain the designed geometry during transportation, unreeling, tension stringing, and service. The product information identifies strict pre-twisting control as a method for preventing strand loosening. This is particularly valuable for larger conductors and applications involving repeated handling or high installation tension.
4.6 Surface and Dimensional Inspection
Finished conductor inspection includes visual examination and dimensional checks. The outer surface should be smooth and free from broken wires, severe abrasions, contamination, sharp projections, and abnormal gaps between strands. Diameter measurements are compared with the relevant tolerances, and the conductor is examined for consistent stranding along the reel length.
Electrical resistance is measured or calculated according to the applicable method. Tensile testing confirms the mechanical performance of the complete conductor or representative components. Weight per unit length, lay characteristics, aluminum area, steel area, and coating properties may also be verified.
4.7 Inspection Systems and Production Facilities
Wopeng operates modern production lines supported by vacuum casting systems, CNC machining equipment, automated assembly technologies, and standardized inspection processes. Although these facilities serve a wider range of busbar and power-transmission products, the same manufacturing discipline benefits conductor-related production: controlled dimensions, repeatable processing, traceability, and systematic testing.
The company’s quality activities include high-voltage tests, insulation tests where applicable, mechanical verification, and routine quality checks. Third-party testing collaboration provides independent validation for selected safety and performance characteristics. This combination of internal control and external verification strengthens confidence in products intended for critical infrastructure.
5. Performance Features Under Operating Conditions
5.1 Conductivity and Resistance Stability
Electrical performance is influenced by aluminum purity, wire drawing, annealing, strand contact, operating temperature, and surface condition. High-purity aluminum and controlled processing help achieve stable conductivity. The supplied product information states that conductivity can exceed 61% IACS for the specified electrical-grade aluminum after annealing.
Under high-frequency conditions, the product description identifies a measured skin-effect coefficient below 1.05 and limits the increase in AC resistance to within 8%. These characteristics may be relevant in systems where alternating-current effects and conductor geometry influence losses. Engineers should verify the test basis, frequency, temperature, and conductor construction before applying the values to a particular system.
Thermal cycling can cause expansion and contraction of the aluminum layers and steel core. A well-controlled composite structure minimizes the risk of permanent strand displacement, connection loosening, and progressive resistance increase. The supplied information states that conductivity degradation does not exceed 2% after 100 thermal cycles under the specified test conditions.
5.2 Tensile Strength and Sag Control
The steel core carries a significant portion of the tensile load. This helps the conductor maintain its position between supports and reduces the risk of excessive sag. Maintaining acceptable sag is essential for preserving phase-to-phase, phase-to-ground, road, building, and vegetation clearances.
The final sag profile depends on conductor temperature, span length, support elevation, installation tension, creep, wind, ice, and the elastic properties of the conductor. A higher tensile rating provides more design flexibility, but it does not eliminate the need for accurate sag-tension calculations.
5.3 Vibration Resistance
Overhead conductors can experience aeolian vibration caused by steady wind flowing across the conductor. Repeated small-amplitude vibration may cause fatigue at suspension clamps, spacers, dead-end fittings, and points where the conductor is constrained.
Uniform stranding, correct lay geometry, balanced tension, and properly selected vibration dampers contribute to long-term reliability. The product information references a two-million-cycle wind-induced vibration fatigue test, demonstrating the importance placed on dynamic durability. Actual line design should also include suitable vibration-control hardware based on span length, terrain, wind conditions, and conductor diameter.
5.4 Ice and Wind Performance
Ice accumulation increases conductor weight and aerodynamic exposure. Wind acting on an iced conductor can create high transverse and longitudinal forces. The steel core helps the conductor withstand these additional mechanical loads, while the aluminum outer layers continue to provide the conductive path.
The supplied product information identifies testing under an ice coating load of 30 mm. Such a test provides useful evidence of environmental adaptability, but the design ice thickness for a project must be determined from local meteorological data, grid standards, and risk assessment.
5.5 Thermal Expansion and Temperature Range
Aluminum and steel have different coefficients of thermal expansion. The composite structure must therefore be designed and manufactured to manage differential movement between the aluminum layers and the steel core. Proper stranding and material control reduce the risk of excessive internal stress or strand displacement during temperature changes.
The product is described as suitable for environmental temperatures from -40°C to +80°C, with stable thermal expansion behavior within that range. The allowable continuous conductor temperature, however, may be different from the ambient temperature range and must be established through the project’s thermal calculation.
5.6 Salt Spray and Ultraviolet Exposure
Outdoor conductors may be exposed to salt spray, moisture, dust, industrial pollutants, and ultraviolet radiation for decades. Aluminum offers good atmospheric corrosion resistance, while the galvanized steel core provides an additional protective layer.
The product information reports more than 95% tensile-strength retention after 5,000 hours of salt-spray testing and no significant surface degradation after 5,000 hours of UV aging. These results support use in demanding outdoor environments, although regular inspection remains advisable in coastal, chemical, and heavily polluted locations.
6. Applications in Power Transmission and Distribution
6.1 Overhead Transmission Lines
Overhead transmission lines are the most recognized application for steel-reinforced aluminum conductors. These lines often require long spans, high reliability, stable clearances, and resistance to severe weather. The conductor’s steel core provides mechanical support, while the aluminum strands carry the electrical current.
For new transmission projects, the conductor can be selected according to the required power-transfer capacity and span conditions. For refurbishment projects, the outside diameter and mechanical characteristics must be compared with existing insulators, clamps, towers, and line hardware.
6.2 High-Tension Distribution Lines
High-tension distribution networks benefit from a conductor that can maintain mechanical stability over varying terrain and weather conditions. Sag control is especially important in areas with long spans between poles, road crossings, rivers, railways, or industrial facilities.
The conductor’s strength-to-weight balance can help reduce deflection and improve line reliability. Its range of available cross-sections also allows utilities to select a construction appropriate for current demand, fault levels, expected network growth, and installation constraints.
6.3 Ground Wires and Shield Wires
Steel-reinforced aluminum strand may also be used as a ground wire or shield wire at the top of transmission towers. In this role, it helps protect phase conductors from lightning by providing a preferred path for surge current toward the tower grounding system.
Ground-wire selection must consider lightning performance, fault-current capacity, mechanical tension, tower geometry, grounding resistance, and coordination with protective devices. The conductor’s mechanical strength is important because the shield wire is exposed to the same wind, ice, and vibration conditions as the phase conductors.
6.4 Long Crossings and Special Structures
River crossings, ravines, highways, railway corridors, and areas with limited tower locations may require longer spans than ordinary distribution routes. A steel-reinforced conductor can be considered for these applications because its core supports higher mechanical loading and helps manage sag.
Special crossing projects often require detailed structural calculations, customized fittings, controlled stringing procedures, and enhanced inspection. The conductor should be selected together with the crossing tower, insulator, damper, and hardware system rather than as an isolated component.
6.5 Damping Wires and Hardware Connections
The product is also identified for use as a damping wire in hardware connection applications, including damping-type end caps. In these applications, the conductor’s structured construction provides a combination of mechanical support and electrical continuity.
Because damping components may experience repeated movement and localized stress, the wire must be compatible with the end cap, clamp, or connector design. Proper dimensional control is important to ensure a secure fit and predictable performance.
6.6 Industrial and Renewable-Energy Infrastructure
Industrial plants, wind-power facilities, substations, and large infrastructure projects often require reliable conductors in areas exposed to vibration, temperature change, and outdoor environmental conditions. Wopeng’s experience with wind-power tube busbars, substations, and power-transmission equipment gives the company an understanding of the interface between conductors, busbars, support structures, and connection systems.
For wind-energy installations, conductor and busbar selection must account for mechanical vibration, variable loads, limited maintenance access, and the need for compact, reliable power transmission. The correct product may be a reinforcing strand, tubular busbar, cast-resin busbar, or a combination of systems depending on the electrical architecture.
7. Advantages Compared with Competing Conductor Options
Several conductor types are available for power networks, including all-aluminum conductors, aluminum alloy conductors, copper conductors, and other reinforced composite designs. Reinforcing steel aluminum strand is not automatically the best choice for every project, but it offers a strong combination of properties for applications where mechanical reinforcement is a priority.
| Performance Factor | Reinforcing Steel Aluminum Strand | All-Aluminum Conductor | Copper Conductor |
| Mechanical strength | High because of the steel core | Lower for comparable general constructions | Good, but high density affects total weight |
| Electrical conductivity | High through the aluminum layers | High through the complete aluminum section | Very high |
| Weight efficiency | Balanced strength-to-weight performance | Lightweight but mechanically limited in some long spans | Heavy for equivalent conductor volume |
| Long-span suitability | Very suitable when properly designed | More limited in high-load conditions | Possible, but structural loading can increase |
| Corrosion behavior | Aluminum exterior and protected steel core | Good atmospheric resistance | Generally good but requires compatible connections |
| Material cost considerations | Often provides a practical balance | Competitive for moderate mechanical requirements | Higher material cost in many markets |
| Typical use | Transmission, distribution, shielding, and special spans | Distribution and applications with moderate tension | Specialized high-conductivity systems and equipment |
7.1 Compared with All-Aluminum Conductors
All-aluminum conductors can be lightweight and electrically efficient, but they may not provide the mechanical strength needed for long spans, severe weather, or high installation tension. Reinforcing steel aluminum strand adds a steel core without abandoning the advantages of aluminum outer layers.
For a project with short spans and moderate loading, an all-aluminum design may be sufficient and economical. For a project with long spans, high wind, ice, or strict sag requirements, the steel-reinforced alternative may offer a more favorable overall solution.
7.2 Compared with Copper Conductors
Copper has excellent conductivity and is widely used in equipment, cables, and busbar systems. However, copper is denser and often more expensive than aluminum. In long overhead lines, a copper conductor can increase structural loading and transportation requirements.
Reinforcing steel aluminum strand uses aluminum for the main conductive area and steel for reinforcement, producing a lower-density alternative with substantial tensile performance. Copper may still be preferred where extremely high conductivity, compact equipment connections, or specific short-circuit requirements dominate the design.
7.3 Compared with Basic Low-Cost Alternatives
Low-cost conductors may appear attractive when judged only by purchase price. However, the total project cost also includes towers, foundations, fittings, installation equipment, maintenance, outage risk, line losses, and replacement costs. A standardized conductor with stable dimensions and verified mechanical properties can reduce installation complications and improve lifecycle value.
Wopeng’s approach emphasizes controlled manufacturing, traceability, technical documentation, and application support rather than treating the conductor as an unqualified commodity. This is particularly important for power infrastructure in which a single weak connection or defective strand can create significant operational consequences.
8. Installation and Maintenance Recommendations
8.1 Transportation and Storage
Reels should be handled with suitable lifting equipment and protected from impact, uncontrolled rolling, standing water, and contamination. The conductor should remain securely wound and should not be dragged across the ground. Reel flanges, wrapping, and markings should be inspected when the material arrives.
Storage areas should be dry, stable, and free from corrosive chemicals. Reels should be positioned to prevent deformation and should be rotated only according to the approved handling procedure. Before installation, the conductor should be checked for visible damage, broken strands, abnormal looseness, and contamination.
8.2 Tension Stringing
Tension stringing is commonly used to control conductor clearance and prevent contact with the ground or obstacles. The steel core allows the conductor to withstand higher tension than many all-aluminum alternatives, but the approved maximum tension must never be exceeded.
Stringing blocks must have a suitable diameter and groove profile. Their condition should be checked before use to prevent crushing, abrasion, or strand displacement. Tensioners, pullers, swivels, socks, and gripping devices must be compatible with the conductor diameter and construction.
During stringing, crews should control running speed, avoid sudden tension changes, monitor reel rotation, and prevent the conductor from contacting sharp edges. If the conductor becomes kinked, birdcaged, crushed, or severely abraded, the damaged section should be evaluated by qualified personnel before continuation.
8.3 Sagging and Clipping-In
Final sag must be established using the approved sag-tension tables and actual project conditions. Temperature measurement should be accurate, and the conductor should be allowed to stabilize as required by the installation procedure.
Clamps should be installed without twisting or crushing the outer aluminum strands. Suspension points must be correctly aligned, and dead-end fittings must be compressed using the specified die sequence and equipment. Incorrect compression can reduce both electrical and mechanical performance.
8.4 Connector Installation
Connections between aluminum and steel components require special attention. The connector must be suitable for the composite conductor and rated for the expected current, tensile load, temperature, and environmental exposure.
Contact surfaces should be prepared according to the connector instructions. Oxide removal, joint compound, bolt torque, compression sequence, and sealing practices must be controlled. After installation, the connector should be inspected for correct dimensions, complete compression, surface damage, and proper alignment.
8.5 Inspection During Service
Routine inspection should look for broken or displaced strands, corrosion, connector overheating, unusual sag, vibration damage, birdcaging, abrasion, and evidence of lightning or fault exposure. Thermal imaging may help identify high-resistance connections, especially in heavily loaded circuits.
Coastal and industrial environments may require more frequent inspection. Areas near suspension clamps, spacers, dead ends, and dampers deserve particular attention because local mechanical stress and movement are concentrated at these points.
9. Why Manufacturing Capability Matters to Buyers
For a conductor used in critical power infrastructure, product quality depends on more than nominal specifications printed on a datasheet. Buyers should consider the manufacturer’s ability to control raw materials, maintain dimensional consistency, verify electrical and mechanical performance, manage production traceability, and provide technical documentation.
9.1 Integrated Power-Equipment Experience
Jiangsu Wopeng Power Technology Co., Ltd. was founded in 2018 as a high-tech enterprise focused on high- and low-voltage busbar systems and power-transmission solutions. Its portfolio includes 35kV epoxy-resin vacuum-cast tubular busbars, low-voltage cast-resin busways, copper and aluminum tubular busbars, wind-power tube busbars, compact busbar systems, and sliding contact line systems.
This product breadth is valuable because conductor projects rarely exist in isolation. A transmission or distribution system may include busbar interfaces, transformer connections, substation equipment, wind-power collection systems, grounding arrangements, and customized mechanical supports. A manufacturer familiar with these interfaces can better understand the practical requirements of the complete electrical system.
9.2 Engineering and Customization
Different projects may require different aluminum-to-steel ratios, outer diameters, delivery lengths, conductor constructions, fittings, or inspection documents. Engineering support helps customers select a suitable product rather than simply choosing the largest available size.
Customization may include construction adjustments within the applicable standard, reel and delivery planning, matching connectors, technical drawings, test documentation, and application guidance. Customization must remain controlled and documented so that changes do not compromise standard compliance or field compatibility.
9.3 Modern Production and Testing
Wopeng operates production lines equipped with vacuum casting systems, CNC machining equipment, and automated assembly technologies. These capabilities support precision manufacturing across the company’s busbar and power-equipment range. Standardized testing includes high-voltage testing, insulation testing where applicable, mechanical verification, and routine quality inspection.
Cooperation with third-party institutions provides an additional level of performance verification. Independent testing is particularly useful for customers working on utility, industrial, renewable-energy, rail-transit, and large commercial projects that require documented compliance and traceable quality records.
9.4 Application Experience
Wopeng products operate across more than 17 provinces and key industrial sectors. This field experience exposes the company to varied environmental conditions, installation methods, operating loads, and customer requirements. Feedback from real applications can support continuous improvement in product design, manufacturing processes, inspection procedures, and technical service.
10. Recommended Purchasing Checklist
Before ordering reinforcing steel aluminum strand, buyers should prepare a complete technical specification. The following points help reduce selection errors and improve project coordination.
Specify the required nominal aluminum and steel-core cross-sectional areas.
Confirm the applicable manufacturing standard, edition, and acceptance criteria.
Define the required electrical resistance, conductivity, current capacity, and operating temperature.
Provide span lengths, support conditions, maximum design tension, wind load, and ice load.
Confirm required outside diameter and compatibility with existing fittings.
Specify the required reel length, total quantity, delivery schedule, and packaging method.
Request material certificates and inspection reports for aluminum and steel-core components.
Confirm tensile-strength, resistance, dimensional, coating, and surface-quality requirements.
Identify whether the conductor will be used for phase conductors, ground wires, shield wires, damping wires, or hardware connections.
Review recommended installation tools, tension limits, connector types, and maintenance procedures.
Consider environmental exposure, including salt spray, pollution, ultraviolet radiation, ice, and temperature extremes.
Request technical support for unusual spans, special crossings, renewable-energy projects, and customized fittings.
11. Frequently Asked Questions
Q1: What is the main purpose of the steel core?
The steel core provides mechanical reinforcement. It increases tensile strength, supports longer spans, reduces excessive sag, and improves resistance to wind, ice, and installation loads. The aluminum strands surrounding the core provide most of the electrical conductivity.
Q2: Is reinforcing steel aluminum strand the same as an all-aluminum conductor?
No. An all-aluminum conductor uses aluminum throughout its cross-section, while reinforcing steel aluminum strand contains a steel core surrounded by aluminum strands. The steel core gives the reinforced design higher mechanical strength, particularly for long-span and high-load applications.
Q3: How should the conductor size be selected?
Selection should consider continuous current, short-circuit conditions, voltage drop, span length, sag requirements, wind and ice loads, operating temperature, tower capacity, outside diameter, and fitting compatibility. The largest cross-section is not always the most economical or technically appropriate choice.
Q4: Can this product be used in coastal environments?
Yes, it can be considered for coastal environments because the aluminum outer layers provide good atmospheric corrosion resistance and the steel core can be galvanized for additional protection. Coastal applications still require suitable connectors, sealing, inspection, and consideration of salt concentration and pollution severity.
Q5: What is the typical conductivity of the product?
The supplied information identifies electrical-grade aluminum with conductivity above 61% IACS after controlled annealing. Complete-conductor conductivity depends on the aluminum-to-steel ratio and the calculation method. The final value should be confirmed in the technical documentation for the selected construction.
Q6: What delivery length is available?
The general delivery length is less than 2,000 meters. Exact reel length depends on conductor size, transportation requirements, project quantity, packaging limitations, and customer specifications.
Q7: Is the product suitable for high-tension distribution lines?
Yes. Its combination of aluminum conductivity and steel-core tensile strength makes it suitable for many high-tension distribution applications. The final selection must be checked against the network voltage, current, span, support structure, weather loads, and applicable utility standards.
Q8: Can it be used as a ground or shield wire?
It can be used for ground-wire or shield-wire applications when the selected construction meets the required mechanical, fault-current, lightning, and environmental conditions. Grounding-system design must also include tower grounding resistance and coordination with the protection system.
Q9: What fittings should be used?
Use suspension clamps, dead-end fittings, compression connectors, dampers, and other accessories specifically designed for the selected aluminum-and-steel conductor construction. Aluminum-to-steel transition connectors may be required to ensure mechanical security and low electrical resistance.
Q10: What makes the manufacturer suitable for customized projects?
Jiangsu Wopeng Power Technology Co., Ltd. combines engineering experience in high- and low-voltage busbar systems with modern production equipment, standardized inspection, mechanical and electrical testing, and experience serving power generation, substations, wind energy, industrial manufacturing, rail transit, and commercial infrastructure. This combination supports customized product selection and system-level technical coordination.
12. Conclusion
Reinforcing steel aluminum strand is a dependable composite conductor for applications that require both electrical efficiency and mechanical strength. Its aluminum strands provide the primary current path, while the steel core supports high tensile loads, long spans, sag control, and resistance to severe environmental conditions.
The product range from 10/2 mm² to 240/30 mm² provides flexibility for different power-transmission and distribution requirements. Standardized construction, controlled aluminum annealing, galvanized steel-core protection, balanced stranding, pre-twisting, dimensional inspection, and mechanical and electrical verification all contribute to stable performance.
Compared with all-aluminum alternatives, the reinforced design offers greater tensile capability and better suitability for long-span or high-load conditions. Compared with copper, it provides a practical combination of aluminum conductivity, steel reinforcement, lower density, and cost efficiency for many overhead applications.
The manufacturer’s broader experience in tubular busbars, cast-resin busways, wind-power busbars, compact busbar systems, and sliding contact line systems strengthens its ability to understand complete power-transmission systems rather than isolated conductor requirements. Modern production equipment, standardized quality procedures, third-party testing cooperation, and field experience across multiple industries provide additional support for customers seeking reliable and customized solutions.
For the best result, conductor selection should be based on a complete engineering review that includes electrical loading, mechanical span, weather conditions, fittings, installation procedures, environmental exposure, and long-term maintenance. When these factors are coordinated correctly, reinforcing steel aluminum strand can provide a robust, efficient, and durable solution for modern power infrastructure.
References
1. GB1179-83, Standard Specification for Stranded Wires and Conductors Used in Electrical Applications.
2. IEC 61089, Round Wire Concentric Lay Overhead Electrical Stranded Conductors.
3. ASTM B399, Standard Specification for Concentric-Lay-Stranded Aluminum Alloy 6201-T81 Conductors.
4. International Annealed Copper Standard, Reference Requirements for Electrical Conductivity.
5. Overhead Line Design Practices, including sag-tension calculation, conductor vibration control, and weather-load assessment.
6. Manufacturer technical data for reinforcing steel aluminum strand, including dimensional, electrical, mechanical, environmental, and delivery specifications.
7. Manufacturer quality and production information for high- and low-voltage busbar systems and related power-transmission equipment.
Product: Reinforcing Steel Aluminum Strand


-
 +86-180 3625 3000
-
 admin@wpbusbar.com
-
 No. 8, Yanjin Road, Chengxi Industrial Park, Shanyang Town, Baoying County, Yangzhou City, Jiangsu Province, China
Copyright © Jiangsu Wopeng Power Technology Co., Ltd.
All Rights Reserved.
 Custom Insulated Bus Bar Manufacturer
Tubular Busbar System Factory