

 EN

 English
 русский
 Français
 Español
 عربى
Ultra-High Voltage Magnesium-Aluminum Alloy Tubular Bus Bar: Design, Performance, Manufacturing, and Applications
Content
- 1 1. What Is an Ultra-High Voltage Magnesium-Aluminum Alloy Tubular Bus Bar?
- 2 2. Why Tubular Geometry Matters in Ultra-High Voltage Systems
- 3 3. Technical Advantages of Magnesium-Aluminum Alloy
- 4 4. Electrical Performance and Safety Characteristics
- 5 5. Comparison with Conventional Busbar Solutions
- 6 6. Advanced Manufacturing Process
- 7 7. Manufacturing Strengths of Jiangsu Wopeng Power Technology
- 8 8. Main Application Scenarios
- 9 9. Customization Options
- 10 10. Installation and System Integration
- 11 11. Service Life and Reliability
- 12 12. Quality Evaluation and Selection Criteria
- 13 13. Frequently Asked Questions
- 13.1 Q1. What is the main advantage of a magnesium-aluminum alloy tubular busbar?
- 13.2 Q2. Can this busbar be used at 500 kV and higher?
- 13.3 Q3. Is it lighter than a copper busbar?
- 13.4 Q4. How does it compare with ordinary aluminum busbars?
- 13.5 Q5. What operating temperature can it withstand?
- 13.6 Q6. Can it be installed outdoors?
- 13.7 Q7. Can it be used in offshore wind power projects?
- 13.8 Q8. What insulation processes are compatible with the conductor?
- 13.9 Q9. Is the tubular busbar seamless?
- 13.10 Q10. What is the maximum support span?
- 13.11 Q11. How long can the product last?
- 13.12 Q12. What information should be provided when requesting a quotation?
- 13.13 Q13. Does the manufacturer provide customized OEM solutions?
- 13.14 Q14. What quality tests are important for an ultra-high voltage busbar?
- 14 14. Why Choose an Integrated Tubular Busbar Manufacturer?
- 15 15. Conclusion
- 16 References
- 17 Product: Ultra-high Voltage Magnesium-Aluminum Alloy Tubular Bus Bar
Ultra-high voltage power systems require conductors that can carry substantial electrical current while maintaining mechanical stability, insulation reliability, thermal performance, and long-term resistance to environmental exposure. As transmission networks expand toward 500 kV, 750 kV, ±800 kV, and 1,000 kV applications, conventional conductor arrangements may become increasingly demanding in terms of weight, support structure, heat dissipation, installation, and lifecycle maintenance.
The ultra-high voltage magnesium-aluminum alloy tubular bus bar is designed to address these requirements. It combines the low density and conductivity advantages of aluminum with the improved strength and corrosion resistance provided by carefully controlled alloying elements. Its tubular structure further improves rigidity, current distribution, heat dissipation, and resistance to mechanical deformation compared with many traditional solid or assembled busbar configurations.
Jiangsu Wopeng Power Technology Co., Ltd. develops and manufactures high- and low-voltage busbar systems, including magnesium-aluminum alloy tubular bus bars for demanding power transmission and transformation environments. Through alloy selection, horizontal hot top casting, transverse piercing hot rolling, thermomechanical treatment, cold drawing, precision machining, insulation compatibility control, and standardized inspection, the company provides customized conductive solutions for substations, power plants, renewable energy projects, industrial facilities, rail transit systems, and other high-current applications.
This article explains the construction, material technology, electrical and mechanical advantages, manufacturing process, application conditions, customization options, installation considerations, and quality requirements of ultra-high voltage magnesium-aluminum alloy tubular bus bars.
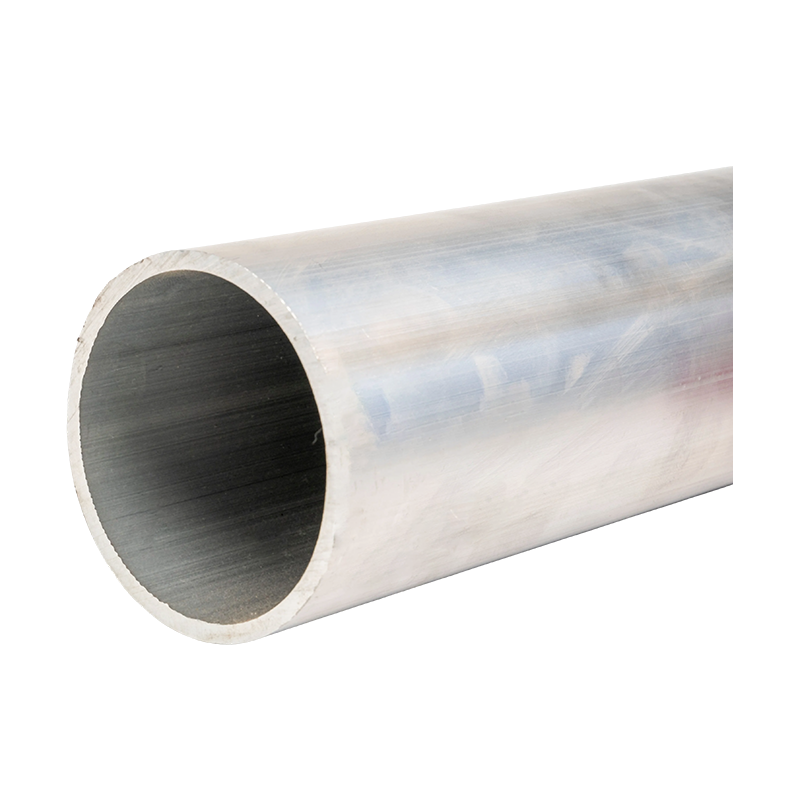
Ultra-high Voltage Magnesium-Aluminum Alloy Tubular Bus Bar
1. What Is an Ultra-High Voltage Magnesium-Aluminum Alloy Tubular Bus Bar?
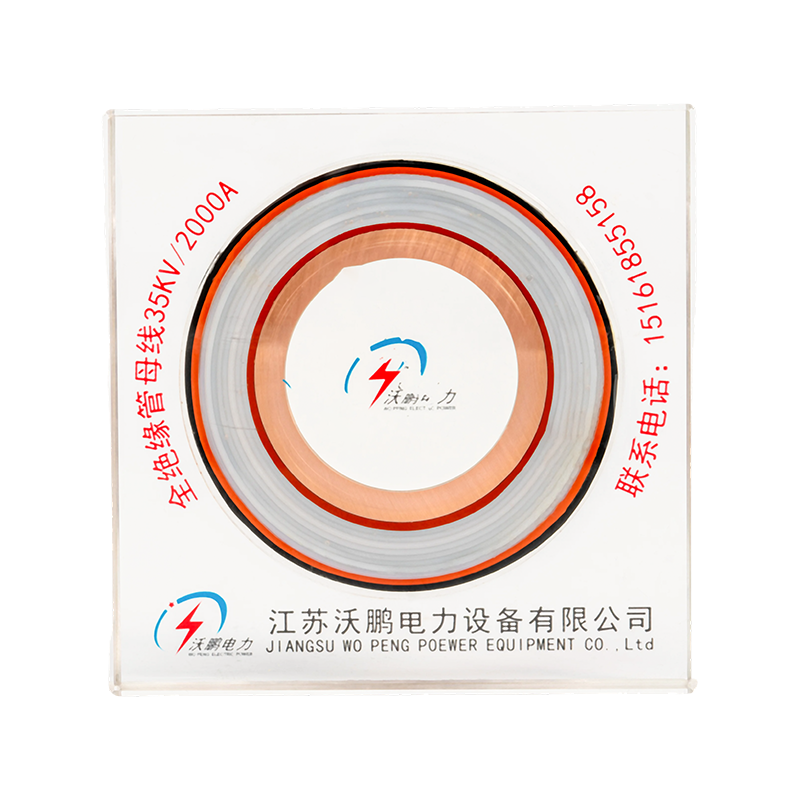
An ultra-high voltage magnesium-aluminum alloy tubular bus bar is a tubular electrical conductor used to transmit and distribute high currents in high-voltage and ultra-high voltage power systems. The conductor is manufactured from a magnesium-aluminum alloy or a closely related aluminum alloy formulation selected for the required balance of electrical conductivity, strength, heat resistance, corrosion resistance, and processability.
Unlike a conventional flat busbar, a tubular bus bar has a hollow circular or specially engineered cross-section. This geometry provides a high ratio of structural stiffness to material weight. It also creates a large external surface area relative to the conductor mass, which supports natural or forced heat dissipation. In outdoor substations and large current transmission systems, the tubular structure can help improve rigidity, reduce deflection, and maintain a more stable electrical clearance.
The product can be used as a principal current-carrying connection between transformers, circuit breakers, disconnectors, generators, converter equipment, transmission line terminals, and other high-voltage apparatus. Depending on system design, the bus bar may be installed as a single conductor, a multi-conductor arrangement, a shielded tubular bus system, or an insulated tubular assembly.
1.1 Material Options
The product range can include several aluminum-based alloy families according to the required voltage class, current capacity, mechanical loading, operating temperature, and environmental conditions. Typical material options include 6063G aluminum-magnesium alloy, LF21Y aluminum-manganese alloy, 6R05 rare-earth aluminum alloy, and 2A14 heat-resistant aluminum alloy.
Each alloy offers a different combination of performance characteristics. Aluminum-magnesium alloys are valued for their corrosion resistance, moderate-to-high strength, and practical forming properties. Aluminum-manganese alloys can provide a useful balance of conductivity, workability, and environmental durability. Rare-earth aluminum alloys are developed to improve microstructural stability and mechanical performance, while heat-resistant alloys are selected for applications requiring stable operation at elevated temperatures.
Alloy selection should be made according to the complete electrical and mechanical design rather than by conductivity alone. A busbar that provides excellent conductivity but insufficient strength may require excessive support structures. Conversely, a high-strength alloy with inadequate conductivity may create unnecessary temperature rise and transmission loss. The purpose of the magnesium-aluminum alloy design is to optimize these properties as an integrated system.
1.2 Voltage and Current Applications
Ultra-high voltage tubular bus bars are intended for demanding power system applications that may include 220 kV, 500 kV, 750 kV, ±800 kV, and 1,000 kV projects. The final rating depends on conductor dimensions, alloy grade, insulation or shielding arrangement, ambient conditions, installation geometry, clearance requirements, and the applicable technical standards.
For certain product configurations, the rated current can reach approximately 12,000 A, while electrical conductivity may reach or exceed 60% IACS. Working temperature ranges can extend from approximately -40°C to 150°C, with specially selected heat-resistant alloys and system designs supporting higher short-term or continuous temperature requirements. These values should be confirmed through project-specific engineering calculations, type tests, and acceptance documentation.
2. Why Tubular Geometry Matters in Ultra-High Voltage Systems
Conductor geometry has a direct influence on electrical field distribution, thermal behavior, mechanical stiffness, corona performance, and installation requirements. In ultra-high voltage equipment, these factors must be considered together because an improvement in one area can affect the others.
2.1 Efficient Use of Material
A tubular cross-section places material away from the neutral axis, increasing bending stiffness without requiring the same mass as a solid conductor of equivalent external diameter. This is especially valuable when busbar spans are long or when the conductor must withstand wind, vibration, seismic forces, transport loads, and short-circuit electromagnetic forces.
The hollow construction can reduce dead weight while maintaining dimensional rigidity. Lower weight may allow the use of lighter support structures, smaller lifting equipment, and more efficient installation methods. It can also reduce the long-term mechanical load imposed on insulators, frames, foundations, and connection points.
2.2 Improved Heat Dissipation
The outer surface of a tubular conductor is continuously exposed to the surrounding air. Under natural convection, heat generated by current flow can be transferred more efficiently from the conductor surface to the atmosphere. The tubular profile can therefore support a favorable balance between current-carrying capacity and temperature rise.
Thermal performance depends on conductor diameter, wall thickness, alloy conductivity, surface condition, solar radiation, wind speed, ambient temperature, installation orientation, and nearby equipment. A properly engineered tubular busbar system can use these factors to achieve high current capacity without relying solely on increased conductor mass.
2.3 Stable Electric Field Distribution
A smooth tubular surface allows the electric field to be distributed more uniformly than it may be on sharp-edged or irregular conductor arrangements. This can help reduce local electric field concentration and support corona control, particularly when the external surface is manufactured to a consistent dimensional and surface-finish standard.
For ultra-high voltage installations, electric field design also includes end fittings, joints, supports, shielding rings, connection hardware, and transitions to other equipment. The tubular conductor is therefore only one part of a complete field-control system. Proper engineering and installation are essential to achieving the intended performance.
2.4 Better Mechanical Stability
The circular tubular structure provides strong resistance to bending, vibration, and localized deformation. This characteristic is useful in outdoor substations, wind power facilities, high-altitude stations, coastal installations, and projects where the conductor must cross a relatively large support span.
Under suitable design conditions, the maximum support span can reach approximately eight meters. The actual allowable span must be determined by structural calculations that consider conductor diameter, wall thickness, support arrangement, wind pressure, ice load, seismic acceleration, thermal expansion, short-circuit forces, and permissible deflection.
3. Technical Advantages of Magnesium-Aluminum Alloy
3.1 Reduced Weight Compared with Copper
Copper has excellent electrical conductivity and is widely used in power equipment. However, copper busbars are substantially heavier than aluminum-based conductors. The weight of a traditional copper busbar may be approximately 25–30 kg per meter in certain comparable arrangements, while the magnesium-aluminum alloy tubular busbar described for UHV applications may be approximately 8–12 kg per meter, depending on dimensions and material grade.
Lower conductor weight can reduce the requirements for support steelwork, lifting equipment, transport capacity, and foundation loading. It can also simplify assembly in locations where access is restricted or where construction work must be completed within a limited outage window.
Weight reduction is particularly important for long busbar runs, elevated structures, renewable energy projects, offshore platforms, and rail transportation systems. A lighter conductor can reduce both direct material costs and indirect engineering costs associated with structural reinforcement and installation logistics.
3.2 Higher Strength Than Ordinary Aluminum
Ordinary aluminum provides good conductivity and low density, but its mechanical strength and high-temperature stability may not be sufficient for every ultra-high voltage application. Magnesium, manganese, rare-earth elements, and heat-resistant alloying systems can improve strength, grain stability, corrosion resistance, and resistance to deformation.
Magnesium-aluminum alloy tubular bus bars are designed to withstand tensile stress, bending loads, vibration, and thermal expansion while preserving dimensional accuracy. Typical tensile strength values for selected products may fall within a range of approximately 180–250 MPa. The final mechanical properties depend on alloy grade, heat treatment, wall thickness, cold-drawing reduction, and quality-control requirements.
3.3 High Electrical Conductivity
Although copper remains a reference material for electrical conductivity, aluminum-based alloys can provide a favorable combination of conductivity and low density. The high specific conductivity of aluminum makes it possible to carry substantial current with a relatively low conductor weight.
In a tubular busbar, electrical performance is also influenced by wall thickness, cross-sectional area, joint resistance, surface condition, conductor length, and connection design. Precision manufacturing helps maintain consistent wall thickness and dimensional tolerances, reducing variations in current distribution and contact performance.
3.4 Heat Resistance
Power transmission equipment may experience continuous loading, emergency loading, short-circuit events, high ambient temperatures, solar heating, and restricted ventilation. The use of heat-resistant or rare-earth aluminum alloys helps maintain mechanical and electrical stability when operating temperatures rise.
Depending on the alloy and design, the product can support operating temperatures in the range of approximately 150°C to 200°C. This capability can provide additional design margin for high-current systems. Thermal limits must nevertheless be established through calculations and verified through the relevant tests because insulation, joint materials, fittings, and support components may have lower temperature limits than the conductor itself.
3.5 Corrosion Resistance
Outdoor busbar systems may be exposed to humidity, rain, ultraviolet radiation, industrial pollutants, salt spray, condensation, and temperature cycling. Aluminum naturally forms a protective oxide layer, and alloy optimization and surface treatment can further improve corrosion resistance.
Enhanced corrosion resistance is especially useful in coastal substations, offshore wind farms, salt-fog environments, chemical plants, high-altitude stations, and industrial areas. Surface oxidation or other approved treatments can also improve compatibility between the conductor and an insulation layer, helping reduce adhesion problems during subsequent insulation processing.
4. Electrical Performance and Safety Characteristics
4.1 High Current-Carrying Capacity
The product is engineered for high-current transmission and distribution. Current capacity is determined by the conductor cross-section, alloy conductivity, allowable temperature rise, installation arrangement, heat dissipation, ambient conditions, and connection quality.
A tubular busbar can provide a large effective conducting area while maintaining a relatively low mass. In a high-current substation, this can reduce the need for multiple parallel flat conductors and may simplify phase arrangement, support design, and maintenance access.
When several conductors are used in parallel, phase spacing and electromagnetic interaction must be carefully analyzed. Correct spacing helps control magnetic forces, induced losses, and electric field conditions during both normal operation and short-circuit events.
4.2 Low Transmission Loss
Electrical losses are affected by conductor resistance, operating temperature, joint resistance, proximity effects, skin effects, and system configuration. The use of a high-conductivity alloy and a carefully designed tubular cross-section can help reduce resistive losses and maintain efficient power transmission.
Some product comparisons indicate power loss of no more than approximately 2% per 100 meters for a specified ultra-high voltage tubular arrangement, compared with higher values for certain conventional aluminum or copper configurations. Such figures are application-specific and should not be treated as universal performance ratings. Actual losses must be calculated from the complete system design and verified through testing.
4.3 Temperature Control
Temperature rise is a critical design parameter because excessive heat can reduce conductor life, accelerate insulation aging, increase joint resistance, and cause thermal expansion. The tubular profile, high external surface area, and suitable alloy composition promote heat dissipation.
Manufacturers can support thermal optimization by controlling wall thickness, surface finish, straightness, alloy condition, and connection geometry. For installations with unusual environmental conditions, thermal calculations may include solar loading, low wind speed, high ambient temperature, enclosed spaces, altitude correction, and forced cooling requirements.
4.4 Corona and Electric Field Control
At ultra-high voltage, corona discharge can produce audible noise, radio interference, ozone, energy loss, and long-term surface deterioration. Smooth tubular surfaces and appropriate conductor diameters help reduce electric field concentration.
A complete system may also include shielding components, corona rings, rounded connection fittings, smooth transition pieces, and carefully controlled clearances. Surface defects, burrs, sharp corners, contamination, and poorly finished joints can negatively affect corona performance. For this reason, precision machining and final visual inspection are essential parts of the manufacturing process.
4.5 Short-Circuit and Seismic Performance
During a short circuit, busbars can experience substantial electrodynamic forces. The conductor, supports, joints, and connected equipment must be able to withstand these forces without excessive displacement or permanent deformation.
The tubular structure offers strong resistance to bending and vibration. With appropriate support spacing and connection design, the system can also adapt to seismic conditions. Seismic performance must be evaluated as part of the project engineering package, including the dynamic characteristics of the complete busbar assembly rather than the conductor alone.
5. Comparison with Conventional Busbar Solutions
Choosing a busbar material requires consideration of more than the initial purchase price. Weight, current capacity, structural requirements, installation time, corrosion protection, temperature performance, maintenance, and expected service life all influence the total value of the system.
| Busbar Type | Approximate Weight | Typical Strength Profile | Thermal Performance | Potential Voltage Application |
|---|---|---|---|---|
| Magnesium-aluminum alloy tubular bus bar | Approximately 8–12 kg/m in a specified design range | High stiffness-to-weight ratio and good vibration resistance | High surface-area-to-mass ratio and heat-resistant alloy options | Applications up to ultra-high voltage levels, subject to system design |
| Traditional copper busbar | Approximately 25–30 kg/m in a specified comparable range | Excellent strength and conductivity but high mass | Good conductivity; thermal design may require larger structural support | Widely used in low-, medium-, and high-voltage equipment |
| Ordinary aluminum busbar | Approximately 7–10 kg/m in a specified range | Low density but potentially lower strength and heat resistance | Good conductivity and low weight; alloy and geometry are important | Commonly used in low- and high-voltage applications |
| Assembled flat busbar arrangement | Varies according to the number and thickness of conductors | May require more supports and careful alignment | Depends on spacing, surface area, and ventilation | Common in distribution boards and substation equipment |
5.1 Advantages over Copper Busbars
The most visible advantage over copper is weight reduction. Lower mass can reduce support loads and improve installation efficiency. For long-distance or elevated busbar systems, the structural savings may be significant.
Magnesium-aluminum alloy also offers strong corrosion resistance and can be selected for high-temperature service. Although copper has excellent conductivity, the total system may not always be optimized by using the most conductive material. A lighter alloy conductor can provide an effective balance of electrical capacity, mechanical performance, and project economics.
5.2 Advantages over Ordinary Aluminum Busbars
Compared with ordinary aluminum, a magnesium-aluminum or specially developed rare-earth aluminum alloy can offer improved strength, corrosion resistance, dimensional stability, and heat resistance. This is valuable in long-span, high-wind, high-vibration, high-temperature, or salt-fog installations.
The tubular structure also provides mechanical advantages over many flat or solid aluminum arrangements. It can increase stiffness, reduce deflection, improve surface heat dissipation, and support more consistent electric field behavior.
5.3 Advantages over Multi-Conductor Assemblies
Multiple parallel flat conductors may require numerous spacers, clamps, supports, and connection points. Each additional component introduces installation work and potential maintenance requirements. A tubular system can reduce assembly complexity while providing a defined external diameter and engineered connection interface.
However, the correct solution depends on the voltage level, current rating, available space, fault level, insulation arrangement, and project standards. A tubular busbar is not automatically superior for every application; its benefits are most apparent when the project requires high current, long spans, low weight, mechanical stability, and controlled electric field performance.
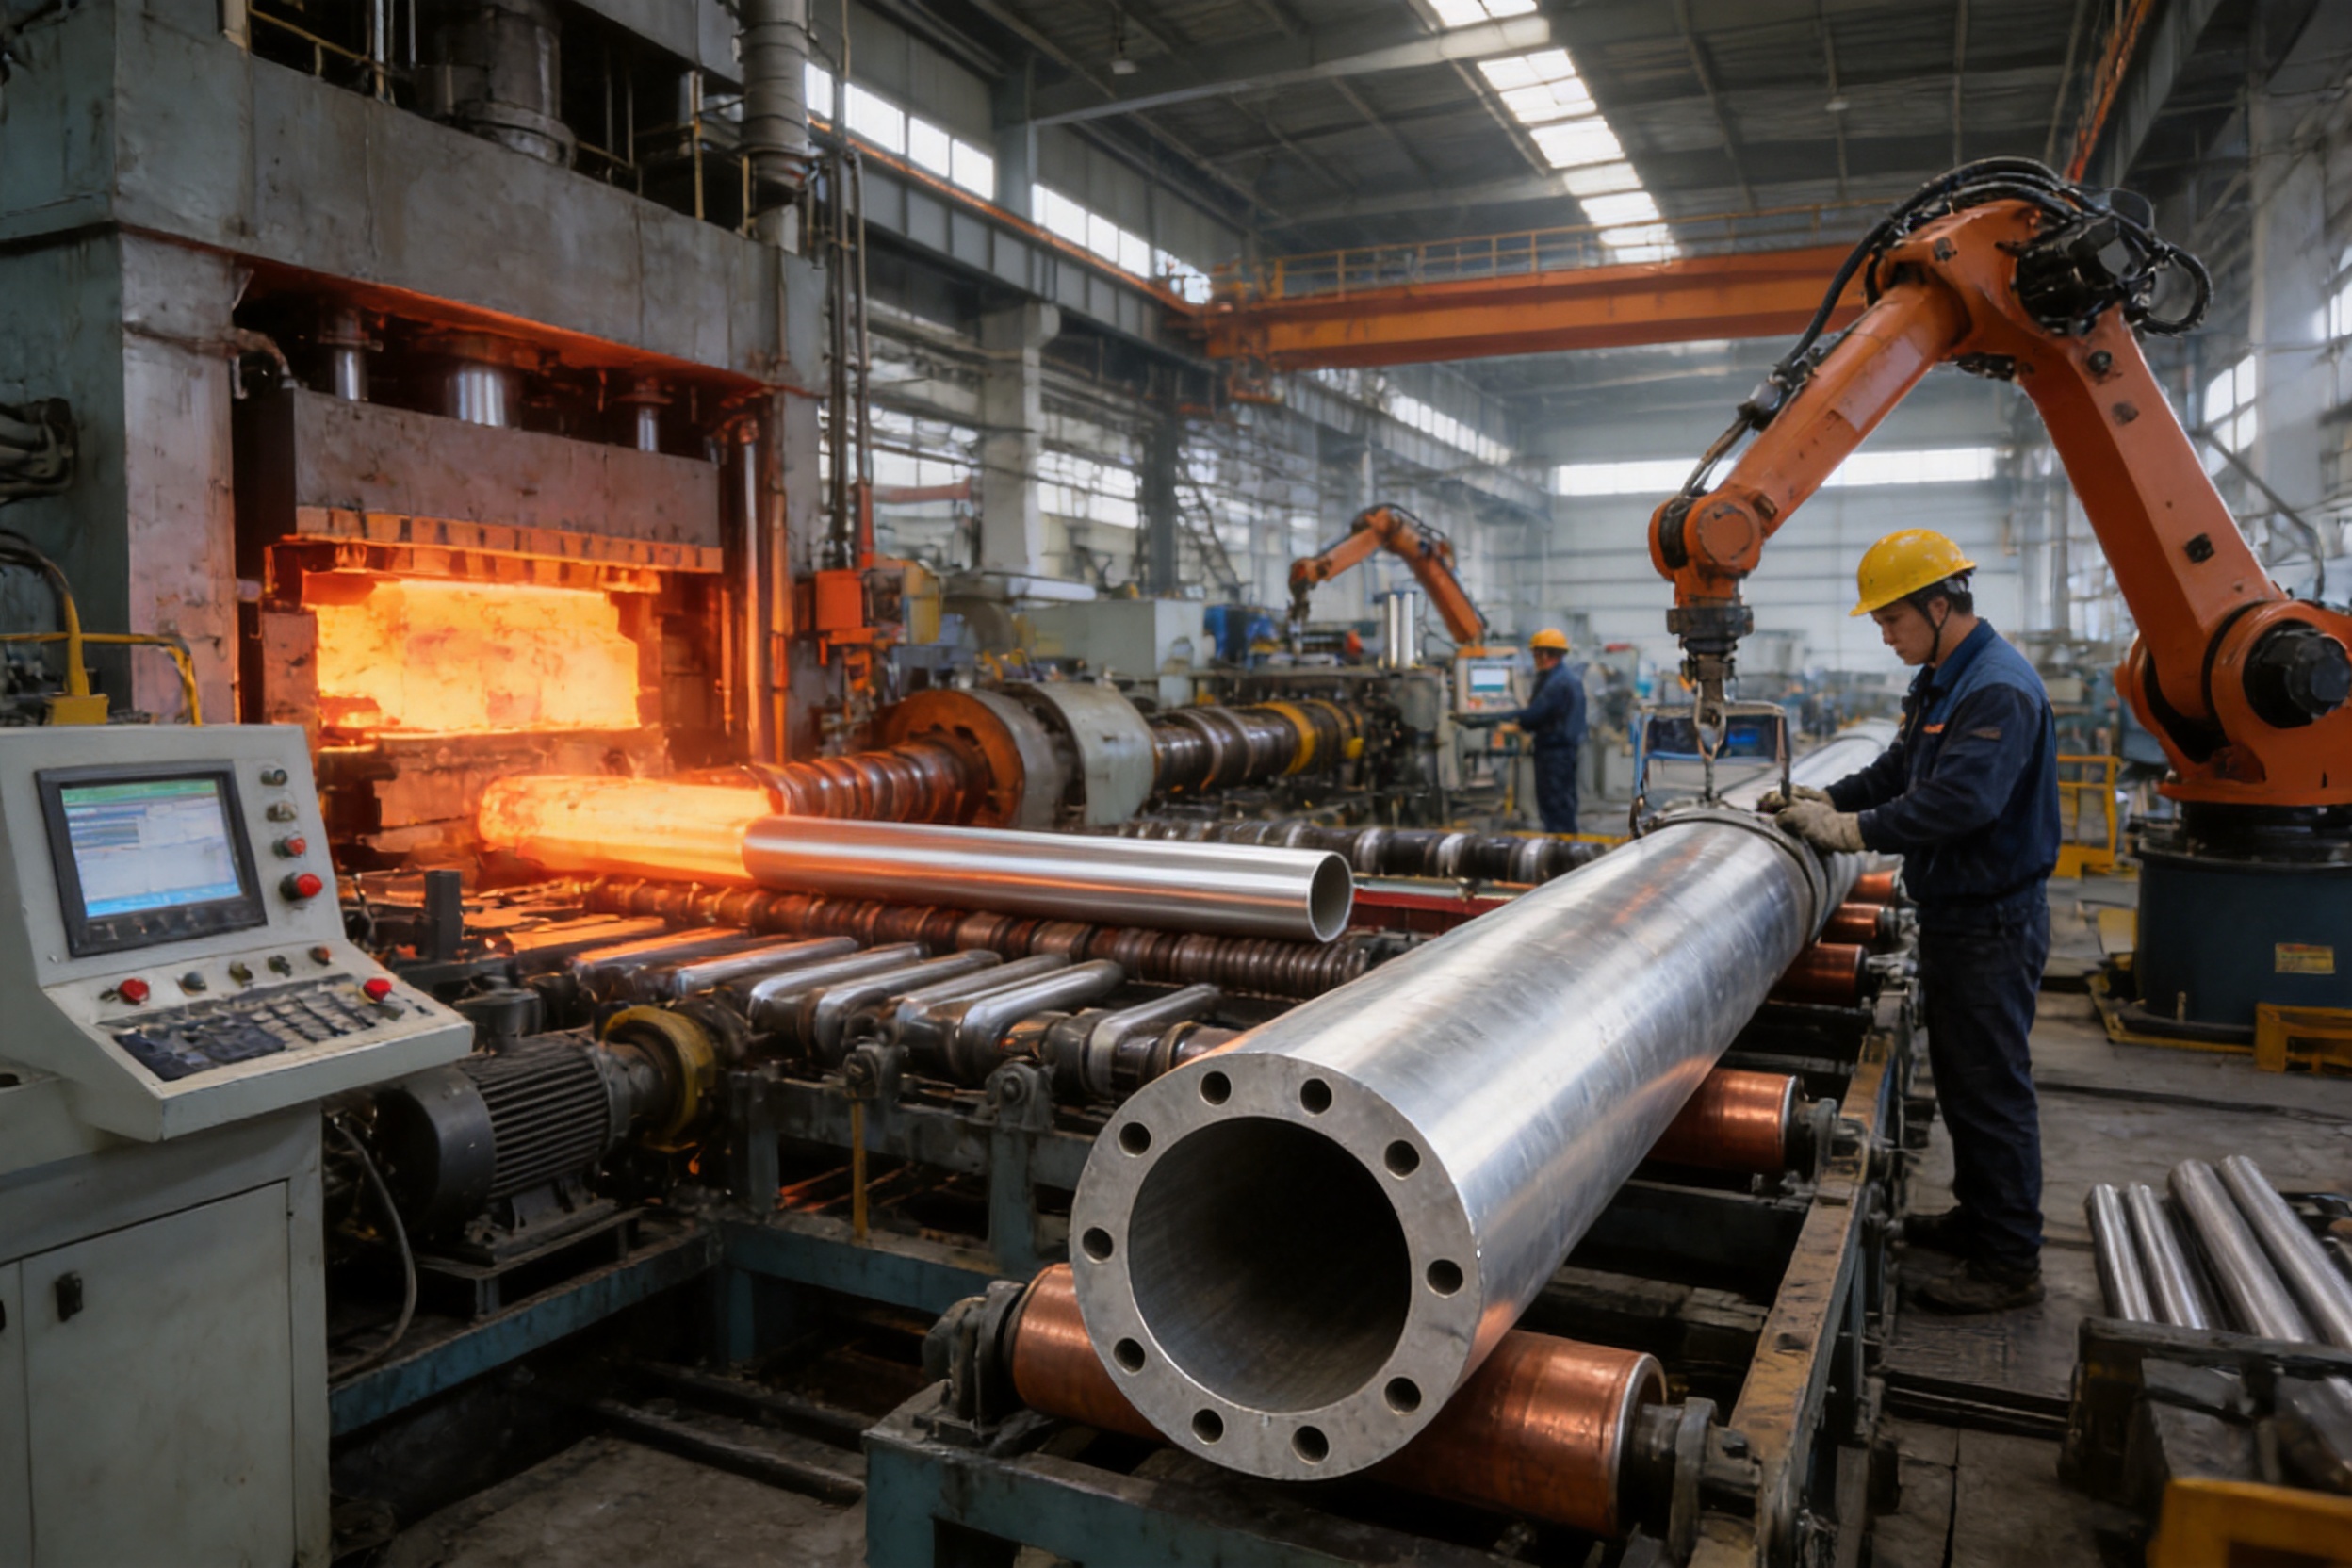
6. Advanced Manufacturing Process
The performance of a magnesium-aluminum alloy tubular bus bar depends heavily on the consistency of its manufacturing process. Alloy composition, casting quality, tube formation, heat treatment, cold working, machining, surface treatment, and inspection must be controlled as a connected production chain.
6.1 Alloy Formulation and Raw Material Control
Production begins with the selection and verification of aluminum, magnesium, manganese, rare-earth additions, heat-resistant elements, and other approved alloying materials. Chemical composition must remain within the required range to ensure repeatable conductivity, strength, corrosion resistance, and processing behavior.
Raw materials are inspected before melting. Material identification, storage conditions, batch records, and contamination control are important because unwanted inclusions or composition deviations can affect tube integrity and electrical performance.
6.2 Horizontal Hot Top Casting
Horizontal hot top casting technology is used to promote material purity and microstructural uniformity. Controlled metal flow and solidification can reduce segregation, improve billet consistency, and create a more stable starting material for subsequent tube production.
Temperature control is critical during casting. If the metal is too hot, grain growth and oxidation may increase. If it is too cold, filling and solidification defects may occur. Process monitoring helps maintain stable casting conditions from one production batch to another.
The resulting billet must be inspected for surface defects, internal discontinuities, dimensional accuracy, and chemical composition. A consistent billet supports reliable performance during hot rolling and cold drawing.
6.3 Transverse Piercing Hot Rolling
Transverse piercing hot rolling enables the manufacture of seamless tubular products. During this process, a solid billet is pierced and rolled to form a hollow tube. The absence of a welded seam eliminates a potential line of weakness and improves structural continuity around the circumference.
Seamless production is especially valuable for ultra-high voltage conductors because the tube must withstand mechanical loads, thermal cycling, vibration, and environmental exposure without relying on a longitudinal weld. The rolling schedule must be selected to achieve the required wall thickness, diameter, straightness, and grain structure.
Rolling temperature, reduction ratio, tool condition, lubrication, and deformation speed are controlled to limit internal stress and dimensional variation. Process stability is essential because uneven deformation can affect current distribution, mechanical balance, and the fit of connection components.
6.4 Thermomechanical Treatment
Thermomechanical treatment combines controlled heating, deformation, cooling, and sometimes aging or stabilization steps to improve the alloy microstructure. The objective is to obtain the required balance of strength, ductility, conductivity, heat resistance, and dimensional stability.
For high-voltage tubular busbars, thermomechanical treatment must also support reliable behavior during thermal expansion and contraction. A stable microstructure helps prevent excessive distortion during service and improves consistency between different sections of the same conductor.
6.5 Multipass Cold Drawing
After hot processing, multipass cold drawing is used to refine the tube dimensions and improve surface quality. The tube passes through a series of dies, with each pass applying a controlled reduction. This method can achieve accurate outside diameter, inside diameter, wall thickness, straightness, and surface finish.
Cold drawing also changes the mechanical properties of the material. The reduction schedule must therefore be balanced with intermediate heat treatment where necessary. Excessive deformation may reduce ductility, while insufficient reduction may fail to achieve the required dimensional accuracy.
Precision cold drawing is particularly important when the busbar must be integrated with insulation layers, shielding components, clamps, terminals, or prefabricated joints. Consistent dimensions help ensure predictable assembly and reduce the risk of localized stress or uneven contact pressure.
6.6 Precision Cutting and Machining
Finished tubes are cut to specified lengths and machined to create connection surfaces, holes, slots, end profiles, and other project-specific features. CNC machining can improve repeatability and reduce dimensional variation between components.
Edges and corners are finished to remove burrs and sharp projections. This is important for personnel safety, insulation integrity, corona control, and reliable connection to terminals and fittings. Machining debris and contaminants must be removed before the conductor enters the next stage of production.
6.7 Surface Treatment
Surface treatment can improve corrosion resistance, cleanliness, insulation adhesion, and long-term appearance. Oxidation treatment or another approved process may be selected according to the insulation system and environmental conditions.
Surface preparation must be compatible with epoxy vacuum casting, PTFE wrapping, or other insulation methods. The treatment should provide a clean and stable interface without introducing excessive roughness, contamination, or chemical incompatibility.
6.8 Insulation and Shielding Compatibility
Although the conductor may be supplied as a bare tubular busbar, it can also be integrated into an insulated or shielded busbar system. Compatibility with epoxy resin vacuum casting and PTFE wrapping allows the same basic conductor technology to be adapted to different insulation requirements.
During insulation processing, the conductor surface must be free from oil, moisture, dust, oxide particles, and machining residue. Vacuum casting parameters, resin viscosity, curing temperature, pressure, and cooling conditions are controlled to reduce voids and improve bonding.
7. Manufacturing Strengths of Jiangsu Wopeng Power Technology
Jiangsu Wopeng Power Technology Co., Ltd. was founded in 2018 as a specialized high-technology enterprise focused on the development and production of high- and low-voltage busbar systems. Its manufacturing and engineering capabilities cover a broad range of power transmission products rather than a single conductor type.
The company’s product portfolio includes 35 kV epoxy resin vacuum-cast tubular busbars, low-voltage cast-resin busway systems, copper and aluminum tubular busbars, wind power tubular busbars, compact busbar systems, and sliding contact line power supply systems.
7.1 Engineering and Technical Team
A team of engineers, technical specialists, and production professionals supports product development, process control, project customization, and application service. Experience across power generation, substations, wind energy, industrial manufacturing, rail transit, and commercial facilities enables the company to consider both conductor performance and system integration.
This engineering approach is important for ultra-high voltage projects because the conductor cannot be selected independently from the connected equipment. Busbar diameter, terminal design, support spacing, expansion joints, insulation, grounding, clearances, and installation sequence all influence the final solution.
7.2 Modern Production Equipment
The company operates production lines equipped with vacuum casting systems, CNC machining equipment, and automated assembly technologies. Vacuum casting supports the production of insulated busbar components with controlled resin penetration and reduced internal void risk. CNC equipment improves the accuracy of conductor and fitting dimensions, while automated assembly supports repeatable production.
Modern equipment also makes it easier to maintain production records, establish process traceability, and repeat approved designs for future projects. This is valuable for customers operating multiple substations, renewable energy sites, or industrial plants that require consistent equipment across locations.
7.3 Quality Management and Testing
Products undergo standardized inspection procedures that may include high-voltage tests, insulation tests, mechanical verification, dimensional inspection, appearance inspection, and routine quality checks. Cooperation with third-party testing institutions provides independent validation of safety and performance where required.
For a high-voltage tubular busbar, quality management should include incoming material inspection, alloy composition verification, casting inspection, dimensional measurement, straightness measurement, surface examination, mechanical testing, conductivity testing, temperature-rise evaluation, and electrical withstand testing according to the project specification.
7.4 Application Experience
Wopeng products operate in more than 17 provinces and across multiple industrial sectors. This operating experience provides practical feedback regarding transportation, installation, temperature variation, outdoor exposure, maintenance, and customer-specific integration.
Application experience is particularly useful when designing busbars for wind power, photovoltaic generation, rail transit, industrial plants, and large commercial facilities. These projects often have different requirements for vibration, compactness, corrosion protection, maintenance access, and installation speed.
8. Main Application Scenarios
8.1 Ultra-High Voltage Substations
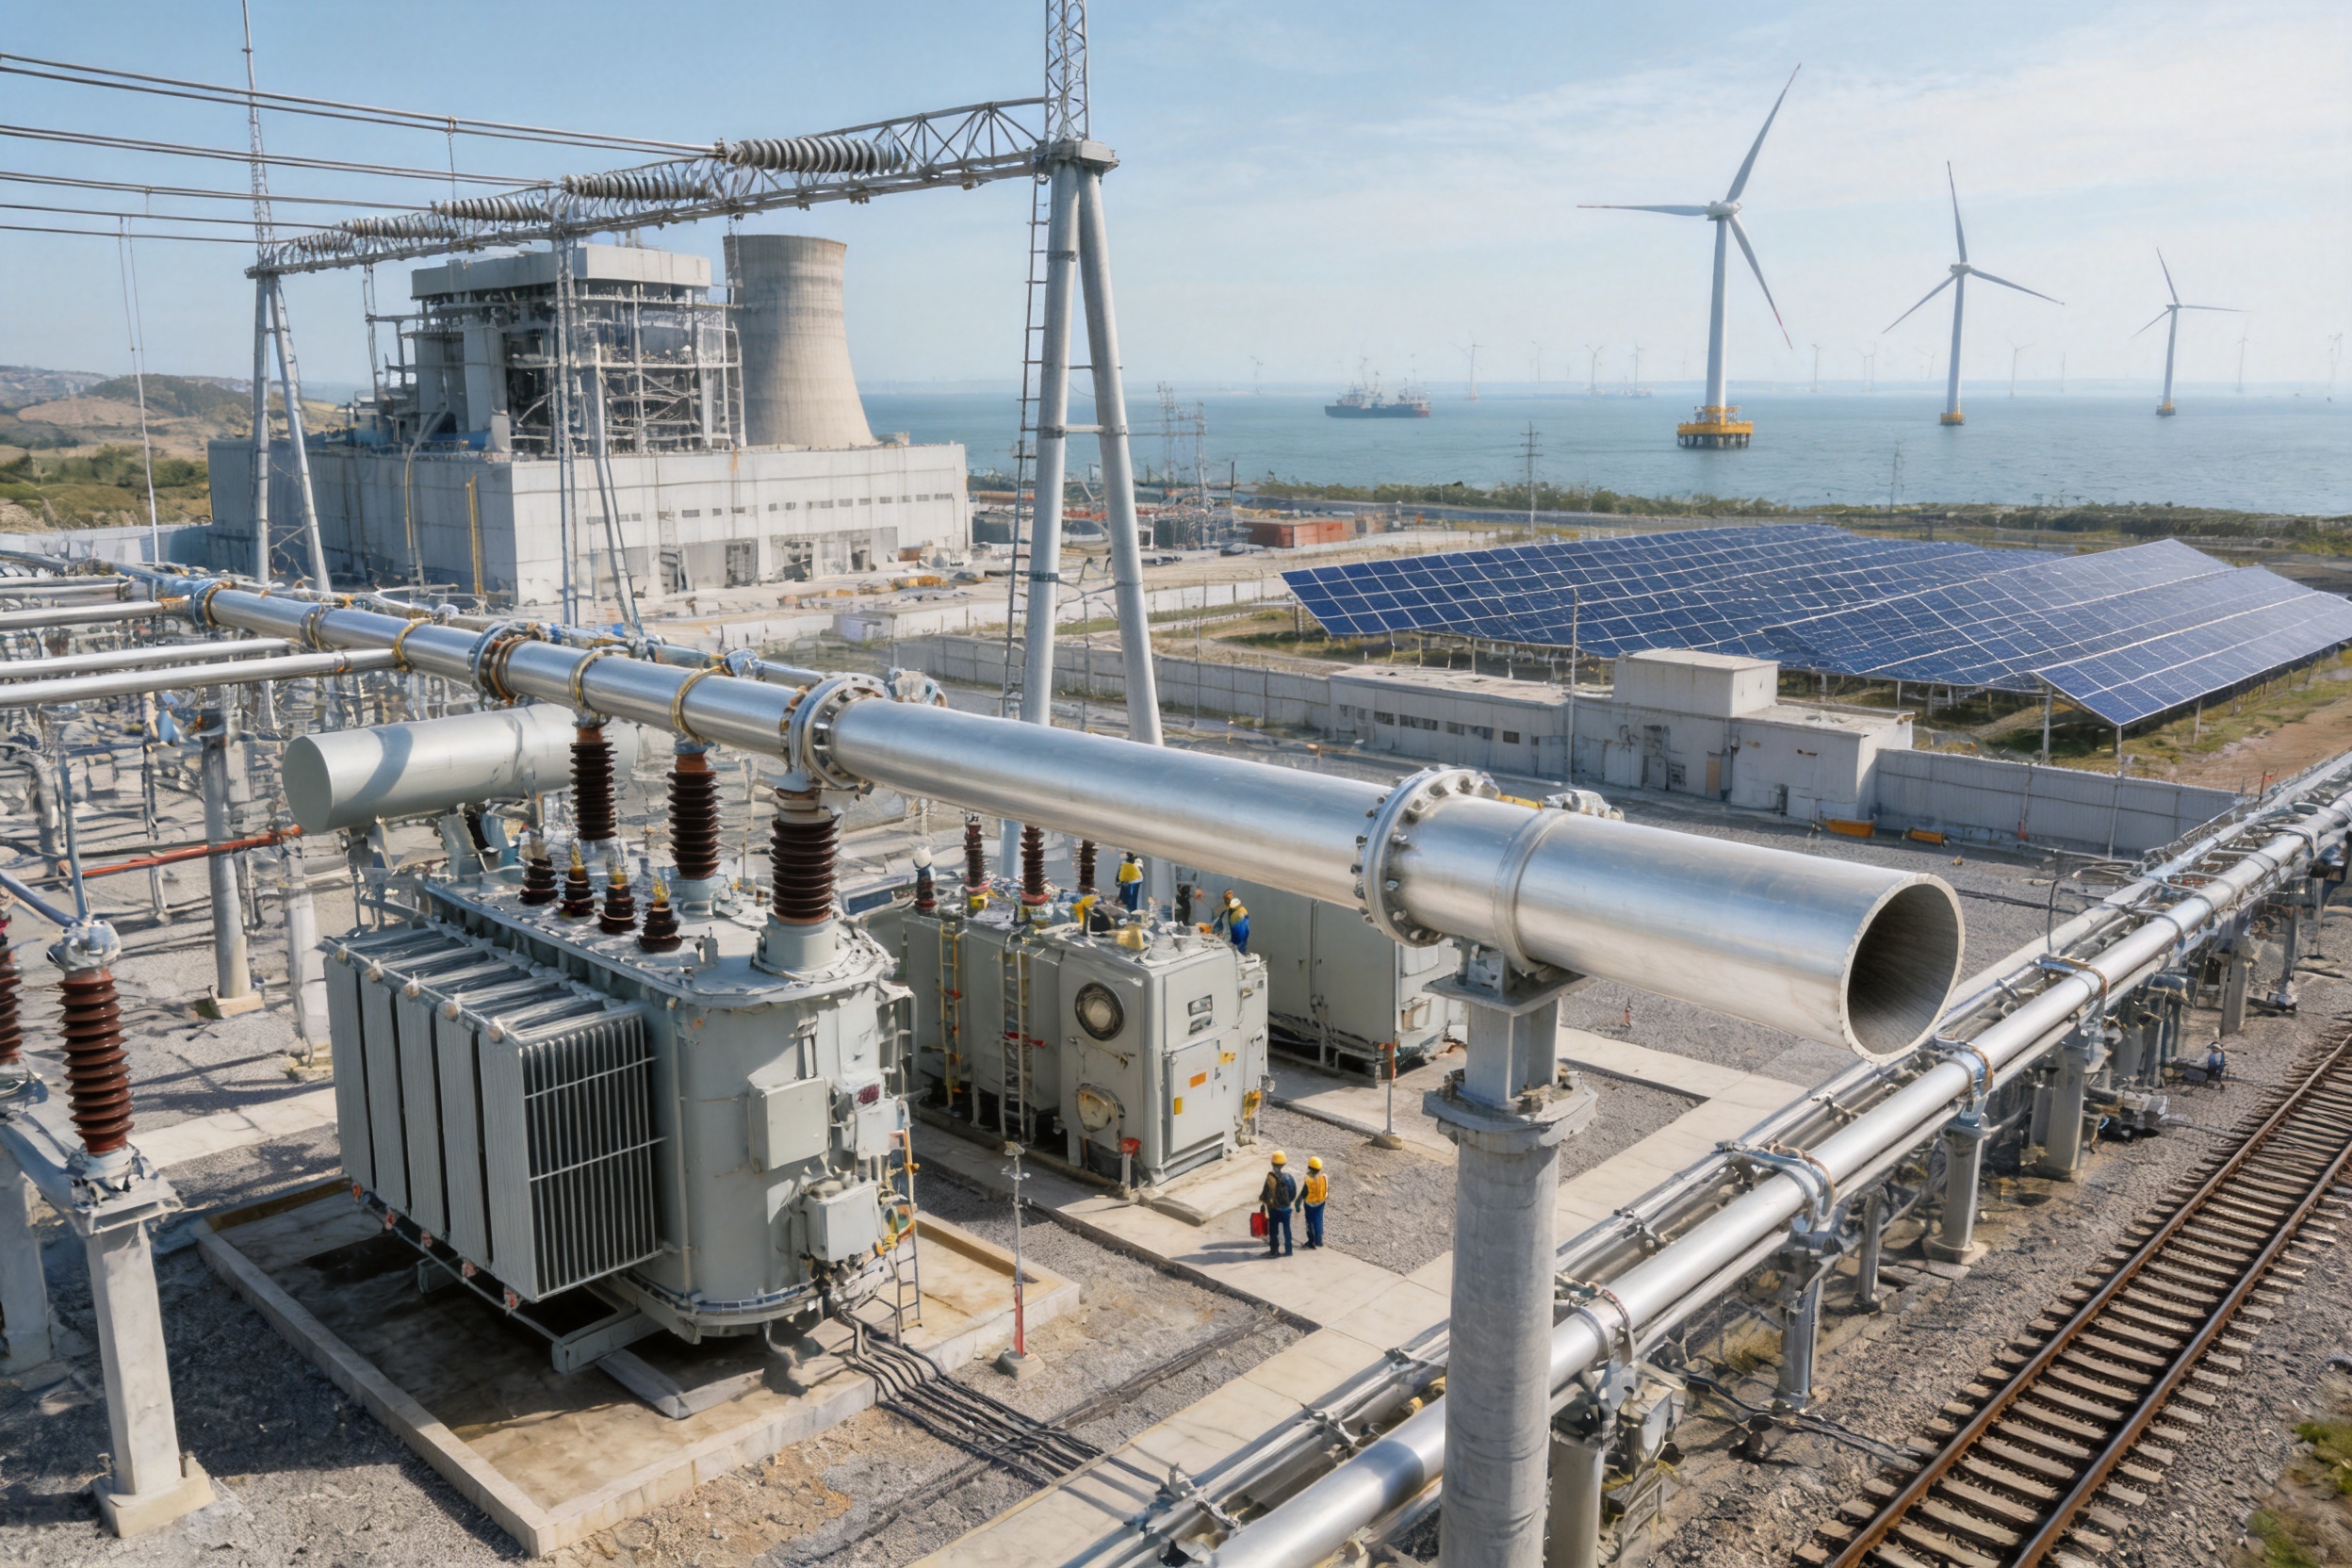
In 500 kV and higher substations, tubular busbars can connect transformers, circuit breakers, disconnectors, voltage transformers, current transformers, and transmission line terminals. The conductor must maintain stable clearances and withstand electrical, thermal, and mechanical stresses.
Low weight is beneficial for elevated bus structures, while tubular stiffness supports longer spans and reduced deflection. Smooth surfaces and suitable shielding arrangements help manage electric field conditions. Corrosion-resistant treatment is valuable for outdoor installations exposed to rain, condensation, industrial pollution, or salt spray.
8.2 Hydroelectric and Thermal Power Plants
Power plants require reliable connections between generators, step-up transformers, switchgear, and grid interfaces. These connections may carry high current continuously and may be subject to vibration, temperature variation, and limited maintenance access.
A magnesium-aluminum alloy tubular busbar can be designed for high current output while reducing the mechanical load on supports. The system can be customized for plant layout, equipment terminal orientation, phase spacing, and required insulation level.
8.3 Wind Power Projects
Wind power systems experience continuous vibration, cyclic loading, temperature changes, and exposure to humidity. Tubular busbars used in wind turbines or wind farm substations must be lightweight, mechanically stable, and compatible with compact installation spaces.
The product’s bending resistance and vibration resistance are suitable for demanding wind power applications when supported by appropriate structural design. Offshore wind farms may also benefit from corrosion-resistant alloy selection and surface treatment designed for marine environments.
8.4 Photovoltaic and Renewable Energy Facilities
Large photovoltaic facilities and renewable energy bases often require high-current collection and grid connection systems. Tubular busbars can provide a compact and efficient connection between transformers, converters, collection equipment, and high-voltage switchgear.
Outdoor renewable energy sites may be located in deserts, coastal zones, high-altitude areas, or regions with large daily temperature changes. Material selection and surface protection should therefore reflect local dust, humidity, ultraviolet, salt-fog, wind, and temperature conditions.
8.5 Industrial Power Distribution
Metallurgical plants, chemical facilities, mining operations, rolling mills, and other high-load industries require dependable power distribution under demanding operating conditions. High current, frequent load variation, vibration, dust, corrosive gases, and restricted installation areas may all affect busbar selection.
The tubular busbar can provide high current capacity, good thermal performance, mechanical stability, and flexible insulation compatibility. Project-specific surface treatment and enclosure design may be used when the atmosphere contains corrosive chemicals or conductive dust.
8.6 Rail Transit
Rail transit systems require compact, reliable, and mechanically secure power supply equipment. Busbars may be exposed to vibration, electromagnetic forces, limited equipment space, and strict maintenance requirements.
The high specific strength and tubular geometry of the magnesium-aluminum alloy conductor support lightweight system design. Depending on the application, the conductor may be combined with insulation, protective shielding, compact supports, and customized connection fittings.
8.7 Coastal, Offshore, and High-Altitude Stations
Marine and high-altitude environments present distinct challenges. Coastal and offshore locations may expose equipment to salt fog and persistent humidity, while high-altitude locations may experience lower air density, high ultraviolet exposure, strong wind, and large temperature differences.
The busbar system must be designed according to the actual environmental correction factors. Alloy selection, surface oxidation, insulation coordination, creepage distance, corona control, and enclosure arrangements should be reviewed during the engineering stage.
9. Customization Options
Ultra-high voltage busbar systems are rarely identical from one project to another. Customization may be required to match electrical ratings, equipment terminals, site geometry, transport limitations, insulation requirements, and local standards.
9.1 Conductor Dimensions
Outside diameter, inside diameter, wall thickness, section length, and allowable tolerance can be customized according to current capacity, mechanical loading, thermal performance, and connection requirements. Larger diameters may improve current distribution and electric field control, while wall thickness is selected according to mechanical and manufacturing requirements.
9.2 Alloy Grade
Customers may select 6063G, LF21Y, 6R05, 2A14, or another approved alloy according to project conditions. The choice should consider conductivity, tensile strength, elongation, heat resistance, corrosion resistance, weldability or machinability, and compatibility with the proposed insulation process.
9.3 Length and Connection Design
Individual sections can be manufactured to meet transportation and installation requirements. Connection ends may include drilled holes, machined interfaces, flanges, transition pieces, expansion joints, or customized terminal structures.
Connection design is a critical factor in system reliability. Contact surfaces must provide low resistance, stable pressure, adequate mechanical strength, and suitable protection against oxidation or contamination. Joints should also allow for thermal expansion without creating excessive stress in connected equipment.
9.4 Insulation Systems
Depending on voltage and installation conditions, the tubular conductor may be supplied as part of an epoxy resin vacuum-cast assembly, PTFE-wrapped system, air-insulated arrangement, or another specified configuration. Insulation design must address dielectric strength, partial discharge, thermal expansion, moisture resistance, tracking resistance, and long-term aging.
9.5 Surface Treatment and Environmental Protection
Surface oxidation and other protective treatments may be specified for general outdoor use, coastal environments, salt-fog conditions, chemical facilities, or high-altitude applications. Protective measures should be selected together with the insulation and connection systems to avoid incompatibility.
10. Installation and System Integration
10.1 Transport and Handling
Tubular busbars should be transported using supports that prevent local crushing, bending, or surface damage. Long sections require suitable lifting points and controlled handling procedures. Protective packaging should prevent contamination, moisture accumulation, and impact damage during shipment.
Before installation, each section should be checked for straightness, surface condition, dimensional accuracy, identification marks, and any signs of deformation. Damaged components should not be installed without technical evaluation.
10.2 Support and Alignment
Supports must be arranged according to the approved structural calculations. Excessive support spacing can increase deflection and mechanical stress, while unnecessary supports can increase cost and complicate thermal expansion.
Alignment is important for maintaining electrical clearances and preventing stress at joints. Supports should be installed with sufficient dimensional accuracy to avoid forcing the conductor into position. Forced alignment can produce residual stress and may transfer excessive loads to terminals or insulation components.
10.3 Thermal Expansion
Aluminum alloy conductors expand and contract as temperature changes. Long busbar runs require expansion allowances, flexible connections, or expansion joints. The design should account for the conductor’s coefficient of thermal expansion, operating temperature range, support constraints, and connected equipment movement.
Expansion components must be installed in the correct orientation and checked for free movement. Improper installation can cause mechanical stress, joint loosening, misalignment, or damage to insulators.
10.4 Electrical Connections
Connection surfaces must be clean and prepared according to the manufacturer’s instructions. Contact pressure, fastener torque, joint compound, surface treatment, and anti-loosening measures should be controlled. The finished joint should have low resistance and sufficient mechanical strength.
After installation, electrical resistance, insulation condition, clearances, grounding, and high-voltage withstand performance should be checked according to the project acceptance plan.
10.5 Inspection and Maintenance
Routine maintenance may include visual inspection, thermographic inspection, joint-condition checks, insulation testing, surface-condition evaluation, and verification of support hardware. In coastal or polluted environments, cleaning and corrosion monitoring may be required more frequently.
Thermal imaging can help identify abnormal joint heating before it develops into a serious fault. Any unusual discoloration, noise, corona activity, insulation cracking, loose hardware, or surface corrosion should be investigated promptly.
11. Service Life and Reliability
With suitable alloy selection, surface protection, insulation design, installation quality, and routine maintenance, the service life of the tubular busbar can reach approximately 30–40 years under normal UHV operating conditions. Actual service life depends on voltage stress, current loading, environmental exposure, fault events, mechanical vibration, maintenance quality, and the performance of connected components.
Long-term reliability begins with material quality. Consistent alloy chemistry and microstructure reduce variations in conductivity and mechanical performance. Seamless tube production removes the potential weakness associated with a longitudinal weld. Thermomechanical treatment and multipass cold drawing improve dimensional control and structural consistency.
Reliability also depends on the complete system. A high-quality conductor may still experience premature failure if joints are poorly installed, supports are misaligned, insulation is contaminated, clearances are inadequate, or thermal expansion is restricted. For this reason, product selection, engineering review, manufacturing inspection, installation supervision, and commissioning should be treated as one integrated process.
12. Quality Evaluation and Selection Criteria
When selecting a supplier, customers should evaluate technical capability, manufacturing equipment, project experience, inspection procedures, customization capacity, and after-sales support. Price alone does not adequately represent the value or risk of an ultra-high voltage busbar system.
12.1 Type Test and Routine Test Documentation
A reliable manufacturer should be able to provide applicable type test reports, routine inspection records, material certificates, dimensional records, mechanical test results, conductivity data, insulation test results, and quality documentation required by the project.
12.2 Alloy Consistency
The supplier should maintain traceability from raw material receipt through casting, tube production, heat treatment, machining, and final assembly. Chemical composition and mechanical properties should be consistent between batches.
12.3 Process Capability
Customers should confirm whether the manufacturer has the equipment and experience required for seamless tube production, precision cold drawing, CNC machining, surface treatment, insulation processing, and high-voltage testing. The ability to produce one prototype is not the same as the ability to maintain stable quality during serial production.
12.4 Application Experience
Experience in substations, power generation, wind energy, industrial facilities, rail transit, and other relevant sectors can help reduce project risk. An experienced supplier is more likely to identify practical issues involving transportation, support spacing, thermal expansion, terminal compatibility, and field installation.
12.5 Technical Service
Technical service should cover specification confirmation, drawing review, interface coordination, installation guidance, commissioning support, troubleshooting, and maintenance recommendations. For customized systems, communication between the manufacturer, design institute, contractor, and end user is essential.
13. Frequently Asked Questions
Q1. What is the main advantage of a magnesium-aluminum alloy tubular busbar?
The main advantage is the combination of low weight, high specific strength, good electrical conductivity, efficient heat dissipation, corrosion resistance, and tubular structural rigidity. This combination can reduce support loads and simplify installation while meeting the requirements of high-current power systems.
Q2. Can this busbar be used at 500 kV and higher?
Yes. The product is designed for high-voltage and ultra-high voltage applications, including 500 kV, 750 kV, ±800 kV, and 1,000 kV scenarios. The final suitability depends on conductor dimensions, insulation coordination, shielding, current rating, clearances, environmental conditions, and the applicable type-test requirements.
Q3. Is it lighter than a copper busbar?
In comparable designs, it can be substantially lighter. A specified magnesium-aluminum alloy tubular busbar arrangement may weigh approximately 8–12 kg per meter, while a comparable traditional copper busbar may weigh approximately 25–30 kg per meter. Actual weight depends on diameter, wall thickness, alloy grade, fittings, insulation, and support components.
Q4. How does it compare with ordinary aluminum busbars?
It can provide improved mechanical strength, heat resistance, corrosion resistance, and dimensional stability through optimized alloy composition and controlled processing. Its tubular geometry also provides higher stiffness and favorable heat-dissipation characteristics. The best choice still depends on the project’s electrical and structural requirements.
Q5. What operating temperature can it withstand?
Selected heat-resistant designs can operate at approximately 150°C to 200°C. The allowable continuous and short-term temperatures must be confirmed for the specific alloy, conductor size, insulation system, joints, supports, and project standard.
Q6. Can it be installed outdoors?
Yes. The busbar can be used in outdoor substations, power plants, wind farms, photovoltaic facilities, coastal projects, and high-altitude stations. Appropriate surface treatment, insulation coordination, drainage, sealing, corrosion protection, and environmental design are required.
Q7. Can it be used in offshore wind power projects?
It can be considered for offshore and coastal applications where low weight and corrosion resistance are important. Marine exposure requires a project-specific review of salt-fog protection, surface treatment, fasteners, insulation, enclosure design, and inspection intervals.
Q8. What insulation processes are compatible with the conductor?
The conductor is compatible with insulation processes such as epoxy resin vacuum casting and PTFE wrapping when the surface preparation and process parameters are correctly controlled. Other insulation systems may also be considered according to voltage, temperature, mechanical, and environmental requirements.
Q9. Is the tubular busbar seamless?
The production route includes transverse piercing hot rolling, which enables seamless tube production. A seamless structure eliminates the weakness associated with a longitudinal weld and supports reliable mechanical performance around the full circumference.
Q10. What is the maximum support span?
Under suitable design conditions, the maximum support span may reach approximately eight meters. The actual span must be confirmed through calculations that include wind pressure, ice, seismic forces, conductor dimensions, thermal expansion, short-circuit forces, and permissible deflection.
Q11. How long can the product last?
With appropriate anti-corrosion treatment, correct installation, suitable operating conditions, and regular maintenance, the expected service life can reach approximately 30–40 years. The actual service life depends on the complete system and site environment.
Q12. What information should be provided when requesting a quotation?
Customers should provide voltage level, rated current, short-circuit current, conductor length, outside diameter or available space, support span, installation environment, altitude, temperature range, wind and ice conditions, insulation requirements, connection details, applicable standards, and delivery schedule.
Q13. Does the manufacturer provide customized OEM solutions?
Yes. Jiangsu Wopeng Power Technology provides customized busbar and tubular busbar system solutions. Customization may include alloy selection, dimensions, section length, terminal interfaces, insulation, surface treatment, supports, connection fittings, and assembly configuration.
Q14. What quality tests are important for an ultra-high voltage busbar?
Important tests may include chemical composition analysis, dimensional inspection, straightness measurement, conductivity testing, tensile and mechanical testing, surface inspection, insulation resistance testing, partial discharge evaluation, high-voltage withstand testing, temperature-rise testing, and routine assembly inspection. The precise test plan should follow the project specification and applicable standards.
14. Why Choose an Integrated Tubular Busbar Manufacturer?
An integrated manufacturer can coordinate alloy selection, tube production, machining, insulation, assembly, and testing within one quality-management system. This reduces interface risks between separate suppliers and makes it easier to maintain dimensional, electrical, and mechanical consistency.
For customized power equipment, integrated production also improves communication. Engineering changes can be reviewed directly with the production and testing teams. This supports faster design confirmation, better control of interfaces, and more efficient resolution of technical issues.
Jiangsu Wopeng Power Technology combines manufacturing facilities, engineering personnel, automated assembly, CNC processing, vacuum casting, and standardized inspection. Its experience in low-voltage, medium-voltage, high-voltage, wind power, rail transit, industrial, and commercial busbar products provides a broad technical foundation for project-specific solutions.
The company’s product range covers systems from low voltage to 35 kV, as well as specialized tubular busbar products for high-current and demanding operating conditions. Its manufacturing experience can support customers that need both individual conductors and complete busbar system integration.
15. Conclusion
The ultra-high voltage magnesium-aluminum alloy tubular bus bar is a high-performance solution for modern power transmission and transformation systems. Its main value lies in the combination of an optimized aluminum-based alloy with a strong, lightweight, seamless tubular structure.
Compared with traditional copper busbars, it can significantly reduce conductor weight and structural loading. Compared with ordinary aluminum busbars, it can provide improved strength, heat resistance, corrosion resistance, and mechanical stability. Its tubular geometry supports efficient heat dissipation, stable current transmission, controlled electric field distribution, and longer support spans.
The manufacturing process is central to product performance. Horizontal hot top casting improves billet quality, transverse piercing hot rolling produces a seamless tube, thermomechanical treatment refines the material structure, multipass cold drawing improves dimensional accuracy, CNC machining ensures precise connections, and surface treatment supports corrosion resistance and insulation compatibility.
For applications such as ultra-high voltage substations, power plants, wind farms, photovoltaic facilities, industrial distribution systems, rail transit, offshore projects, and high-altitude power stations, the busbar can be customized according to voltage, current, environmental, mechanical, insulation, and installation requirements.
Jiangsu Wopeng Power Technology Co., Ltd. supports these requirements through its engineering team, modern production equipment, quality inspection procedures, third-party testing cooperation, and experience across multiple power sectors. By combining material technology with complete busbar system engineering, the company provides a practical route toward lighter, safer, more efficient, and more reliable high-current power transmission infrastructure.
References
1. Aluminum Association. Aluminum Standards and Data: Material Properties and Design Considerations.
2. International Electrotechnical Commission. High-Voltage Power Systems: Insulation Coordination and Electrical Testing Principles.
3. International Electrotechnical Commission. Busbar Systems and Power Equipment Routine Testing Practices.
4. IEEE Standards Association. Guide for the Design and Application of Substation Bus Systems.
5. ASM International. Aluminum Alloy Phase Relations, Heat Treatment, and Mechanical Properties.
6. CIGRE Technical Publications. Design Considerations for High-Voltage and Ultra-High Voltage Substations.
7. CIGRE Technical Publications. Outdoor Electrical Equipment, Corona Control, and Environmental Performance.
8. Manufacturer technical documentation for magnesium-aluminum alloy tubular busbars, insulated busbar systems, and related power transmission equipment.
Product: Ultra-high Voltage Magnesium-Aluminum Alloy Tubular Bus Bar


-
 +86-180 3625 3000
-
 admin@wpbusbar.com
-
 No. 8, Yanjin Road, Chengxi Industrial Park, Shanyang Town, Baoying County, Yangzhou City, Jiangsu Province, China
Copyright © Jiangsu Wopeng Power Technology Co., Ltd.
All Rights Reserved.
 Custom Insulated Bus Bar Manufacturer
Tubular Busbar System Factory