

 EN

 English
 русский
 Français
 Español
 عربى
Epoxy Resin Casting Tubular Bus Bar: Design, Manufacturing, Performance, and Applications
Content
- 1 1. Product Overview
- 2 2. Integrated Structure and Operating Principle
- 3 3. Advanced Vacuum Casting Manufacturing Process
- 4 4. Main Technical Advantages
- 5 5. Comparison with Conventional and Alternative Busbar Systems
- 6 6. Voltage Range and Design Parameters
- 7 7. Environmental and Mechanical Performance
- 8 8. Typical Applications
- 9 9. Manufacturing Strengths and Quality Management
- 10 10. Installation and Commissioning Considerations
- 11 11. Maintenance and Service Life
- 12 12. Selection Guide for Project Owners and Engineers
- 13 13. Frequently Asked Questions
- 13.1 Q1: What is an epoxy resin casting tubular bus bar?
- 13.2 Q2: What voltage levels can the product support?
- 13.3 Q3: What is the designed service life?
- 13.4 Q4: Is it suitable for outdoor installation?
- 13.5 Q5: How does the product resist moisture?
- 13.6 Q6: What conductor material is used?
- 13.7 Q7: How are the busbar sections connected?
- 13.8 Q8: What is the maximum suspended span?
- 13.9 Q9: What tests should be requested from a supplier?
- 13.10 Q10: Why choose a cast tubular busbar instead of a conventional bare busbar?
- 13.11 Q11: Can the product be customized?
- 13.12 Q12: What makes the manufacturing process advanced?
- 14 14. Conclusion
- 15 References
- 16 Product: Epoxy Resin Casting Tubular Bus Bar
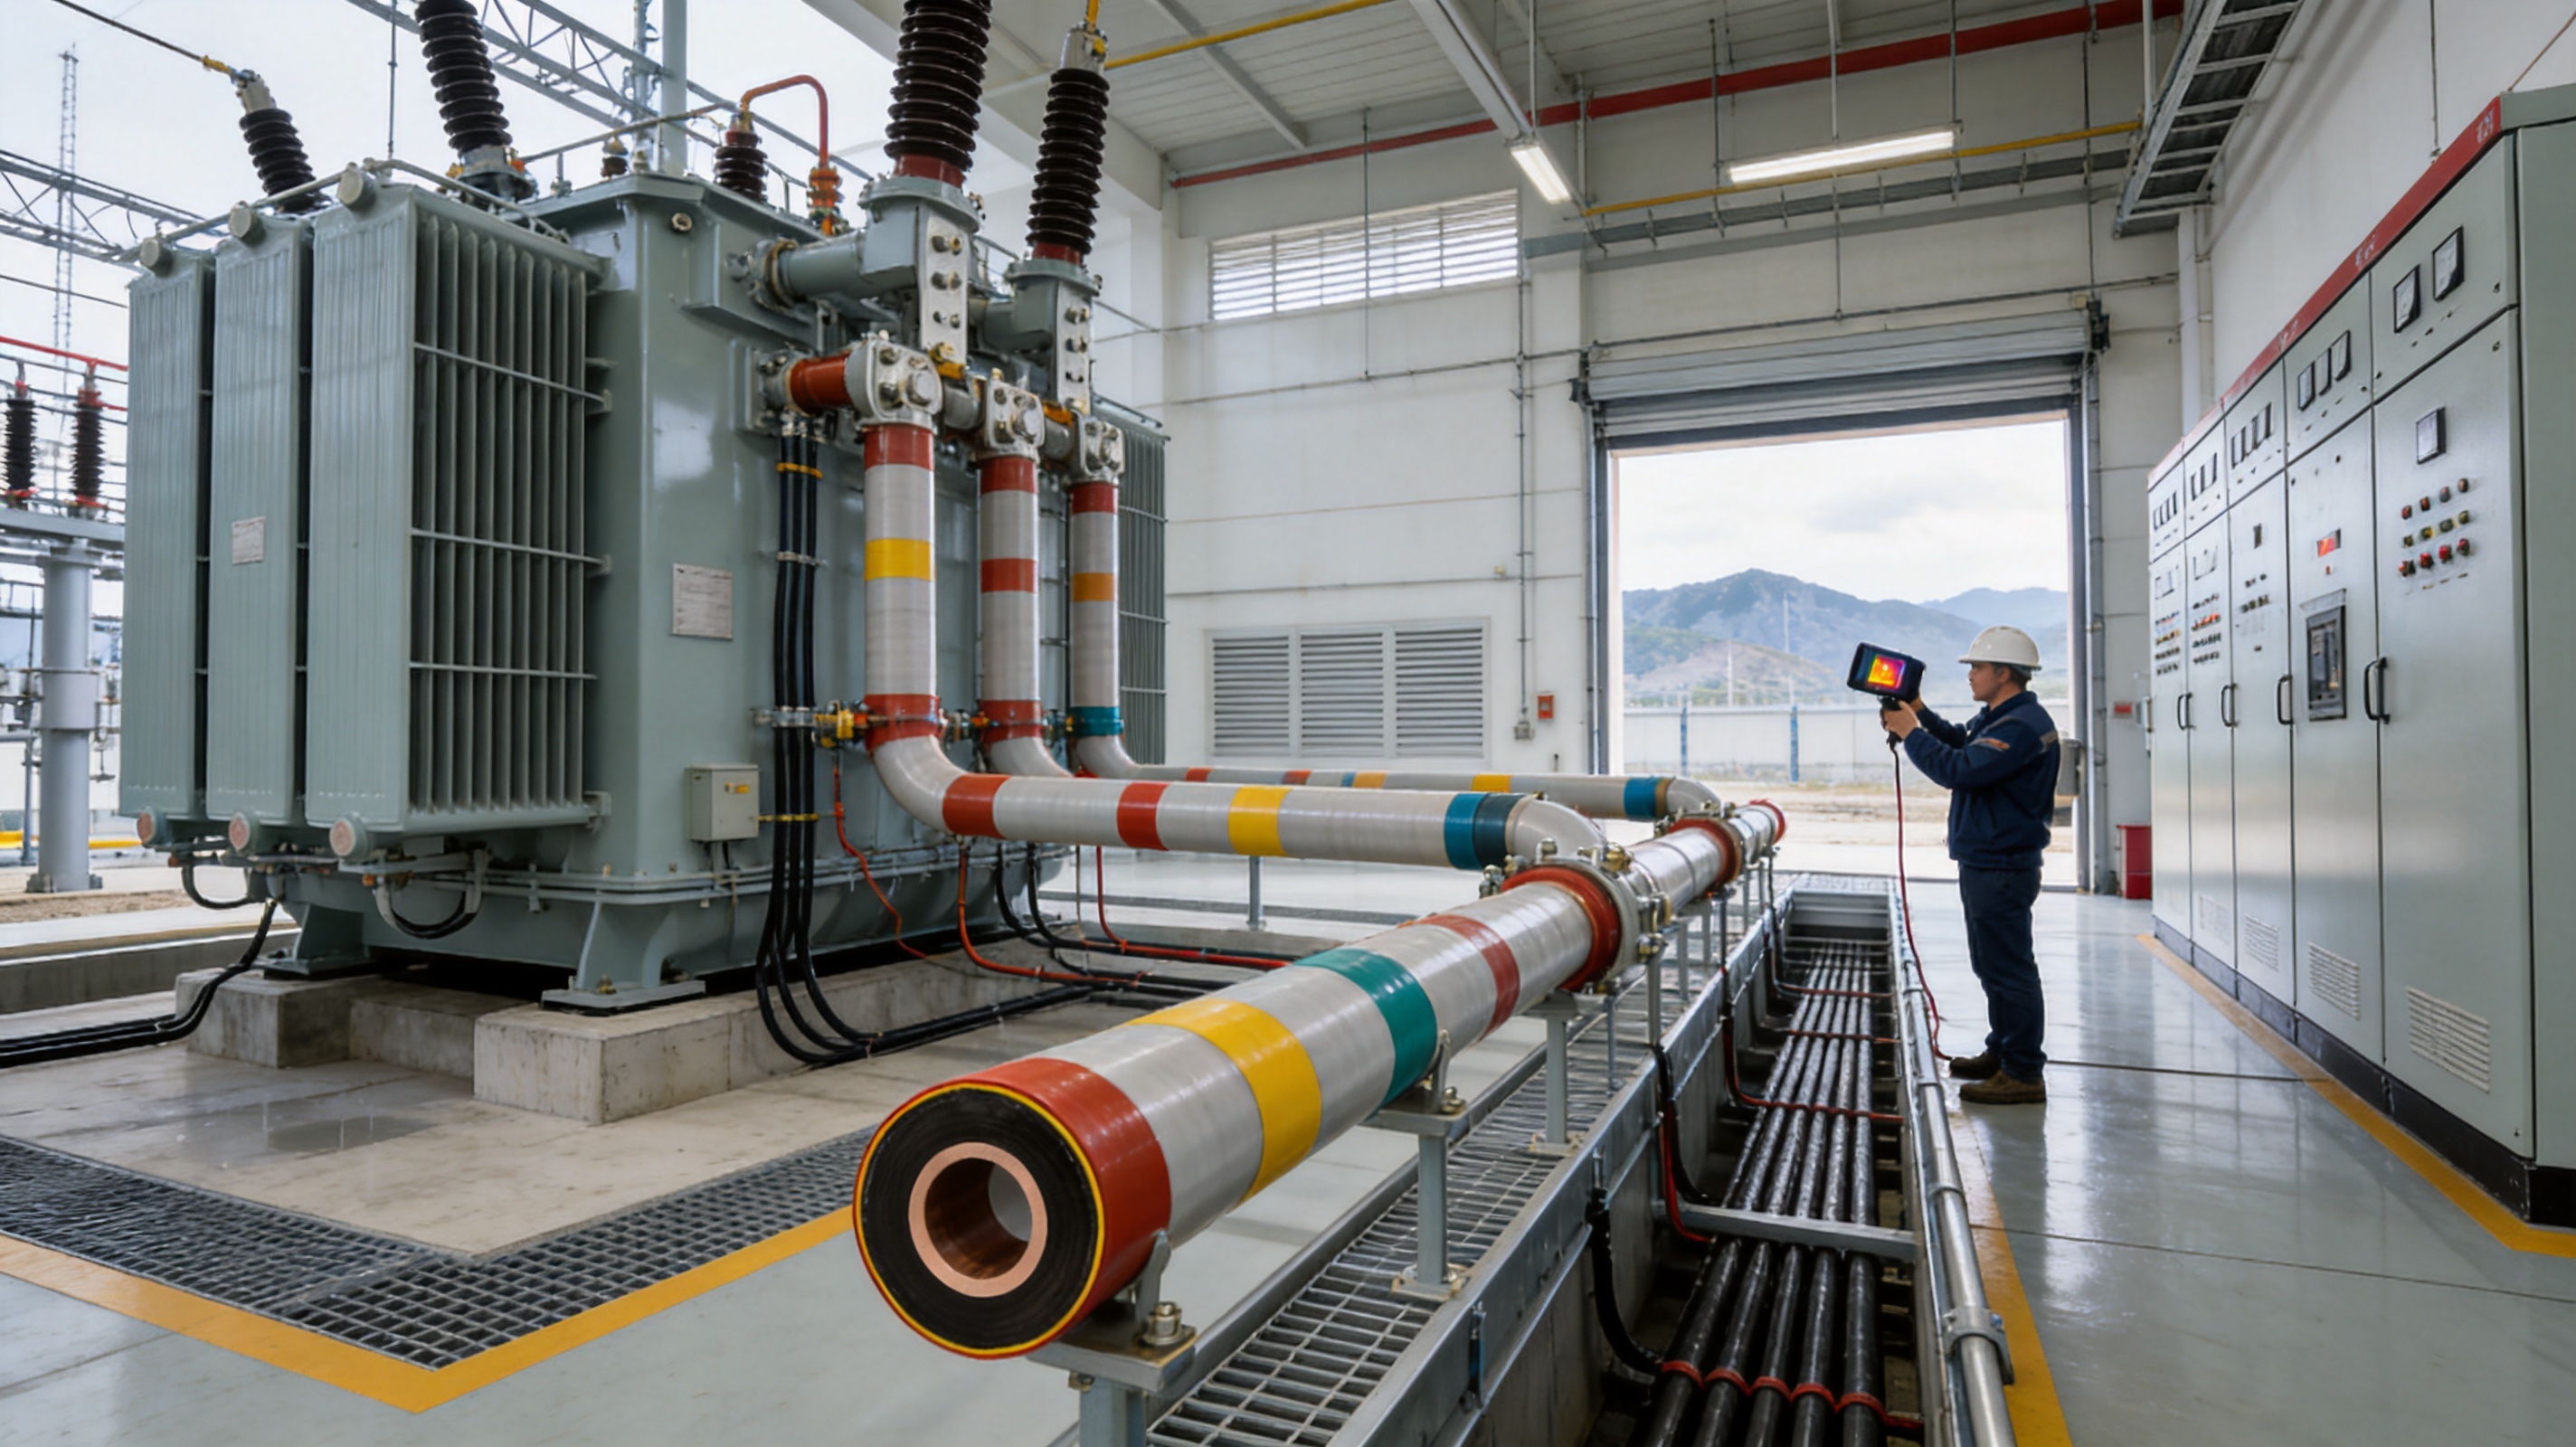
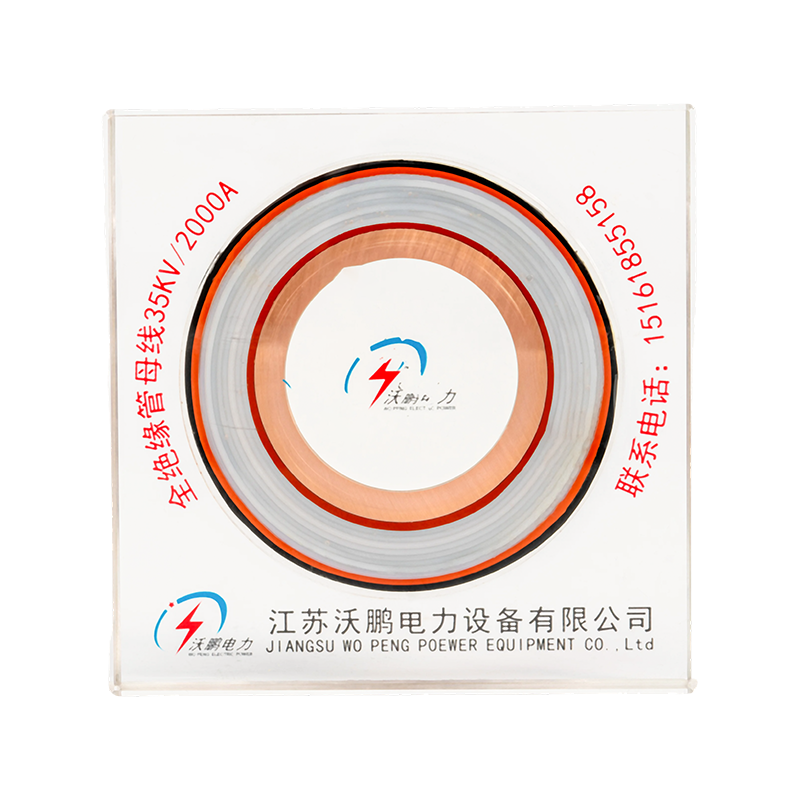
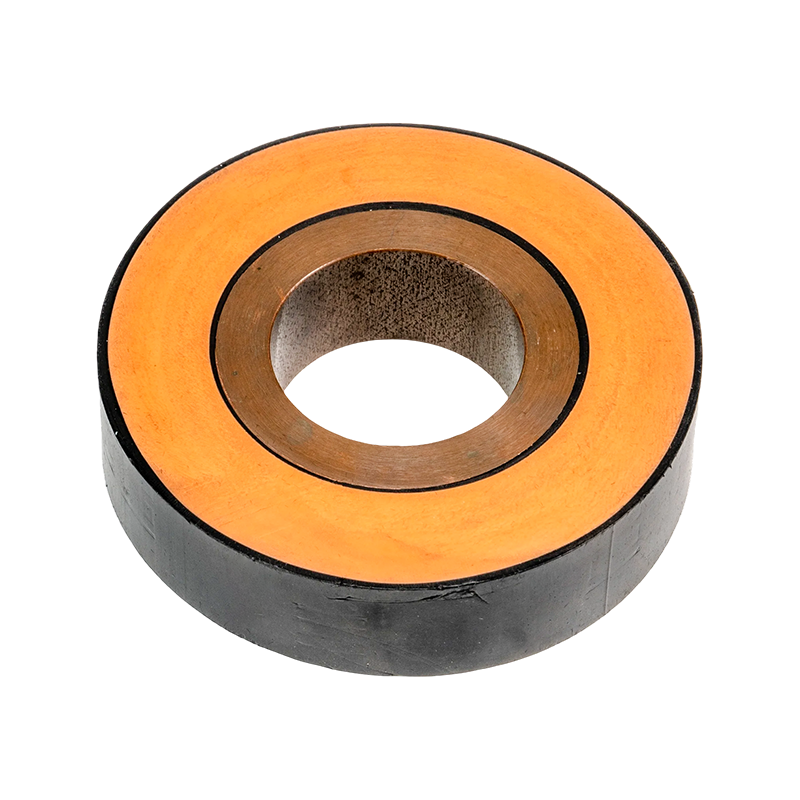
Epoxy resin casting tubular bus bar is a modern power transmission solution developed for medium- and high-voltage electrical systems that require strong insulation, reliable mechanical support, resistance to environmental stress, and stable long-term operation. Unlike conventional bare busbars or separately assembled insulated conductors, this product combines the conductor, insulation system, shielding layers, protective structure, and connection provisions into a compact tubular assembly.
The product is manufactured through an automated two-component vacuum injection and casting process. Pressure injection, vacuum treatment, and high-temperature curing allow the insulating material to surround the conductor and associated shielding components as an integrated body. This approach reduces internal voids, improves insulation consistency, and produces a nonseparable structure with strong resistance to moisture, flame, aging, and mechanical disturbance.
Epoxy resin casting tubular bus bar is suitable for power transmission between transformers, switchgear, control rooms, distribution cabinets, and other major electrical equipment. It can be configured for different voltage levels, conductor materials, current requirements, installation routes, and environmental conditions. Copper conductors are commonly selected for high conductivity and compact dimensions, while aluminum alloy or aluminum conductors may be considered where weight and cost optimization are important.
1. Product Overview
A tubular bus bar is a conductive power distribution component in which the conductor is arranged in a tubular or substantially cylindrical form. When epoxy resin is cast around the conductor under vacuum and pressure, the result is a fully insulated busbar assembly with a high level of structural integration.
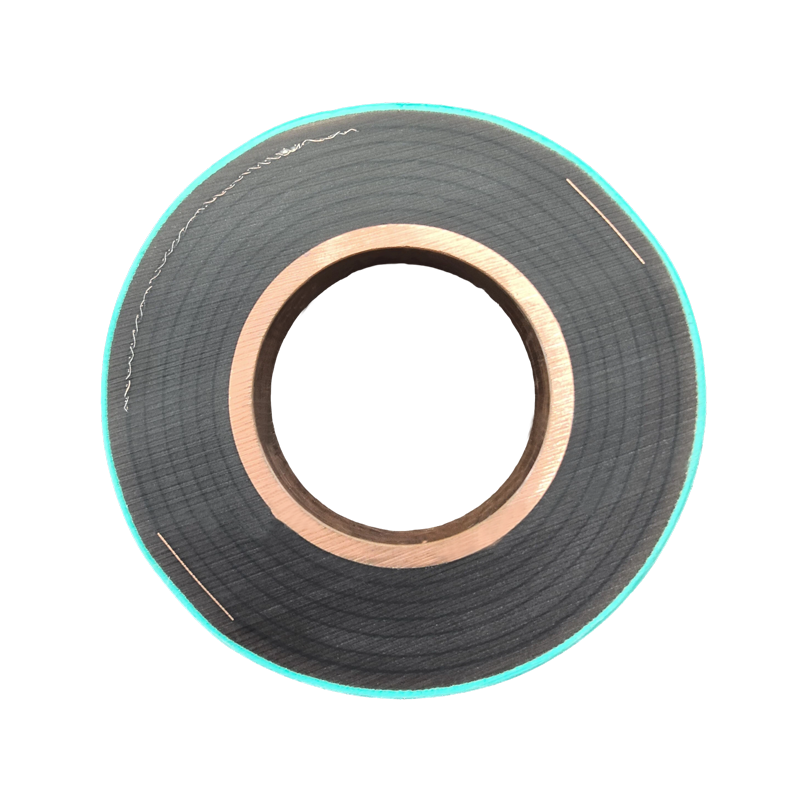
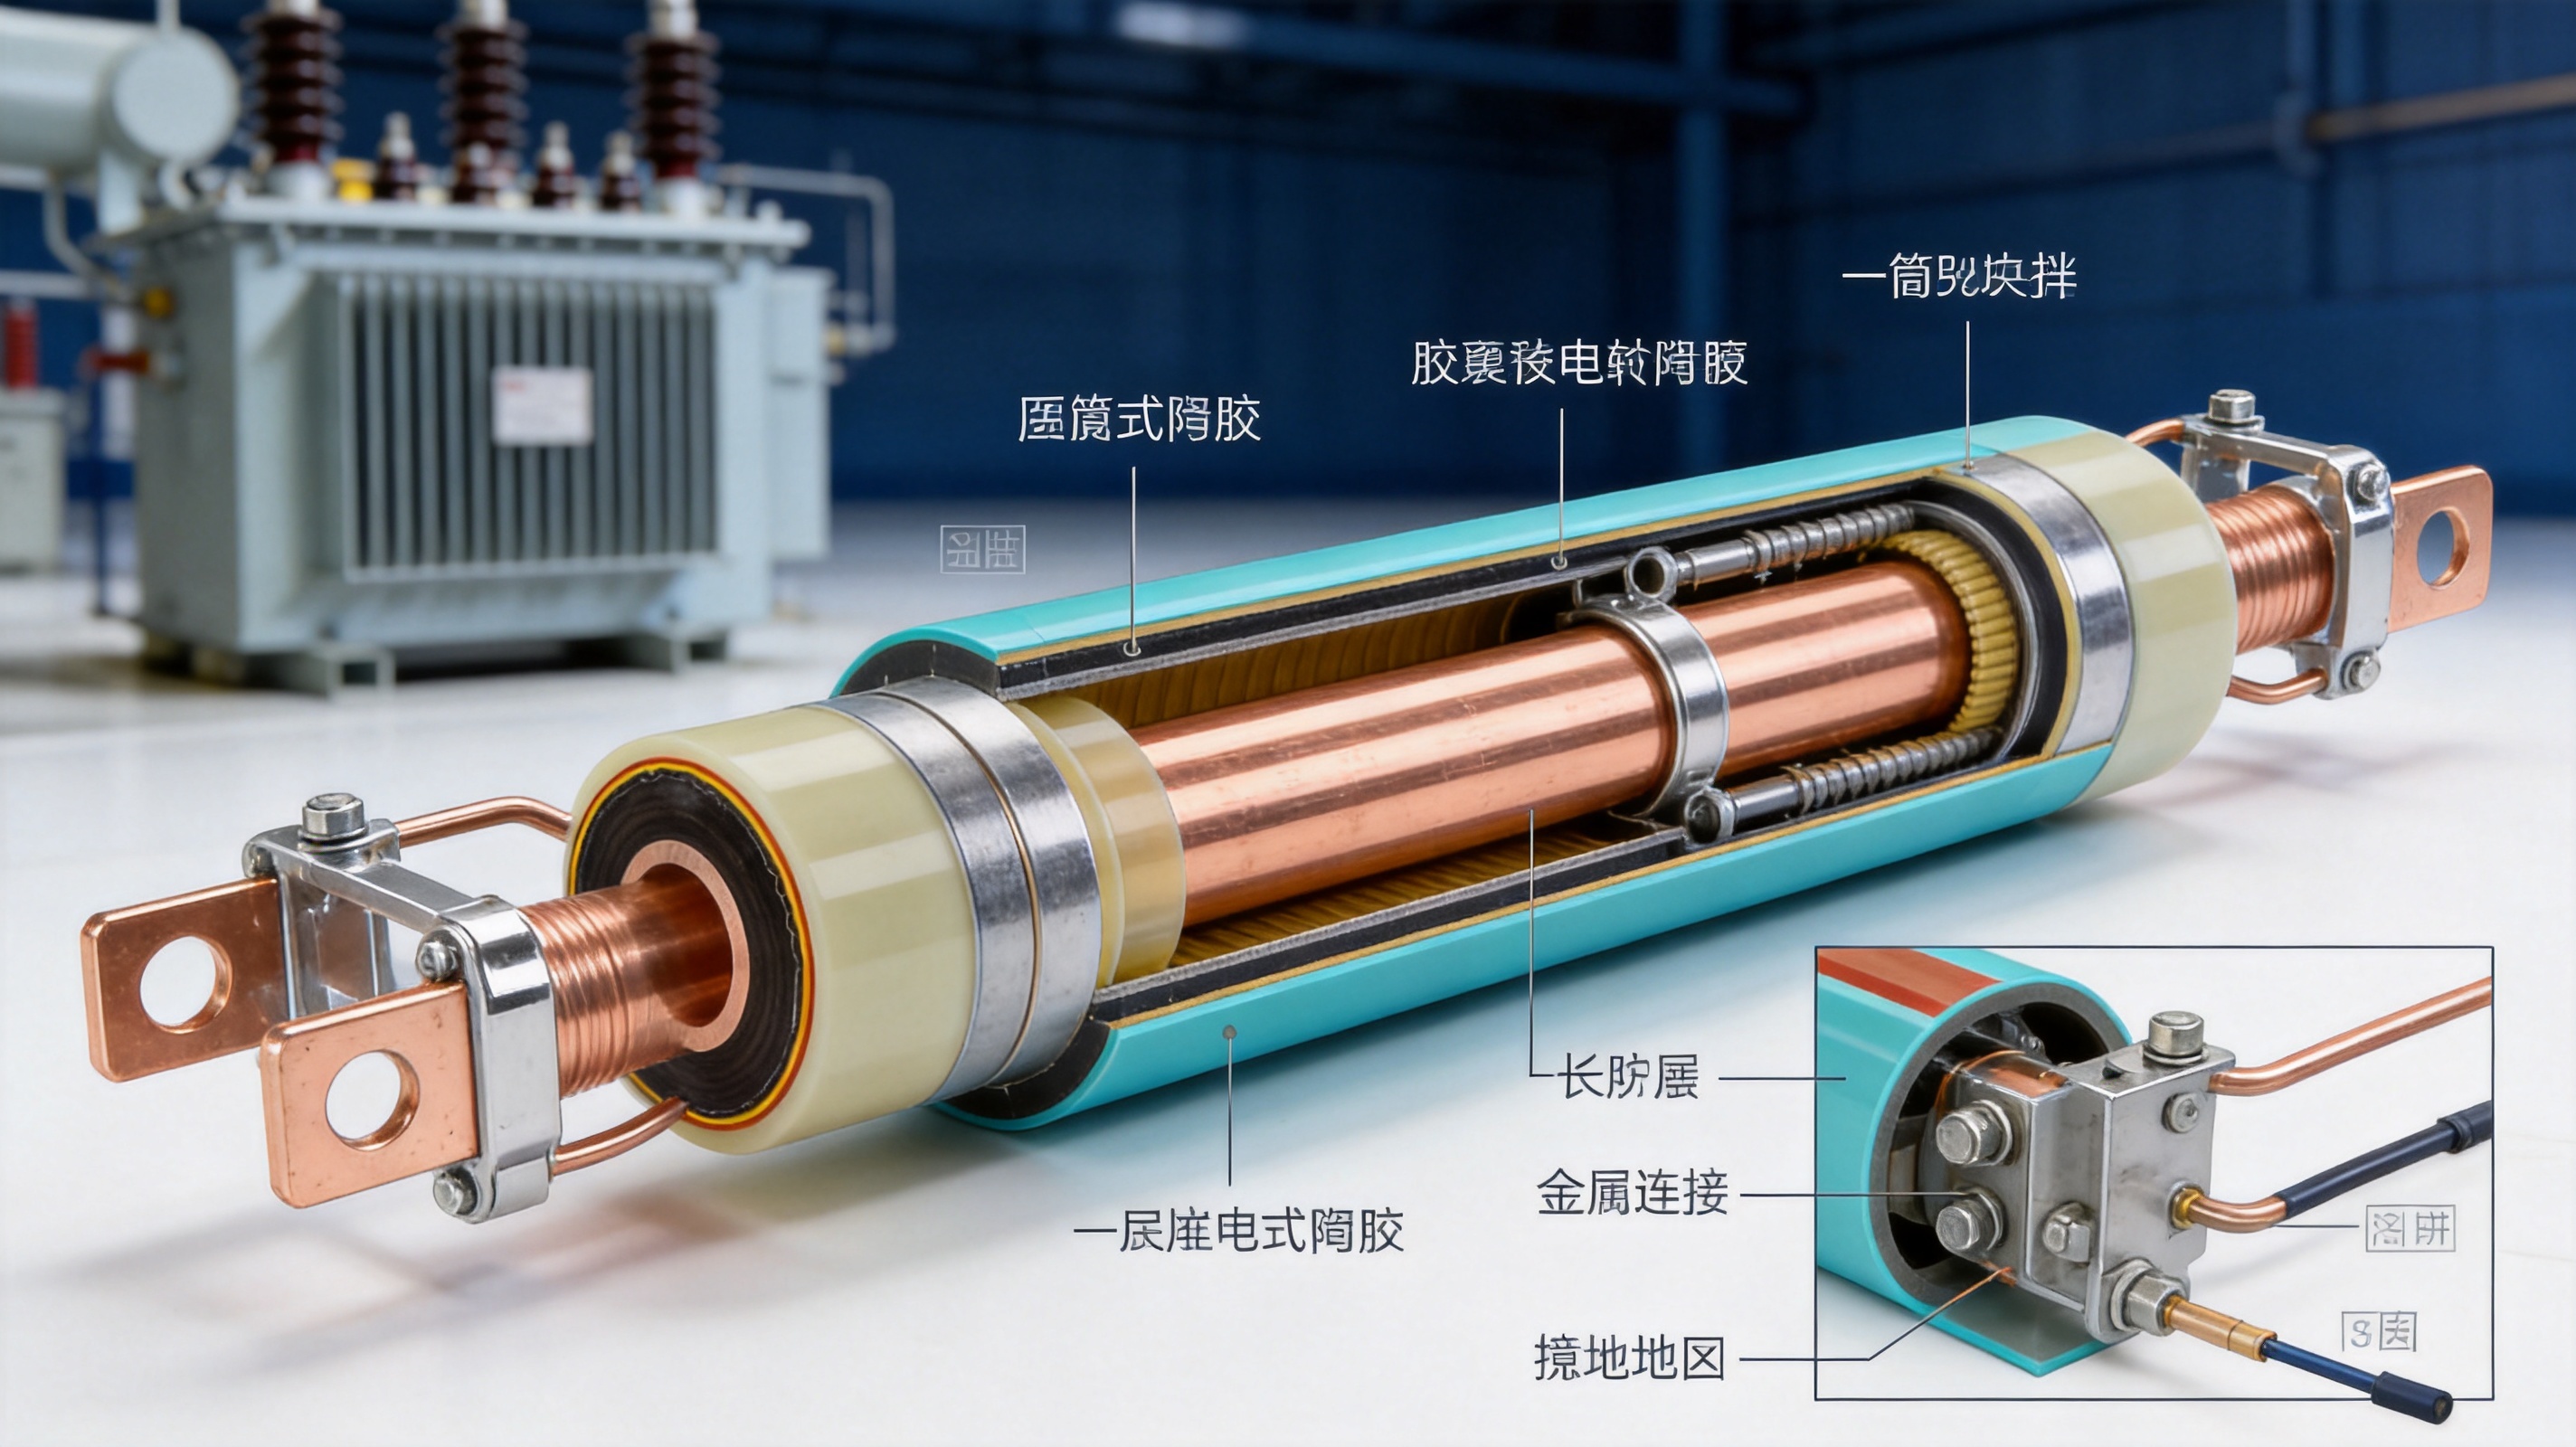
The epoxy resin casting tubular bus bar described in this article uses a conductor, inner shielding layer, semiconductive layer, outer shielding layer, metal shielding layer, and outer protective layer. These elements are formed into an integrated structure rather than being installed as a series of loose or detachable parts. The nonseparable design helps prevent displacement of internal components during transportation, installation, short-circuit forces, vibration, and thermal cycling.
The insulation joints and copper conductors are manufactured through a one-shot molding process. This allows the joint insulation and conductor body to be formed as a unified assembly without a conventional interface between separately produced insulation components. Intermediate connections use an embedded stainless steel clamp welding method. Properly designed terminal connections are connected to electrical equipment using flexible links and bolted fastening arrangements.
The system also incorporates a metal shielding layer. According to the supplied technical structure, the shielding system uses copper braided tape and copper strip or a composite structure involving tinned steel strip and copper strip, depending on the product configuration. Grounding leads are reliably welded to the metal shielding layer, and each grounding point can be identified, numbered, protected against moisture, and connected to the site grounding system.
The design objective is to provide an insulated power transmission path that is compact, mechanically stable, electrically reliable, and suitable for demanding installation environments. The product is intended to combine the advantages of conventional busbar systems with the environmental protection and installation flexibility associated with insulated cable-type solutions.
2. Integrated Structure and Operating Principle
2.1 Conductor Core
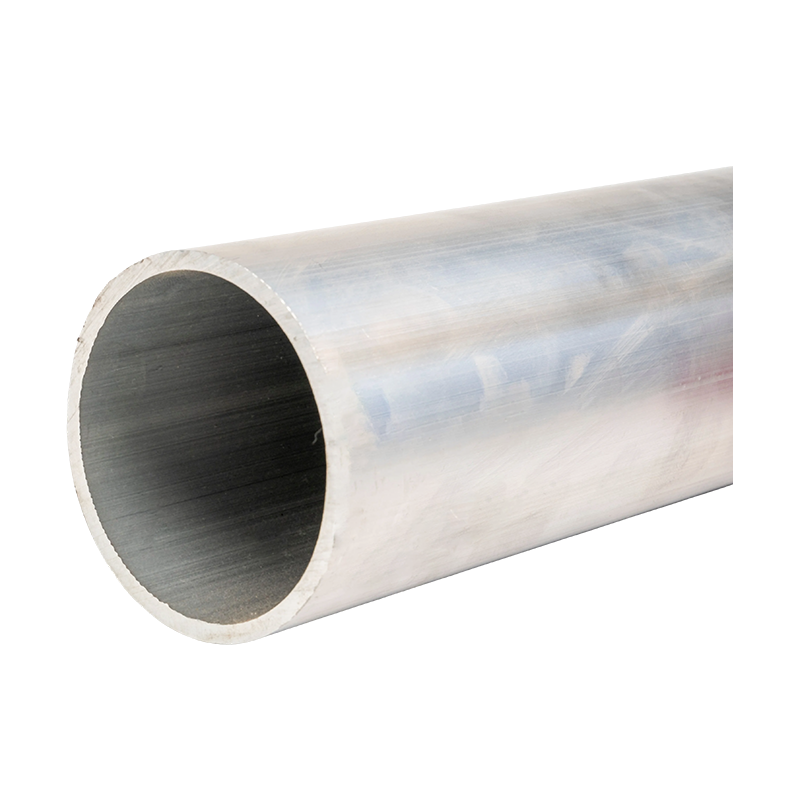
The conductor is the primary current-carrying element. High-quality copper of TZ7 grade or higher is specified for the copper conductor, with the pure copper tube having a copper content of at least 99.90 percent. This material selection provides high electrical conductivity, good thermal performance, and reliable compatibility with mechanical connection processes.
The tubular conductor shape offers useful mechanical and thermal characteristics. A tube can provide an efficient ratio between electrical cross-sectional area and structural rigidity. The final conductor dimensions are selected according to voltage level, rated current, short-circuit withstand requirements, permissible temperature rise, installation route, and connection requirements.
Where project priorities emphasize lower weight or material economy, aluminum alloy tubular bus bar may be considered as an alternative product category. Aluminum conductors require careful engineering of joints, surface treatment, contact pressure, and thermal expansion. The choice between copper and aluminum should be based on the complete system design rather than conductor material price alone.
2.2 Primary Insulation
The epoxy resin insulation layer provides electrical separation between the conductor and the external environment. The insulation is formed around the conductor by vacuum injection and pressure casting, followed by high-temperature curing. This process helps produce a dense, continuous insulating body with controlled thickness.
The supplied insulation schedule lists thicknesses associated with different voltage levels: 10 mm for 10 kV, 15 mm for 35 kV, 20 mm for 66 kV, 30 mm for 110 kV, and 45 mm for 220 kV. Actual insulation dimensions must be confirmed through project-specific electrical calculations, type testing, applicable standards, and the final approved technical specification.
Epoxy resin provides high dielectric strength, mechanical rigidity, resistance to surface contamination, and protection from moisture. It can also be formulated with flame-retardant properties. The product information identifies the structure as flame retardant and aging resistant, with a designed service life exceeding 30 years under suitable operating and maintenance conditions.
2.3 Semiconductive and Shielding Layers
Semiconductive and shielding layers help control the electric field around the conductor and reduce the risk of localized electrical stress. A well-designed shield system supports a more uniform field distribution and reduces the effect of surface irregularities, conductor geometry, and connection transitions.
The metal shield also provides an important grounding and safety function. When properly connected to the site grounding system, it can help maintain an equipotential external surface and provide a defined path for induced currents or fault-related current, subject to the design of the complete protection and grounding system.
Grounding leads are welded reliably to the metal shielding layer. Grounding points must be securely connected during site installation, protected from water and moisture, and clearly marked. Heat-shrink insulation bushings may be used around grounding connections, with visible phase colors such as yellow, green, and red where required by the installation design.
2.4 External Protection
The outer protective layer protects the insulation and shielding system from mechanical damage, contamination, handling impacts, and environmental exposure. It also contributes to the overall appearance and dimensional stability of the product.
Because the insulation, shielding, and protective layers are integrated during casting, the final assembly has fewer exposed interfaces than a system composed of separately installed insulation sleeves, shields, and covers. Fewer interfaces can simplify inspection and reduce the number of locations where moisture or contaminants may enter.
3. Advanced Vacuum Casting Manufacturing Process
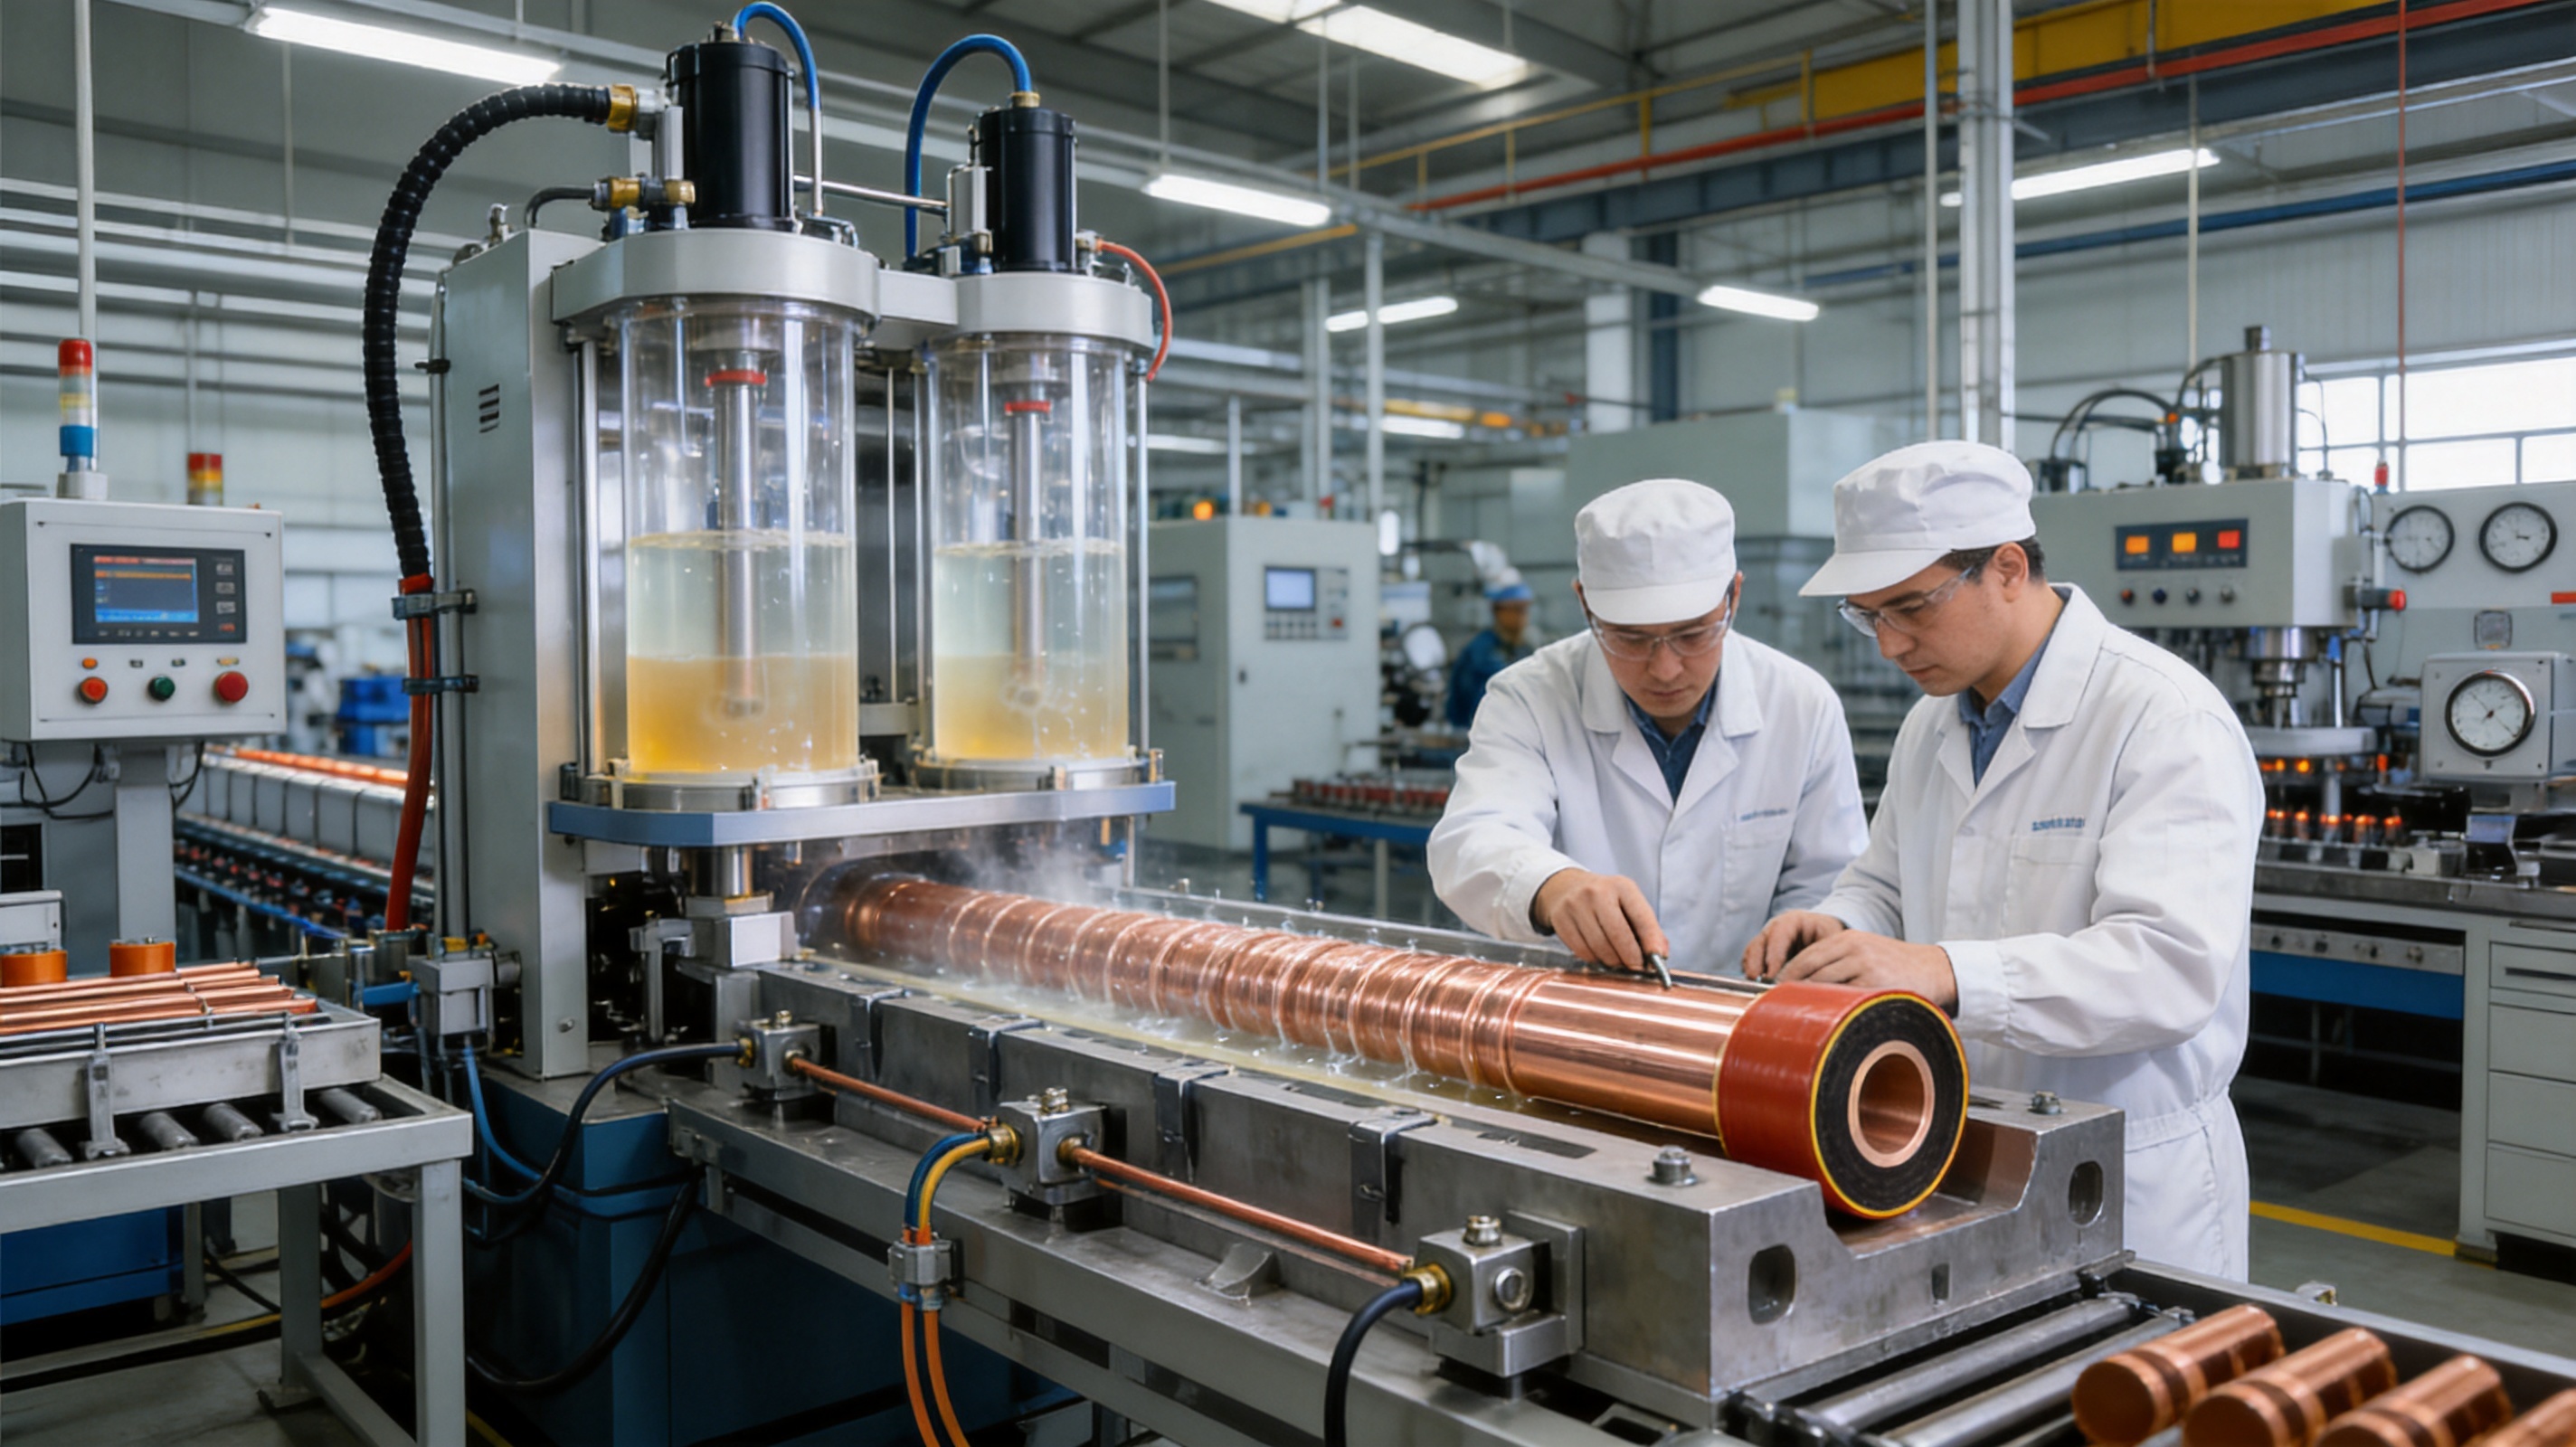
The manufacturing process is one of the principal advantages of epoxy resin casting tubular bus bar. The product is formed using an automated dual-component vacuum injection molding machine. Two resin components are accurately metered, mixed, degassed, and injected into the mold under controlled conditions.
3.1 Preparation of Materials and Components
Before casting begins, the conductor tube, shielding materials, semiconductive layers, connection elements, and mold components must be inspected and prepared. The conductor surface must be clean and free from oil, oxidation, burrs, and other contaminants that could affect electrical contact or resin adhesion.
The conductor ends are prepared for connection. The end of the copper tube should be rounded, and the connection surface may be silver plated or tin plated. These treatments help reduce contact resistance, improve corrosion resistance, and provide a stable interface for bolted or flexible connections.
Metal parts used inside or around the casting system are positioned according to the approved drawing. The alignment of the conductor and shield must be controlled carefully because eccentricity can influence insulation thickness, electric-field distribution, and mechanical balance.
3.2 Vacuum Treatment
Moisture and trapped air are important concerns in cast insulation. Voids, bubbles, or foreign particles inside the insulation can create local electric-field concentration and reduce dielectric reliability. Vacuum treatment is therefore used to remove air and help reduce the possibility of internal voids.
The vacuum stage is applied to the mold and, where applicable, to the resin components before injection. Resin storage, mixing, temperature, viscosity, and vacuum level must be controlled within the process window established by the manufacturer. The purpose is not simply to fill the mold, but to create a dense and uniform insulation body with consistent bonding to the prepared components.
3.3 Two-Component Mixing and Pressure Injection
Epoxy resin systems generally contain a resin component and a curing component. The automated equipment meters the components in a controlled ratio and mixes them before injection. Accurate proportioning is essential because an incorrect mixture can affect curing, mechanical strength, dielectric performance, thermal stability, and long-term aging behavior.
Pressure injection helps the mixed material flow through the mold and around the conductor and shielding structure. Controlled pressure supports complete filling of complex sections, including joint areas and transition regions. The process also improves repeatability compared with manual pouring or uncontrolled gravity filling.
Automated injection reduces variation between production batches. It can also support the recording of process parameters such as resin temperature, injection pressure, vacuum level, mixing ratio, filling time, and curing conditions. These records strengthen traceability and help quality personnel identify deviations before products are released.
3.4 High-Temperature Curing
After filling, the casting is cured under controlled temperature conditions. High-temperature curing allows the epoxy resin to develop its designed mechanical and electrical properties. The curing schedule must be matched to the resin formulation, casting dimensions, mold temperature, and product design.
Uniform curing is important for dimensional stability and resistance to thermal cycling. An under-cured product may have insufficient mechanical strength or electrical performance, while excessive or uneven curing can create internal stress. Automated production equipment and standardized process instructions help maintain consistent curing quality.
3.5 Inspection and Verification
After demolding and finishing, each product should undergo visual, dimensional, electrical, and mechanical inspections according to the applicable quality plan. Typical checks include surface appearance, casting integrity, conductor dimensions, joint dimensions, shield continuity, grounding connection quality, insulation resistance, and high-voltage withstand performance.
The company information indicates that production is supported by vacuum casting systems, CNC machining equipment, and automated assembly technologies. Standardized inspections include high-voltage tests, insulation tests, mechanical verification, and routine quality checks. Cooperation with third-party testing institutions provides additional independent validation for safety and performance.
Epoxy Resin Casting Tubular Bus Bar
4. Main Technical Advantages
4.1 Monolithic and Nonseparable Construction
The integrated casting method combines the conductor, insulation, shielding layers, and protective structure into a single body. This is a major distinction from systems assembled from multiple detachable insulation and shielding components.
A monolithic design can reduce the possibility of layer movement, loosened insulation, and incorrect assembly. It also provides a stable geometry over the service life of the system. During installation, the product is handled as a designed assembly rather than as a collection of individual layers that must be positioned manually in the field.
The nonseparable structure is particularly useful in locations where vibration, thermal expansion, limited access, or difficult installation conditions make field assembly challenging. It also simplifies the task of protecting the internal insulation system from accidental damage.
4.2 Strong Insulation and Environmental Protection
Epoxy resin insulation provides a solid barrier against dust, moisture, and many common industrial contaminants. Unlike exposed bare conductors, the insulated tubular bus bar does not rely on large air clearances alone to maintain electrical separation. This allows more compact routing and can support safer installation in areas with restricted space.
The supplied environmental design includes operation at altitudes up to 4,000 meters, minimum ambient temperatures down to -45°C, maximum ambient temperatures up to +60°C, daily temperature variation of 35 K, solar radiation intensity of 1,000 W/m², and maximum wind speed of 40 m/s. Daily average relative humidity is specified at up to 95 percent, with a monthly average of up to 90 percent. Ice thickness is specified at no more than 20 mm.
These conditions describe a demanding design envelope. The suitability of a particular installation must still be confirmed through the final product rating, enclosure arrangement, terminal design, site altitude correction, and project-specific testing.
4.3 Flame Retardance and Aging Resistance
The product structure is designed to provide flame-retardant performance and resistance to aging. These properties are important in substations, industrial plants, high-rise buildings, hospitals, data centers, and other facilities where electrical equipment must limit the spread of fire and maintain safe operation over long periods.
The product is designed for a service life of more than 30 years. Actual life depends on operating temperature, load profile, short-circuit events, ultraviolet exposure, chemical contamination, installation quality, connection maintenance, and the environmental conditions specified for the project.
4.4 Reliable Joint Technology
Joints are often the most sensitive parts of a busbar system because they combine electrical contact, mechanical load, thermal expansion, insulation transition, and field control. The product design addresses these requirements through one-shot molded insulation joints, embedded stainless steel clamp welding for intermediate connections, and flexible bolted links at equipment interfaces.
The supplied technical information states that the temperature rise at terminal joints is lower than that of the conductor body. This characteristic indicates that the joint design is intended to minimize contact resistance and manage heat effectively. Actual temperature-rise performance must be verified for the selected current rating and installation arrangement.
Flexible links between the tubular busbar terminal and connected equipment can accommodate small alignment differences and reduce mechanical stress on transformer or switchgear terminals. Bolted fastening permits controlled installation and future inspection when required by the maintenance plan.
4.5 Shielded and Grounded Design
A fully shielded structure offers advantages in electric-field management and personnel safety. The metal shielding layer is connected to grounding leads by reliable welding, while grounding points are marked and numbered for inspection and commissioning.
Moistureproof measures at grounding points are important because exposed or poorly sealed connections can become vulnerable to corrosion and insulation degradation. Heat-shrink components, protective covers, sealing materials, and appropriate installation practices can help preserve the grounding system over time.
4.6 Compact Installation
Compared with conventional open busbar arrangements, an insulated tubular busbar can reduce required phase-to-phase and phase-to-ground clearances, subject to the applicable standards and product design. It can therefore be routed through cable trenches, cable mezzanines, switchgear interfaces, and other areas where open conductors would be difficult to install.
Compact routing can reduce the amount of supporting steelwork and improve the visual organization of a power distribution room. It may also reduce exposure to accidental contact, dust accumulation, and external objects.
5. Comparison with Conventional and Alternative Busbar Systems
Different busbar technologies are suitable for different electrical and environmental conditions. A proper comparison should consider not only insulation material, but also connection design, short-circuit strength, heat dissipation, installation conditions, maintenance, fire performance, and total lifecycle cost.
| Characteristic | Epoxy Resin Casting Tubular Bus Bar | Silicone Rubber Insulated Bus Bar | PVC Insulated Bus Bar | Conventional Bare Busbar |
|---|---|---|---|---|
| Insulation structure | Solid cast, integrated epoxy structure | Flexible elastomeric insulation | Polymeric insulated covering | Air insulation with exposed conductor |
| Mechanical rigidity | High | Medium to high, depending on design | Medium | High conductor rigidity but exposed system |
| Moisture resistance | Excellent when correctly cast and sealed | Good | Generally lower in severe environments | Dependent on enclosure and clearances |
| Fire performance | Flame-retardant formulations available | Formulation dependent | Formulation dependent and commonly lower | No insulation flame contribution, but exposed arc and fault risks remain |
| Protection against contamination | High due to solid external insulation | Good | Moderate | Requires environmental control and cleaning |
| Field assembly requirements | Pre-engineered integrated sections with defined joints | Requires controlled assembly and termination | Requires controlled assembly and termination | Requires clearances, supports, and exposed connection work |
| Typical advantage | Compact, strong, shielded, and environmentally resistant | Flexible installation and good insulation performance | Economical for less demanding applications | Simple visual inspection and high natural heat dissipation |
Compared with silicone rubber insulation, epoxy resin casting generally provides a more rigid and structurally integrated assembly. Silicone rubber may offer greater flexibility, which can be beneficial where repeated movement or complex bends are required. Epoxy casting is often preferred where mechanical strength, dimensional stability, and a solid molded structure are priorities.
Compared with PVC insulation, epoxy resin provides a stronger solid structure and better suitability for high-voltage or harsh industrial environments when correctly formulated and tested. PVC products may remain attractive for lower-voltage or cost-sensitive installations, but their suitability must be evaluated against temperature, fire, moisture, and mechanical requirements.
Compared with bare busbar, the fully insulated tubular design offers improved protection against accidental contact, contamination, and moisture. Bare busbar may have advantages in heat dissipation and visual access, but it requires greater clearances, stronger environmental control, and more extensive safety protection.
6. Voltage Range and Design Parameters
The product structure can be engineered for several voltage classes. The supplied insulation table includes 10 kV, 35 kV, 66 kV, 110 kV, and 220 kV configurations, with corresponding nominal insulation thicknesses. The company’s stated product portfolio focuses particularly on 35 kV epoxy resin vacuum-cast tubular busbars while also covering low-voltage and other tubular busbar solutions.
Voltage rating alone does not determine the correct product. Engineers must also evaluate rated current, short-time withstand current, peak withstand current, system frequency, lightning impulse withstand level, power-frequency withstand voltage, creepage distance, pollution level, altitude, ambient temperature, and installation method.
The supplied environmental data identifies pollution level V or serious pollution conditions in one technical description, with a creepage distance design value of 31 mm/kV. It also mentions an outdoor terminal arrangement with a climbing device and a total climbing distance of at least 680 mm. These details should be confirmed against the final applicable standard and project drawings.
Temporary overvoltage conditions must also be considered. The provided requirements state that temporary overvoltage should not exceed eight hours within a 24-hour period or 125 hours during a full year. Protection coordination, system grounding, surge arresters, and switching practices should be reviewed together with the busbar insulation design.
The maximum suspended span is specified as no more than five meters. This limit is important because the busbar must remain mechanically stable under its own weight, wind loading, seismic activity, conductor electromagnetic forces, thermal expansion, and installation loads. Supports and hangers must be designed according to the actual product mass and site conditions.
7. Environmental and Mechanical Performance
7.1 Temperature
The product is designed for a wide ambient temperature range. The supplied environmental information gives a minimum ambient temperature of -45°C and a maximum of +60°C. The epoxy resin system, conductor, joint components, seals, and external protective materials must all be compatible with the project temperature range.
Temperature rise is affected by current, conductor dimensions, installation spacing, surrounding air movement, enclosure conditions, support design, and connection resistance. A complete thermal study should be carried out for high-current applications. The rated current should not be selected from conductor size alone.
7.2 Humidity and Moisture
High humidity can affect exposed metal surfaces, grounding connections, joint interfaces, and unsealed insulation systems. The solid epoxy structure provides strong resistance to moisture ingress, but the ends, joints, grounding points, and equipment interfaces still require careful sealing and installation.
Waterproof and moistureproof measures should be applied at grounding points and terminal transitions. During storage and transportation, products should be protected from standing water, condensation, and impact. Any protective packaging should remain in place until the product is ready for installation.
7.3 Wind and Ice
For outdoor routes, wind and ice loads can place substantial mechanical stress on supports and joints. The supplied design conditions include a maximum wind speed of 40 m/s and ice thickness of up to 20 mm. These values should be incorporated into structural calculations, especially for elevated spans and exposed terminal arrangements.
7.4 Seismic Conditions
The design conditions include seismic intensity of eight degrees, ground horizontal acceleration of 0.20 g, vertical acceleration of 0.15 g, a frequency of 20 Hz, and a sine-wave endurance period of three cycles. These requirements highlight the importance of support spacing, connection flexibility, equipment interface design, and mechanical verification.
Flexible connections to transformers and switchgear can help accommodate relative movement. However, flexibility must not compromise electrical clearance, shielding continuity, grounding integrity, or terminal support. Seismic engineering must address the complete system rather than the busbar body alone.
8. Typical Applications
8.1 Transformer-to-Switchgear Connections
One of the most common applications is the connection between the low-voltage or medium-voltage terminals of a main transformer and the terminals of a switch cabinet or control room. The tubular busbar can provide a direct, organized, and insulated route for high-current power transmission.
This arrangement is suitable for substations, industrial plants, power generation facilities, and large commercial buildings. It can be installed above ground, through a cable trench, or through a cable mezzanine, depending on the project layout.
8.2 Cable Trenches and Cable Mezzanines
Where overhead routing is impractical, the busbar can be installed through underground cable trenches or cable mezzanines. The fully insulated structure is particularly useful where the route passes through restricted areas or where conventional open conductors would require excessive clearance.
Care must be taken to provide drainage, ventilation, support access, fire separation, and sufficient working space. The busbar should not be exposed to unexpected mechanical loads from other services, standing water, or construction activities.
8.3 Switchgear Interconnections
Tubular busbars can connect adjacent switch cabinets or form the top or bottom cable connection arrangement of a switchgear system. The preferred route depends on equipment layout, cable entry direction, maintenance requirements, and the available space around the switchgear.
Flexible links and bolted joints allow the product to interface with equipment terminals while accommodating small alignment variations. Correct torque, contact surface preparation, plating, and joint inspection are essential for reliable operation.
8.4 Renewable Energy Facilities
Solar and wind power facilities often include transformer stations, converter systems, collector circuits, and compact electrical rooms. Tubular busbars can be used where high-current transmission, insulation, space efficiency, and resistance to environmental contamination are required.
Wind power applications may impose vibration, temperature variation, and restricted routing conditions. The mechanical strength and integrated construction of cast tubular busbars can be valuable, although the final design must account for nacelle movement, tower structure, maintenance access, and equipment-specific vibration behavior.
8.5 Industrial and Commercial Infrastructure
Petrochemical, metallurgy, manufacturing, rail transit, hospitals, data centers, and high-rise buildings require dependable power distribution with strong fire and insulation performance. The compact structure of epoxy resin casting tubular busbar can help organize crowded electrical rooms and reduce exposure to dust and accidental contact.
For critical facilities, the selection process should include redundancy, maintenance bypass arrangements, fire compartmentation, emergency power coordination, and the consequences of a busbar outage.
9. Manufacturing Strengths and Quality Management
A reliable tubular busbar depends on more than the resin formulation. It requires coordinated control of conductor fabrication, mold design, vacuum equipment, mixing accuracy, curing, CNC machining, joint preparation, assembly, testing, and documentation.
Jiangsu Wopeng Power Technology Co., Ltd. was founded in 2018 as a specialized high-tech enterprise focused on high- and low-voltage busbar systems. Its stated product range includes 35 kV epoxy resin vacuum-cast tubular busbars, low-voltage cast-resin busways, copper and aluminum tubular busbars, wind power tubular busbars, compact busbar systems, and sliding contact line systems.
The company operates production lines equipped with vacuum casting systems, CNC machining equipment, and automated assembly technologies. These capabilities support the dimensional accuracy and process repeatability required for molded electrical products. CNC equipment is particularly useful for conductor ends, joint surfaces, drilling patterns, and other components requiring controlled tolerances.
Automated assembly helps standardize the positioning of shielding layers, connection components, grounding leads, and protective parts. Standardized processes reduce dependence on individual operator technique and help create consistent product records.
The company reports that its products undergo high-voltage tests, insulation tests, mechanical verification, and routine quality inspections. Third-party testing cooperation provides an additional level of validation. For purchasers, the availability of type test reports, routine test records, material certificates, inspection plans, and installation instructions is an important indicator of supplier capability.
Engineering strength is also important because tubular busbar systems are usually customized. The supplier must interpret transformer and switchgear terminal drawings, calculate support arrangements, coordinate phase spacing, design transitions, confirm short-circuit forces, and provide route-specific manufacturing drawings.
Wopeng reports that its products operate across more than 17 provinces and key industrial sectors. This field experience can help the company address different environmental conditions, project layouts, installation methods, and customer requirements. The stated engineering team includes engineers, technical specialists, and production professionals with experience in power equipment technology.
9.1 Process Traceability
For cast-resin products, traceability should extend from incoming raw materials to final testing. Resin batch numbers, conductor material records, mixing ratios, vacuum conditions, injection parameters, curing temperatures, and inspection results should be retained according to the quality management procedure.
Traceability supports root-cause analysis if a deviation is discovered. It also provides customers with confidence that each section has been produced according to the approved design rather than relying solely on a final visual inspection.
9.2 Testing Capability
Electrical testing may include insulation resistance, power-frequency withstand, impulse withstand where applicable, partial discharge evaluation, shield continuity, and conductor resistance. Mechanical testing may include dimensional inspection, terminal strength, support verification, vibration assessment, and short-circuit force evaluation.
Not every test applies to every product configuration. The test plan should be established according to voltage class, applicable standards, customer specifications, and the intended installation environment. Type tests validate the design, while routine tests confirm the quality of each manufactured unit.
10. Installation and Commissioning Considerations
Installation should be carried out by qualified personnel using approved drawings and procedures. Before installation, the route should be inspected for correct dimensions, support locations, equipment alignment, drainage, access, and clearance from other systems.
Busbar sections should be lifted using approved methods that prevent bending, impact, and damage to terminal components. The product should not be dragged across the ground or used as a support for cables, tools, scaffolding, or unrelated equipment.
Connection surfaces must be clean and correctly prepared. Silver-plated or tin-plated conductor ends should not be damaged during handling. Bolts and screws are specified as hot-dip galvanized materials in the supplied requirements. Fasteners should be tightened to the approved torque, and the torque record should be retained where required.
Intermediate stainless steel clamp welds and field metal welding should be checked carefully. Anti-rust treatment is required for metal welding performed during site construction. Grounding points must be connected securely, protected against moisture, and marked according to the approved grounding diagram.
After installation, the system should be inspected for phase identification, support spacing, terminal alignment, shield continuity, grounding continuity, joint torque, clearances, sealing, and visible surface damage. Electrical tests should be performed before energization, and test results should be compared with the acceptance criteria.
The system should be energized only after all covers, flexible connections, grounding links, and protective components are correctly installed. Any abnormal noise, odor, temperature, partial discharge indication, or protection operation during commissioning should be investigated immediately.
11. Maintenance and Service Life
One advantage of a solid cast tubular busbar is that routine maintenance can be less extensive than maintenance for exposed conductors or systems with many detachable insulation components. Nevertheless, the product remains part of a critical electrical system and requires periodic inspection.
Maintenance activities may include visual inspection of the external insulation, checking for cracks or impact marks, inspecting terminal covers and flexible links, verifying grounding connections, checking support structures, monitoring temperature, and reviewing protection records.
Thermal imaging can help identify abnormal heating at joints and terminals while the system is energized, provided the inspection is performed safely and according to site procedures. A temperature rise that differs significantly from neighboring phases or from previous measurements may indicate loose fasteners, contamination, contact degradation, overload, or ventilation problems.
Grounding points should remain identifiable and accessible for inspection. Moisture seals and heat-shrink components should be checked for damage. Outdoor installations should also be inspected for ultraviolet degradation, corrosion of exposed hardware, water accumulation, and damage caused by ice or windborne objects.
The designed service life is more than 30 years, while some general product descriptions refer to possible service lives of 30 to 40 years under normal conditions. These figures are design expectations rather than a substitute for correct operation and maintenance. Excessive overloading, repeated short-circuit events, improper installation, chemical attack, or prolonged exposure beyond the rated environment can reduce service life.
12. Selection Guide for Project Owners and Engineers
Selection should begin with the electrical system requirements. The purchaser should provide system voltage, rated current, frequency, fault current, duration of short circuit, insulation coordination parameters, transformer and switchgear terminal drawings, route dimensions, support conditions, and environmental data.
The required conductor material should then be selected. Copper is appropriate where high conductivity, compact size, and strong connection performance are priorities. Aluminum or aluminum alloy may be considered where weight reduction and material economy are important. The thermal expansion, joint construction, surface treatment, and installation tools for the selected conductor must be included in the engineering review.
The installation environment determines the required insulation, shielding, sealing, creepage distance, and mechanical support. Outdoor, coastal, high-altitude, dusty, humid, chemically aggressive, seismic, or high-wind sites may require special materials and additional protection.
The customer should also confirm whether the busbar will be suspended, supported on a structure, installed in a trench, routed through a mezzanine, or connected directly to switchgear. The maximum suspended span should not exceed the approved design limit, and support details should be checked against the product mass and site load conditions.
Finally, the supplier’s technical and manufacturing capability should be evaluated. Important documentation includes general arrangement drawings, conductor material certificates, insulation specifications, type test reports, routine test procedures, installation manuals, joint details, grounding diagrams, maintenance instructions, and quality certificates.
13. Frequently Asked Questions
Q1: What is an epoxy resin casting tubular bus bar?
An epoxy resin casting tubular bus bar is an insulated power transmission assembly in which a copper, aluminum, or aluminum alloy tubular conductor is surrounded by a molded epoxy resin insulation system. Shielding, grounding, and protective layers are integrated into the structure to provide electrical insulation, mechanical strength, and environmental protection.
Q2: What voltage levels can the product support?
The supplied technical information lists configurations associated with 10 kV, 35 kV, 66 kV, 110 kV, and 220 kV voltage levels. The actual rating depends on insulation coordination, conductor design, shielding, terminal structure, testing, and the applicable project standards.
Q3: What is the designed service life?
The product is designed for a service life exceeding 30 years under suitable operating and maintenance conditions. Some general product information indicates a possible service life of 30 to 40 years under normal conditions. Actual life depends on temperature, load, environment, installation quality, and fault history.
Q4: Is it suitable for outdoor installation?
It can be engineered for outdoor applications when the complete design includes suitable external protection, terminal sealing, creepage distance, grounding, ultraviolet resistance, mechanical supports, and weather protection. The outdoor suitability of each configuration must be confirmed with the supplier before ordering.
Q5: How does the product resist moisture?
The solid epoxy insulation provides a dense barrier against moisture, while the integrated structure reduces exposed interfaces. However, terminal joints, grounding points, and equipment connections must still be sealed and protected. Waterproof and moistureproof measures are specifically required at grounding points.
Q6: What conductor material is used?
The supplied specification identifies TZ7 or higher-grade oxygen-free copper, with copper content of at least 99.90 percent for the pure copper tube. Copper, aluminum, and aluminum alloy configurations may be available depending on the product series and project requirements.
Q7: How are the busbar sections connected?
Insulation joints are formed through a one-shot molding process. Intermediate connections use embedded stainless steel clamp welding, while connections to transformers, switchgear, or other equipment use flexible links secured by bolts. The conductor end should be rounded and silver plated or tin plated where specified.
Q8: What is the maximum suspended span?
The supplied requirement states that the maximum suspended span should not exceed five meters. The actual support arrangement must also consider product weight, wind, ice, seismic forces, thermal expansion, and short-circuit mechanical forces.
Q9: What tests should be requested from a supplier?
Purchasers should request applicable type test reports, routine test procedures, high-voltage withstand results, insulation resistance results, conductor resistance data, shield continuity records, mechanical verification, material certificates, and inspection documentation. The specific test list should match the voltage class and project standards.
Q10: Why choose a cast tubular busbar instead of a conventional bare busbar?
A cast tubular busbar provides solid insulation, shielding, protection against contamination, compact routing, improved accidental-contact protection, and a nonseparable mechanical structure. Bare busbar may provide excellent heat dissipation and simple visual access, but it normally requires greater clearances and stronger environmental controls.
Q11: Can the product be customized?
Yes. Tubular busbar systems are commonly customized according to voltage, current, conductor material, route length, terminal orientation, support method, connection type, environmental conditions, and equipment interface drawings. Customization should be completed through approved engineering drawings and technical confirmation.
Q12: What makes the manufacturing process advanced?
The main process advantages are automated two-component metering and mixing, vacuum treatment, pressure injection, high-temperature curing, CNC machining, automated assembly, and standardized electrical and mechanical inspection. These methods improve repeatability, reduce internal void risk, and support traceable production.
14. Conclusion
Epoxy resin casting tubular bus bar is a high-performance solution for insulated power transmission in medium- and high-voltage systems. Its integrated epoxy structure combines the conductor, insulation, shielding, grounding provisions, and protective layers into a stable assembly. The resulting product is compact, mechanically strong, resistant to moisture and contamination, and suitable for demanding installation environments.
The most important technical advantages include one-shot molded insulation joints, embedded stainless steel clamp welding, low-resistance conductor connections, fully shielded construction, reliable grounding, flame-retardant performance, aging resistance, and a designed service life exceeding 30 years. These features distinguish the product from conventional bare busbars and from less integrated insulated busbar alternatives.
Manufacturing quality is central to product reliability. Automated vacuum casting, controlled two-component mixing, pressure injection, high-temperature curing, CNC machining, automated assembly, and standardized testing provide the process foundation required for consistent performance. A supplier with engineering experience, production capability, testing resources, and project application knowledge can further reduce installation and operational risks.
For project owners and electrical engineers, the correct selection should consider voltage, current, fault level, route arrangement, environment, support spacing, terminal design, grounding, testing, and maintenance. When these factors are addressed through a complete engineering process, epoxy resin casting tubular bus bar can provide a dependable, safe, and space-efficient power transmission system for substations, industrial facilities, renewable energy projects, commercial buildings, rail transit, and other critical infrastructure.
References
1. Manufacturer-provided technical description for epoxy resin casting tubular bus bar, including structure, materials, environmental conditions, connection requirements, and insulation thickness data.
2. Manufacturer-provided product and company information for high- and low-voltage busbar systems, vacuum casting production, CNC machining, automated assembly, and quality inspection.
3. IEC 62271 series, High-voltage switchgear and controlgear.
4. IEC 61439 series, Low-voltage switchgear and controlgear assemblies.
5. IEC 60840, Power cables with extruded insulation and their accessories for rated voltages above 30 kV up to 150 kV.
6. IEC 60071 series, Insulation coordination.
7. IEC 60243 series, Electrical strength of insulating materials.
8. UL 94, Tests for Flammability of Plastic Materials for Parts in Devices and Appliances.
9. General engineering practices for busbar system design, conductor jointing, grounding, thermal verification, seismic support, and electrical commissioning.
Product: Epoxy Resin Casting Tubular Bus Bar


-
 +86-180 3625 3000
-
 admin@wpbusbar.com
-
 No. 8, Yanjin Road, Chengxi Industrial Park, Shanyang Town, Baoying County, Yangzhou City, Jiangsu Province, China
Copyright © Jiangsu Wopeng Power Technology Co., Ltd.
All Rights Reserved.
 Custom Insulated Bus Bar Manufacturer
Tubular Busbar System Factory