

 EN

 English
 русский
 Français
 Español
 عربى
Reinforcing Steel Aluminum Strand: High-Strength Conductors for Reliable Power Transmission
Content
- 1 1. What Is Reinforcing Steel Aluminum Strand?
- 2 2. Operating Principle of the Composite Structure
- 3 3. Main Technical Specifications
- 4 4. Advantages Compared with Conventional Conductors
- 5 5. Manufacturing Process and Quality Control
- 6 6. Environmental and Mechanical Performance
- 7 7. Applications in Electrical Infrastructure
- 8 8. Installation and Maintenance Recommendations
- 9 9. Why Choose Jiangsu Wopeng Power Technology?
- 10 10. Comparison with Competing Conductor Designs
- 11 11. Selection Guide for Engineers and Buyers
- 12 12. Frequently Asked Questions
- 12.1 Q1: What is the main purpose of the steel core?
- 12.2 Q2: Does the steel core carry electrical current?
- 12.3 Q3: What is the available size range?
- 12.4 Q4: Can the product be used for long transmission spans?
- 12.5 Q5: Can it be used in coastal environments?
- 12.6 Q6: What delivery length is normally available?
- 12.7 Q7: What standards should buyers request?
- 12.8 Q8: How should the conductor be installed?
- 12.9 Q9: What fittings are recommended for aluminum-to-steel connections?
- 12.10 Q10: How does the product compare with an all-aluminum conductor?
- 12.11 Q11: What inspections are important after installation?
- 12.12 Q12: Can the manufacturer provide customized solutions?
- 13 13. Conclusion
- 14 References
- 15 Product: Reinforcing Steel Aluminum Strand
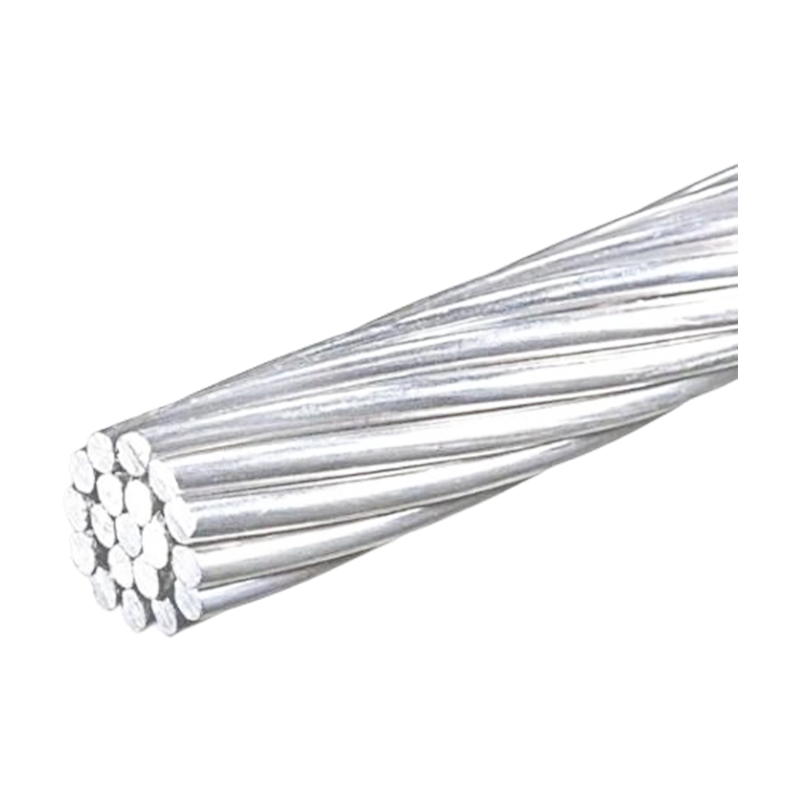
Reinforcing steel aluminum strand is a composite electrical conductor designed to combine the conductivity of aluminum with the mechanical strength of a steel core. This balanced construction makes it suitable for power transmission, distribution, grounding, shielding, and specialized hardware connection applications where electrical performance and structural reliability must work together.
For transmission infrastructure, the choice of conductor directly affects span length, tower spacing, line sag, installation tension, resistance, maintenance requirements, and long-term operating safety. An all-aluminum conductor may provide low weight and good conductivity, but it may not offer sufficient mechanical strength for demanding spans or severe weather conditions. A steel-reinforced aluminum strand addresses this limitation by placing high-strength steel wires at the center and conductive aluminum wires around the outside.
The product described in this article is manufactured according to the GB1179-83 standard and is available across a broad nominal cross-section range from 10/2 mm² to 240/30 mm². Depending on the design, the strand contains 6 to 30 aluminum wires surrounding 1 to 7 steel-core wires. Aluminum wire diameters range from 1.50 mm to 4.72 mm, while steel-core wire diameters range from 1.50 mm to 3.60 mm.
With calculated cross-sectional areas from 12.37 mm² to 275.96 mm², outer diameters from 4.50 mm to 21.60 mm, calculated tensile strength from 4,012 N to 91,120 N, and calculated weights from 42.9 kg/km to 964.2 kg/km, the product can be selected for different current-carrying and mechanical requirements. Depending on the specification, DC resistance is controlled within a range not exceeding 2.706 Ω/km to 0.1410 Ω/km.
Jiangsu Wopeng Power Technology Co., Ltd. applies its experience in busbar systems, tubular conductors, high-voltage equipment, and industrial power transmission to the development and supply of this type of conductor. The company’s manufacturing capabilities, engineering support, quality control procedures, and broad power equipment portfolio enable it to provide coordinated solutions for modern electrical infrastructure.
1. What Is Reinforcing Steel Aluminum Strand?
Reinforcing steel aluminum strand is a concentric stranded conductor consisting of aluminum strands placed around a steel core. The aluminum component performs most of the electrical conduction, while the steel core contributes tensile strength, dimensional stability, and resistance to mechanical loading.
This construction differs from a conductor made entirely of aluminum. Aluminum has excellent conductivity, low density, and strong resistance to atmospheric corrosion, but its mechanical strength is lower than that of steel. By combining both materials in a controlled stranded structure, the conductor achieves a practical compromise between electrical efficiency, weight, mechanical strength, and installation performance.
The outer aluminum layers are positioned where they can effectively carry current and protect the inner steel component from direct environmental exposure. The steel core is located near the neutral mechanical axis of the conductor, allowing it to support tensile loads while the aluminum layers remain available for current transmission.
The conductor may be used as an overhead line conductor, a ground wire, a shield wire, or a component in selected connection hardware. In the supplied product application, it is also identified as a damping wire for hardware connections such as damping-type end caps. This makes the product relevant not only to primary conductors but also to accessory and connection assemblies that require controlled mechanical and electrical properties.
Its performance depends on more than the nominal cross-sectional area. The number and diameter of aluminum and steel wires, the stranding pitch, the steel grade, the aluminum purity, the surface condition, the galvanizing quality, and the manufacturing tension all influence the final product. For this reason, standardized manufacturing and process control are essential.
Reinforcing Steel Aluminum Strand
2. Operating Principle of the Composite Structure
The aluminum wires in the outer layers provide the principal conductive path. Their high conductivity allows electrical current to travel along the conductor with comparatively low resistance. The aluminum also contributes corrosion resistance and keeps the total conductor weight lower than a conductor made from an equivalent amount of steel.
The steel core provides the main mechanical reinforcement. During installation and operation, the conductor may be exposed to tension from its own weight, wind, ice, temperature changes, and vibration. The core carries a substantial portion of the tensile load and helps reduce permanent elongation and excessive sag.
When a long span is required, conductor sag becomes a central design consideration. Excessive sag can reduce electrical clearances, increase the risk of contact with vegetation or structures, and create safety concerns beneath the line. The strengthened core allows the line to be installed at higher controlled tension and helps maintain a more stable geometry over long distances.
The concentric stranded arrangement also improves flexibility compared with a solid composite rod. Individual wires can accommodate bending during transportation, stringing, and connection work. At the same time, the controlled pitch of each layer prevents the wires from separating or moving excessively under normal operating loads.
Properly manufactured strands must maintain uniform contact and geometry throughout their length. Irregular wire diameter, unstable pitch, excessive pre-twist, or loose outer layers may create local stress concentrations and uneven current distribution. Jiangsu Wopeng Power Technology emphasizes standardized production and inspection processes to reduce these risks.
Electrical Function
The aluminum portion is selected for reliable current-carrying performance. The supplied technical information identifies electrical-grade aluminum with purity of at least 99.7 percent and conductivity exceeding 61 percent IACS after controlled annealing. These properties support efficient power transmission while helping the conductor meet standardized resistance requirements.
Although the steel core has lower conductivity than aluminum, the outer aluminum layers account for the principal conductive area. The final electrical resistance therefore depends on the total aluminum area, aluminum resistivity, strand configuration, contact conditions, temperature, and manufacturing consistency.
Under high-frequency conditions, current distribution can be influenced by skin effect and proximity effect. The supplied product information identifies a measured skin-effect coefficient below 1.05 and states that the increase in AC resistance is controlled within 8 percent. These characteristics may be relevant in systems where current harmonics or changing electrical loads must be considered.
Mechanical Function
The steel core carries the main tensile load and helps the conductor withstand installation tension, wind-induced movement, ice loading, and long-term suspension forces. The specified calculated tensile strength ranges from 4,012 N to 91,120 N, depending on the selected construction.
Mechanical performance is also affected by stranding pitch. A scientifically selected pitch ratio helps distribute stress between wires and layers. If the pitch is too short, the strand may become unnecessarily stiff and experience increased material consumption. If the pitch is too long, individual wires may become unstable or more likely to loosen. Controlled stranding is therefore important for both performance and service life.
3. Main Technical Specifications
The product range provides multiple conductor constructions for different electrical and mechanical conditions. Engineers can select the required size according to current capacity, span length, installation tension, line accessories, allowable sag, environmental loading, and connection requirements.
| Technical Parameter | Available or Typical Range | Engineering Significance |
|---|---|---|
| Applicable standard | GB1179-83 | Provides a standardized basis for construction and performance |
| Nominal cross-section | 10/2 mm² to 240/30 mm² | Supports different current and mechanical requirements |
| Aluminum wire count | 6 to 30 wires | Determines conductive area and outer configuration |
| Steel-core wire count | 1 to 7 wires | Determines reinforcement and tensile capacity |
| Aluminum wire diameter | 1.50 mm to 4.72 mm | Supports different strand designs |
| Steel-core wire diameter | 1.50 mm to 3.60 mm | Influences mechanical strength |
| Calculated area | 12.37 mm² to 275.96 mm² | Used for electrical and mechanical calculations |
| Outer diameter | 4.50 mm to 21.60 mm | Important for fittings, clearances, and aerodynamic behavior |
| Calculated tensile strength | 4,012 N to 91,120 N | Indicates resistance to mechanical loading |
| Calculated weight | 42.9 kg/km to 964.2 kg/km | Used for tower loading and installation planning |
| Typical delivery length | Generally less than 2,000 m | Supports handling, packaging, and project logistics |
The table represents the stated product range rather than a single fixed specification. Actual values depend on the selected nominal size, wire arrangement, material condition, and applicable order requirements. Before production, the purchaser should confirm the required current, span, installation tension, environmental loading, fitting compatibility, and acceptance criteria.
4. Advantages Compared with Conventional Conductors
High Strength-to-Weight Performance
One of the most important advantages of steel-reinforced aluminum strand is its high strength-to-weight balance. The steel core improves tensile performance without requiring the entire conductor to be made from heavy steel. The aluminum outer layers maintain a relatively low overall density while delivering useful conductivity.
Compared with an all-aluminum conductor of similar electrical function, the reinforced design offers greater resistance to mechanical loading and is better suited to long spans. Compared with a steel conductor, it provides a much more effective conductive outer layer and generally offers better resistance to atmospheric corrosion.
Longer Span Capability
Transmission and distribution lines often cross rivers, valleys, roads, railways, industrial zones, and other areas where tower construction is difficult or expensive. A higher-strength conductor can support longer spans and reduce the number of intermediate structures required.
Longer span capability does not eliminate the need for engineering calculations. Span length must still be evaluated together with temperature, wind, ice, terrain, tower strength, clearance requirements, vibration control, and local regulations. However, the steel core gives designers a broader range of technically feasible solutions.
Reduced Sag and Improved Stability
Line sag changes with conductor temperature and mechanical loading. When current increases, the conductor heats and expands, which can increase sag. Wind and ice also affect the line profile. The reinforced structure helps limit elongation and supports stable installation tension, reducing the risk of unacceptable clearance changes.
The supplied technical information states that creep deformation is limited to within 0.05 percent under long-term operating loads. Actual creep behavior depends on temperature, stress, material properties, and operating time, but the stated value demonstrates the importance placed on dimensional stability.
Good Corrosion Resistance
Aluminum naturally forms a protective oxide layer that helps resist atmospheric corrosion. The steel core is protected through the surrounding aluminum layers and, where specified, galvanized treatment. The supplied information identifies a zinc coating weight of at least 300 g/m² on the galvanized steel core.
This combination is valuable in industrial, coastal, and humid environments. Nevertheless, conductor selection must consider the specific atmosphere, pollution level, salt exposure, chemical emissions, and connection design. Good material resistance should be supported by suitable fittings, correct installation, and periodic inspection.
Broad Specification Coverage
The range from 10/2 mm² to 240/30 mm² allows the conductor to serve different electrical and mechanical duties. Smaller constructions may be appropriate for selected distribution, grounding, or accessory applications, while larger constructions can support higher current and stronger mechanical requirements.
A broad product range also makes it easier for a project supplier to coordinate conductors with fittings, tubular busbars, busway systems, substations, wind power equipment, and other power transmission products.
Standardized Technical Parameters
Standardized parameters simplify engineering calculations, purchasing, inspection, and replacement. Values such as calculated area, resistance, tensile strength, diameter, and weight allow designers to compare alternatives and select appropriate accessories.
Standardization also improves communication between manufacturers, contractors, utilities, and testing organizations. When the product is manufactured consistently, project teams can use established calculation methods rather than relying on uncertain or incomplete data.
5. Manufacturing Process and Quality Control
The performance of a composite stranded conductor depends heavily on the manufacturing process. Jiangsu Wopeng Power Technology uses controlled production methods intended to maintain material quality, dimensional consistency, structural stability, and traceability from incoming materials to finished products.
Material Preparation
The first stage is the inspection and preparation of aluminum wire and steel-core wire. Aluminum must meet the required purity and electrical performance criteria. Steel wire must provide the required tensile strength, dimensional accuracy, surface condition, and corrosion protection.
Incoming materials can be checked through documentation review, dimensional measurement, surface inspection, resistance testing, tensile testing, and coating verification where applicable. Material traceability helps link each production batch to its source and inspection record.
Controlled Aluminum Processing
Electrical-grade aluminum requires controlled drawing and annealing. Drawing reduces the wire to the required diameter and improves dimensional accuracy. Annealing adjusts the material condition and helps achieve the required balance between conductivity, flexibility, and mechanical performance.
Excessive drawing or unsuitable thermal treatment may reduce conductivity or create internal stress. For that reason, process parameters must be controlled according to the wire size, alloy or aluminum grade, and final conductor design.
Steel-Core Treatment
The steel core is prepared to provide the required mechanical reinforcement. Where galvanized steel is specified, the zinc coating must be continuous and sufficiently uniform. The stated minimum coating weight of 300 g/m² provides a reference for corrosion protection of the steel component.
Steel-core inspection may include diameter measurement, tensile testing, coating inspection, surface evaluation, and torsion or wrapping tests when required by the applicable specification. These checks help prevent weak sections, coating defects, and dimensional variation from entering the stranding process.
Concentric Stranding
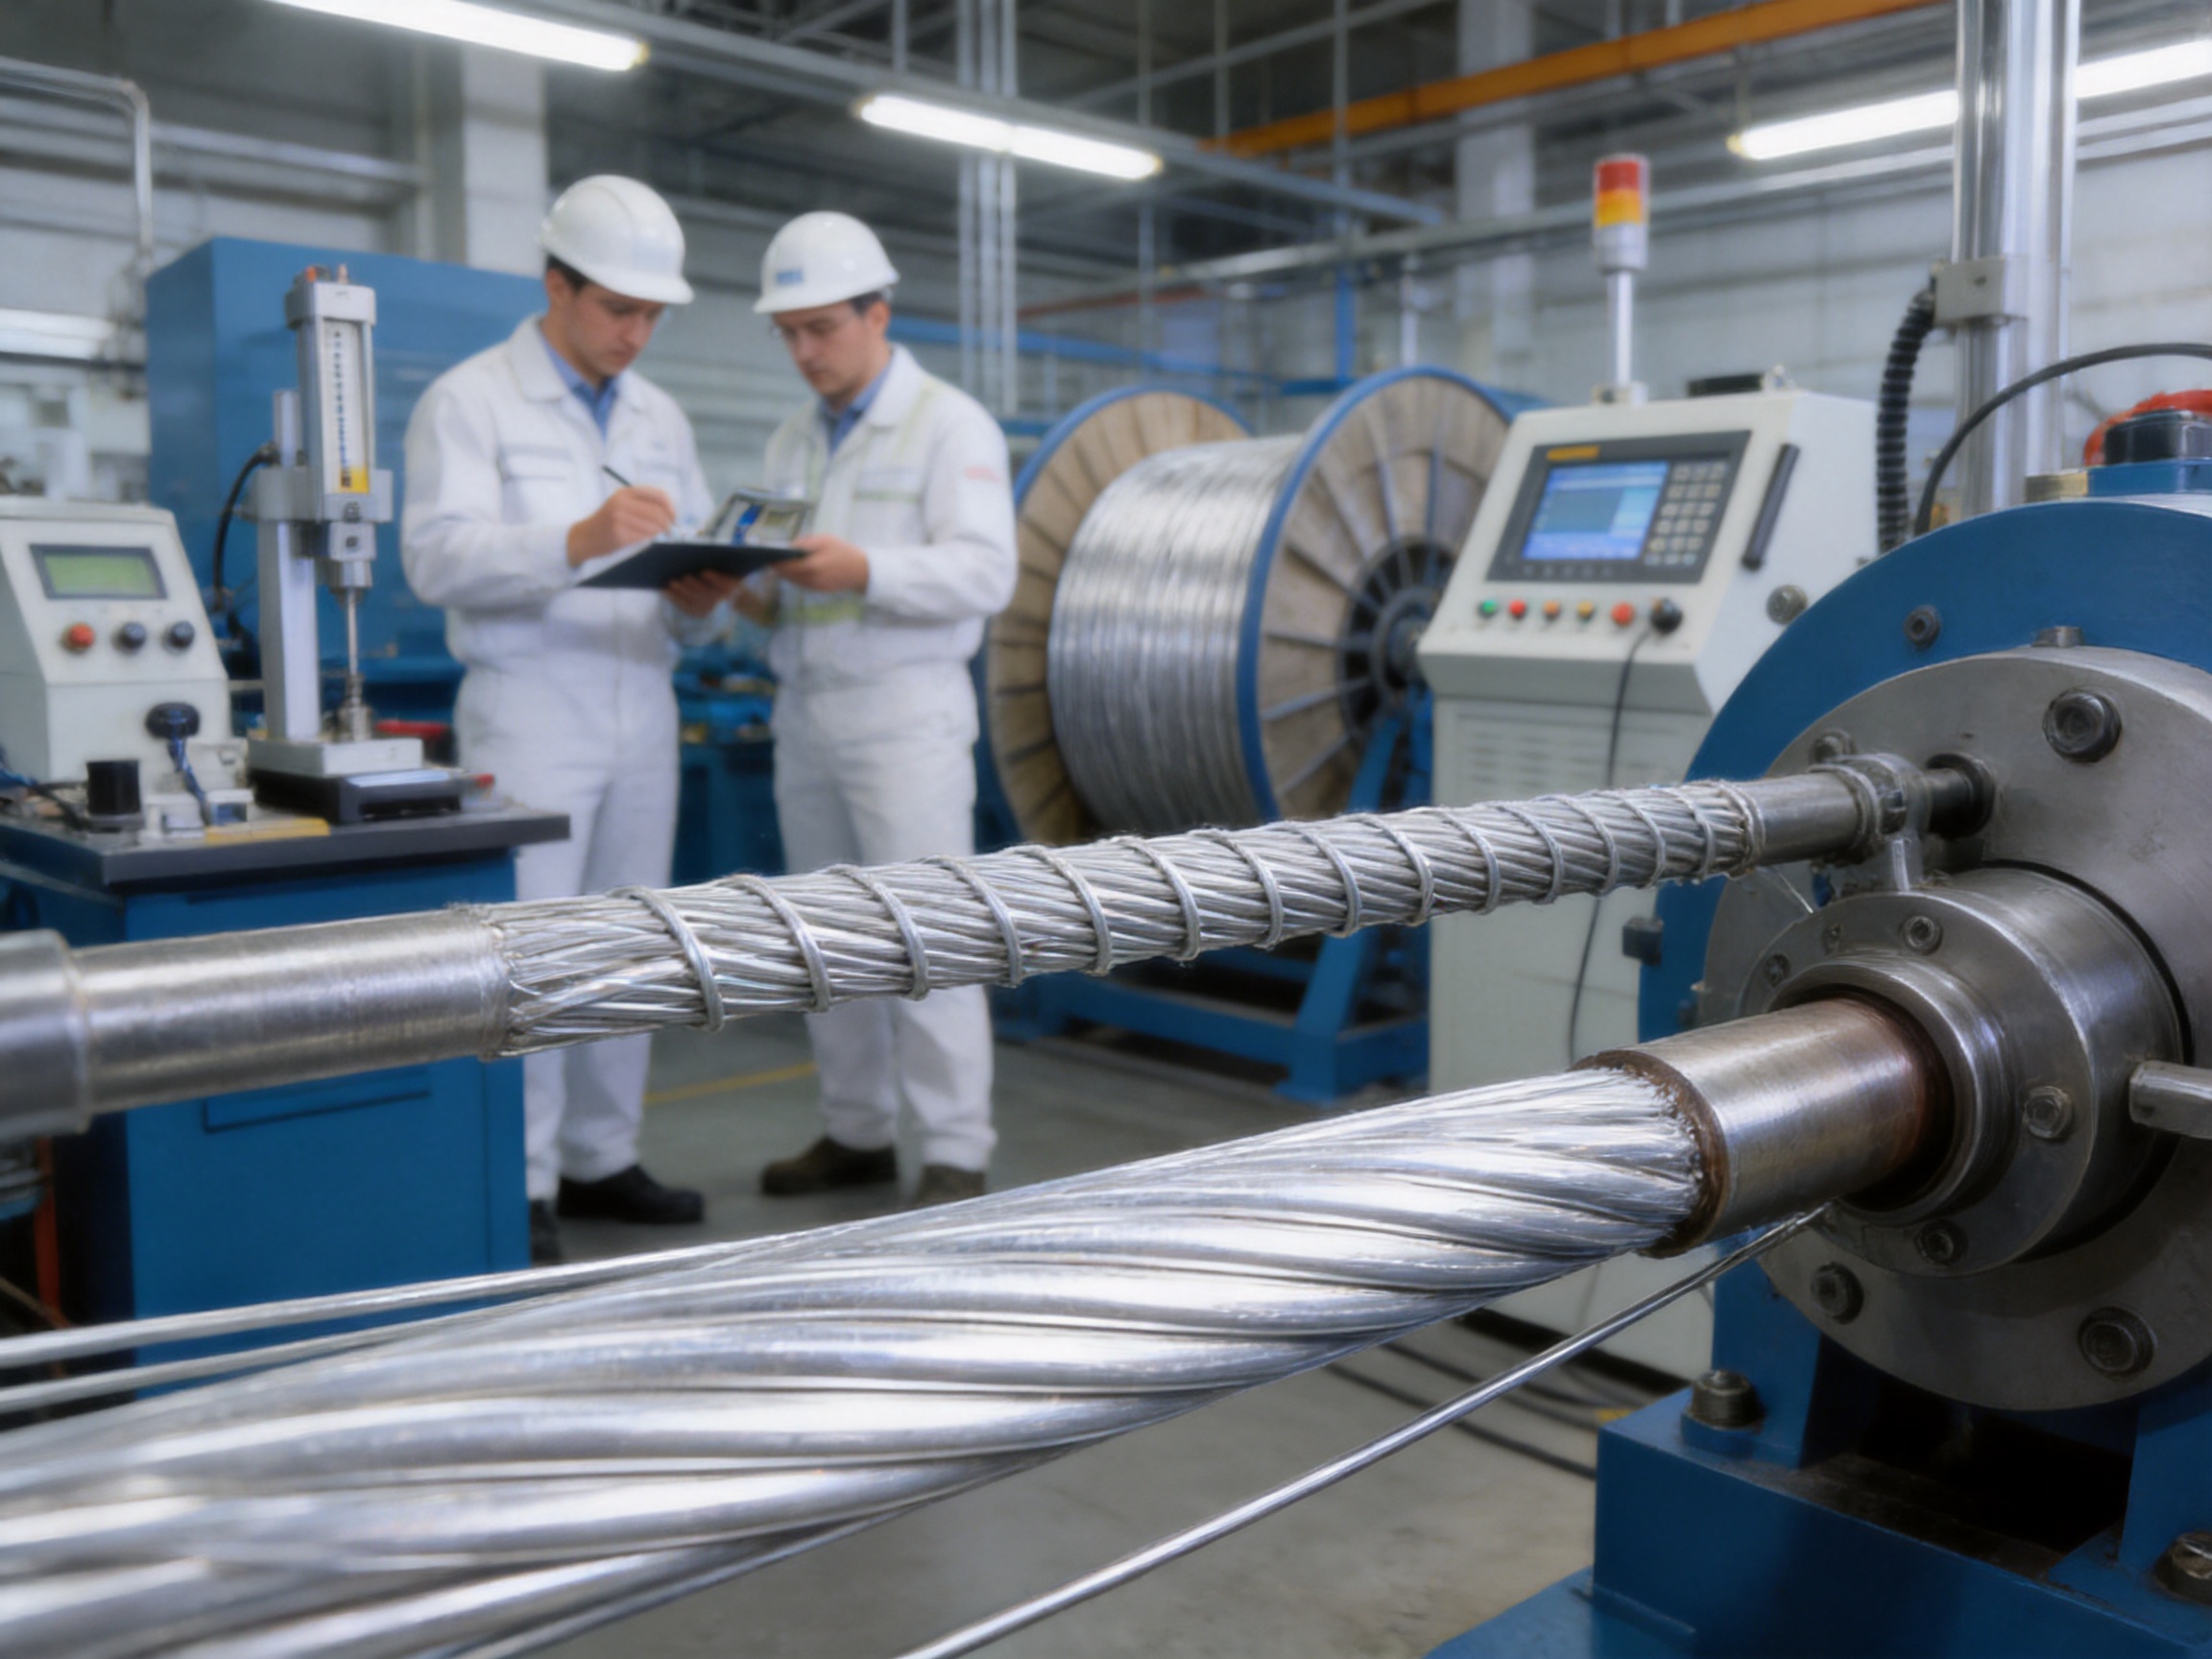
During stranding, aluminum wires are wrapped around the steel core in one or more controlled layers. The number of wires, wire diameter, lay direction, and pitch are selected according to the required conductor construction.
Modern stranding equipment helps maintain stable wire tension and consistent pitch. Balanced tension is important because excessive tension in one wire can create uneven load distribution, while insufficient tension can cause looseness or instability. The objective is to produce a compact, uniform conductor in which the wires remain properly positioned during handling and service.
Pre-Twisting and Stability Control
A controlled pre-twisting process helps prevent strand loosening after cutting, coiling, transportation, and installation. This is particularly important when the conductor is connected to fittings or when sections are exposed during termination.
The production team must control the relationship between stranding speed, wire tension, pitch, take-up tension, and reel winding. These parameters influence the final diameter, residual stress, flexibility, and dimensional stability of the product.
Dimensional and Electrical Inspection
Finished conductor inspection may include measurement of outer diameter, wire arrangement, pitch, calculated area, weight, DC resistance, surface condition, and delivery length. Measurements are compared with the applicable specification and purchase requirements.
Electrical inspection verifies that resistance remains within the specified limit. Mechanical inspection evaluates tensile strength and may include checks on wire continuity, lay stability, and core condition. Visual inspection is also important because surface damage, loose wires, corrosion, or abnormal gaps may affect installation and service reliability.
Packaging and Delivery
The product is generally delivered in lengths below 2,000 meters, depending on the order and project requirements. Appropriate reels or coils protect the conductor during handling and transportation. Packaging must prevent crushing, excessive bending, moisture intrusion, contamination, and damage to the aluminum surface.
Delivery planning is especially important for large infrastructure projects. Reel dimensions, lifting points, storage conditions, transportation route, and on-site pulling equipment should be coordinated before shipment.
6. Environmental and Mechanical Performance
Power conductors operate in changing outdoor conditions. Temperature variation, wind, rain, ice, sunlight, pollution, and salt spray can all influence service life. A reliable conductor must maintain its electrical and mechanical properties throughout these conditions.
Temperature Range
The supplied product information identifies performance validation from -40°C to +80°C. Within this range, the coefficient of thermal expansion is described as stable. Stable thermal behavior helps engineers predict sag and tension changes during seasonal and daily operating cycles.
Temperature performance should always be evaluated alongside the actual allowable operating temperature of the complete line system. Fittings, insulators, clamps, expansion components, and support structures may have different limits.
Wind and Vibration
Wind can create repeated oscillation and vibration in overhead conductors. Aeolian vibration, galloping, and sub-span oscillation may contribute to fatigue at clamps and connection points. The product information states that structural reliability was validated through a 2-million-cycle wind-induced vibration fatigue test.
Even when the conductor itself has good fatigue resistance, the complete system requires appropriate vibration control. Dampers, suitable clamps, correct tensioning, and adequate inspection are important for long-term performance.
Ice Loading
Ice accumulation increases conductor weight and aerodynamic loading. The stated product information identifies resistance to an ice coating load of 30 mm. Actual line design must consider local ice maps, span length, wind combined with ice, tower loading, and emergency conditions.
The steel core is particularly valuable under ice loading because it contributes tensile strength and helps limit excessive elongation. However, a higher-strength conductor does not remove the need to verify tower and foundation capacity.
Salt Spray and Ultraviolet Exposure
In coastal and industrial environments, salt and airborne pollutants can accelerate corrosion of exposed metal surfaces. The aluminum outer layer provides useful corrosion resistance, while the protected steel core is less directly exposed to the environment.
The supplied information reports that the conductor retained more than 95 percent of its tensile strength after 5,000 hours of salt-spray testing and showed no significant surface degradation after 5,000 hours of ultraviolet aging. Such results support use in demanding environments, subject to proper system-level design and maintenance.
7. Applications in Electrical Infrastructure
Overhead Transmission Lines
The most recognized application is overhead transmission. The conductor supports its own weight across spans between towers while carrying electrical current over long distances. The steel core permits higher mechanical performance than many all-aluminum alternatives.
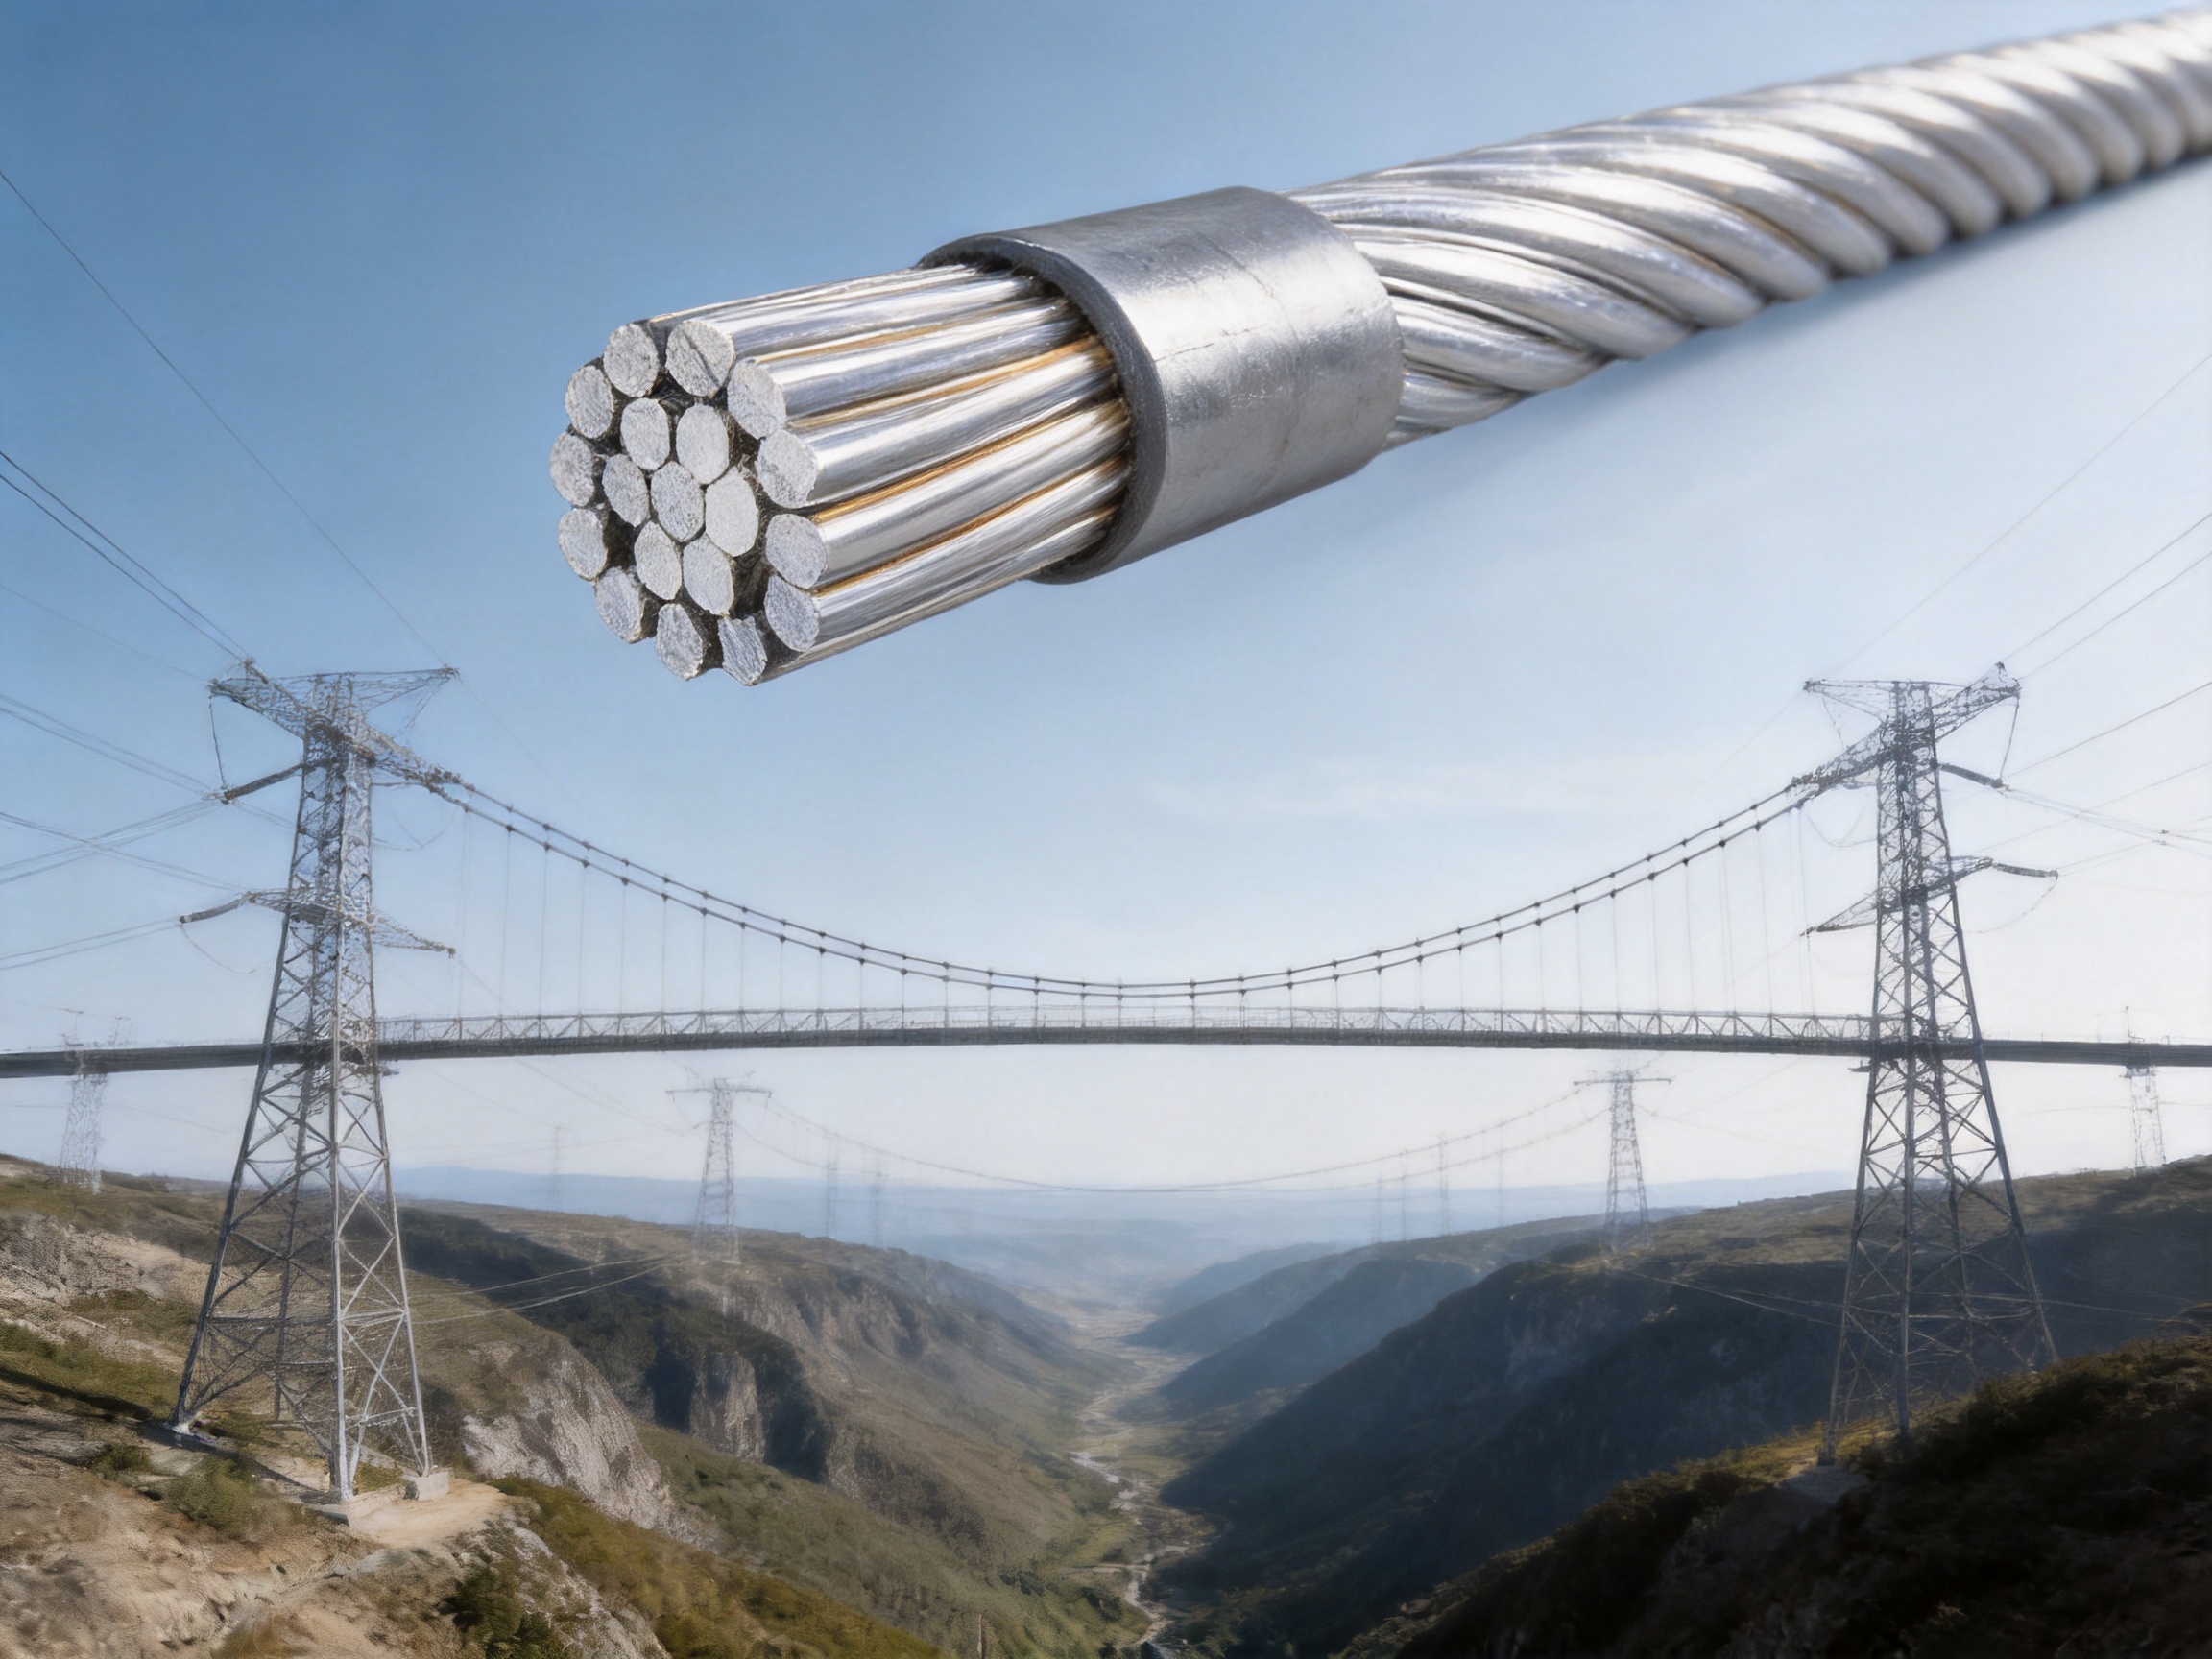
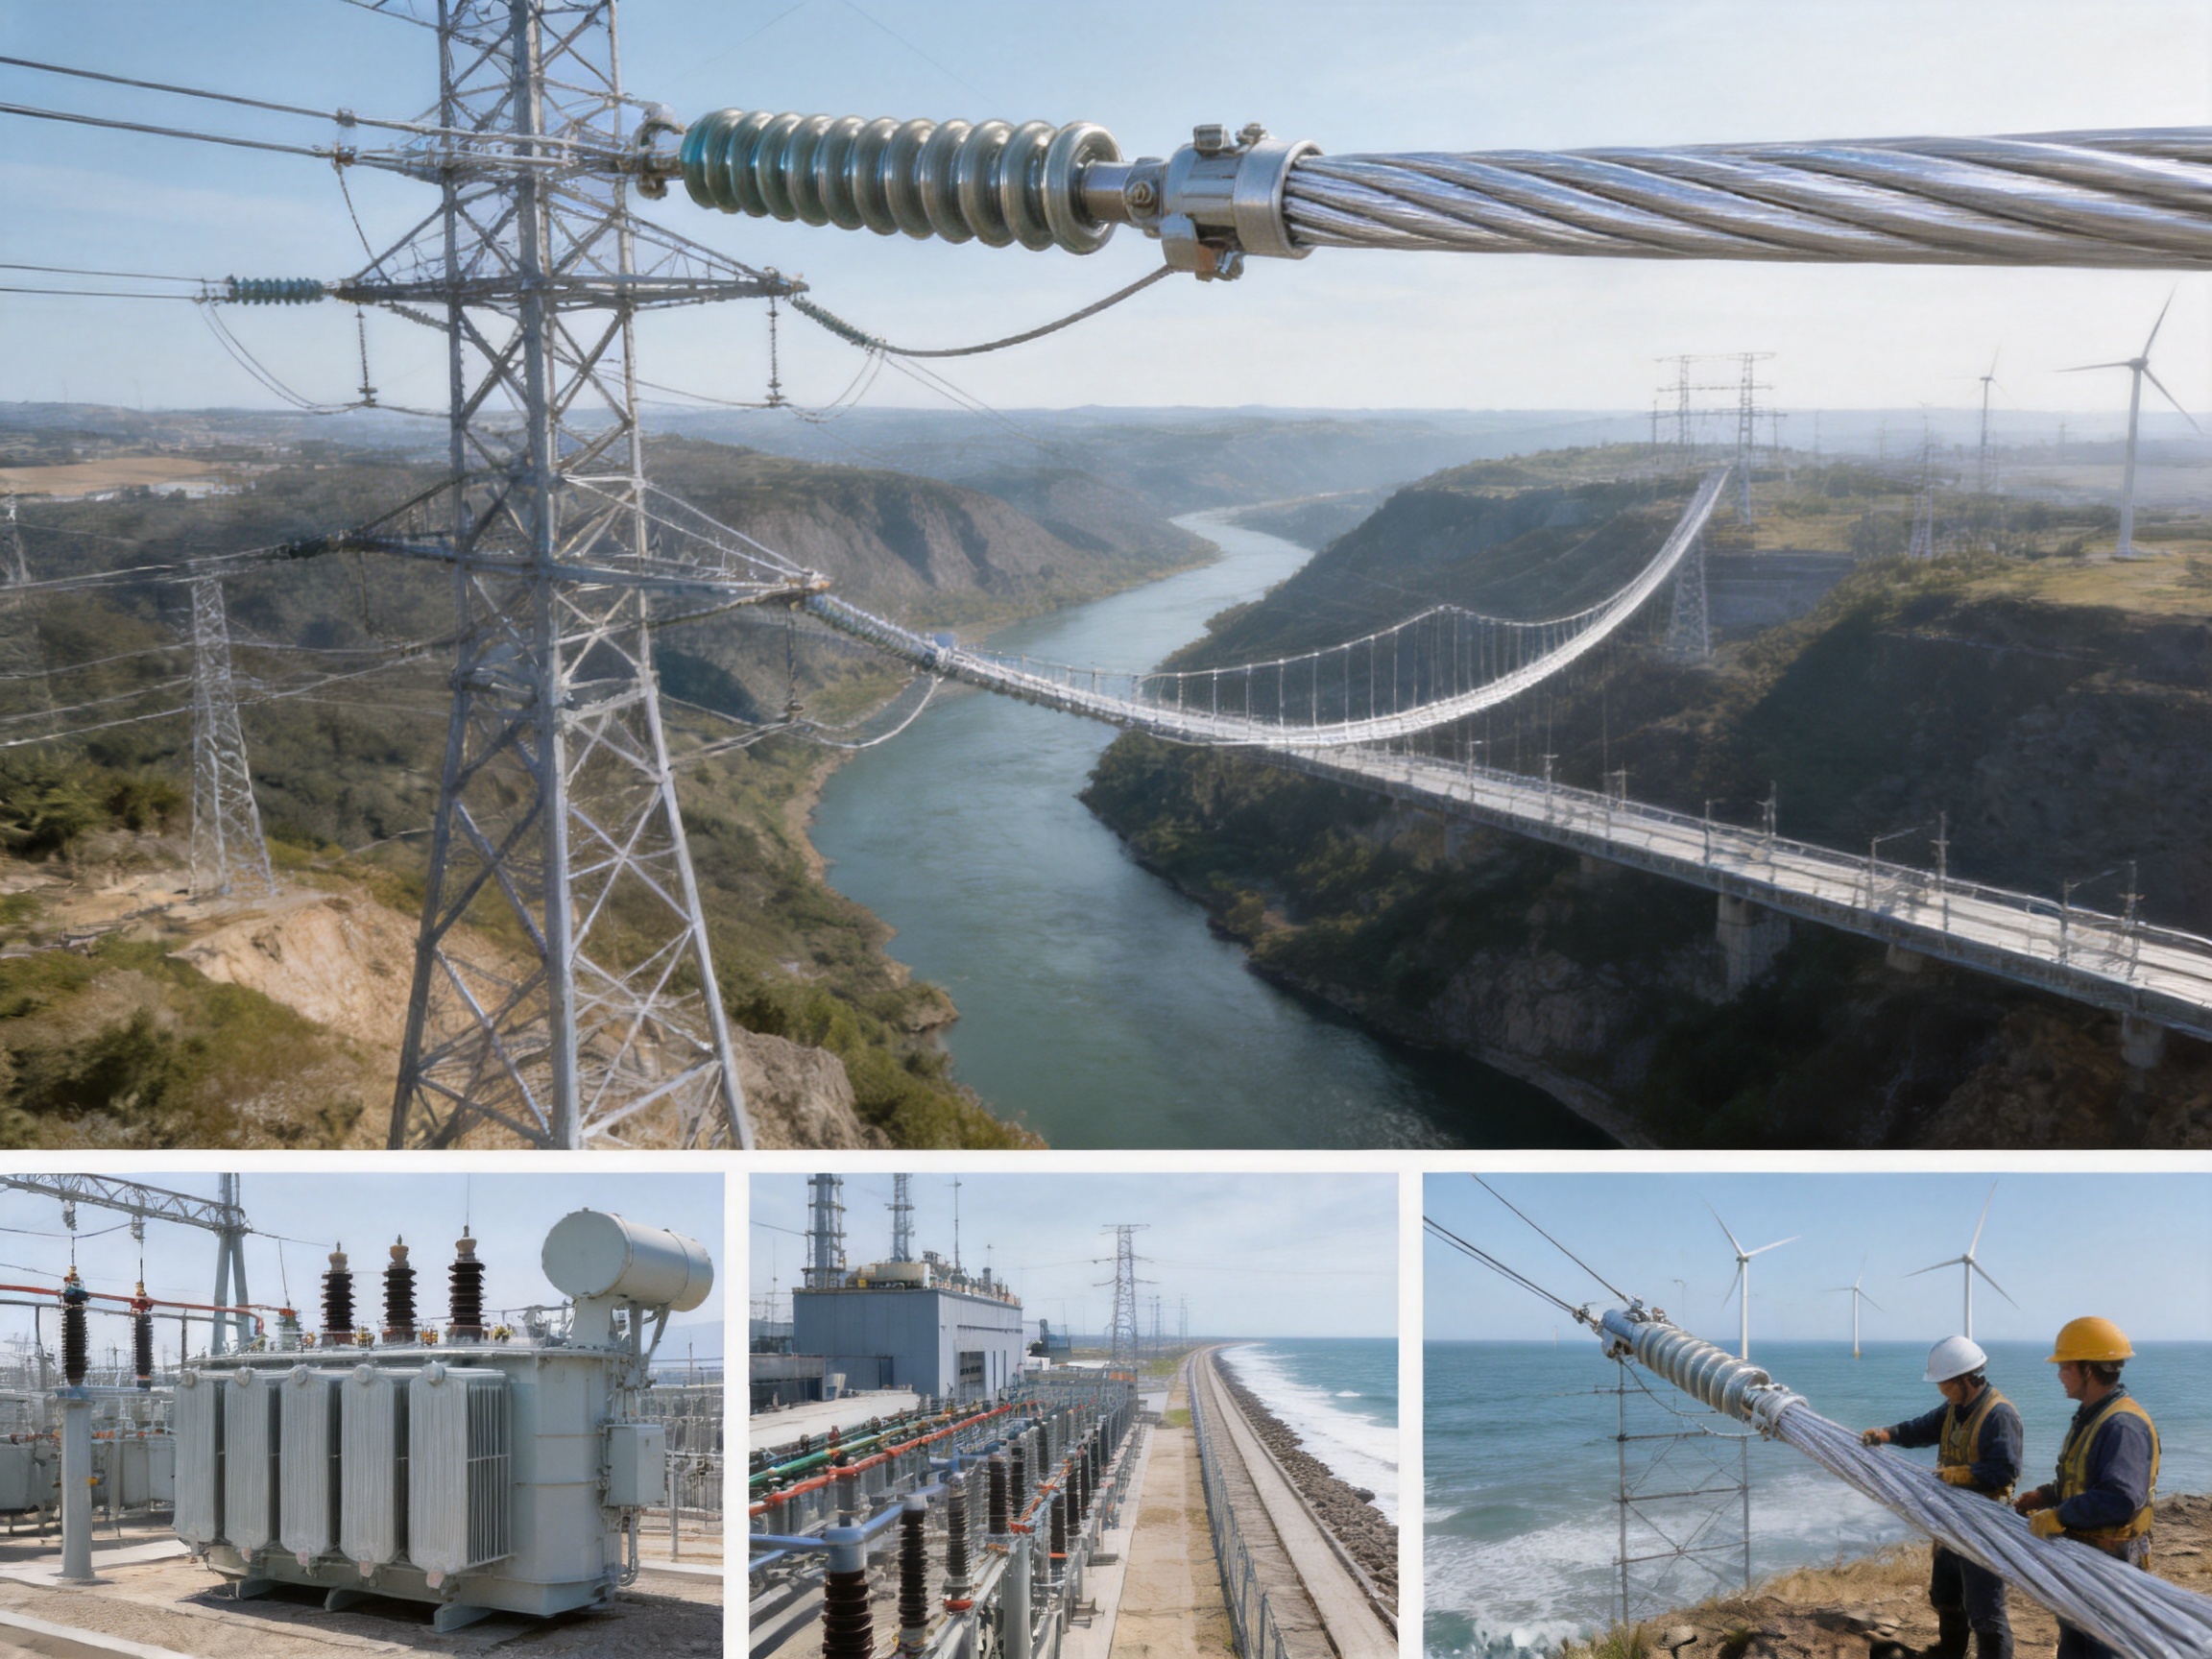
For river crossings, mountain routes, highways, railway corridors, and other difficult alignments, the increased strength may help reduce the number of support structures. Fewer towers can simplify construction and reduce the amount of land, foundation work, and access infrastructure required.
Distribution Networks
In high-tension distribution networks, reliable geometry and resistance to environmental loading are important. The strand can help maintain conductor clearance and reduce sagging under wind, temperature, and moderate ice conditions.
Its broad specification range allows utilities and contractors to select a suitable construction for feeder lines, regional distribution, industrial parks, and utility connections. Selection should be based on the required electrical load, fault conditions, span, and local design standards.
Ground Wires and Shield Wires
Steel-reinforced aluminum strand may be used as a ground wire or shield wire at the top of transmission towers. In this position, the conductor helps intercept lightning and provide a path toward the grounding system.
Grounding applications require consideration of short-circuit current, thermal capacity, tower bonding, grounding resistance, lightning performance, and mechanical strength. The supplied information identifies a short-circuit thermal capacity of 150 kA²·s, which may be useful as a reference for system calculations, subject to confirmation for the selected construction.
Substation and Industrial Connections
Selected constructions can be used in industrial power systems and substation connection assemblies where a combination of conductivity, mechanical reinforcement, and environmental durability is required. Correct connector design is essential, especially where aluminum conductor components transition to copper, steel, or aluminum alloy equipment.
Damping and Hardware Connections
The product is also intended for use as a damping wire in hardware connection applications, including damping-type end caps. In such applications, the strand may contribute controlled flexibility, mechanical reinforcement, and electrical continuity within an accessory assembly.
Connection hardware must be designed for the actual conductor diameter, material combination, mechanical load, and operating environment. A matching end cap, compression connector, clamp, or transition fitting helps prevent local resistance increases, oxidation, slippage, and premature fatigue.
Wind Power and Specialized Power Projects
Wind power projects often require reliable conductors and busbar systems in locations exposed to vibration, changing temperatures, and difficult installation conditions. Jiangsu Wopeng Power Technology supplies a broader range of power transmission products, including tubular busbars for wind turbines, which allows the company to support coordinated project requirements beyond a single conductor type.
8. Installation and Maintenance Recommendations
Correct installation protects the conductor from damage and ensures that its rated performance can be achieved. The installation team should review the product specification, reel instructions, stringing procedure, allowable tension, minimum bending radius, pulling equipment, and connector requirements before work begins.
Transportation and Storage
Reels should be lifted from designated points and should not be dropped, rolled uncontrolled, or dragged across rough surfaces. The conductor should be protected from sharp edges, standing water, corrosive chemicals, and contamination.
During storage, reels should remain stable and be supported on firm ground. If the conductor will be stored for an extended period, the packaging and surface should be inspected periodically for moisture, mechanical damage, or corrosion.
Tension Stringing
Tension stringing allows the conductor to be installed while maintaining separation from the ground and obstacles. Because the steel core supports higher mechanical tension, the method can be effective for long spans. However, the pulling tension must remain within the approved installation limits.
Excessive tension can cause permanent deformation, damage to wires, abnormal residual stress, or fitting problems. Stringing blocks must be correctly sized and aligned so that the conductor does not experience sharp bending or local pressure.
Connector Compatibility
Connectors must be compatible with the conductor construction and the materials being joined. Aluminum-to-steel transitions require particular attention because differences in material properties and electrochemical behavior can affect connection performance.
Compression connectors should be selected according to the conductor diameter, wire arrangement, tensile requirement, current rating, and applicable installation procedure. Contact surfaces must be clean and prepared as specified by the connector manufacturer.
Inspection During Service
Routine inspection should look for loose strands, surface damage, corrosion, unusual vibration marks, broken wires, clamp slippage, discoloration, and signs of overheating. Particular attention should be given to suspension points, dead ends, vibration dampers, jumpers, and transition fittings.
Inspection intervals should reflect the operating environment. Coastal areas, industrial pollution zones, high-wind regions, heavy-ice areas, and lines with frequent fault exposure may require more frequent examination.
9. Why Choose Jiangsu Wopeng Power Technology?
Jiangsu Wopeng Power Technology Co., Ltd. was founded in 2018 as a specialized high-tech enterprise focused on high- and low-voltage busbar systems and related power transmission equipment. Its product portfolio includes 35 kV epoxy resin vacuum-cast tubular busbars, low-voltage cast-resin busways, copper and aluminum tubular busbars, wind power tube busbars, compact busbar systems, and sliding contact line systems.
This product range gives the company a broader understanding of electrical infrastructure than a supplier focused only on one wire product. Conductors must operate as part of a complete system that may include busbars, connectors, insulators, switchgear, transformers, grounding components, and structural supports. Experience across these product categories helps engineers understand interface requirements and practical project constraints.
Engineering Capability
The company has a team of engineers, technical specialists, and production professionals with experience in power equipment technology. This supports technical communication during product selection, specification confirmation, drawing review, manufacturing, inspection, and delivery.
For customized projects, the engineering process can consider conductor dimensions, installation conditions, environmental loading, connection requirements, current levels, mechanical forces, and integration with other busbar or power transmission equipment.
Advanced Production Equipment
Wopeng operates production lines equipped with vacuum casting systems, CNC machining equipment, and automated assembly technologies. Although these technologies are commonly associated with busbar and insulation production, they also demonstrate the company’s ability to manage precision manufacturing, controlled process parameters, and repeatable assembly operations.
Precision equipment supports dimensional consistency and reduces variation between production batches. Automated or semi-automated operations can improve repeatability, while CNC machining helps produce accurate interfaces and fitting components.
Quality Management
Each product undergoes standardized inspection procedures that may include high-voltage tests, insulation tests, mechanical verification, and routine quality checks. Third-party testing collaboration provides additional independent validation for selected products and projects.
For reinforcing steel aluminum strand, relevant quality activities include verification of material certificates, conductor dimensions, resistance, tensile performance, strand stability, coating condition, delivery length, packaging, and visual appearance. Maintaining documented inspection records improves traceability and supports project acceptance.
Project Experience
Wopeng products operate in more than 17 provinces and across multiple industrial sectors. Its products serve power generation, substations, wind energy, industrial manufacturing, rail transit, and large commercial facilities.
This experience exposes the company to varied operating conditions, different design standards, demanding delivery schedules, and customized technical requirements. Such practical experience can help identify potential installation and integration issues before production begins.
OEM and Customized Solutions
The company provides tailored OEM solutions for customers with specific electrical, mechanical, dimensional, or installation requirements. Customization may involve conductor construction, product length, fitting interfaces, packaging, inspection documentation, labeling, and coordinated busbar system design.
Customization should be based on confirmed technical data rather than general product descriptions. Customers should provide information about voltage level, continuous current, short-circuit conditions, span, environmental loading, conductor supports, connection hardware, operating temperature, applicable standard, and required delivery schedule.
10. Comparison with Competing Conductor Designs
Different conductor types are appropriate for different projects. Reinforcing steel aluminum strand is not automatically the best choice for every application, but it offers a particularly strong balance when mechanical loading and long-span performance are important.
| Conductor Type | Main Strength | Potential Limitation | Typical Selection Consideration |
|---|---|---|---|
| Reinforcing steel aluminum strand | Balanced conductivity and tensile strength | Requires compatible fittings and careful installation | Long spans, overhead transmission, grounding, and demanding outdoor conditions |
| All-aluminum conductor | Low weight and good conductivity | Lower tensile strength | Shorter spans and applications with moderate mechanical loading |
| Steel conductor | High mechanical strength | Lower conductivity and greater corrosion concerns if unprotected | Special mechanical or grounding duties |
| Copper conductor | Very high conductivity | Higher material cost and weight | Compact high-current connections and specialized equipment |
| Insulated cable | Protection from direct contact and environmental exposure | Higher cost and different installation requirements | Urban, enclosed, underground, or contact-sensitive systems |
Compared with competing all-aluminum products, the steel-reinforced design offers greater mechanical support and improved long-span capability. Compared with steel-only products, it provides a more effective conductive surface and better aluminum-based corrosion resistance. Compared with copper, it can provide a lower-weight and potentially more economical solution where the complete system design permits aluminum conductors.
The final decision should consider lifecycle cost rather than purchase price alone. Tower quantity, foundation work, transport, installation tension, maintenance access, replacement frequency, connector costs, and outage risk can all influence the economic result.
11. Selection Guide for Engineers and Buyers
The first step is to determine the electrical duty. Required continuous current, emergency current, short-circuit duration, voltage level, permissible temperature, and expected load growth should be defined.
The second step is to determine the mechanical duty. This includes span length, conductor weight, installation tension, maximum sag, wind speed, ice thickness, vibration, tower geometry, and required safety factors.
The third step is to confirm the environment. Temperature range, salt spray, industrial pollution, ultraviolet exposure, altitude, humidity, rainfall, and chemical atmosphere may affect material and coating choices.
The fourth step is to verify compatibility with accessories. The selected conductor must match suspension clamps, tension clamps, dead-end fittings, damping devices, end caps, grounding components, and transition connectors.
The fifth step is to confirm the acceptance documentation. Buyers may require material certificates, dimensional inspection reports, resistance results, tensile test reports, coating records, factory inspection reports, packing lists, and certificates of conformity.
Customers should also confirm whether the project requires GB, IEC, ASTM, or another standard. The supplied product is described as conforming to GB1179-83, while some international projects may request additional or alternative standards. Any such requirement should be agreed before manufacturing.
12. Frequently Asked Questions
Q1: What is the main purpose of the steel core?
The steel core provides mechanical reinforcement. It helps the conductor withstand installation tension, wind, ice, vibration, and long-term suspension loads while limiting elongation and excessive sag.
Q2: Does the steel core carry electrical current?
The steel core may carry a limited portion of the current, but the aluminum outer layers provide the main conductive path. The electrical resistance of the finished conductor depends primarily on the aluminum area, material conductivity, conductor design, and operating temperature.
Q3: What is the available size range?
The stated nominal cross-section range is 10/2 mm² to 240/30 mm². The appropriate size depends on current capacity, tensile requirement, span, environmental loading, and compatible fittings.
Q4: Can the product be used for long transmission spans?
Yes. The reinforced construction is particularly suitable for applications where higher tensile strength and reduced sag are required. Long-span design must still verify tower loading, clearances, wind, ice, temperature, vibration, and installation tension.
Q5: Can it be used in coastal environments?
It can be considered for coastal and salt-spray environments because the aluminum outer layer provides useful corrosion resistance and the steel core can receive protective galvanizing. Site conditions, connector materials, pollution levels, and inspection requirements must be evaluated before selection.
Q6: What delivery length is normally available?
The general delivery length is less than 2,000 meters. Actual length depends on the selected construction, reel capacity, transportation conditions, and customer requirements.
Q7: What standards should buyers request?
The supplied product is identified as conforming to GB1179-83. International projects may also request IEC, ASTM, or utility-specific requirements. Buyers should specify the required standard and testing documentation during the quotation stage.
Q8: How should the conductor be installed?
Installation should use approved stringing equipment, suitable pulling tension, correctly sized blocks, and compatible compression or mechanical fittings. The conductor should not be dragged over sharp surfaces or bent below the permitted radius.
Q9: What fittings are recommended for aluminum-to-steel connections?
Compression connectors and transition fittings specifically designed for aluminum-to-steel conductor assemblies should be used. The fitting must match the conductor diameter, wire arrangement, tensile load, current rating, and applicable installation procedure.
Q10: How does the product compare with an all-aluminum conductor?
The reinforcing steel aluminum strand generally offers higher tensile strength, better long-span capability, and improved resistance to sagging. An all-aluminum conductor may be lighter and suitable for applications with lower mechanical demands, so the correct choice depends on the complete design.
Q11: What inspections are important after installation?
Inspection should examine connection points, clamps, dampers, end caps, conductor surfaces, broken or loose wires, corrosion, unusual vibration marks, overheating, and displacement. High-risk environments may require more frequent inspection and specialized testing.
Q12: Can the manufacturer provide customized solutions?
Yes. Jiangsu Wopeng Power Technology provides customized OEM solutions and can coordinate product requirements with broader busbar and power transmission projects. Customized production should be based on confirmed technical specifications and interface information.
13. Conclusion
Reinforcing steel aluminum strand is a practical solution for electrical systems that require both efficient current transmission and dependable mechanical reinforcement. Its aluminum outer layers provide conductivity and atmospheric corrosion resistance, while the steel core improves tensile strength, span capability, stability, and resistance to sagging.
The product range described here covers nominal constructions from 10/2 mm² to 240/30 mm² and includes multiple combinations of aluminum and steel wires. Standardized parameters for area, diameter, resistance, tensile strength, weight, and delivery length support engineering selection and project control.
Its advantages are strengthened by controlled aluminum processing, galvanized steel-core protection, precise concentric stranding, pre-twisting, dimensional inspection, electrical testing, mechanical verification, and organized delivery procedures. The product can serve overhead transmission lines, high-tension distribution, ground wires, shield wires, industrial connections, and damping-type hardware applications.
Jiangsu Wopeng Power Technology adds value through its broader expertise in high- and low-voltage busbar systems, tubular busbars, wind power equipment, cast-resin products, compact busbar systems, and sliding contact line systems. Its engineering team, production equipment, quality management system, OEM capability, and project experience support customers seeking reliable and coordinated power transmission solutions.
For the best result, product selection should be based on complete electrical, mechanical, environmental, installation, and interface data. When properly specified, manufactured, installed, and maintained, reinforcing steel aluminum strand can provide a durable and economical foundation for modern power transmission infrastructure.
References
GB1179-83, Aluminum Stranded Conductors and Steel-Reinforced Aluminum Stranded Conductors.
International Electrotechnical Commission, Overhead Electrical Conductors and Related Performance Considerations.
ASTM International, Standards for Aluminum and Aluminum-Alloy Conductors and Reinforced Conductors.
IEEE Engineering Practice, Overhead Transmission Line Design, Conductor Selection, and Mechanical Loading.
International Annealed Copper Standard, Reference Principles for Electrical Conductivity Measurement.
Manufacturer technical data for reinforcing steel aluminum strand, including construction, resistance, tensile strength, dimensions, delivery length, and environmental performance.
Jiangsu Wopeng Power Technology Co., Ltd., Product and Company Information for High- and Low-Voltage Busbar Systems and Power Transmission Equipment.
Product: Reinforcing Steel Aluminum Strand


-
 +86-180 3625 3000
-
 admin@wpbusbar.com
-
 No. 8, Yanjin Road, Chengxi Industrial Park, Shanyang Town, Baoying County, Yangzhou City, Jiangsu Province, China
Copyright © Jiangsu Wopeng Power Technology Co., Ltd.
All Rights Reserved.
 Custom Insulated Bus Bar Manufacturer
Tubular Busbar System Factory