

 EN

 English
 русский
 Français
 Español
 عربى
Reinforcing Steel Aluminum Strand: High-Strength Conductivity for Reliable Power Transmission
Content
- 1 1. Product Overview
- 2 2. How the Composite Structure Works
- 3 3. Technical Specifications
- 4 4. Electrical Performance
- 5 5. Mechanical Performance and Long-Span Capability
- 6 6. Environmental Adaptability
- 7 7. Advantages Compared with Standard All-Aluminum Conductors
- 8 8. Primary Applications
- 9 9. Manufacturing Process and Quality Control
- 10 10. Engineering and Manufacturing Strengths
- 11 11. Installation Recommendations
- 12 12. Maintenance and Service-Life Considerations
- 13 13. Selection Guide for Engineers and Buyers
- 14 14. Safety and Reliability Benefits
- 15 15. Frequently Asked Questions
- 15.1 Q1: What is reinforcing steel aluminum strand?
- 15.2 Q2: What standard does this product follow?
- 15.3 Q3: What sizes are available?
- 15.4 Q4: Why is steel added to an aluminum conductor?
- 15.5 Q5: Does the steel core carry electrical current?
- 15.6 Q6: Is the product suitable for long-span transmission lines?
- 15.7 Q7: Can it be used in coastal environments?
- 15.8 Q8: What connectors should be used?
- 15.9 Q9: Can the conductor be used as a ground wire or shield wire?
- 15.10 Q10: What delivery length is normally available?
- 15.11 Q11: What quality checks are important before shipment?
- 15.12 Q12: Why choose a supplier with busbar manufacturing experience?
- 16 16. Conclusion
- 17 References
- 18 Product: Reinforcing Steel Aluminum Strand
Reinforcing steel aluminum strand is a composite conductor engineered to combine the electrical conductivity of aluminum with the mechanical strength of a galvanized steel core. This structure enables the conductor to carry electrical current while supporting substantial tensile loads, making it suitable for overhead transmission lines, high-tension distribution systems, grounding wires, shield wires, and specialized hardware connection applications.
Unlike an all-aluminum conductor, which prioritizes low weight and conductivity but has limited mechanical strength, a steel-reinforced aluminum strand is designed for demanding spans and difficult operating conditions. The aluminum strands form the conductive outer layers, while the steel core resists tension, wind loading, ice loading, vibration, and installation stress. The result is a balanced conductor solution for projects where electrical performance and structural reliability are equally important.
Manufactured according to the GB1179-83 standard, the product is available in nominal cross-sectional combinations from 10/2 mm² to 240/30 mm². Depending on the model, the conductor may contain 6 to 30 aluminum strands surrounding 1 to 7 steel-core strands. This broad specification range allows engineers to select a conductor according to current capacity, span length, mechanical loading, allowable sag, installation conditions, and system voltage.
Jiangsu Wopeng Power Technology Co., Ltd. supplies power transmission and busbar products for demanding electrical infrastructure. Its manufacturing capabilities, engineering experience, quality-control procedures, and product range support the development of reliable conductor and busbar solutions for substations, power generation facilities, wind-energy projects, industrial plants, rail transit systems, and commercial infrastructure.
Reinforcing Steel Aluminum Strand
1. Product Overview
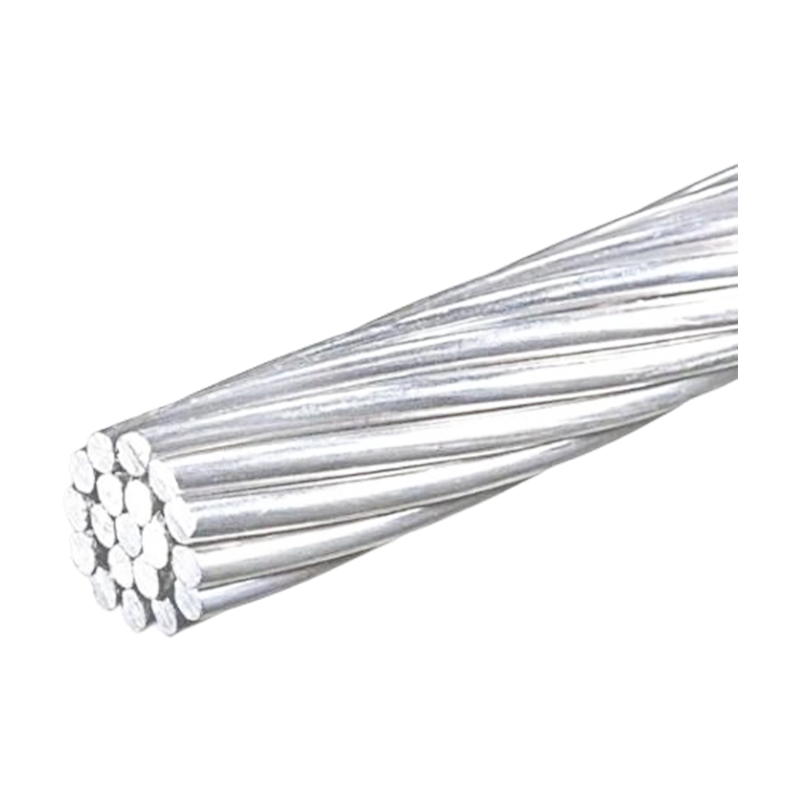
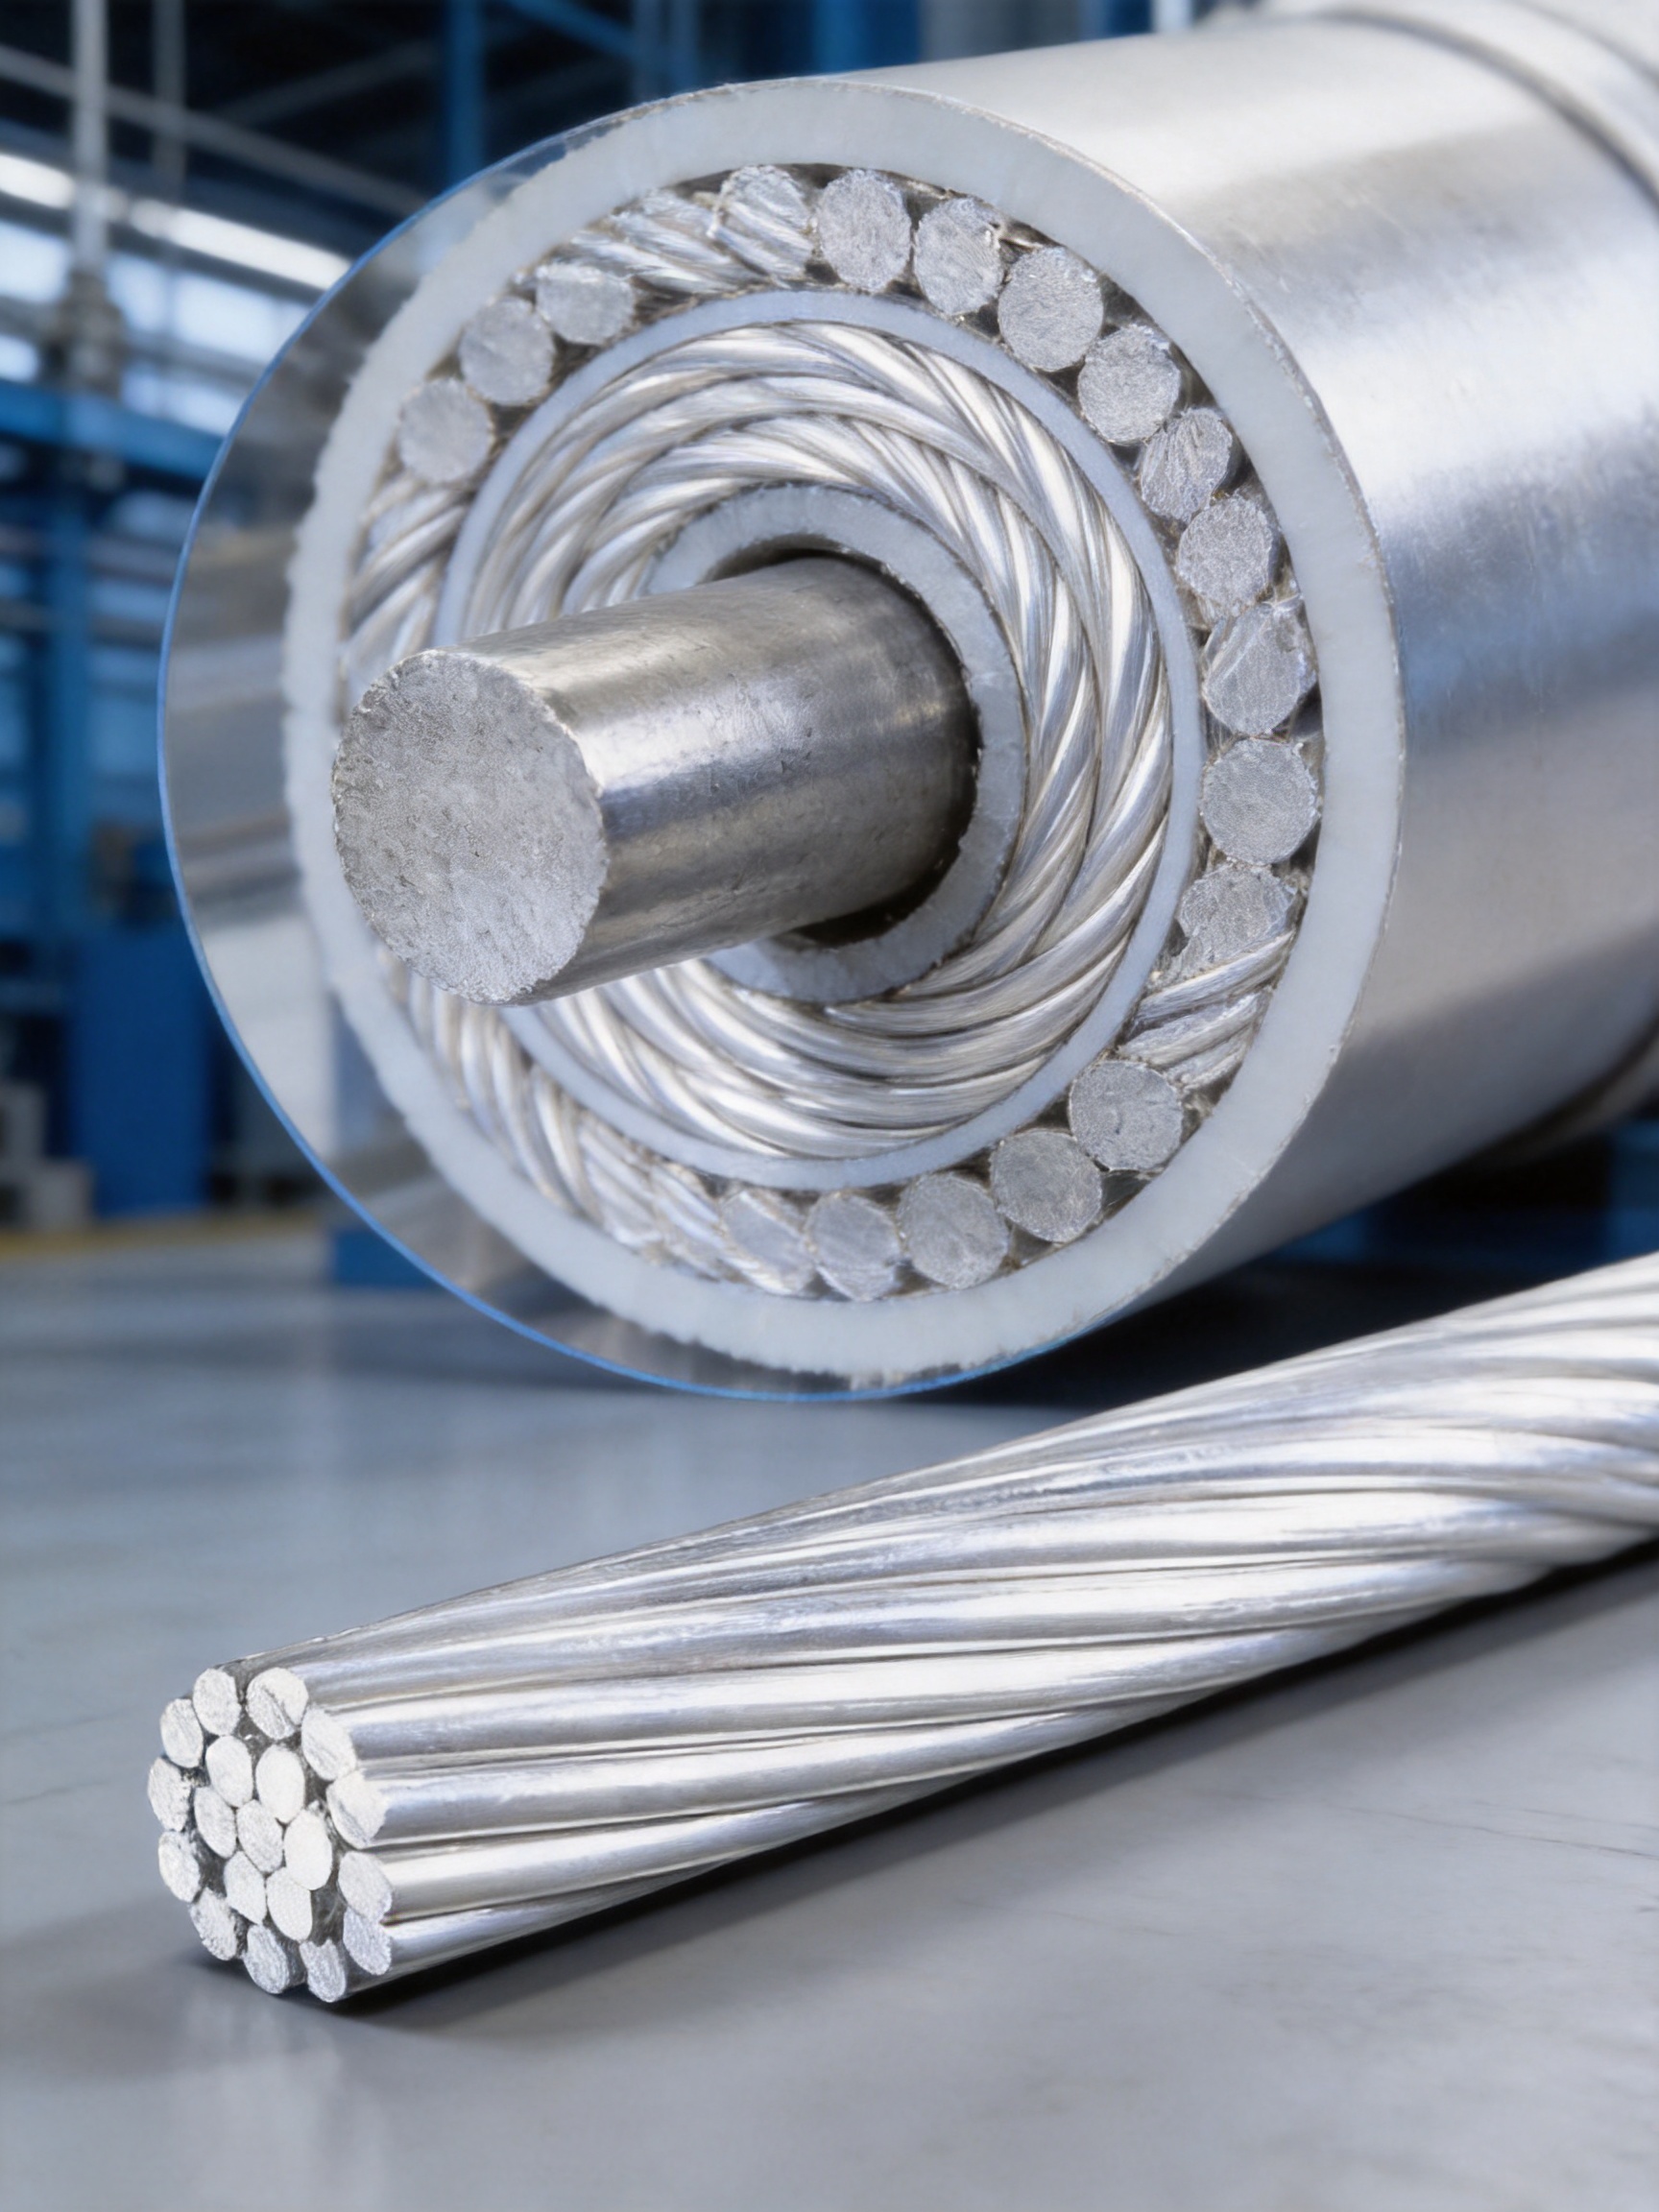
Reinforcing steel aluminum strand is commonly understood as a steel-reinforced aluminum conductor formed by concentrically stranding aluminum wires around a steel core. The product is sometimes described as a steel-cored aluminum strand because its construction gives the conductor two clearly differentiated functions: aluminum handles most of the current transmission, and steel provides mechanical reinforcement.
The product supplied under this specification conforms to the GB1179-83 standard. Standardized production is important because conductors must interface with suspension fittings, tension fittings, compression connectors, damping devices, end caps, grounding hardware, and other accessories. A defined construction ensures that the conductor diameter, wire count, cross-sectional area, tensile strength, resistance, and weight remain within a predictable technical range.
The nominal designation combines the aluminum and steel cross-sectional areas. For example, a designation expressed as 10/2 mm² indicates an aluminum component with a nominal area of approximately 10 mm² and a steel component with a nominal area of approximately 2 mm². Larger designations, such as 240/30 mm², provide significantly greater current-carrying capacity and tensile performance for more demanding transmission applications.
The aluminum strands use electrical-grade aluminum with a stated purity of at least 99.7 percent. With suitable drawing and annealing control, the aluminum achieves conductivity above 61 percent IACS under the described manufacturing requirements. The steel core is galvanized, and the zinc coating weight is controlled according to the stated requirement of at least 300 g/m². The coating helps protect the steel from atmospheric corrosion and supports long-term structural performance.
The conductor is manufactured in concentric layers. The steel core is positioned at the center, and aluminum strands are wrapped around it according to a controlled stranding pattern. The number of aluminum strands ranges from 6 to 30, while the steel core may contain from 1 to 7 individual steel strands. Aluminum wire diameters range from approximately 1.50 mm to 4.72 mm, and steel-core wire diameters range from approximately 1.50 mm to 3.60 mm.
The product’s calculated cross-sectional area ranges from 12.37 mm² to 275.96 mm². Outer diameters range from approximately 4.50 mm to 21.60 mm. Depending on the selected construction, direct-current resistance is controlled within the stated range of no more than 2.706 Ω/km to 0.1410 Ω/km. Calculated tensile strength ranges from approximately 4,012 N to 91,120 N, while calculated weight ranges from 42.9 kg/km to 964.2 kg/km.
Delivery lengths are generally less than 2,000 meters. This format supports manageable transportation, storage, installation planning, and quality inspection. Specific delivery arrangements can be evaluated according to project requirements, conductor size, packaging method, and installation schedule.
2. How the Composite Structure Works
The main advantage of a steel-reinforced aluminum strand comes from the division of responsibilities between its two materials. Aluminum is widely used in electrical conductors because it offers good electrical conductivity at a lower density than copper. Steel, by contrast, has much higher tensile strength and greater resistance to mechanical deformation. By combining the two, the conductor can achieve a useful balance between electrical transmission and structural support.
2.1 Aluminum Conductive Layers
The outer aluminum strands form the primary conductive path. Their high conductivity allows the conductor to transmit electrical power with controlled resistance. Aluminum also offers useful resistance to atmospheric corrosion because it naturally forms a protective oxide film when exposed to air.
The aluminum strands are drawn to controlled diameters before stranding. Accurate diameter control is essential because variations can affect the finished outer diameter, contact between layers, resistance, tensile distribution, connector compatibility, and installation behavior. Annealing is also controlled to produce the required combination of conductivity, flexibility, and mechanical properties.
2.2 Galvanized Steel Core
The steel core is the mechanical reinforcement element. It supports a significant portion of the tensile load during installation and operation. This is particularly important for long spans between towers, high wind zones, regions with heavy ice, and installations where conductor sag must be carefully controlled.
Galvanizing adds a protective zinc layer to the steel. The zinc coating acts as a barrier against moisture and provides sacrificial protection if the surface is damaged. Consistent coating weight is important because localized corrosion of the core could reduce the mechanical strength of the entire conductor.
2.3 Concentric Stranding
Concentric stranding creates a balanced cylindrical conductor. The wires are arranged in layers with controlled pitch ratios. This construction allows the strands to share load and follow the conductor’s curvature during handling, tensioning, and service.
A controlled pre-twisting process helps prevent strand loosening. It also supports dimensional stability when the conductor is unwound, tensioned, clamped, or subjected to wind-induced vibration. Correct pitch design reduces the possibility of uneven stress concentration between the inner and outer layers.
3. Technical Specifications
The available specification range allows the product to serve both relatively compact conductor requirements and higher-capacity transmission applications. Engineers can select the appropriate size based on electrical load, mechanical span, environmental loading, allowable temperature, voltage level, fittings, and installation method.
| Technical Item | Stated Range or Requirement | Engineering Significance |
|---|---|---|
| Applicable standard | GB1179-83 | Provides standardized construction and performance requirements |
| Nominal cross-sectional combinations | 10/2 mm² to 240/30 mm² | Supports a broad range of current and mechanical requirements |
| Number of aluminum strands | 6 to 30 | Determines conductive area and outer-layer construction |
| Number of steel-core strands | 1 to 7 | Determines mechanical reinforcement configuration |
| Aluminum wire diameter | Approximately 1.50 mm to 4.72 mm | Supports different conductor sizes and stranding patterns |
| Steel wire diameter | Approximately 1.50 mm to 3.60 mm | Provides design flexibility for tensile performance |
| Calculated cross-sectional area | Approximately 12.37 mm² to 275.96 mm² | Helps engineers calculate current capacity and system losses |
| Outer diameter | Approximately 4.50 mm to 21.60 mm | Supports fitting selection and clearance calculations |
| Calculated tensile strength | Approximately 4,012 N to 91,120 N | Supports span, sag, and installation-load calculations |
| Calculated weight | Approximately 42.9 kg/km to 964.2 kg/km | Supports tower loading and transportation planning |
| Typical delivery length | Generally less than 2,000 meters | Facilitates handling, packaging, and construction control |
When selecting a model, technical personnel should not rely on cross-sectional area alone. The required conductor must also satisfy current-carrying capacity, short-circuit performance, tensile strength, span length, environmental loading, connector compatibility, and permissible sag. The selected specification should be verified against the complete system design and the applicable project standards.
4. Electrical Performance
The principal electrical function of the product is to provide a stable conductive path through the aluminum layers. The steel core contributes comparatively less to current transmission, but the majority of the conductor’s effective conductive area is aluminum. The conductor therefore maintains useful electrical performance while gaining a higher strength-to-weight ratio than many all-aluminum alternatives.
Direct-current resistance is one of the key selection parameters. Lower resistance reduces I²R losses and helps improve transmission efficiency. The stated resistance range extends from no more than approximately 2.706 Ω/km for smaller constructions to approximately 0.1410 Ω/km for larger constructions. Actual system performance depends on conductor size, operating temperature, installation configuration, current level, and connection quality.
Under high-frequency conditions, the described skin-effect coefficient is below 1.05. The increase in alternating-current resistance is controlled within 8 percent under the stated performance conditions. These characteristics are important in power systems where current distribution, harmonic content, transient behavior, or specialized electrical equipment must be considered.
The stated short-circuit thermal capacity reaches 150 kA²·s. This parameter is relevant to the conductor’s ability to withstand the thermal stress associated with short-circuit current for a defined duration. Protection settings, fault levels, conductor size, installation conditions, and system grounding design must still be evaluated by the project engineer.
After 100 thermal cycles, the stated conductivity degradation does not exceed 2 percent. Thermal cycling performance is significant because conductors may repeatedly heat and cool as load changes. Stable electrical properties help reduce the risk of unexpected resistance growth and support predictable long-term operation.
4.1 Current-Carrying Considerations
Current-carrying capacity is affected by conductor size, ambient temperature, solar radiation, wind speed, installation height, conductor spacing, surface condition, and permissible operating temperature. The aluminum area is the primary factor in determining continuous current capacity, while the steel core is primarily responsible for mechanical reinforcement.
For practical design, engineers should calculate the required current capacity using the project’s environmental conditions rather than applying a general value. In parallel-conductor systems, current sharing must also be considered. Proper connector installation and clean contact surfaces are essential because a poorly installed connection can create a localized hot spot even when the conductor itself has adequate capacity.
5. Mechanical Performance and Long-Span Capability
Mechanical strength is the defining advantage of the steel-reinforced construction. In overhead lines, the conductor must support its own weight across a span while resisting wind, ice, vibration, and installation tension. Excessive sag may reduce electrical clearances, while excessive tension may increase loads on towers, insulators, and fittings.
The steel core allows the conductor to withstand higher tensile forces than a comparable all-aluminum conductor. This can support longer spans, reduce sag, and improve stability in areas where environmental forces are severe. In suitable projects, longer spans may reduce the number of support towers, foundations, and associated construction activities.
Mechanical performance is not determined by tensile strength alone. The stranding pitch, pre-twist, wire surface quality, steel coating, aluminum temper, connector design, and installation procedure also influence reliability. A well-controlled composite structure distributes stress across the conductor and reduces the risk of local strand displacement.
5.1 Wind and Vibration Resistance
Overhead conductors may experience repeated oscillation caused by wind. Aeolian vibration, galloping, and other movement modes can produce fatigue at clamps, fittings, and conductor strands. The product’s controlled stranding design and stated validation through a 2-million-cycle wind-induced vibration fatigue test support its use in applications where vibration endurance is important.
Damping devices may be installed to reduce vibration amplitude. The product is also described as suitable for use as a damping wire in hardware connection applications, including damping-type end caps. In such applications, the correct wire construction and compatibility with the hardware are important for maintaining mechanical and electrical integrity.
5.2 Creep and Sag Stability
Long-term conductor sag can increase through material creep and permanent deformation. The described product limits creep deformation to within 0.05 percent under the stated conditions. This contributes to stable clearances and predictable line geometry throughout the service life.
Actual sag is influenced by conductor temperature, span length, initial tension, tower height, wind, ice, and installation conditions. A project-specific sag-tension calculation remains necessary. The conductor’s mechanical data should be provided to the design team so that tower and foundation loads can be accurately determined.
6. Environmental Adaptability
Power transmission equipment must operate through seasonal temperature changes, moisture, ultraviolet exposure, pollution, wind, and occasional ice. The steel-reinforced aluminum strand is designed for a broad stated operating temperature range from -40°C to +80°C. Within this range, the coefficient of thermal expansion is described as stable.
The aluminum outer layer provides useful resistance to atmospheric exposure and salt contamination. The galvanized steel core is protected by its zinc coating. Together, these materials create a conductor suited to many inland, industrial, coastal, and high-exposure environments, provided that the product is selected and installed correctly.
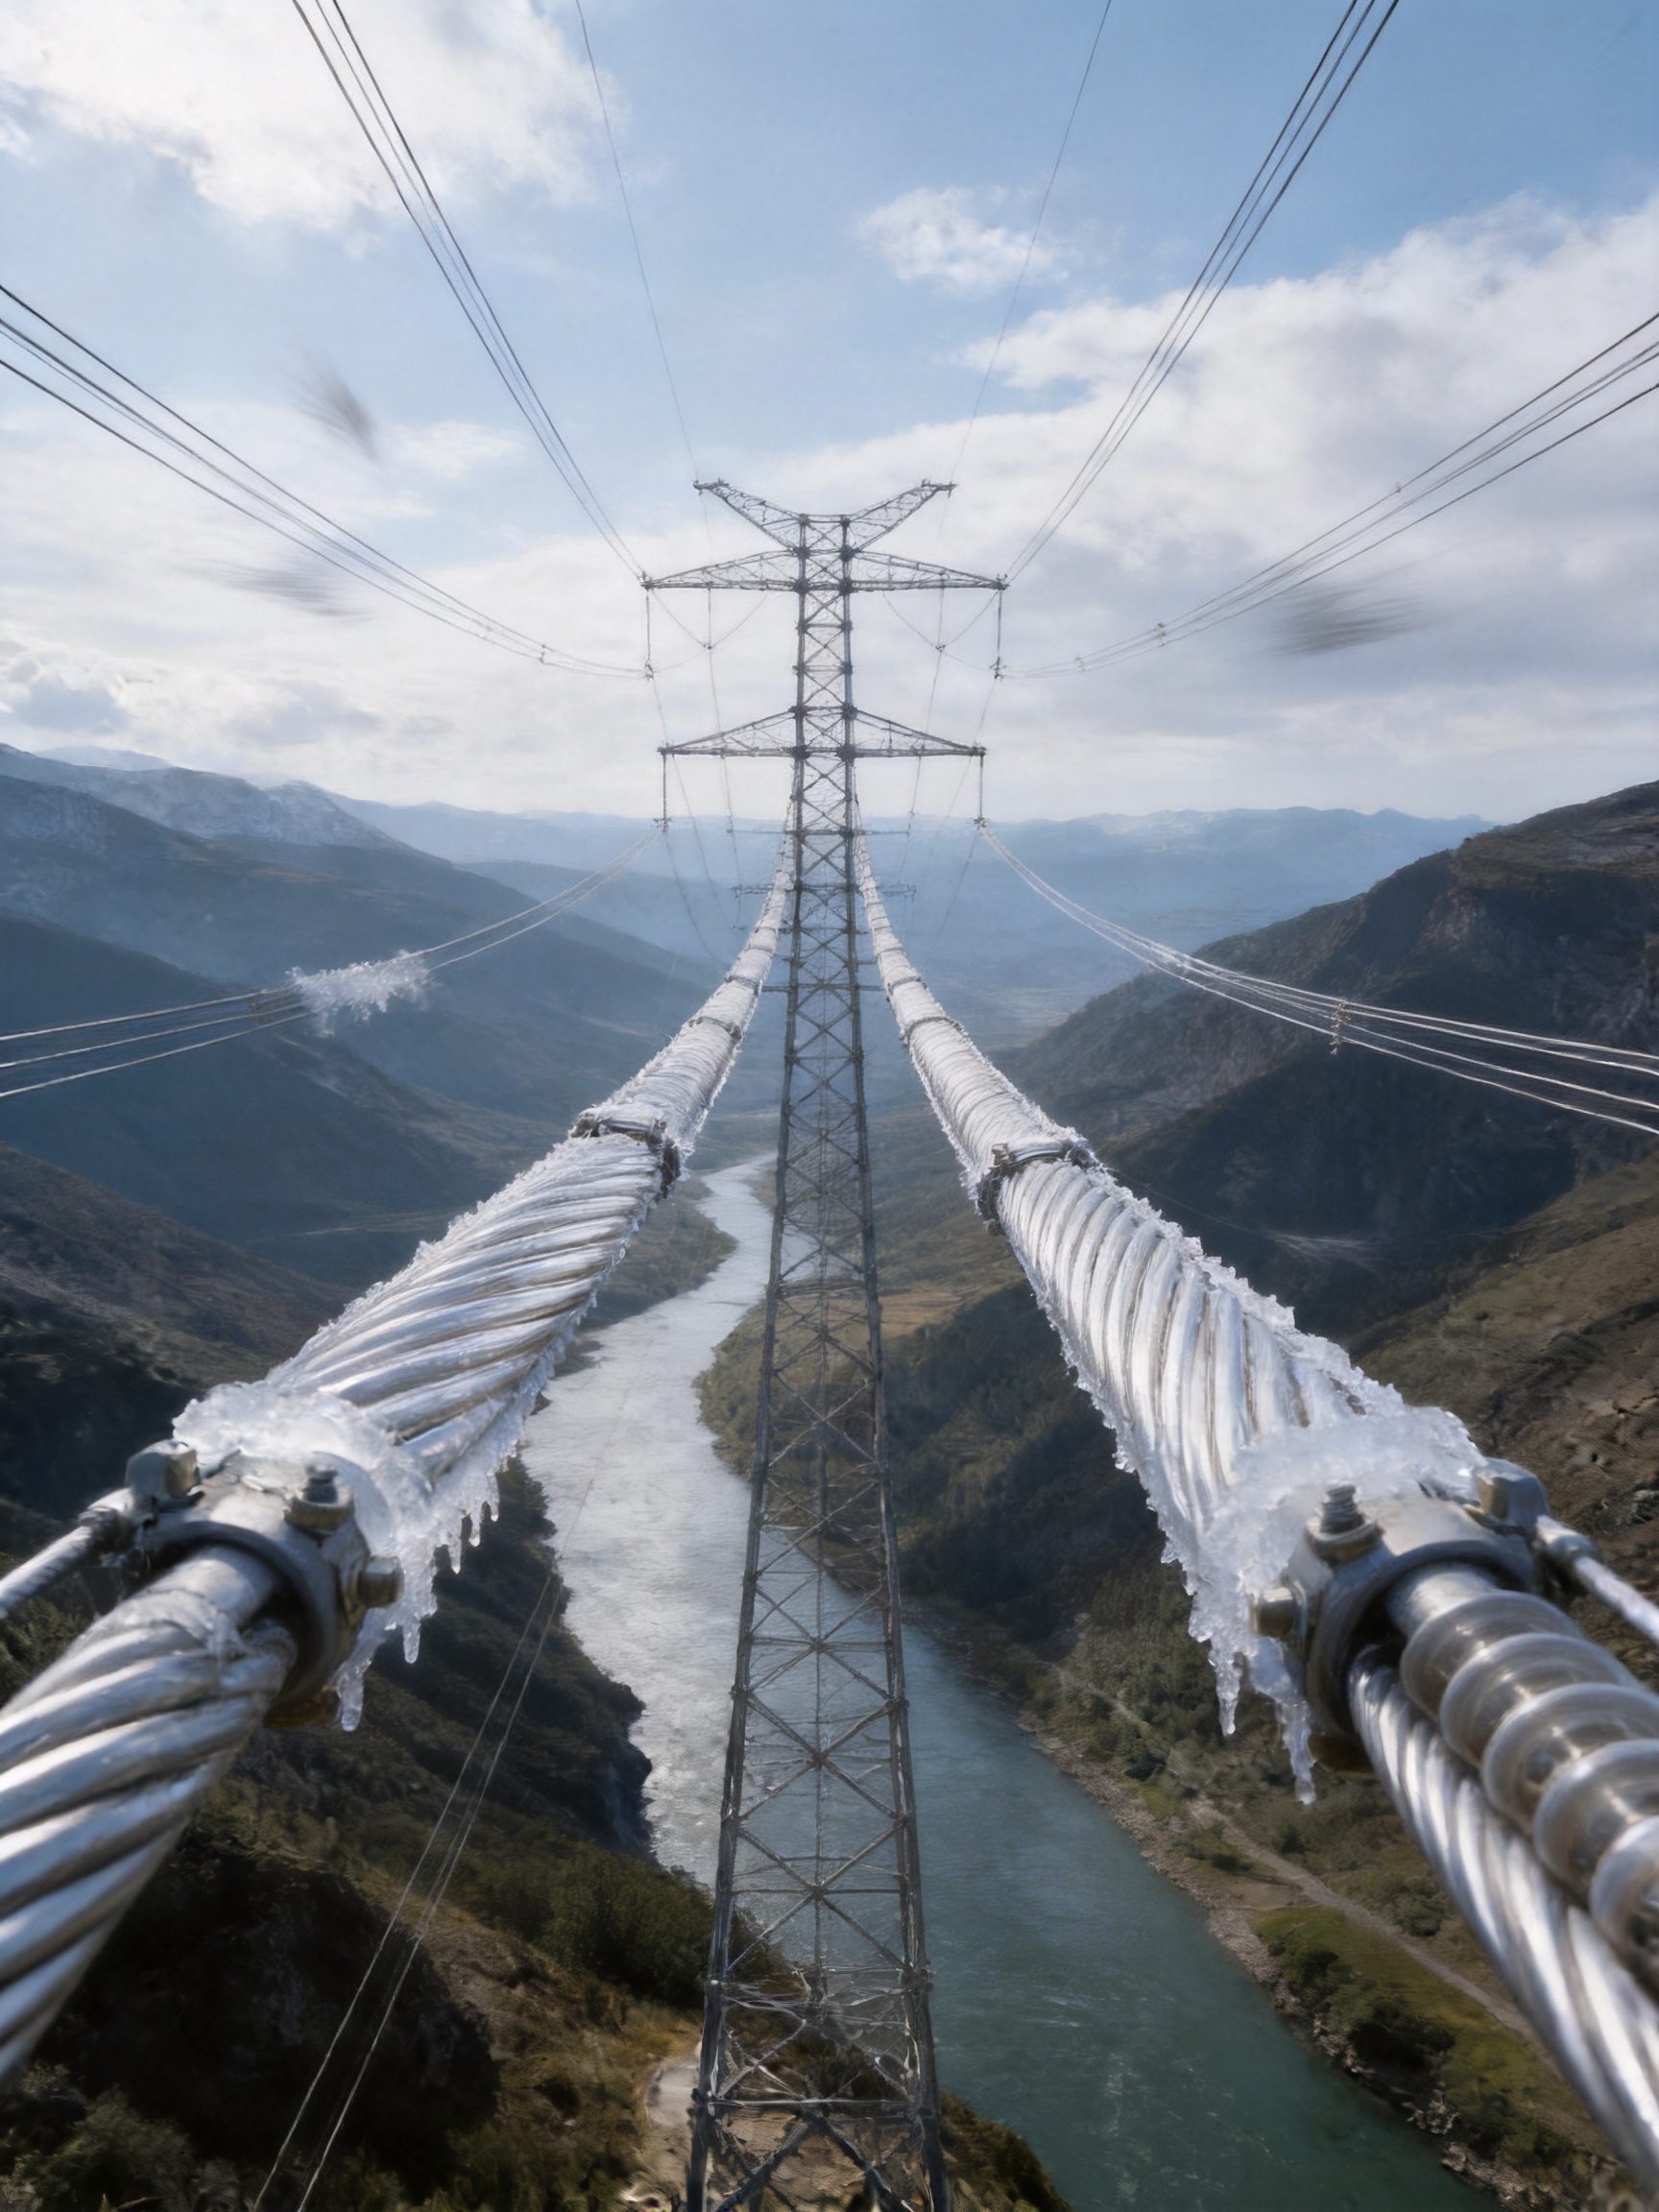
The product is stated to withstand an ice coating load of 30 mm. Ice loading can add substantial weight and increase tension in the conductor. The actual allowable ice condition depends on span length, support spacing, conductor size, tower design, and local engineering requirements.
After 5,000 hours of salt-spray testing, the product retains more than 95 percent of its tensile strength under the stated test conditions. It is also described as showing no significant surface degradation after 5,000 hours of ultraviolet aging. These results indicate a focus on corrosion resistance and outdoor durability, although site-specific inspection remains necessary in aggressive environments.
6.1 Coastal and Industrial Environments
Coastal installations expose conductors to salt-laden air, moisture, and cyclic wetting and drying. Industrial environments may add chemical pollutants, dust, and conductive deposits. The aluminum surface and galvanized steel core help protect the conductor, but joints, clamps, damaged surfaces, and areas beneath fittings require particular attention.
Routine inspection should look for pitting, unusual discoloration, broken strands, loose wires, corrosion around connectors, clamp slippage, and evidence of overheating. In coastal areas, maintenance intervals may need to be shorter than in clean inland environments.
7. Advantages Compared with Standard All-Aluminum Conductors
All-aluminum conductors are valuable where low weight, simple construction, and good conductivity are the main priorities. However, their lower tensile strength can limit span length and increase sag under mechanical loading. The steel-reinforced aluminum strand addresses this limitation by adding a high-strength core without abandoning the conductive advantages of aluminum.
| Performance Category | Steel-Reinforced Aluminum Strand | Standard All-Aluminum Conductor |
|---|---|---|
| Tensile strength | High because of the steel core | Low to moderate depending on alloy and construction |
| Long-span suitability | Well suited to long spans and high mechanical loading | More suitable for short to medium spans unless specially designed |
| Sag control | Improved mechanical resistance supports reduced sag | May require shorter spans or lower installation temperatures |
| Electrical conductivity | High through the aluminum layers | High through the aluminum conductor body |
| Wind and ice resistance | Strong mechanical support under environmental loading | More limited mechanical reserve |
| Weight | Moderate because of the steel reinforcement | Generally lighter |
| Corrosion behavior | Aluminum exterior with galvanized steel reinforcement | Aluminum exterior and conductive body |
| Typical applications | Transmission lines, long spans, shield wires, demanding distribution systems | General distribution and applications with moderate mechanical requirements |
The main trade-off is weight. The steel core increases the conductor’s mass compared with a similar all-aluminum design. However, this additional weight may be justified when the project requires higher tensile strength, longer spans, improved sag control, or greater resistance to weather-related loading.
Compared with a conductor made entirely from a high-strength alloy, the steel-reinforced design offers another type of performance balance. Its steel core delivers substantial mechanical support, while the aluminum layers provide an established conductive surface and corrosion-resistant exterior. The most suitable option depends on the project’s electrical, mechanical, environmental, and economic priorities.
8. Primary Applications
8.1 Overhead Transmission Lines
Overhead transmission is the most recognized application. Conductors must bridge long distances between towers while maintaining required ground clearances and phase-to-phase spacing. The steel core improves tensile performance and helps limit sag, making the product suitable for long-span routes and challenging terrain.
Longer spans can reduce the number of towers and foundations required for a line. This may be valuable when the route crosses rivers, highways, railways, valleys, industrial zones, or environmentally sensitive areas. The final span length must be determined through a complete mechanical design rather than by conductor tensile strength alone.
8.2 High-Tension Distribution
High-tension distribution networks require reliable conductors that can remain stable under changing weather conditions and operating loads. The composite structure supports improved mechanical stability and helps reduce the risk of excessive sag, which can affect clearances and service reliability.
The available range from smaller to larger cross-sectional combinations makes it possible to match the conductor to different distribution capacities. Selection should account for load growth, short-circuit current, line length, voltage drop, environmental exposure, and the required reliability class.
8.3 Ground Wires and Shield Wires
Steel-reinforced aluminum strands can be used as ground wires or shield wires on transmission structures. Installed above the phase conductors, these wires help intercept lightning and provide a path for fault or lightning current toward the grounding system.
In this role, mechanical durability is especially important because the ground wire is exposed to wind, ice, vibration, and repeated environmental stress. Electrical performance, grounding continuity, hardware compatibility, and tower earthing must all be considered together.
8.4 Damping Wires and Hardware Connections
The product is also intended for damping wire applications and hardware connections such as damping-type end caps. In these installations, the strand may work with specialized fittings to reduce vibration or maintain a secure connection between conductor components.
Correct compression procedures and compatible fittings are essential. Aluminum-to-steel transition hardware must be selected to accommodate the composite conductor, prevent strand damage, maintain contact pressure, and limit oxidation or galvanic interaction.
9. Manufacturing Process and Quality Control
The performance of a steel-reinforced aluminum strand depends heavily on manufacturing consistency. Small variations in wire diameter, steel coating, stranding pitch, pre-twist, material temper, or final dimensions can affect electrical resistance, tensile strength, flexibility, and installation behavior. For this reason, the production process must be controlled from raw-material inspection through final shipment.
9.1 Raw-Material Selection
Production begins with the selection of electrical-grade aluminum and suitable steel wire. Aluminum purity, surface condition, chemical composition, and drawing quality influence conductivity and mechanical behavior. Steel quality affects tensile performance, fatigue resistance, dimensional stability, and galvanizing results.
Incoming materials should be checked against procurement specifications and manufacturing requirements. Inspection may include diameter measurement, surface examination, conductivity verification, tensile testing, and coating assessment. Controlling raw materials at the beginning of the process reduces the risk of defects in later stages.
9.2 Aluminum Wire Drawing and Annealing
Aluminum wire is drawn through controlled dies to achieve the required diameter and surface quality. Drawing equipment must maintain stable line speed, tension, lubrication, and die condition. Excessive drawing stress or poor lubrication can create surface defects and affect wire flexibility.
Annealing is used to adjust the aluminum’s mechanical properties and restore the desired balance between strength and ductility. Temperature, time, cooling conditions, and furnace uniformity must be controlled. Proper annealing supports the stated conductivity target above 61 percent IACS and helps the strands withstand stranding and installation without excessive cracking or breakage.
9.3 Steel Wire Galvanizing
The steel core wires are galvanized to improve corrosion protection. The galvanizing process requires control of surface preparation, bath conditions, coating adhesion, coating thickness, and cooling. The stated zinc coating weight of at least 300 g/m² provides a defined basis for corrosion protection.
Uniform coating is important because thin or damaged areas may become localized corrosion sites. The finished steel wire should be inspected for continuity, adhesion, surface defects, and dimensional consistency before it enters the stranding process.
9.4 Core Stranding
Individual steel wires are stranded to form the central core when a multi-wire core is specified. The stranding machine must control tension and pitch so that the core remains compact and stable. Uneven tension may cause one wire to carry excessive load or create an irregular core diameter.
The core is inspected for roundness, pitch, surface condition, and mechanical continuity. Proper core formation is essential because the aluminum layers depend on the core’s geometry for uniform support.
9.5 Aluminum Layer Stranding
Aluminum wires are applied around the steel core in one or more concentric layers. The machine controls the number of wires, pitch, direction of lay, tension, and final diameter. The strands must remain closely arranged without excessive gaps, crossing, or local displacement.
Layer-by-layer inspection helps verify that the conductor remains within dimensional tolerances. The controlled pre-twisting process reduces the possibility of loosening when the finished conductor is handled or placed under tension.
9.6 Final Inspection and Testing
Final inspection may include outer-diameter measurement, cross-sectional verification, resistance testing, tensile testing, weight measurement, visual inspection, and packaging checks. Depending on project requirements, additional tests may evaluate thermal cycling, vibration endurance, corrosion resistance, or surface condition.
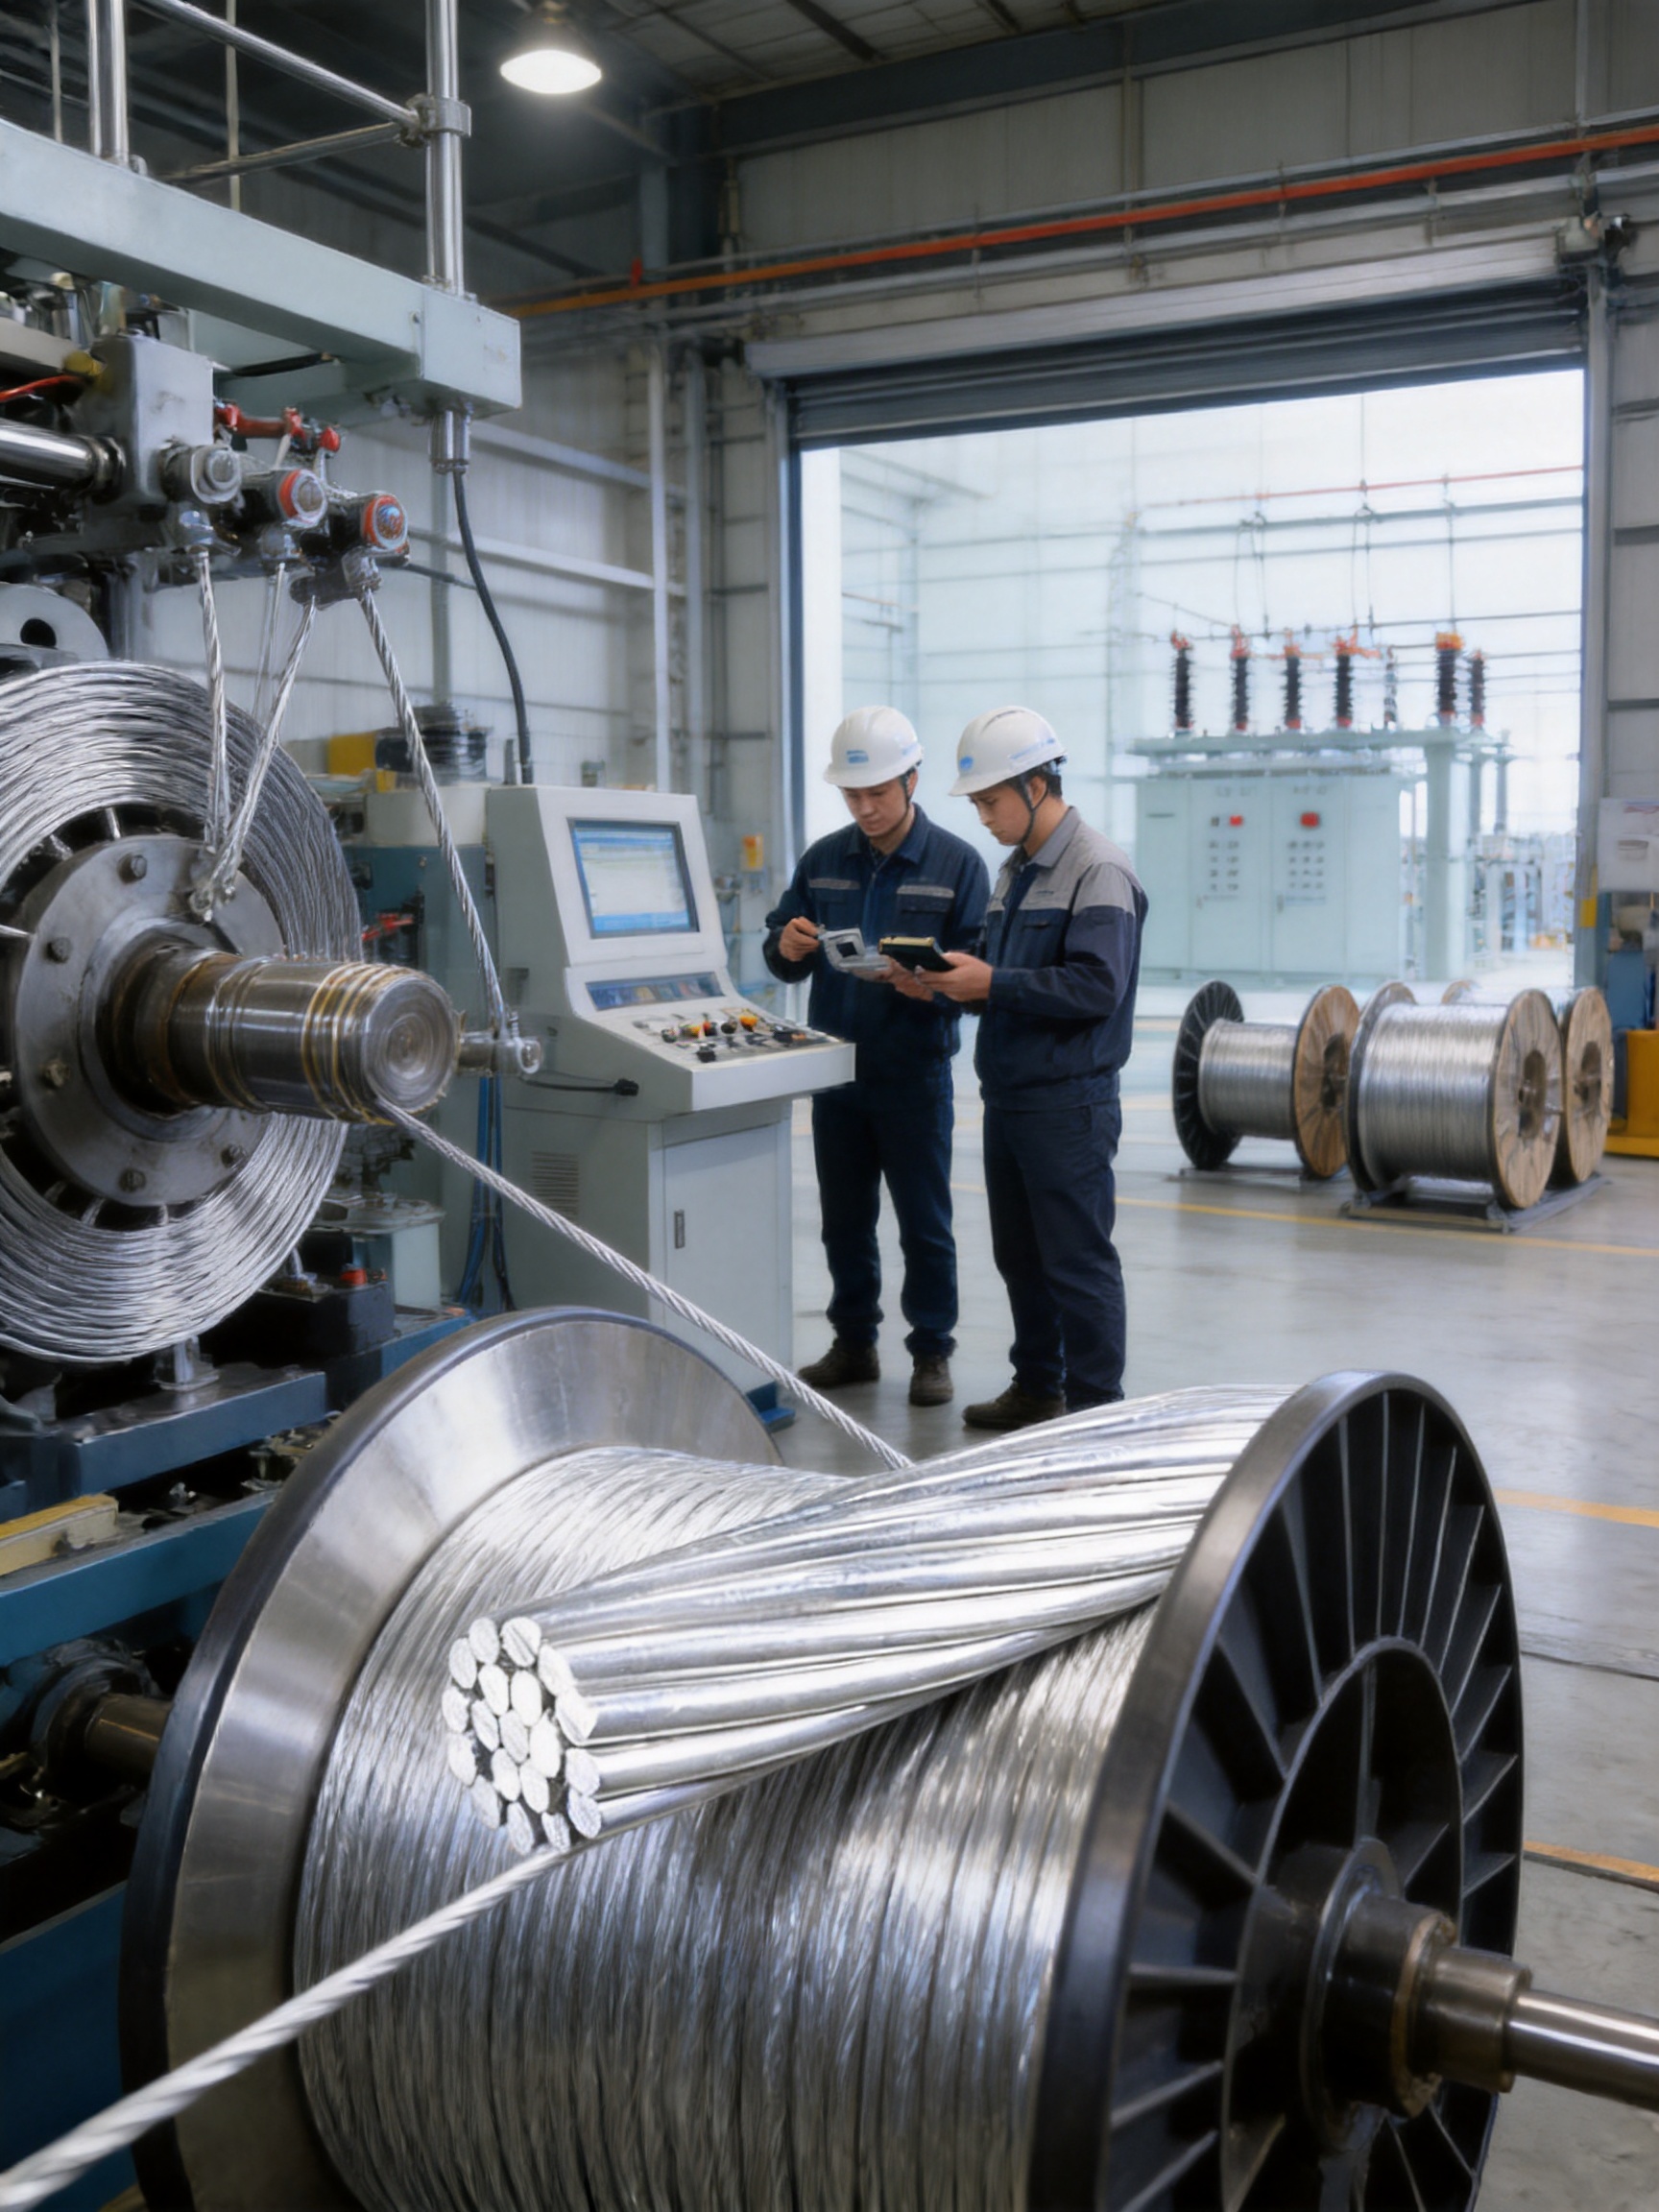
Jiangsu Wopeng Power Technology operates production lines supported by vacuum casting systems, CNC machining equipment, and automated assembly technologies. Although these systems are primarily associated with the company’s broader busbar portfolio, they demonstrate an engineering environment built around controlled processing, dimensional accuracy, equipment integration, and repeatable quality management.
The company also applies standardized inspection procedures to its power products, including high-voltage testing, insulation testing, mechanical verification, and routine quality checks. Collaboration with third-party testing institutions provides additional independent validation for applicable products and projects.
10. Engineering and Manufacturing Strengths
Jiangsu Wopeng Power Technology Co., Ltd. was founded in 2018 as a high-tech enterprise focused on high- and low-voltage busbar systems and related power transmission solutions. The company’s product portfolio includes 35 kV epoxy resin vacuum-cast tube busbars, low-voltage cast-resin busways, copper and aluminum tubular busbars, wind-power tube busbars, compact busbar systems, and sliding contact line systems.
This product breadth is relevant to customers purchasing steel-reinforced aluminum strand because conductor selection is often part of a wider electrical infrastructure project. A supplier with experience in tubular busbars, insulated busbars, busway systems, and high-current equipment can better understand the relationship between conductors, connection hardware, insulation, mechanical supports, clearances, and system integration.
The company’s engineering team includes engineers, technical specialists, and production professionals with experience in power equipment technology. This combination supports technical communication during specification development, product selection, drawing review, production coordination, and quality verification.
Wopeng products are used across more than 17 provinces and multiple industrial sectors. Applications include power generation, substations, wind energy, industrial manufacturing, rail transit, and large commercial facilities. This operating experience provides exposure to varied requirements involving high current, demanding environmental conditions, compact installation spaces, and continuous-duty operation.
Modern production equipment contributes to consistency, but equipment alone does not guarantee product performance. The company’s manufacturing strength also depends on process discipline, inspection procedures, engineering review, material control, and personnel experience. These factors help convert design requirements into repeatable products.
10.1 Integrated Power-Product Capability
Many electrical projects require several types of power equipment. A supplier that can provide or coordinate multiple product categories may help simplify technical communication and project management. Wopeng’s portfolio covers low-voltage systems through 35 kV applications, including insulated busbars, tubular busbars, busways, and specialized power supply systems.
For a customer evaluating steel-reinforced aluminum strand alongside tubular busbar equipment, this integrated perspective can be useful. The design team can consider conductor properties, connection methods, insulation requirements, mechanical support, thermal performance, and installation constraints as parts of one electrical system rather than as isolated components.
10.2 OEM and Customization Support
Power infrastructure projects often have requirements that differ from standard catalog conditions. These may include special cross-sectional combinations, defined delivery lengths, custom packaging, project-specific markings, connector requirements, environmental performance, or coordination with existing equipment.
A custom manufacturing approach allows the supplier to review the customer’s technical data and determine the appropriate product configuration. Customization should be based on verified engineering calculations and applicable standards. It should not compromise conductor geometry, material quality, tensile performance, or electrical safety.
11. Installation Recommendations
Correct installation is necessary to preserve the product’s designed performance. The conductor should be transported and stored in a way that prevents drum damage, excessive bending, impact, moisture accumulation, and contamination. The reel should be inspected before deployment to confirm that the conductor has not been crushed or exposed to abnormal mechanical stress.
11.1 Tension Stringing
Tension stringing is commonly used where conductor clearance and installation control are important. The stringing tension must remain within the approved limits. Although the steel core permits higher tension than many all-aluminum conductors, the elastic limit must not be exceeded.
Stringing equipment, pulleys, rollers, swivels, and grips must be compatible with the conductor diameter and construction. Excessive bending over small pulleys can damage strands or create permanent deformation. During installation, technicians should monitor for birdcaging, strand displacement, surface damage, and irregular tension.
11.2 Connector Compatibility
Compression connectors must be suitable for a composite aluminum-and-steel conductor. A connector intended only for all-aluminum conductors may not correctly grip the steel core or maintain the required electrical and mechanical connection.
Aluminum-to-steel transition connectors should be selected according to conductor designation, strand arrangement, diameter, tensile requirement, and applicable installation instructions. Surfaces must be prepared as specified, and compression dies must match the connector manufacturer’s requirements.
11.3 Sag-Tension Adjustment
After stringing, the conductor should be adjusted according to the approved sag-tension tables and environmental design conditions. Temperature, span length, initial tension, wind, ice, and elevation differences all influence the final position.
Accurate sag control protects electrical clearances and limits excessive mechanical loading. Surveying and verification should be completed before final clipping and before the line is placed into service.
11.4 Inspection During Installation
Installation personnel should examine the conductor for broken aluminum wires, damaged galvanized steel wires, abnormal kinks, surface abrasion, loose strands, and connector deformation. Defects should be recorded and evaluated before the conductor is covered, clamped, or energized.
All fittings should be installed according to approved drawings and procedures. Damping devices should be positioned at the specified locations, and the installation should ensure that vibration-control hardware does not create concentrated damage on the conductor.
12. Maintenance and Service-Life Considerations
Regular inspection helps maintain the reliability of overhead conductors. Visual inspections may identify broken strands, corrosion, birdcaging, clamp movement, unusual sag, surface deposits, and signs of overheating. Infrared inspection can help identify high-resistance connections or abnormal temperature rise under load.
In areas with strong wind, repeated icing, salt spray, or industrial pollution, inspection frequency should be adjusted to the site conditions. Particular attention should be given to suspension points, tension fittings, splices, grounding connections, and locations where vibration may concentrate.
Electrical measurements can supplement visual inspection. Resistance checks, thermal imaging, grounding continuity tests, and hardware torque verification may be used according to the maintenance plan. Any repair or replacement should use compatible components and follow the original conductor manufacturer’s technical requirements.
The aluminum exterior should not be aggressively scraped or treated with unsuitable chemicals. Cleaning methods must preserve the conductor surface and avoid damaging the zinc coating on exposed steel components. If corrosion or mechanical damage is found, the appropriate corrective action should be determined by a qualified engineer.
13. Selection Guide for Engineers and Buyers
Before ordering reinforcing steel aluminum strand, the purchaser should prepare a complete technical specification. Important information includes the nominal aluminum and steel areas, required standard, conductor length, allowable resistance, tensile strength, outer diameter, weight, delivery packaging, environmental conditions, and intended application.
The electrical design should define continuous current, emergency current, short-circuit current, operating temperature, voltage level, and allowable voltage drop where applicable. The mechanical design should define span length, support arrangement, wind pressure, ice thickness, temperature range, installation tension, sag limits, and vibration-control requirements.
Connector and fitting information should also be provided. The conductor must work with the selected clamps, end caps, suspension hardware, tension fittings, dampers, grounding equipment, and splicing accessories. Compatibility should be verified before production whenever the conductor is intended for an existing system.
Buyers should evaluate not only the lowest initial price but also total project value. A conductor with higher tensile strength may reduce tower quantity, improve clearance, reduce maintenance risks, or simplify difficult crossings. The economic comparison should include material cost, transportation, installation equipment, support structures, maintenance, and expected service life.
14. Safety and Reliability Benefits
Electrical infrastructure must maintain safe clearances and stable mechanical support under normal and abnormal conditions. The steel-reinforced construction contributes to safety by improving resistance to tension, sag, wind, and ice. Stable conductor geometry helps protect the required distance from ground, buildings, roads, railways, and other circuits.
Reliable conductivity also supports safe operation. Controlled resistance reduces unnecessary heating and energy loss. Consistent manufacturing minimizes the likelihood of local defects that could become electrical hot spots, mechanical weak points, or sources of premature failure.
The product should nevertheless be treated as part of a complete engineered system. Safety depends on conductor selection, tower design, insulation coordination, grounding, overcurrent protection, connectors, installation quality, inspection, and maintenance. No individual material can replace a complete electrical and mechanical design.
15. Frequently Asked Questions
Q1: What is reinforcing steel aluminum strand?
Reinforcing steel aluminum strand is a composite conductor made by stranding aluminum wires around a galvanized steel core. The aluminum provides most of the electrical conductivity, while the steel core supplies mechanical strength and resistance to tension.
Q2: What standard does this product follow?
The product described in this specification conforms to GB1179-83. Customers should confirm whether additional national, regional, utility, ASTM, IEC, or project-specific requirements apply to their installation.
Q3: What sizes are available?
The stated nominal cross-sectional range is from 10/2 mm² to 240/30 mm². The first value represents the approximate aluminum area and the second represents the approximate steel-core area. Specific construction details should be confirmed through the product drawing or technical datasheet.
Q4: Why is steel added to an aluminum conductor?
Steel is added to increase tensile strength and improve mechanical stability. This helps the conductor withstand long spans, installation tension, wind, ice, vibration, and other mechanical loads more effectively than many standard all-aluminum designs.
Q5: Does the steel core carry electrical current?
The aluminum layers carry the majority of the electrical current. The steel core contributes primarily to mechanical reinforcement. Because the conductor contains a substantial aluminum conductive area, it retains useful electrical performance while gaining higher tensile strength.
Q6: Is the product suitable for long-span transmission lines?
It is designed for applications where mechanical strength is important, including long-span overhead transmission lines. The actual suitability depends on span length, conductor size, tower design, environmental loading, sag requirements, and the approved sag-tension calculation.
Q7: Can it be used in coastal environments?
Yes, the aluminum outer layer and galvanized steel core provide resistance to many outdoor corrosion conditions. The product is described as retaining more than 95 percent of its tensile strength after 5,000 hours of salt-spray testing under the stated test conditions. Coastal installations should still receive regular inspection.
Q8: What connectors should be used?
Connectors must be specifically compatible with a steel-reinforced aluminum conductor. Aluminum-to-steel transition compression connectors or other approved fittings should be selected according to the conductor designation and the manufacturer’s installation requirements.
Q9: Can the conductor be used as a ground wire or shield wire?
Yes, the product can be used for ground-wire and shield-wire applications when its electrical, mechanical, and grounding requirements are satisfied. The tower grounding system, lightning performance, fittings, and fault-current duty must be evaluated as part of the overall design.
Q10: What delivery length is normally available?
The stated delivery length is generally less than 2,000 meters. The final length depends on the product size, project requirements, packaging method, and production arrangement.
Q11: What quality checks are important before shipment?
Important checks may include outer diameter, cross-sectional area, resistance, tensile strength, weight, strand condition, zinc coating, surface quality, packaging, and identification markings. Additional tests may be required for specific projects.
Q12: Why choose a supplier with busbar manufacturing experience?
A supplier experienced in busbars and power transmission equipment may provide broader engineering support for system integration. This can be useful when the conductor must coordinate with tubular busbars, insulated busbars, connection hardware, substations, wind-power systems, or other high-current equipment.
16. Conclusion
Reinforcing steel aluminum strand provides a practical combination of aluminum conductivity and steel mechanical strength. Its composite structure makes it suitable for overhead transmission, high-tension distribution, shield wires, grounding applications, damping wires, and hardware connections where a standard all-aluminum conductor may not provide sufficient tensile performance.
The product range from 10/2 mm² to 240/30 mm² supports different current capacities, span conditions, and mechanical requirements. Controlled aluminum purity, annealing, galvanized steel reinforcement, concentric stranding, pre-twisting, and standardized inspection contribute to stable electrical and mechanical performance.
Compared with standard all-aluminum conductors, the steel-reinforced design offers improved tensile strength, long-span capability, sag control, and resistance to wind and ice loading. Its moderate increase in weight is often justified when structural reliability and installation performance are major priorities.
Jiangsu Wopeng Power Technology Co., Ltd. strengthens this product offering through engineering experience, modern production equipment, a broad busbar portfolio, standardized quality procedures, and project-oriented technical support. Its capabilities in high- and low-voltage power systems provide a useful foundation for customers seeking coordinated solutions for conductors, tubular busbars, insulated busbars, and related electrical infrastructure.
For the best result, every order should be based on a complete technical review covering electrical capacity, tensile requirements, span length, environmental exposure, installation method, connector compatibility, and maintenance conditions. When correctly selected, installed, and maintained, reinforcing steel aluminum strand can support safe, efficient, and durable power transmission infrastructure.
References
GB1179-83, Standard Specification for Stranded Conductors Used in Electrical Power Transmission Applications.
IEC 61089, Round Wire Concentric Lay Overhead Electrical Stranded Conductors.
ASTM B399, Standard Specification for Concentric-Lay-Stranded Aluminum-Alloy Conductors, Steel Reinforced.
International Annealed Copper Standard, Reference Requirements for Electrical Conductivity.
Overhead Transmission Line Design Principles, including conductor sag, tension, wind loading, ice loading, vibration, and clearance calculations.
Electrical Power Equipment Inspection and Maintenance Practices for Outdoor Conductors and Connection Hardware.
Product: Reinforcing Steel Aluminum Strand


-
 +86-180 3625 3000
-
 admin@wpbusbar.com
-
 No. 8, Yanjin Road, Chengxi Industrial Park, Shanyang Town, Baoying County, Yangzhou City, Jiangsu Province, China
Copyright © Jiangsu Wopeng Power Technology Co., Ltd.
All Rights Reserved.
 Custom Insulated Bus Bar Manufacturer
Tubular Busbar System Factory