

 EN

 English
 русский
 Français
 Español
 عربى
Reinforcing Steel Aluminum Strand: Structure, Performance, Manufacturing Quality, and Application Guide
Content
- 1 1. Product Overview
- 2 2. Main Technical Specifications
- 3 3. Material Composition and Functional Design
- 4 4. Manufacturing Process and Quality Control
- 5 5. Technical Advantages Compared with Alternative Conductors
- 6 6. Applications
- 7 7. Installation and Maintenance Guidance
- 8 8. Why Choose an Experienced Manufacturer
- 9 9. Customization and Project Support
- 10 10. Frequently Asked Questions
- 10.1 Q1: What is reinforcing steel aluminum strand?
- 10.2 Q2: What standard applies to the supplied product?
- 10.3 Q3: What nominal sizes are available?
- 10.4 Q4: Why is a steel core used?
- 10.5 Q5: Is the steel core the main current-carrying component?
- 10.6 Q6: Can the product be used in coastal areas?
- 10.7 Q7: Can it be used with damping-type end caps?
- 10.8 Q8: How should the conductor be installed?
- 10.9 Q9: What information should be provided when requesting a quotation?
- 10.10 Q10: What makes an experienced manufacturer valuable?
- 11 11. Conclusion
- 12 References
- 13 Product: Reinforcing Steel Aluminum Strand
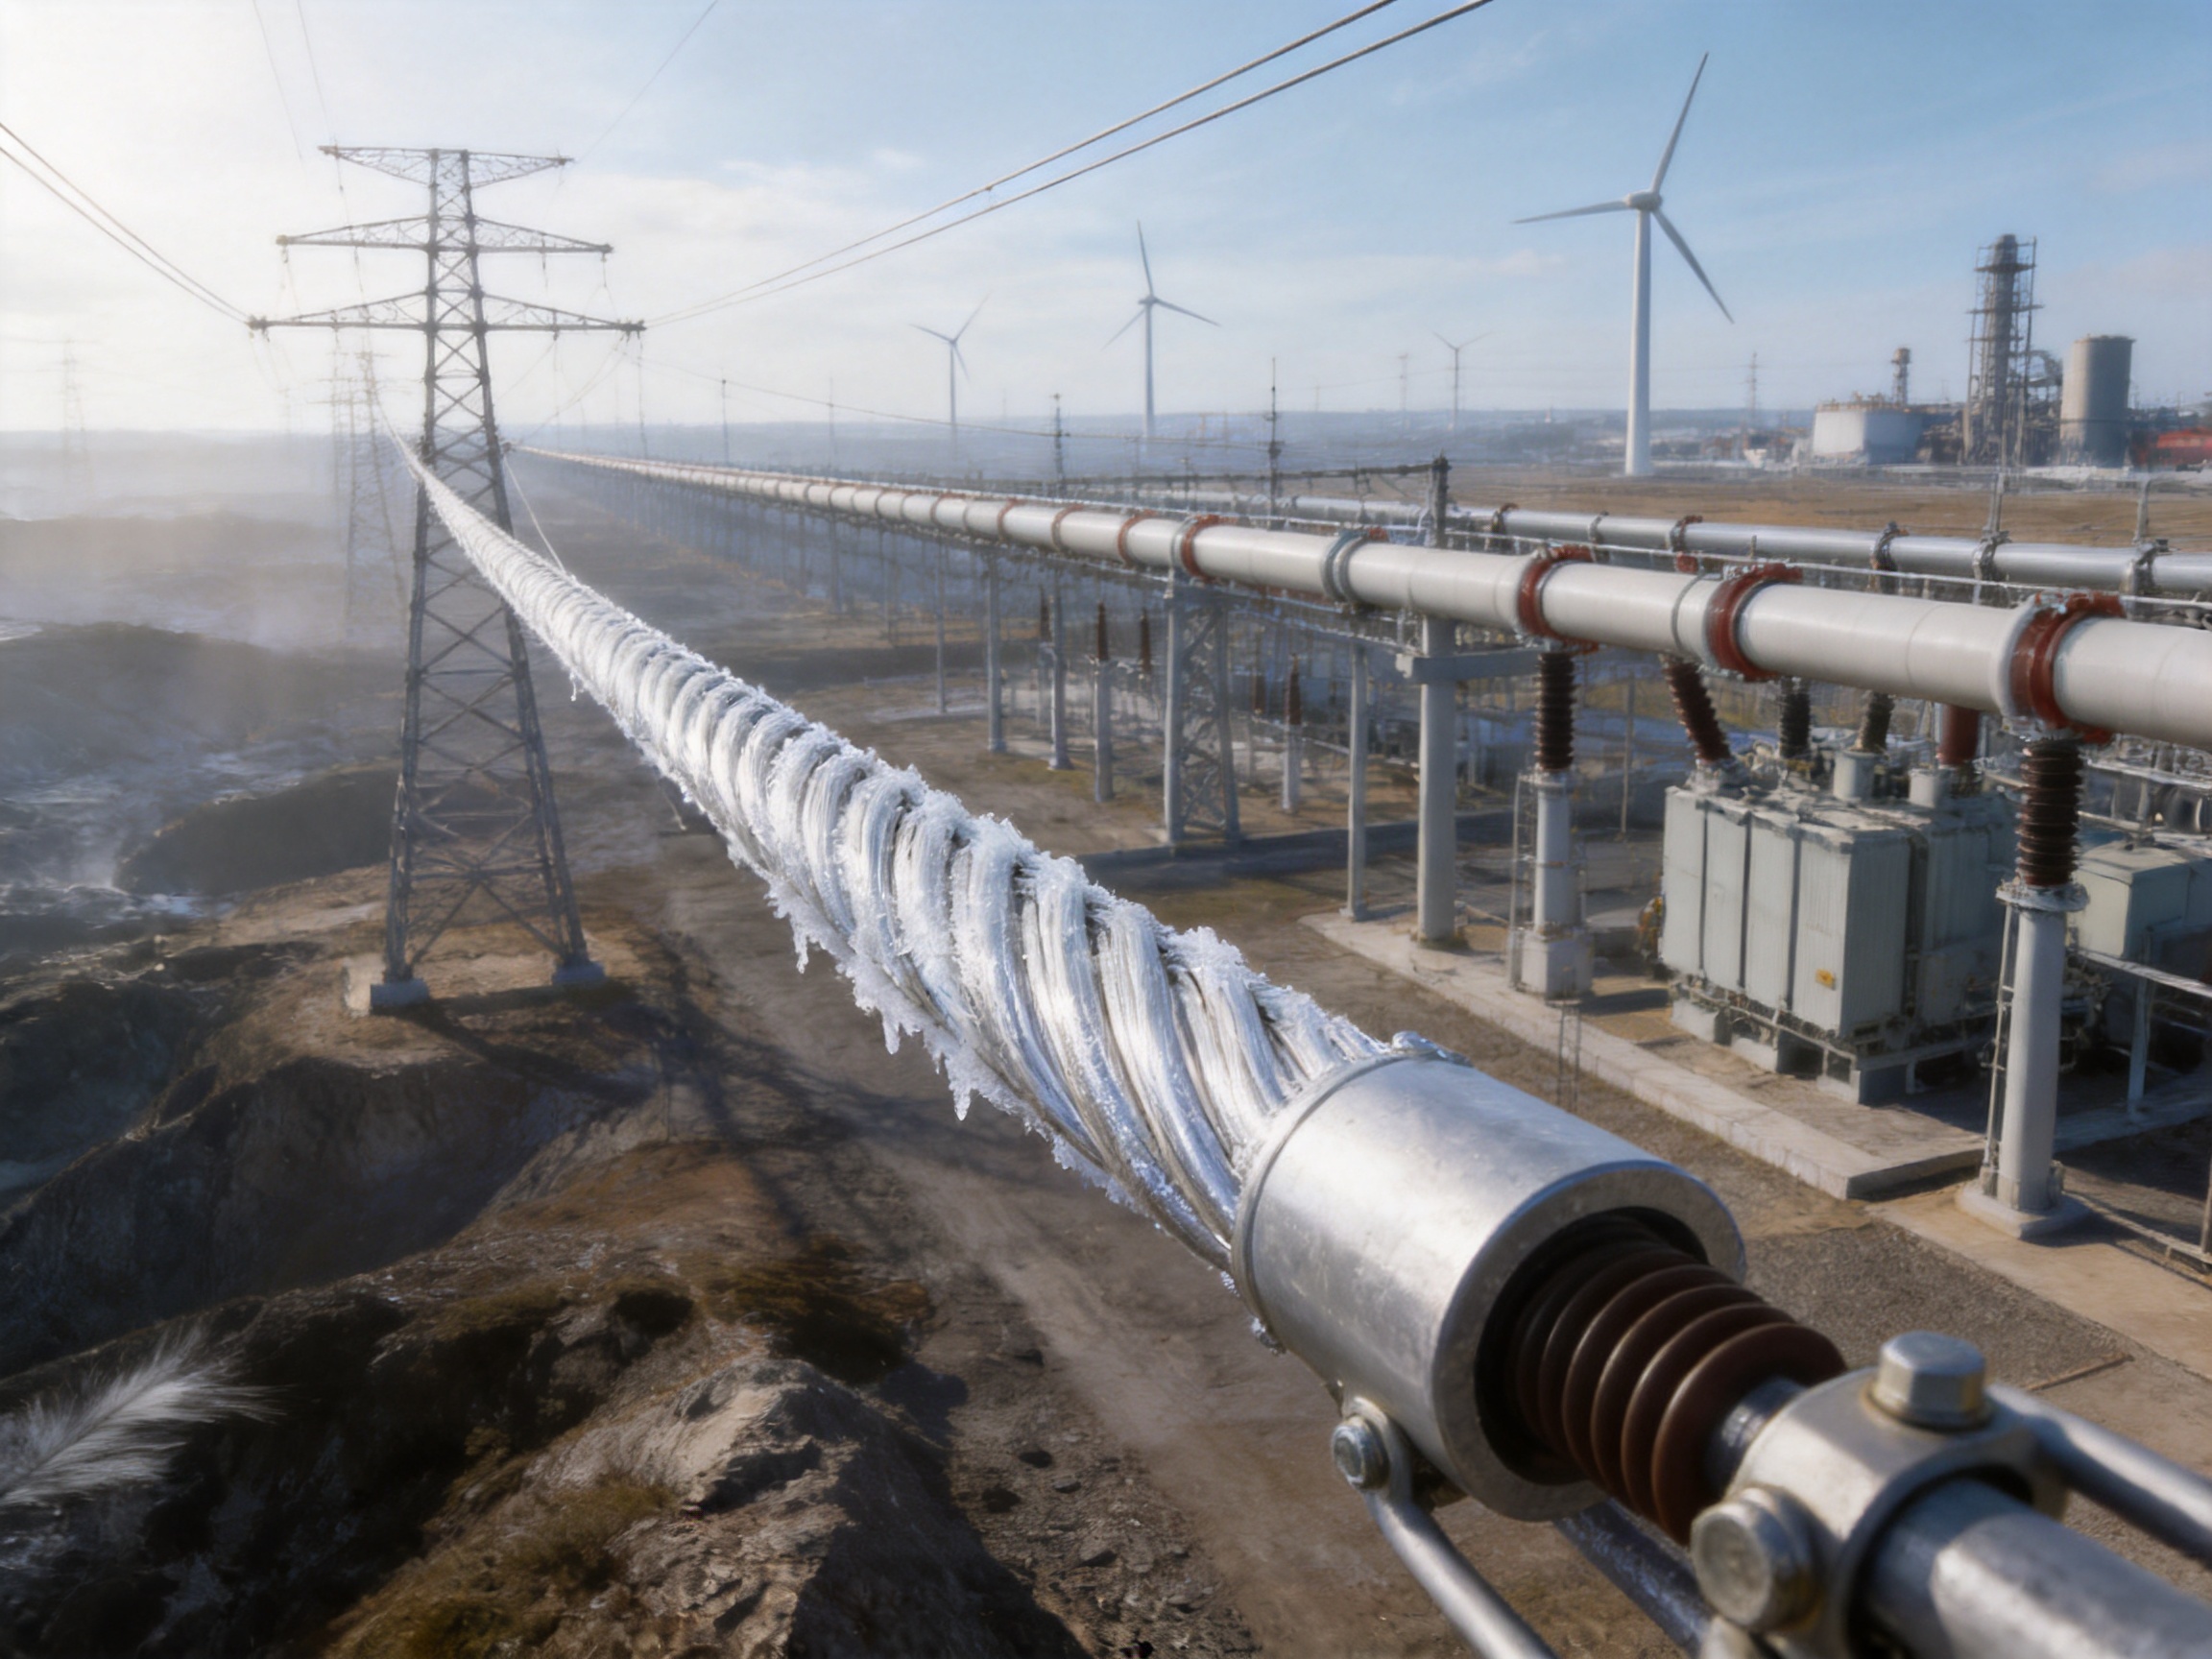
Reinforcing steel aluminum strand is a composite stranded conductor designed to combine the electrical conductivity of aluminum with the mechanical strength of a steel core. This construction makes it suitable for applications in which a conductor must carry electrical current while also resisting tension, vibration, wind, ice, installation stress, and long-term mechanical loading. Unlike an all-aluminum conductor, the product uses a steel reinforcement element to improve tensile performance, dimensional stability, and span capability.
Manufactured in accordance with the GB1179-83 standard, reinforcing steel aluminum strand is available in a broad range of nominal cross-sections, from 10/2 mm² to 240/30 mm². Depending on the selected specification, the conductor is formed by wrapping aluminum strands around one or more galvanized steel-core strands. The aluminum component performs the primary electrical conduction function, while the steel component provides structural support.
Jiangsu Wopeng Power Technology Co., Ltd. supplies power-transmission products and related busbar systems for demanding electrical infrastructure. Its experience in tubular busbars, cast-resin busbar systems, copper and aluminum conductors, wind-power applications, and industrial power distribution provides a strong technical foundation for supplying engineered conductive components. Through controlled material selection, precision stranding, standardized inspection, and application-oriented engineering support, the company can provide reinforcing steel aluminum strand solutions for power equipment and hardware connection requirements.
1. Product Overview
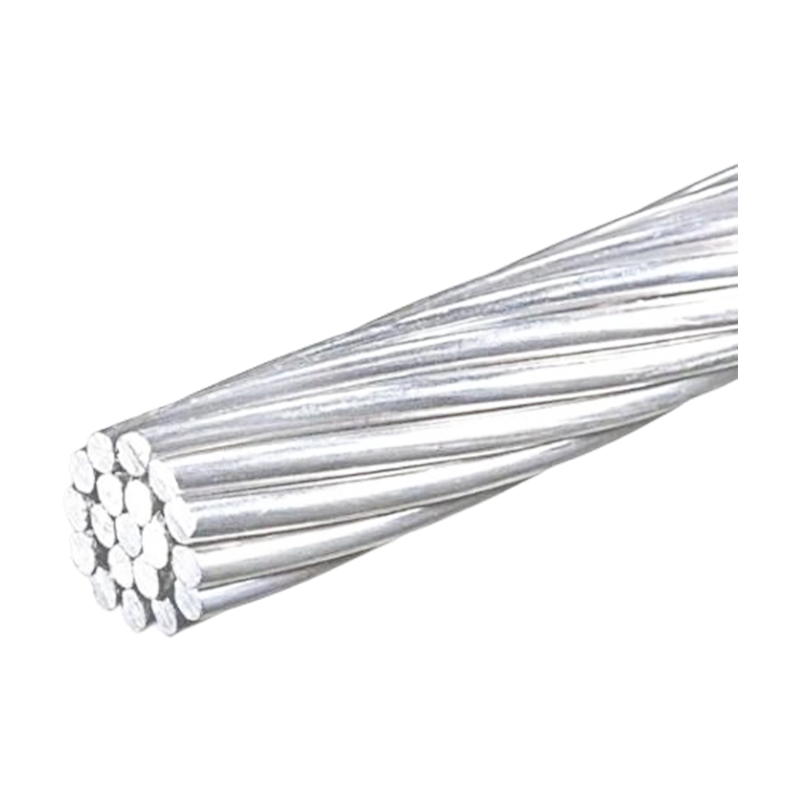
Reinforcing steel aluminum strand is a concentric stranded conductor consisting of aluminum wires arranged around a steel core. The product is often identified by a paired nominal area, such as 10/2 mm² or 240/30 mm². The first value generally represents the nominal aluminum area, while the second represents the nominal steel-core area. This designation helps engineers evaluate the balance between conductivity, weight, tensile strength, and installation performance.
The conductor’s composite design addresses a central challenge in electrical engineering. Aluminum is lightweight, relatively economical, and highly conductive, but it does not provide the same tensile strength as steel. Steel offers excellent mechanical strength but is not suitable as the primary current-carrying material. By combining the two materials in a concentric structure, reinforcing steel aluminum strand offers a practical balance between electrical and mechanical requirements.
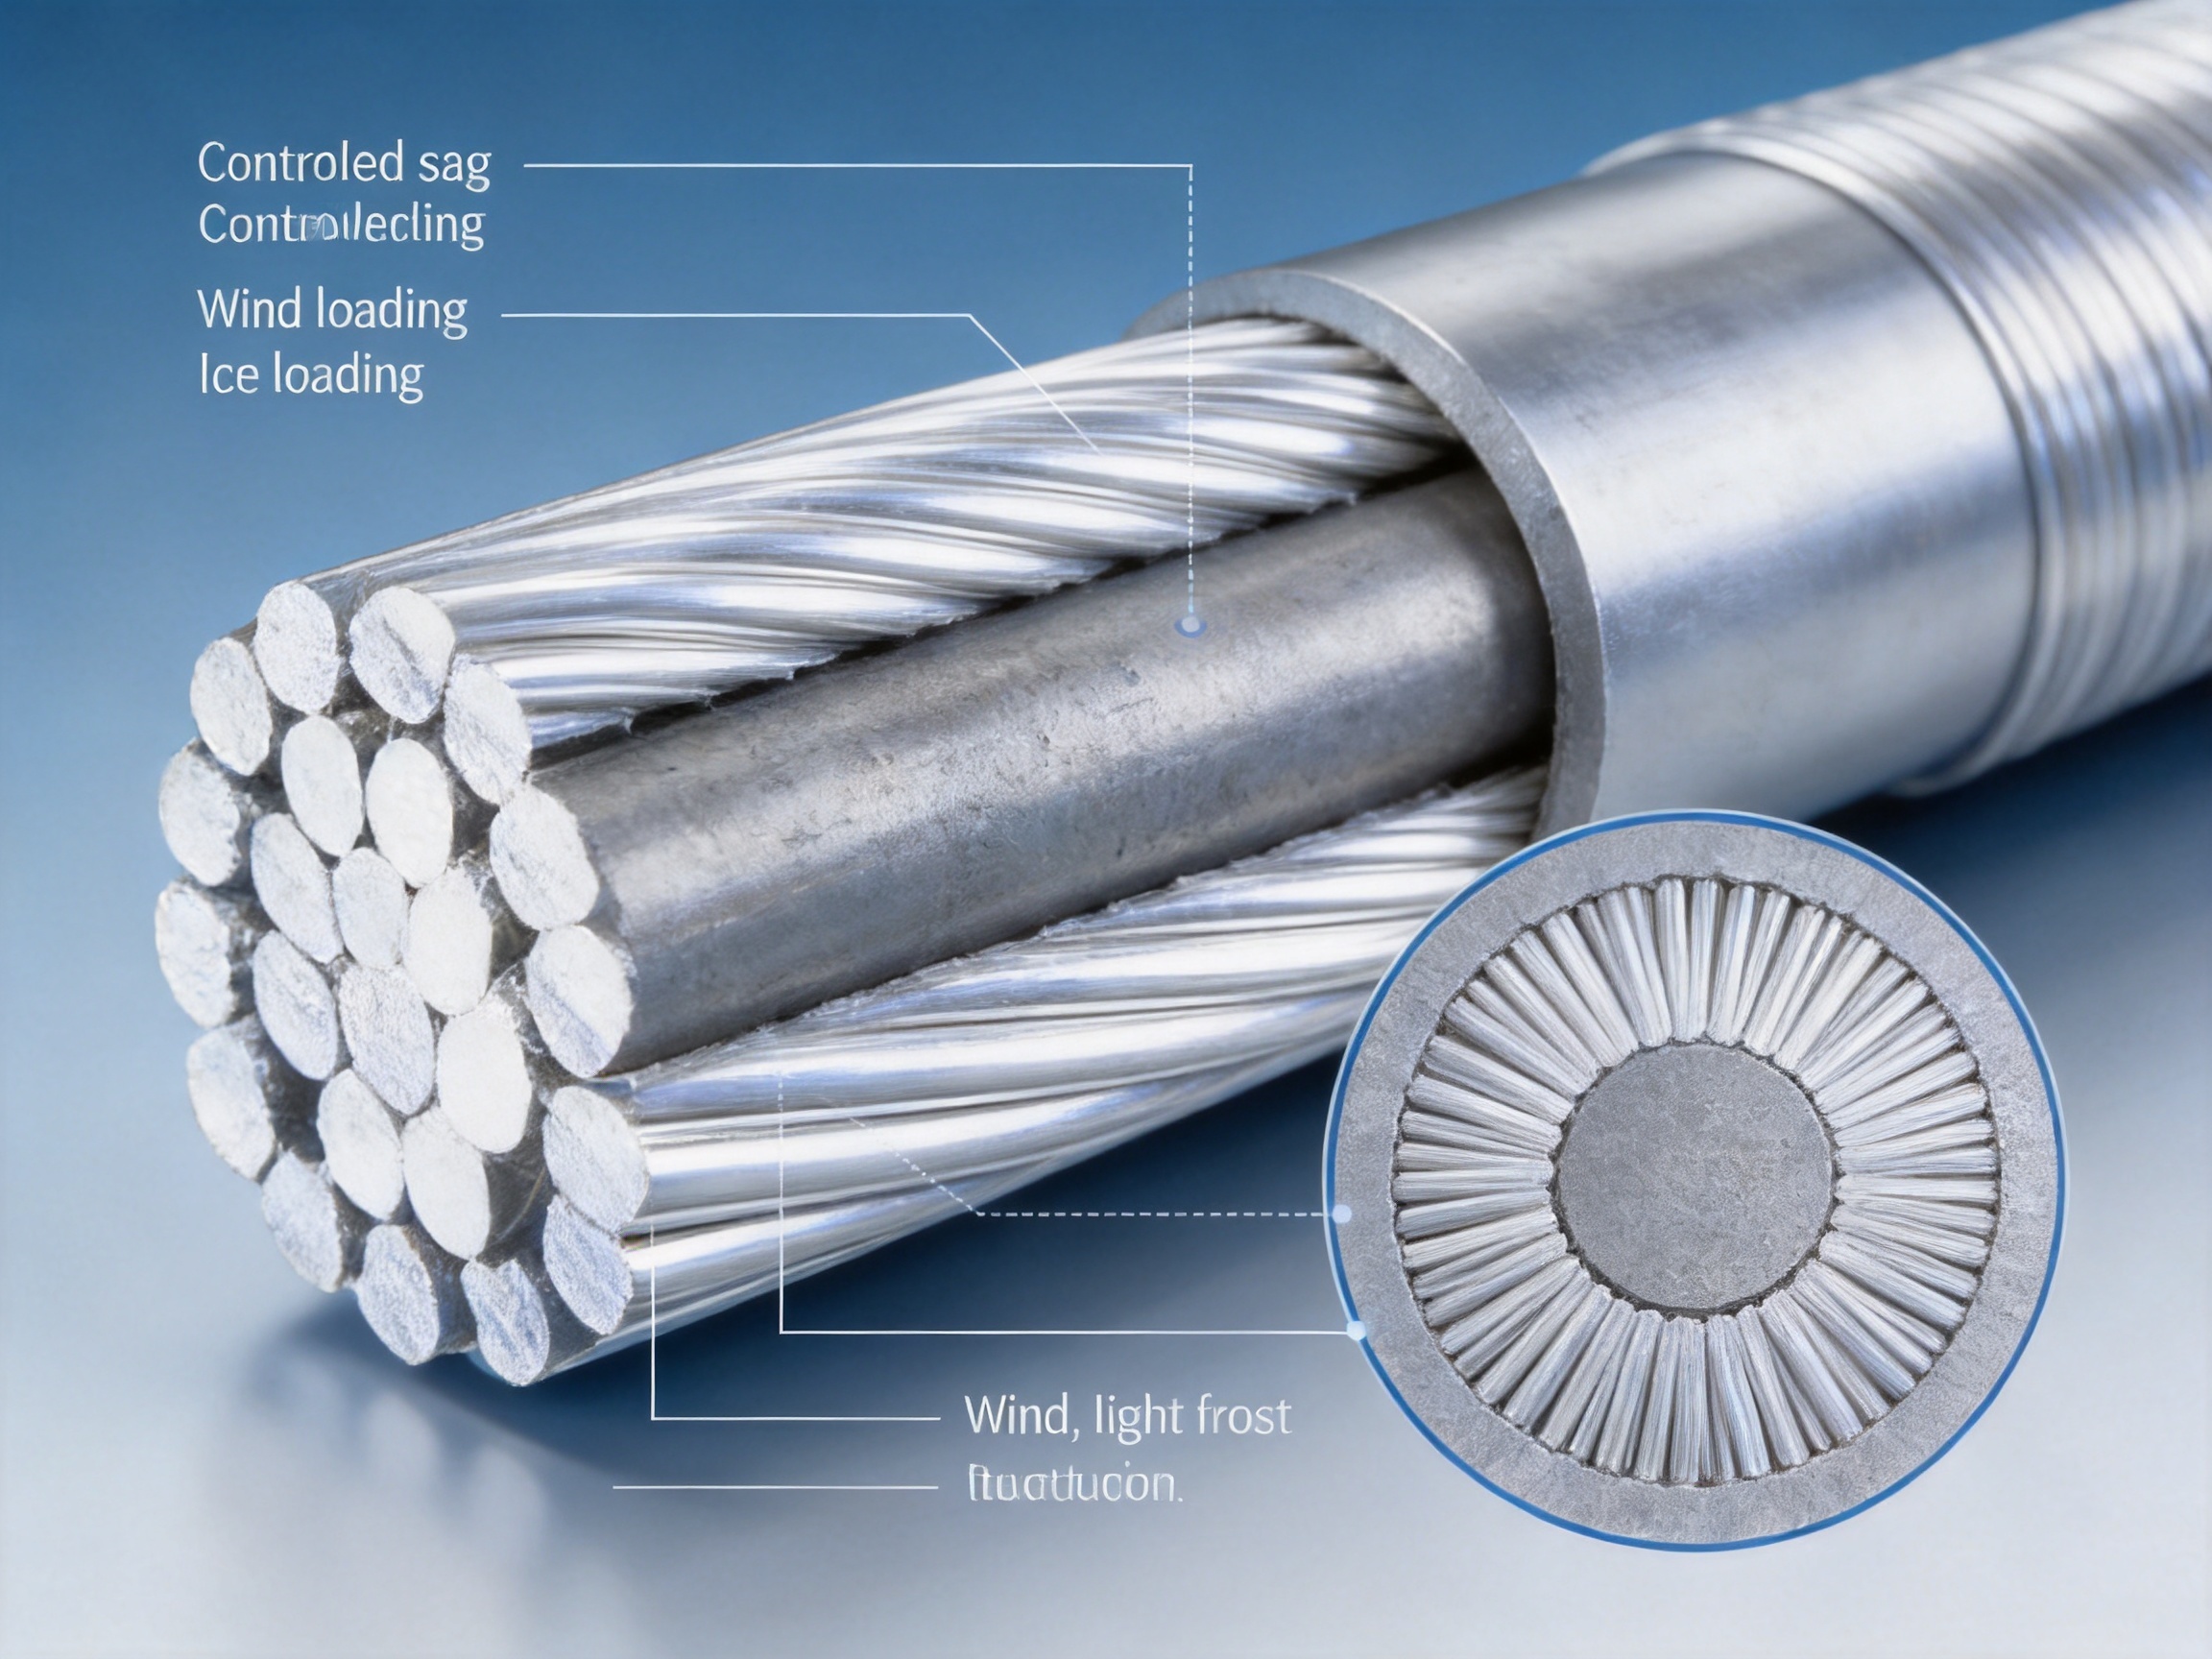
The aluminum strands form the outer conductive layers. These layers are arranged with controlled geometry to provide a stable circular profile and efficient current-carrying area. Inside them, the steel core supports the conductor against tensile loads. The steel core also limits excessive elongation and helps maintain the designed sag and tension relationship during service.
In the supplied product range, the aluminum component may contain from 6 to 30 individual strands, while the steel core may contain from 1 to 7 strands. Aluminum strand diameters range approximately from 1.50 mm to 4.72 mm, and steel-core strand diameters range approximately from 1.50 mm to 3.60 mm. These configurations allow the conductor to be selected according to required current capacity, tensile loading, installation length, and environmental conditions.
Although reinforcing steel aluminum strand is widely associated with overhead electrical conductors, it can also serve as a specialized damping wire in hardware connection assemblies. One example is its use with damping-type end caps and related connection hardware. In such applications, the conductor must provide dependable mechanical behavior, controlled flexibility, and compatibility with the connected electrical system.
Reinforcing Steel Aluminum Strand
2. Main Technical Specifications
The technical performance of a reinforcing steel aluminum strand depends on the aluminum area, steel-core area, strand arrangement, material quality, stranding pitch, surface condition, and manufacturing consistency. Standardized specifications enable designers to compare products and select a conductor that satisfies both electrical and mechanical requirements.
The available nominal cross-section range extends from 10/2 mm² to 240/30 mm². This range covers relatively compact conductors for moderate loads as well as larger conductors intended for higher current and greater mechanical duty. The calculated total cross-sectional area ranges approximately from 12.37 mm² to 275.96 mm². The corresponding outer diameter ranges from approximately 4.50 mm to 21.60 mm.
Depending on the specification, the direct-current resistance is stated at values ranging from no more than approximately 2.706 Ω/km for the smaller sizes to approximately 0.1410 Ω/km for the larger sizes. The calculated tensile strength ranges from approximately 4,012 N to 91,120 N, while calculated weight ranges from approximately 42.9 kg/km to 964.2 kg/km.
These values are reference design parameters rather than a substitute for a project-specific data sheet. Actual selection should consider operating temperature, installation tension, span length, fault-current requirements, environmental exposure, connection hardware, and the applicable inspection standard. Before installation, the buyer and manufacturer should confirm the exact conductor designation, nominal area, lay direction, delivery length, surface treatment, and acceptance criteria.
| Parameter | Typical Product Range | Engineering Significance |
|---|---|---|
| Nominal cross-section | 10/2 mm² to 240/30 mm² | Defines the approximate aluminum and steel areas |
| Aluminum strand count | 6 to 30 strands | Influences conductive area, flexibility, and outer geometry |
| Steel-core strand count | 1 to 7 strands | Influences tensile strength and core stability |
| Aluminum wire diameter | Approximately 1.50 mm to 4.72 mm | Supports standardized construction and dimensional control |
| Steel wire diameter | Approximately 1.50 mm to 3.60 mm | Determines part of the mechanical load capacity |
| Calculated cross-sectional area | Approximately 12.37 mm² to 275.96 mm² | Supports electrical and mechanical calculations |
| Outer diameter | Approximately 4.50 mm to 21.60 mm | Required for fittings, clearances, and installation tools |
| Calculated tensile strength | Approximately 4,012 N to 91,120 N | Indicates resistance to installation and service tension |
| Calculated weight | Approximately 42.9 kg/km to 964.2 kg/km | Used for support, sag, transport, and handling calculations |
| Typical delivery length | Generally less than 2,000 m | Supports manageable transportation and installation planning |
The product is designed for standardized production rather than unrestricted custom variation. This is important because conductor geometry affects connector compatibility, electrical resistance, mechanical behavior, and long-term stability. A controlled specification allows construction contractors, equipment manufacturers, and engineering consultants to use consistent calculation methods across projects.
3. Material Composition and Functional Design
3.1 Aluminum Conductive Layers
The aluminum strands carry most of the electrical current. According to the supplied technical information, electrical-grade aluminum with a purity of at least 99.7% may be used, with conductivity reaching more than 61% IACS after controlled annealing. High-purity aluminum helps reduce electrical resistance and provides a consistent basis for conductor design.
Aluminum also contributes to corrosion resistance. When exposed to air, aluminum naturally forms a thin oxide layer that protects the underlying metal. This characteristic is valuable in outdoor and industrial environments. However, surface oxidation, contact pressure, connector design, and galvanic interaction must still be considered when the strand is installed with other metals.
The aluminum strands are manufactured and assembled with controlled diameters. Consistent wire diameter helps maintain the designed outer profile and reduces variation between production lots. It also supports predictable connector compression and more uniform stress distribution during stranding and service.
3.2 Galvanized Steel Core
The steel core provides the mechanical reinforcement that distinguishes this product from an all-aluminum conductor. The core absorbs a significant portion of tensile loading and improves resistance to sag, elongation, and mechanical deformation. This allows the conductor to handle demanding installation conditions and longer spans when the overall system design permits.
The supplied product information specifies a galvanized steel core with a zinc coating weight complying with a minimum value of approximately 300 g/m². Galvanization improves resistance to atmospheric corrosion and helps protect the steel substrate. The coating must remain continuous and sufficiently bonded during drawing, stranding, handling, and connection.
Steel-core construction does not eliminate the need for correct installation. Excessive bending, improper gripping, unsuitable pulling tension, or damaged galvanized surfaces may reduce service life. For this reason, the product should be handled with appropriate stringing equipment, compatible sheaves, approved clamps, and installation procedures suitable for steel-reinforced conductors.
3.3 Composite Balance
The product’s value lies in the balance between the two materials. Increasing the aluminum area generally improves current-carrying capability but also increases weight and diameter. Increasing the steel area improves mechanical strength but may affect the ratio of conductive area to total weight. The selected design must therefore reflect the actual priorities of the application.
For overhead transmission and distribution systems, engineers commonly evaluate electrical capacity, permissible temperature, tensile strength, sag, wind loading, ice loading, vibration, and corrosion exposure together. For hardware connection or damping applications, the emphasis may shift toward mechanical stability, compatibility with end fittings, flexibility, and resistance to repeated vibration.
4. Manufacturing Process and Quality Control
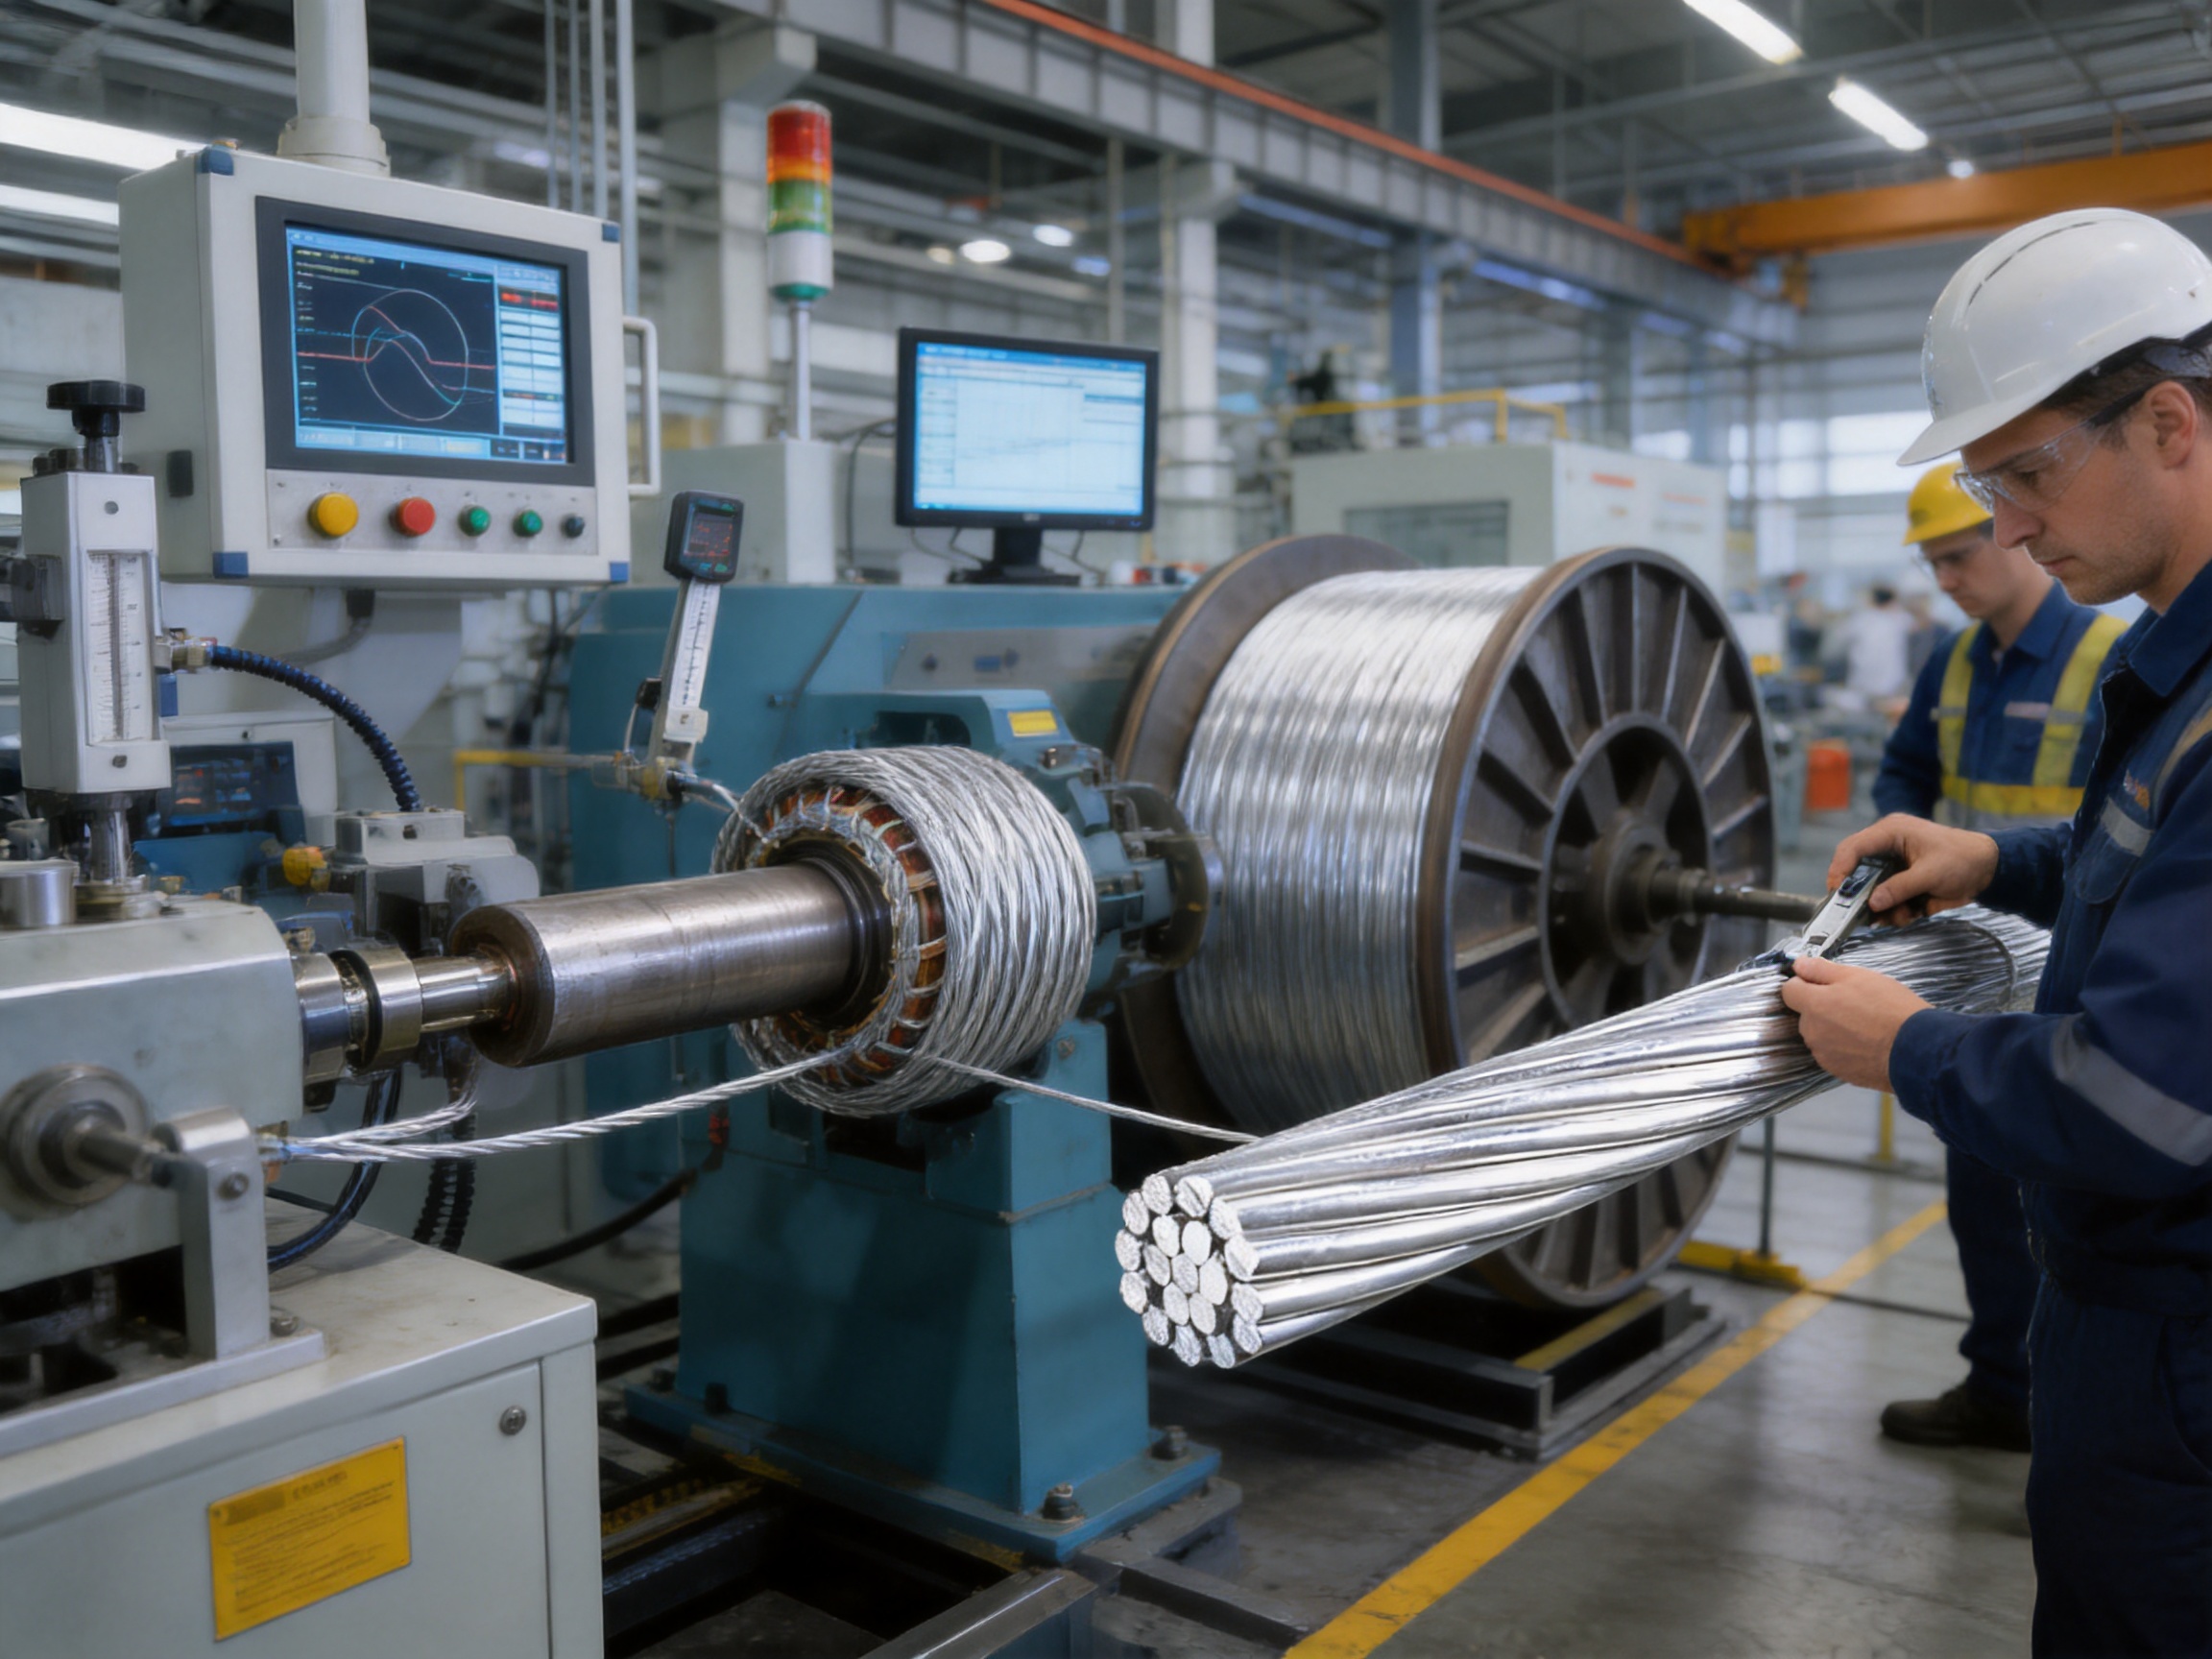
The performance of reinforcing steel aluminum strand depends heavily on manufacturing discipline. A conductor with the correct nominal area may still perform poorly if the materials are inconsistent, the lay is irregular, the steel core is damaged, or the aluminum strands are not properly compacted around the core. Jiangsu Wopeng Power Technology Co., Ltd. emphasizes controlled production processes, engineering supervision, and standardized inspection across its power-transmission product portfolio.
4.1 Incoming Material Inspection
Production begins with the inspection of aluminum wire, steel wire, zinc-coated steel components, packaging materials, and related production inputs. Typical checks include diameter, surface condition, tensile properties, elongation, electrical resistance, coating condition, and material documentation.
Incoming inspection is especially important for the steel core. The steel must provide adequate tensile strength while remaining suitable for drawing and stranding. The zinc coating should be continuous and free from defects that could expose the steel prematurely to moisture or contaminants. Aluminum wire must also meet the specified purity, diameter, surface, and conductivity requirements.
Material identification and batch traceability support quality management. When each production batch can be connected to its raw material records, test results, and process parameters, potential deviations can be investigated more efficiently. This also provides customers with better documentation for project acceptance and future maintenance.
4.2 Wire Drawing and Dimensional Control
Wire drawing reduces the input material to the required diameter while improving dimensional uniformity. The drawing process must be controlled to avoid excessive work hardening, surface damage, cracking, or uncontrolled variation. Drawing dies, lubrication, drawing speed, reduction ratios, and intermediate treatment all influence the final wire condition.
For aluminum wire, controlled annealing may be used to restore suitable electrical and mechanical properties after drawing. The objective is to obtain a reliable combination of conductivity, flexibility, and strand stability. For steel wire, process control must preserve tensile performance and protect the galvanized surface where applicable.
Dimensional checks are performed at appropriate stages. Measuring wire diameter before stranding helps prevent cumulative errors in the completed conductor. Even small variations can affect the outer diameter, interstrand contact, lay geometry, and connector fit.
4.3 Core Stranding
The steel core may be formed from a single wire or multiple steel wires. In a multi-wire core, the strands are arranged concentrically with controlled pitch and tension. The process must produce a stable core that does not loosen, buckle, or shift during subsequent aluminum stranding.
Core tension is carefully managed. Excessive tension may create unwanted residual stress, while insufficient tension can result in an unstable or poorly formed core. The production line must also maintain alignment between the core and the surrounding aluminum layers.
4.4 Aluminum Layer Stranding
After core preparation, aluminum strands are wrapped around the steel core in one or more layers. The strand count, direction, pitch, and tension are selected according to the specified conductor construction. Uniform pitch helps distribute mechanical loads and gives the finished product a regular surface profile.
Controlled pre-twisting can reduce the tendency of the strands to loosen after production. This is particularly important during pay-off, transport, installation, and connection. The supplied product information indicates that a controlled pre-twisting process is used to improve structural stability and reduce strand loosening under long-term loading.
Proper tension balance between the aluminum layers and steel core is essential. If the layers are too loose, the conductor may exhibit instability and uneven load transfer. If they are too tight, internal stress may increase and flexibility may decrease. Modern stranding equipment, calibrated tension systems, and experienced operators help maintain the required balance.
4.5 Final Inspection
Finished conductors are inspected for outer diameter, surface condition, lay length, strand count, mass, electrical resistance, tensile performance, and overall construction. Visual examination can identify broken wires, excessive protrusion, damaged coatings, irregular lay, and surface contamination.
Routine inspection should be supported by documented test procedures. Depending on customer requirements and the applicable standard, tests may include direct-current resistance measurement, tensile testing, dimensional verification, coating inspection, elongation testing, and examination of the finished coil or drum.
Jiangsu Wopeng Power Technology Co., Ltd. operates production lines that include vacuum casting systems, CNC machining equipment, and automated assembly technologies for its broader busbar and power-equipment product range. This manufacturing environment supports precise fabrication, repeatable component quality, and coordinated production of conductors, connectors, insulation systems, and related power-transmission assemblies where required.
5. Technical Advantages Compared with Alternative Conductors
The most important advantage of reinforcing steel aluminum strand is its ability to combine useful conductivity with significantly improved mechanical performance. An all-aluminum conductor may be lighter and simpler, but it generally offers lower tensile strength. A steel-only conductor offers high mechanical strength but poor electrical conductivity. The composite arrangement provides a practical middle ground.
5.1 Higher Tensile Capability
The steel core allows the conductor to withstand greater tensile forces than a comparable all-aluminum design. This is valuable in long-span transmission, high-tension distribution, ground-wire applications, and mechanically demanding connection assemblies. Higher tensile capability can reduce excessive sag and improve stability under wind or ice loading.
Mechanical performance must always be considered together with the complete support system. Tower strength, insulator arrangement, clamp design, foundation conditions, and local weather loads remain important. The conductor’s higher tensile capability is an engineering advantage, not permission to exceed the safe working limits of the entire installation.
5.2 Improved Span Performance
For suitable projects, the product can support longer spans than an all-aluminum conductor of comparable electrical function. Longer spans may reduce the number of support structures, simplify route planning, and reduce some construction requirements. The actual economic benefit depends on terrain, tower design, access conditions, conductor size, and installation equipment.
5.3 Stable Electrical Function
Although the steel core is not the primary current-carrying element, the outer aluminum layers provide a large conductive area. The supplied technical information indicates aluminum conductivity above 61% IACS for the specified material condition. This supports low resistance and efficient current transmission when the conductor is correctly selected.
The product information also describes a measured skin-effect coefficient below 1.05 under high-frequency conditions, an increase in AC resistance controlled within 8%, short-circuit thermal capacity reaching 150 kA²·s, and conductivity degradation of no more than 2% after 100 thermal cycles. These values should be confirmed against the final product test report and the exact size ordered, but they illustrate the performance characteristics targeted by the design.
5.4 Environmental Resistance
Aluminum’s natural corrosion resistance and the galvanized steel core provide a useful combination for outdoor service. The product information states that the strand has been evaluated from -40°C to +80°C, with stable thermal-expansion behavior, resistance to a 30 mm ice coating load, retention of more than 95% tensile strength after 5,000 hours of salt-spray testing, and no significant surface degradation after 5,000 hours of ultraviolet aging.
Environmental performance depends on installation quality and local conditions. Coastal, industrial, polluted, or high-humidity environments may require additional inspection, special fittings, protective compounds, or adjusted maintenance intervals. Galvanic compatibility between the strand and connectors must be addressed through suitable hardware design.
5.5 Controlled Sag and Vibration Behavior
The steel core helps limit elongation and improves resistance to mechanical deformation. The supplied information states that creep deformation can be limited to within 0.05% under long-term operating loads and that structural reliability has been evaluated through a 2-million-cycle wind-induced vibration fatigue test.
Wind-induced vibration remains a system-level issue. Even a strong conductor can experience fatigue if the span, tension, wind profile, clamp geometry, and support arrangement create unfavorable vibration conditions. Dampers, armor rods, end caps, and other fittings should be selected according to the conductor design and local engineering requirements.
| Performance Factor | Reinforcing Steel Aluminum Strand | All-Aluminum Alternative | Practical Implication |
|---|---|---|---|
| Tensile strength | High because of the steel core | Low to moderate | Better support for long spans and high installation tension |
| Electrical conductivity | High through the aluminum layers | High through the full aluminum section | Selection depends on required resistance and total area |
| Weight | Moderate | Usually lighter for the same outside diameter | Support and transport calculations remain necessary |
| Sag control | Improved by steel reinforcement | More dependent on aluminum strength and temperature | Useful where clearance must be maintained |
| Corrosion behavior | Aluminum exterior with protected steel core | Aluminum exterior throughout | Connector compatibility and coating integrity are important |
| Mechanical durability | Suitable for high tension and vibration service | More limited under heavy mechanical loading | Can improve reliability in demanding applications |
6. Applications
6.1 Overhead Transmission Lines
Overhead transmission is the most recognized application for steel-reinforced aluminum conductors. The conductor must carry current across long distances while remaining mechanically stable between towers. Wind, ice, temperature changes, and its own weight all affect the line.
The steel core helps control sag and provides greater resistance to installation tension. In suitable designs, this can support longer spans and reduce the number of support structures. Engineers must still calculate conductor temperature, maximum sag, everyday tension, extreme weather loading, and clearance from buildings, roads, and other infrastructure.
6.2 High-Tension Distribution
Distribution networks may use reinforcing steel aluminum strand where mechanical reliability is more important than the minimum possible conductor weight. The product can help maintain conductor position in areas exposed to wind, ice, vibration, or difficult terrain.
A stable conductor reduces the risk of excessive sag, phase-to-phase contact, and clearance violations. It may also provide greater installation flexibility when routes require longer pulls or when access for additional support structures is limited.
6.3 Ground Wires and Shield Wires
At the top of transmission structures, steel-reinforced aluminum strands may be used as ground wires or shield wires. Their mechanical strength helps them withstand exposure and maintain a protective position above the phase conductors. In lightning-protection applications, the complete grounding path, tower grounding resistance, fittings, and connection method must be evaluated together.
6.4 Damping Wires and Hardware Connections
The product is also used as a damping wire in hardware connection applications, including damping-type end caps. In this role, the conductor may be required to absorb or manage mechanical vibration while maintaining a reliable connection with associated hardware.
Correct end fittings are essential. Compression connectors should be compatible with aluminum-to-steel transitions and should provide stable contact pressure without damaging the strands. Oxidation control, surface preparation, compression sequence, and tooling calibration all influence connection performance.
6.5 Wind Power and Industrial Power Equipment
Wind-power installations and industrial facilities often require compact, mechanically stable electrical connections. In these environments, vibration, space limitations, thermal cycling, and maintenance access can influence conductor selection. A steel-reinforced aluminum design may be useful where mechanical stability and controlled flexibility are needed.
Jiangsu Wopeng Power Technology Co., Ltd. supplies products for wind energy, substations, power generation, industrial manufacturing, rail transit, and large commercial facilities. Its broader product experience includes wind-power tubular busbars, low-voltage cast-resin busways, copper and aluminum tubular busbars, compact busbar systems, and sliding contact line systems. This application background helps connect conductor selection with the practical requirements of complete electrical systems.
7. Installation and Maintenance Guidance
7.1 Transportation and Storage
Reinforcing steel aluminum strand should be delivered on suitable reels or coils that protect it from impact, excessive bending, moisture, contamination, and flange damage. The delivery length is generally less than 2,000 meters, although the precise length should be confirmed with the order.
During storage, reels should be placed on stable surfaces and protected from standing water. The conductor ends should remain secured to prevent loosening. If the product is stored outdoors, suitable weather protection should be provided while allowing sufficient ventilation to reduce condensation.
7.2 Tension Stringing
Tension stringing is commonly used where conductor clearance and surface protection are important. The pulling equipment, tensioner, traveler, and sheaves should be selected for the conductor diameter and construction. Sheaves must be large enough and properly aligned to avoid excessive bending and strand damage.
Because the product contains a steel core, it can handle higher installation tension than many all-aluminum conductors. Nevertheless, the allowable tension must be based on the approved installation design. Exceeding the elastic limit may create permanent deformation, alter sag behavior, or damage the aluminum layers.
7.3 Connector Compatibility
Connections should use fittings designed for the exact conductor construction. Aluminum-to-steel transition connectors, compression sleeves, end caps, and damping hardware must be compatible with the aluminum area, steel-core diameter, outer diameter, and stranding arrangement.
Improper connection methods can increase contact resistance, cause local overheating, damage the steel core, or reduce mechanical strength. Compression tools should be calibrated, dies should match the connector specification, and the compression sequence should follow the approved installation procedure.
7.4 Inspection During Service
Routine inspection should examine conductor surface condition, fittings, clamps, end caps, vibration dampers, support points, and signs of corrosion or mechanical wear. Coastal and industrial environments may require more frequent inspections because salt, chemical pollutants, and moisture can accelerate surface degradation.
Inspectors should look for broken aluminum strands, displaced layers, unusual discoloration, loose hardware, damaged galvanizing, connector heating, and abnormal vibration marks. Thermal imaging, resistance measurement, and visual inspection can be combined where appropriate.
8. Why Choose an Experienced Manufacturer
Purchasing a conductor based only on nominal cross-section can create avoidable risks. Manufacturing consistency, material traceability, process control, test documentation, and technical support are equally important. An experienced manufacturer can help ensure that the conductor is compatible with the intended fittings and operating environment.
Jiangsu Wopeng Power Technology Co., Ltd. was founded in 2018 as a specialized high-tech enterprise focused on high- and low-voltage busbar systems. The company has developed capabilities in engineering design, production, quality inspection, and project support. Its product range covers systems from low voltage to 35 kV, including epoxy-resin vacuum-cast tubular busbars, low-voltage cast-resin busway, copper and aluminum tubular busbars, wind-power tubular busbars, compact busbar systems, and sliding contact line systems.
This product breadth is valuable because reinforcing steel aluminum strand may be used as part of a larger electrical installation rather than as an isolated commodity. A manufacturer familiar with complete power-transmission assemblies can better understand insulation coordination, connection interfaces, mechanical support, thermal behavior, and installation constraints.
The company’s modern manufacturing facilities include vacuum casting systems, CNC machining equipment, and automated assembly technologies. Vacuum casting supports the production of high-quality insulated busbar components by helping reduce voids and improve resin encapsulation. CNC machining supports dimensional precision for metallic components, connectors, housings, and interfaces. Automated assembly improves repeatability and reduces variation in production operations.
Wopeng applies standardized inspection procedures that include high-voltage testing, insulation testing, mechanical verification, and routine quality checks for relevant products. Collaboration with third-party testing institutions provides independent validation where required. This combination of internal control and external verification strengthens customer confidence in safety and performance.
The company’s products operate across more than 17 provinces and major industrial sectors in China. This field experience exposes the engineering and production teams to diverse conditions, including substations, industrial plants, wind-power facilities, transportation infrastructure, commercial buildings, and other high-current applications.
9. Customization and Project Support
Different projects may require different conductor areas, delivery lengths, packaging methods, connector arrangements, inspection documents, or environmental requirements. A project-oriented manufacturer should be able to review the application before production and confirm the technical details in writing.
Potential customization and engineering-confirmation items include nominal aluminum and steel areas, aluminum and steel strand diameters, number of strands, lay direction, lay length, outer diameter, electrical resistance, tensile strength, drum size, delivery length, marking, coating requirements, and testing documentation.
For busbar-related applications, additional requirements may include insulation type, rated voltage, rated current, short-circuit withstand, enclosure arrangement, support spacing, thermal expansion, connection structure, and installation orientation. Jiangsu Wopeng Power Technology Co., Ltd. can coordinate these considerations across its busbar and power-equipment product capabilities.
Technical communication should also cover the installation environment. Information about altitude, ambient temperature, solar radiation, humidity, salt exposure, industrial pollution, wind speed, ice loading, vibration, and seismic conditions may affect conductor or busbar selection. Supplying this information early helps avoid redesign and improves the reliability of the final system.
10. Frequently Asked Questions
Q1: What is reinforcing steel aluminum strand?
It is a composite stranded conductor made from aluminum strands surrounding a steel core. The aluminum provides most of the electrical conductivity, while the steel core supplies mechanical reinforcement and tensile strength.
Q2: What standard applies to the supplied product?
The product is described as conforming to GB1179-83. Project requirements may also reference other national, regional, or international standards. The applicable standard should be confirmed before ordering because requirements for dimensions, resistance, strength, testing, and acceptance may differ.
Q3: What nominal sizes are available?
The stated nominal cross-section range is 10/2 mm² to 240/30 mm². The exact availability, construction, delivery length, and test requirements should be confirmed for each order.
Q4: Why is a steel core used?
The steel core improves tensile strength, limits elongation, supports longer spans, and helps the conductor resist sag and mechanical loads caused by wind, ice, installation tension, and vibration.
Q5: Is the steel core the main current-carrying component?
No. The aluminum layers carry most of the electrical current. The steel core is primarily a mechanical reinforcement element, although its presence contributes to the total cross-sectional structure and overall electrical characteristics.
Q6: Can the product be used in coastal areas?
It can be used in coastal environments when the conductor, fittings, coatings, and maintenance plan are selected appropriately. Aluminum and galvanized steel provide useful corrosion resistance, but salt exposure can still affect surfaces and connections. Regular inspection and compatible hardware are recommended.
Q7: Can it be used with damping-type end caps?
Yes. The supplied application information identifies damping wire use with hardware such as damping-type end caps. The end cap or connector must be designed for the exact conductor construction and installed using the approved procedure.
Q8: How should the conductor be installed?
Installation should use suitable reels, sheaves, tensioners, grips, compression tools, and fittings. The approved pulling tension, minimum bending radius, sag-tension data, and connector instructions must be followed. The steel core does not make the conductor immune to excessive bending or improper handling.
Q9: What information should be provided when requesting a quotation?
Customers should provide the required nominal size, application, voltage or current conditions, span or mechanical loading, environmental conditions, delivery length, packaging preference, applicable standard, connection hardware, inspection requirements, and destination. Drawings or existing system information are helpful for confirming compatibility.
Q10: What makes an experienced manufacturer valuable?
An experienced manufacturer can control raw materials, wire dimensions, stranding tension, lay geometry, inspection, packaging, and technical documentation. A company with broader busbar and power-equipment experience can also help integrate the conductor into a complete electrical system.
11. Conclusion
Reinforcing steel aluminum strand is a practical composite conductor for applications requiring both electrical performance and mechanical strength. Its aluminum layers provide efficient current transmission, while its galvanized steel core improves tensile capacity, sag control, vibration resistance, and long-span capability.
The available range from 10/2 mm² to 240/30 mm² allows engineers to select a suitable balance of conductive area, mechanical strength, diameter, weight, and installation performance. Standardized dimensions and clearly defined technical parameters support design calculations, procurement, construction, and maintenance.
The product’s advantages are maximized when manufacturing quality and system engineering are treated as equally important. Controlled aluminum and steel materials, precise drawing, stable core formation, uniform stranding, calibrated inspection, and suitable packaging all contribute to dependable service. Connector compatibility, correct installation tension, environmental assessment, and routine maintenance are also essential.
With experience in high- and low-voltage busbar systems, tubular busbars, cast-resin products, wind-power applications, and industrial power equipment, Jiangsu Wopeng Power Technology Co., Ltd. provides more than a standard conductor supply function. Its manufacturing infrastructure, engineering team, inspection procedures, and project experience support the development of reliable power-transmission solutions for substations, generation facilities, industrial plants, rail transit, renewable-energy projects, and commercial infrastructure.
For projects requiring a reinforced aluminum conductor, the correct approach is to evaluate electrical, mechanical, environmental, and installation requirements together. When the conductor size, fittings, manufacturing process, and operating conditions are properly matched, reinforcing steel aluminum strand can provide a durable and efficient solution for modern power-transmission systems.
References
1. GB1179-83, Aluminium Stranded Conductors and Steel-Reinforced Aluminium Stranded Conductors.
2. ASTM B399/B399M, Standard Specification for Concentric-Lay-Stranded Aluminum-Alloy 6201-T81 Conductors.
3. IEC 61089, Round Wire Concentric Lay Overhead Electrical Stranded Conductors.
4. International Annealed Copper Standard, reference conductivity convention for electrical conductor comparison.
5. General engineering practices for overhead line conductor selection, sag-tension calculation, vibration control, and compression connector installation.
6. Manufacturer-provided technical information for reinforcing steel aluminum strand, tubular busbars, cast-resin busbar systems, and related power-transmission equipment.
Product: Reinforcing Steel Aluminum Strand


-
 +86-180 3625 3000
-
 admin@wpbusbar.com
-
 No. 8, Yanjin Road, Chengxi Industrial Park, Shanyang Town, Baoying County, Yangzhou City, Jiangsu Province, China
Copyright © Jiangsu Wopeng Power Technology Co., Ltd.
All Rights Reserved.
 Custom Insulated Bus Bar Manufacturer
Tubular Busbar System Factory