

 EN

 English
 русский
 Français
 Español
 عربى
Epoxy Resin Casting Tubular Bus Bar: Advanced Insulation, Reliable Power Transmission, and Customized Manufacturing
Content
- 1 1. What Is an Epoxy Resin Casting Tubular Bus Bar?
- 2 2. Main Construction of the Product
- 3 3. Advanced Vacuum Casting and Manufacturing Process
- 4 4. Technical Advantages Compared with Conventional Solutions
- 5 5. Performance Comparison with Other Insulated Bus Bar Systems
- 6 6. Operating Environmental Conditions
- 7 7. Typical Application Solutions
- 8 8. Intelligent Monitoring and Digital Maintenance
- 9 9. Manufacturing Strengths and Quality Management
- 10 10. Selection Guidelines for Buyers and Engineers
- 11 11. Installation and Commissioning Considerations
- 12 12. Frequently Asked Questions
- 12.1 Q1: What is the main advantage of epoxy resin casting tubular bus bar?
- 12.2 Q2: What conductor materials are available?
- 12.3 Q3: What copper quality is specified for the product?
- 12.4 Q4: How long can the product operate?
- 12.5 Q5: Can the tubular busbar be used outdoors?
- 12.6 Q6: What is the maximum suspension span?
- 12.7 Q7: How are intermediate connections made?
- 12.8 Q8: How are terminal connections made?
- 12.9 Q9: Is the product suitable for high-humidity environments?
- 12.10 Q10: What tests should be performed before energization?
- 12.11 Q11: Can the product be customized?
- 12.12 Q12: What makes an experienced manufacturer important?
- 13 13. Why Choose a Specialized Tubular Busbar Manufacturer?
- 14 14. Conclusion
- 15 References
- 16 Product: Epoxy Resin Casting Tubular Bus Bar
Modern electrical infrastructure requires power transmission equipment that can carry high currents safely, withstand demanding environmental conditions, and maintain stable performance over a long operating life. As substations, industrial plants, renewable energy facilities, transportation systems, commercial buildings, and data centers become more complex, traditional open conductors and conventional cable arrangements may not provide the required combination of insulation, mechanical protection, compact installation, and operational reliability.
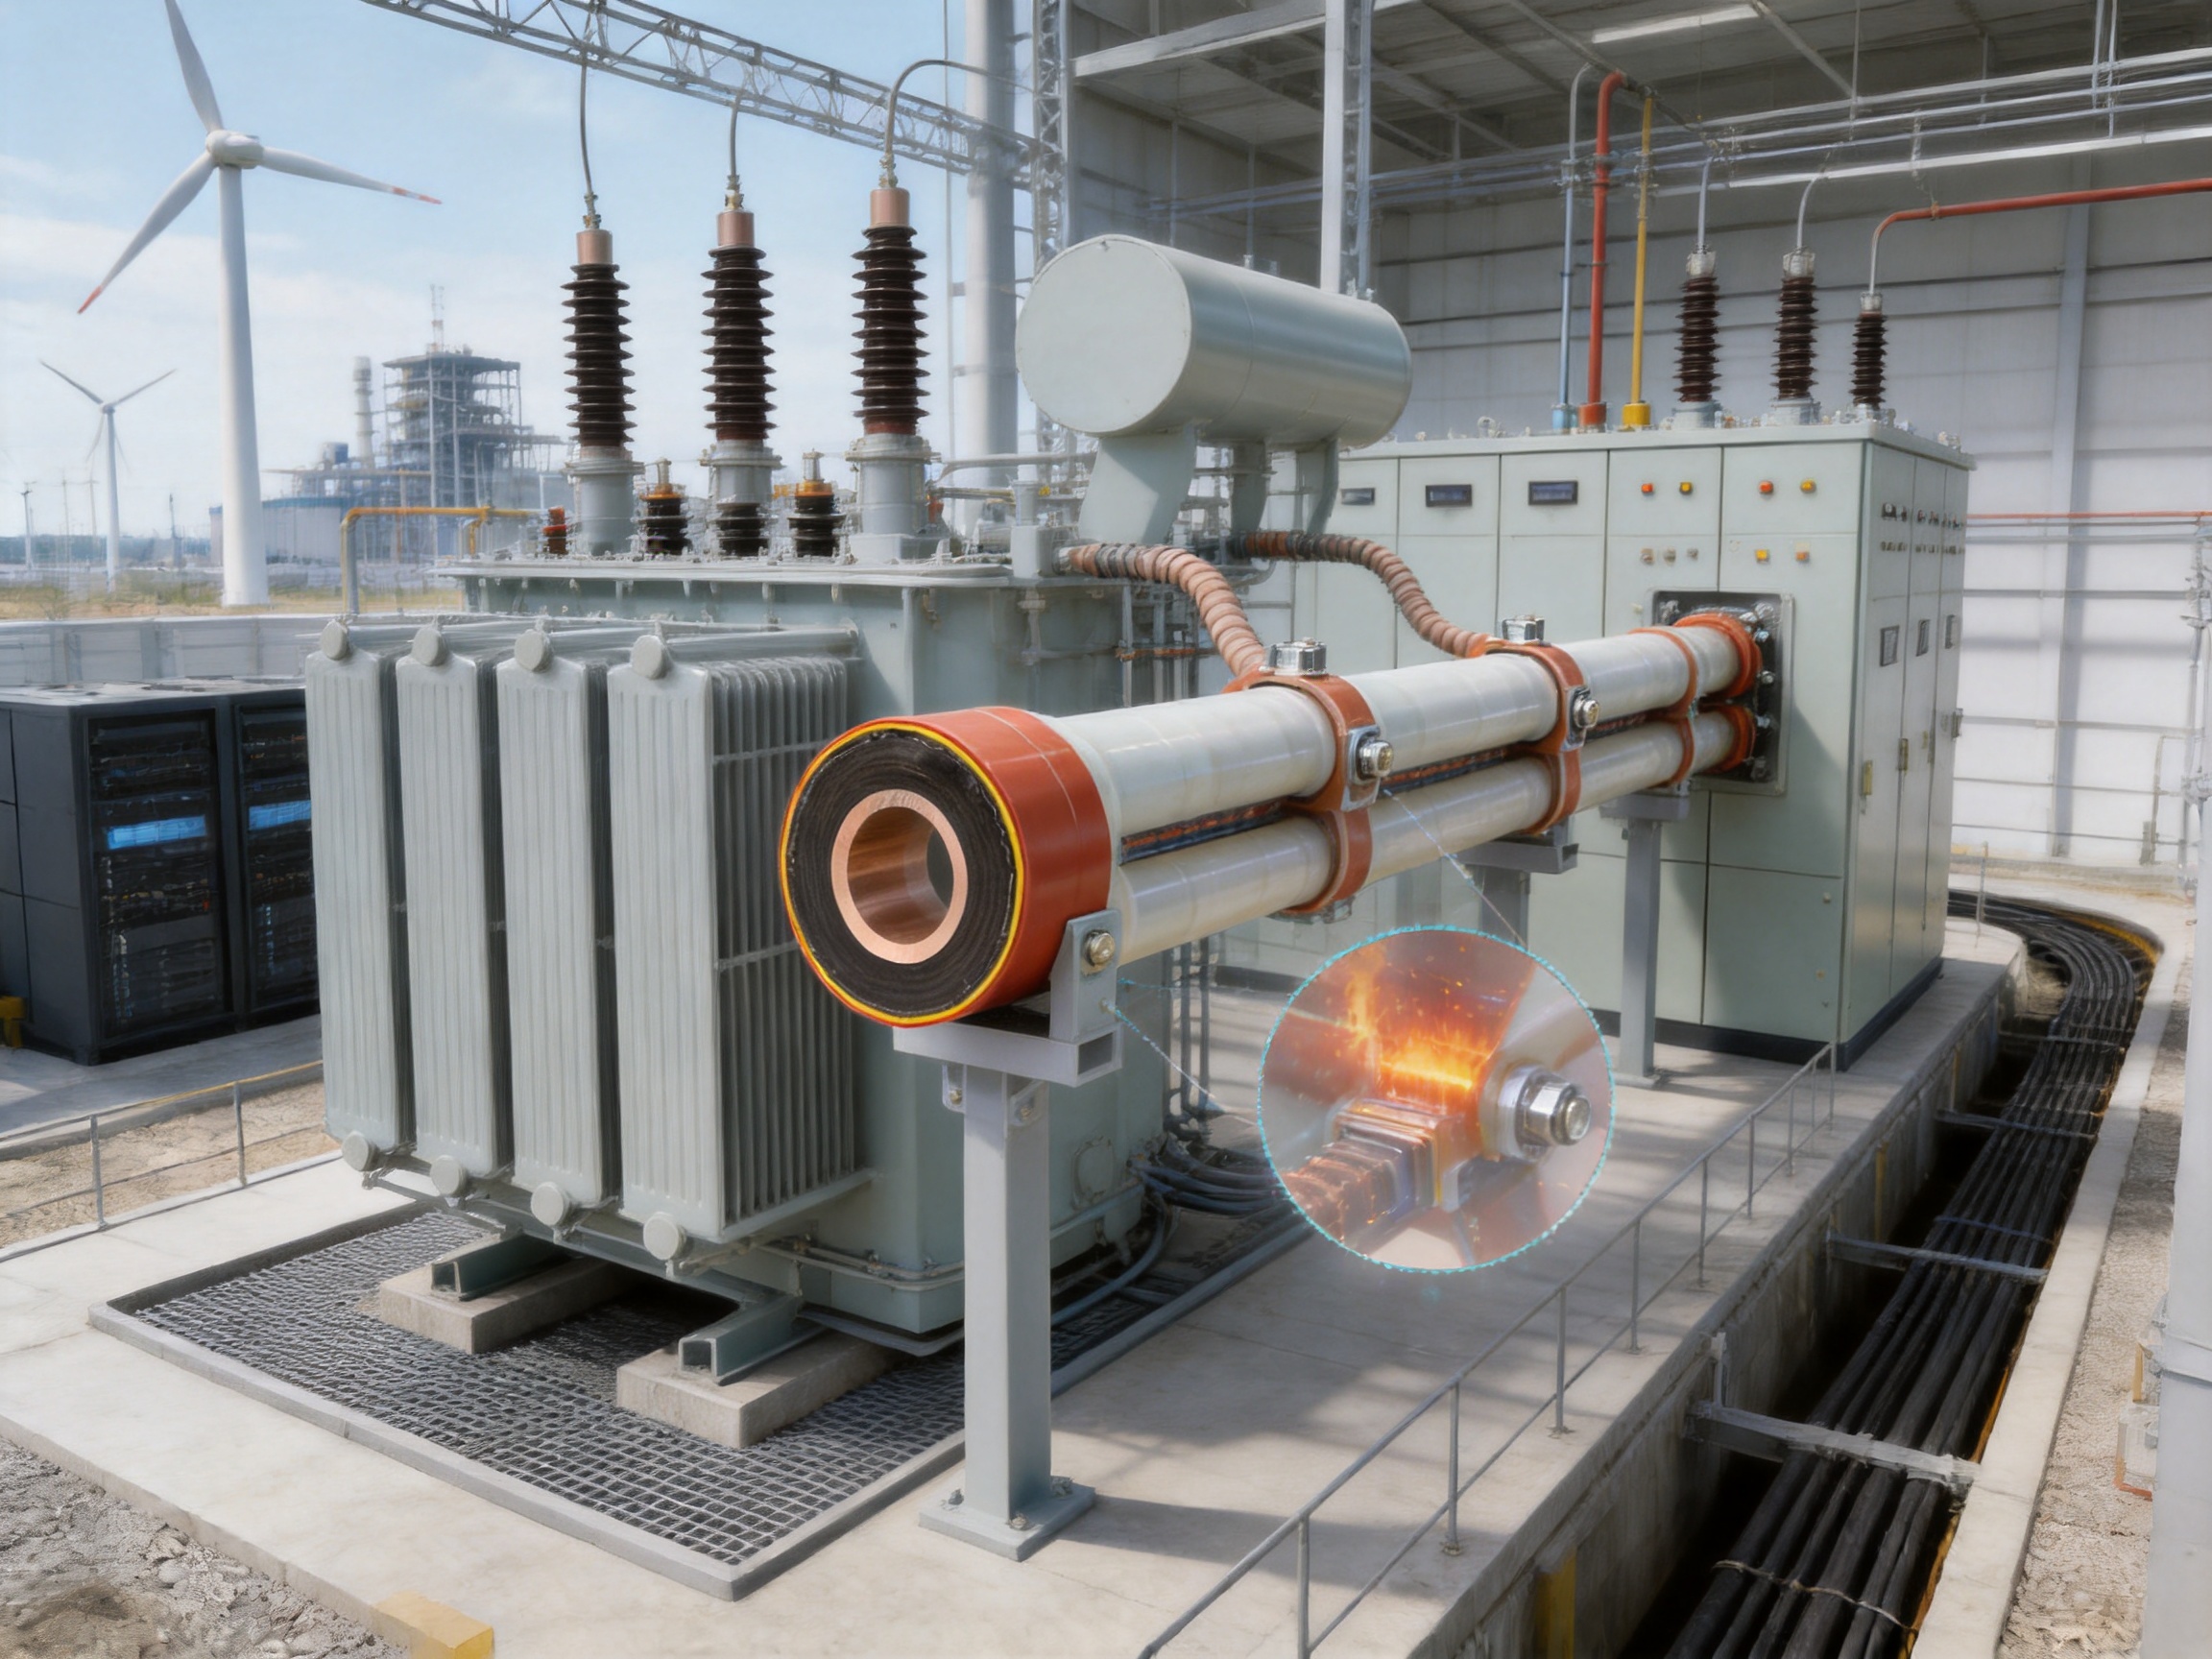
Epoxy resin casting tubular bus bar is designed to address these requirements. It combines a tubular copper or aluminum conductor with a fully molded insulation system, shielding layers, protective materials, and engineered connection components. Unlike a loosely assembled conductor system, a cast tubular bus bar is manufactured as an integrated structure. The conductor, insulation, semiconductive layers, metal shielding, and external protective layer work together as one coordinated product.
This integrated construction provides important advantages over many conventional bus bar and cable solutions. It reduces the number of exposed interfaces, improves resistance to moisture and contamination, strengthens mechanical protection, and supports reliable operation in confined or technically demanding installation areas. It can also simplify routing between transformers, switchgear, control rooms, and other high-current equipment.
Jiangsu Wopeng Power Technology Co., Ltd. manufactures high- and low-voltage busbar systems, including epoxy resin vacuum-cast tubular busbars, low-voltage cast resin busways, copper and aluminum tubular busbars, wind power tubular busbars, compact busbar systems, and sliding contact line systems. Through vacuum casting, automated mixing, pressure injection, high-temperature curing, CNC processing, and standardized testing, the company provides customized solutions for power transmission applications.
This article explains the structure, manufacturing technology, technical advantages, application scenarios, environmental capabilities, connection methods, quality controls, and selection considerations associated with epoxy resin casting tubular bus bar systems.
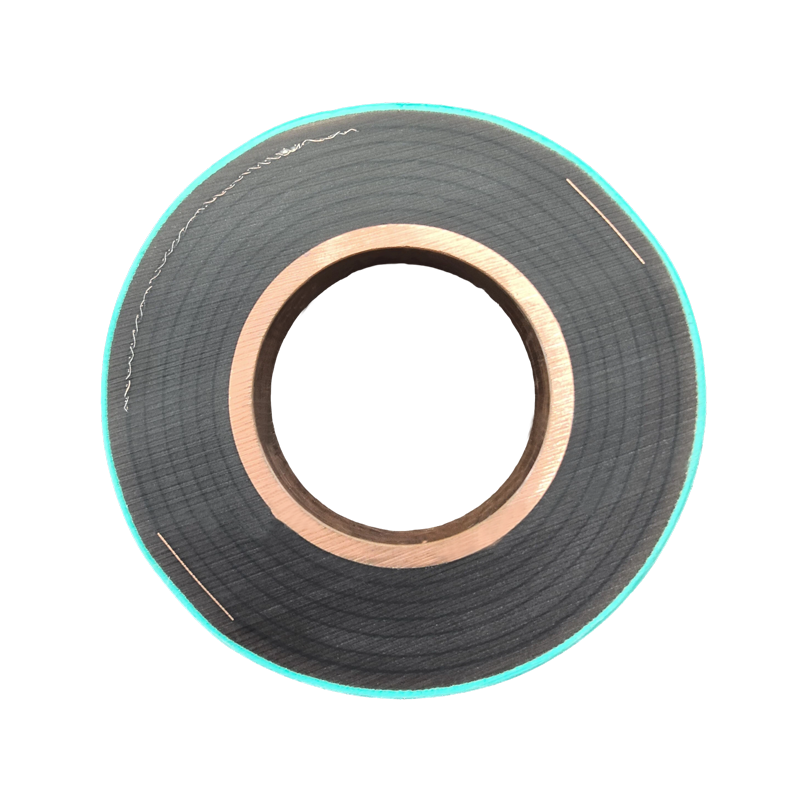
Epoxy Resin Casting Tubular Bus Bar
1. What Is an Epoxy Resin Casting Tubular Bus Bar?
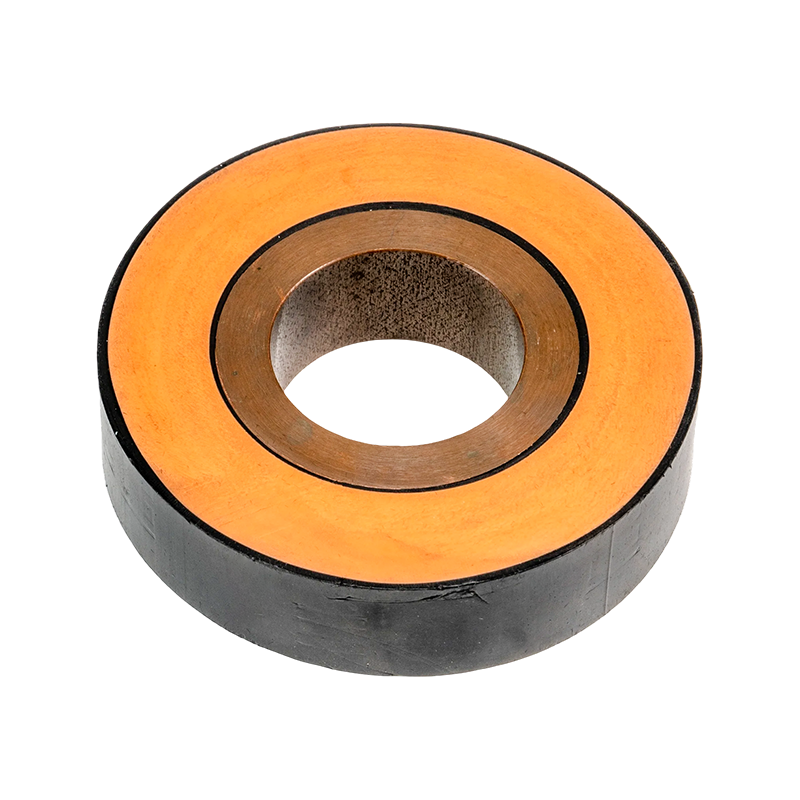
An epoxy resin casting tubular bus bar is an insulated power transmission component manufactured by placing a conductive tube or tubular conductor inside a precision-designed insulation system and then casting epoxy resin around the assembly. The casting process creates a solid, mechanically stable product that is not intended to be disassembled into separate operational layers.
The conductor is generally produced from high-purity copper or aluminum alloy, depending on the required current rating, weight, conductivity, installation conditions, and project budget. For high-performance copper products, the specified material may be TZ7 or a higher-grade oxygen-free copper, with copper content of at least 99.90 percent. The conductor’s tubular configuration offers an efficient current path and can provide a favorable balance between electrical performance, mechanical strength, and material utilization.
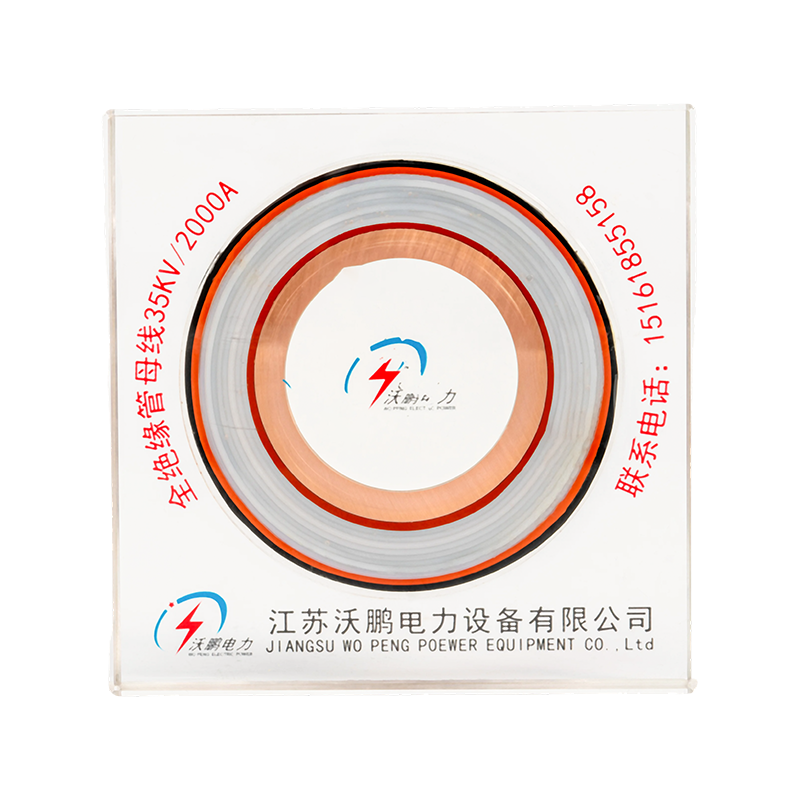
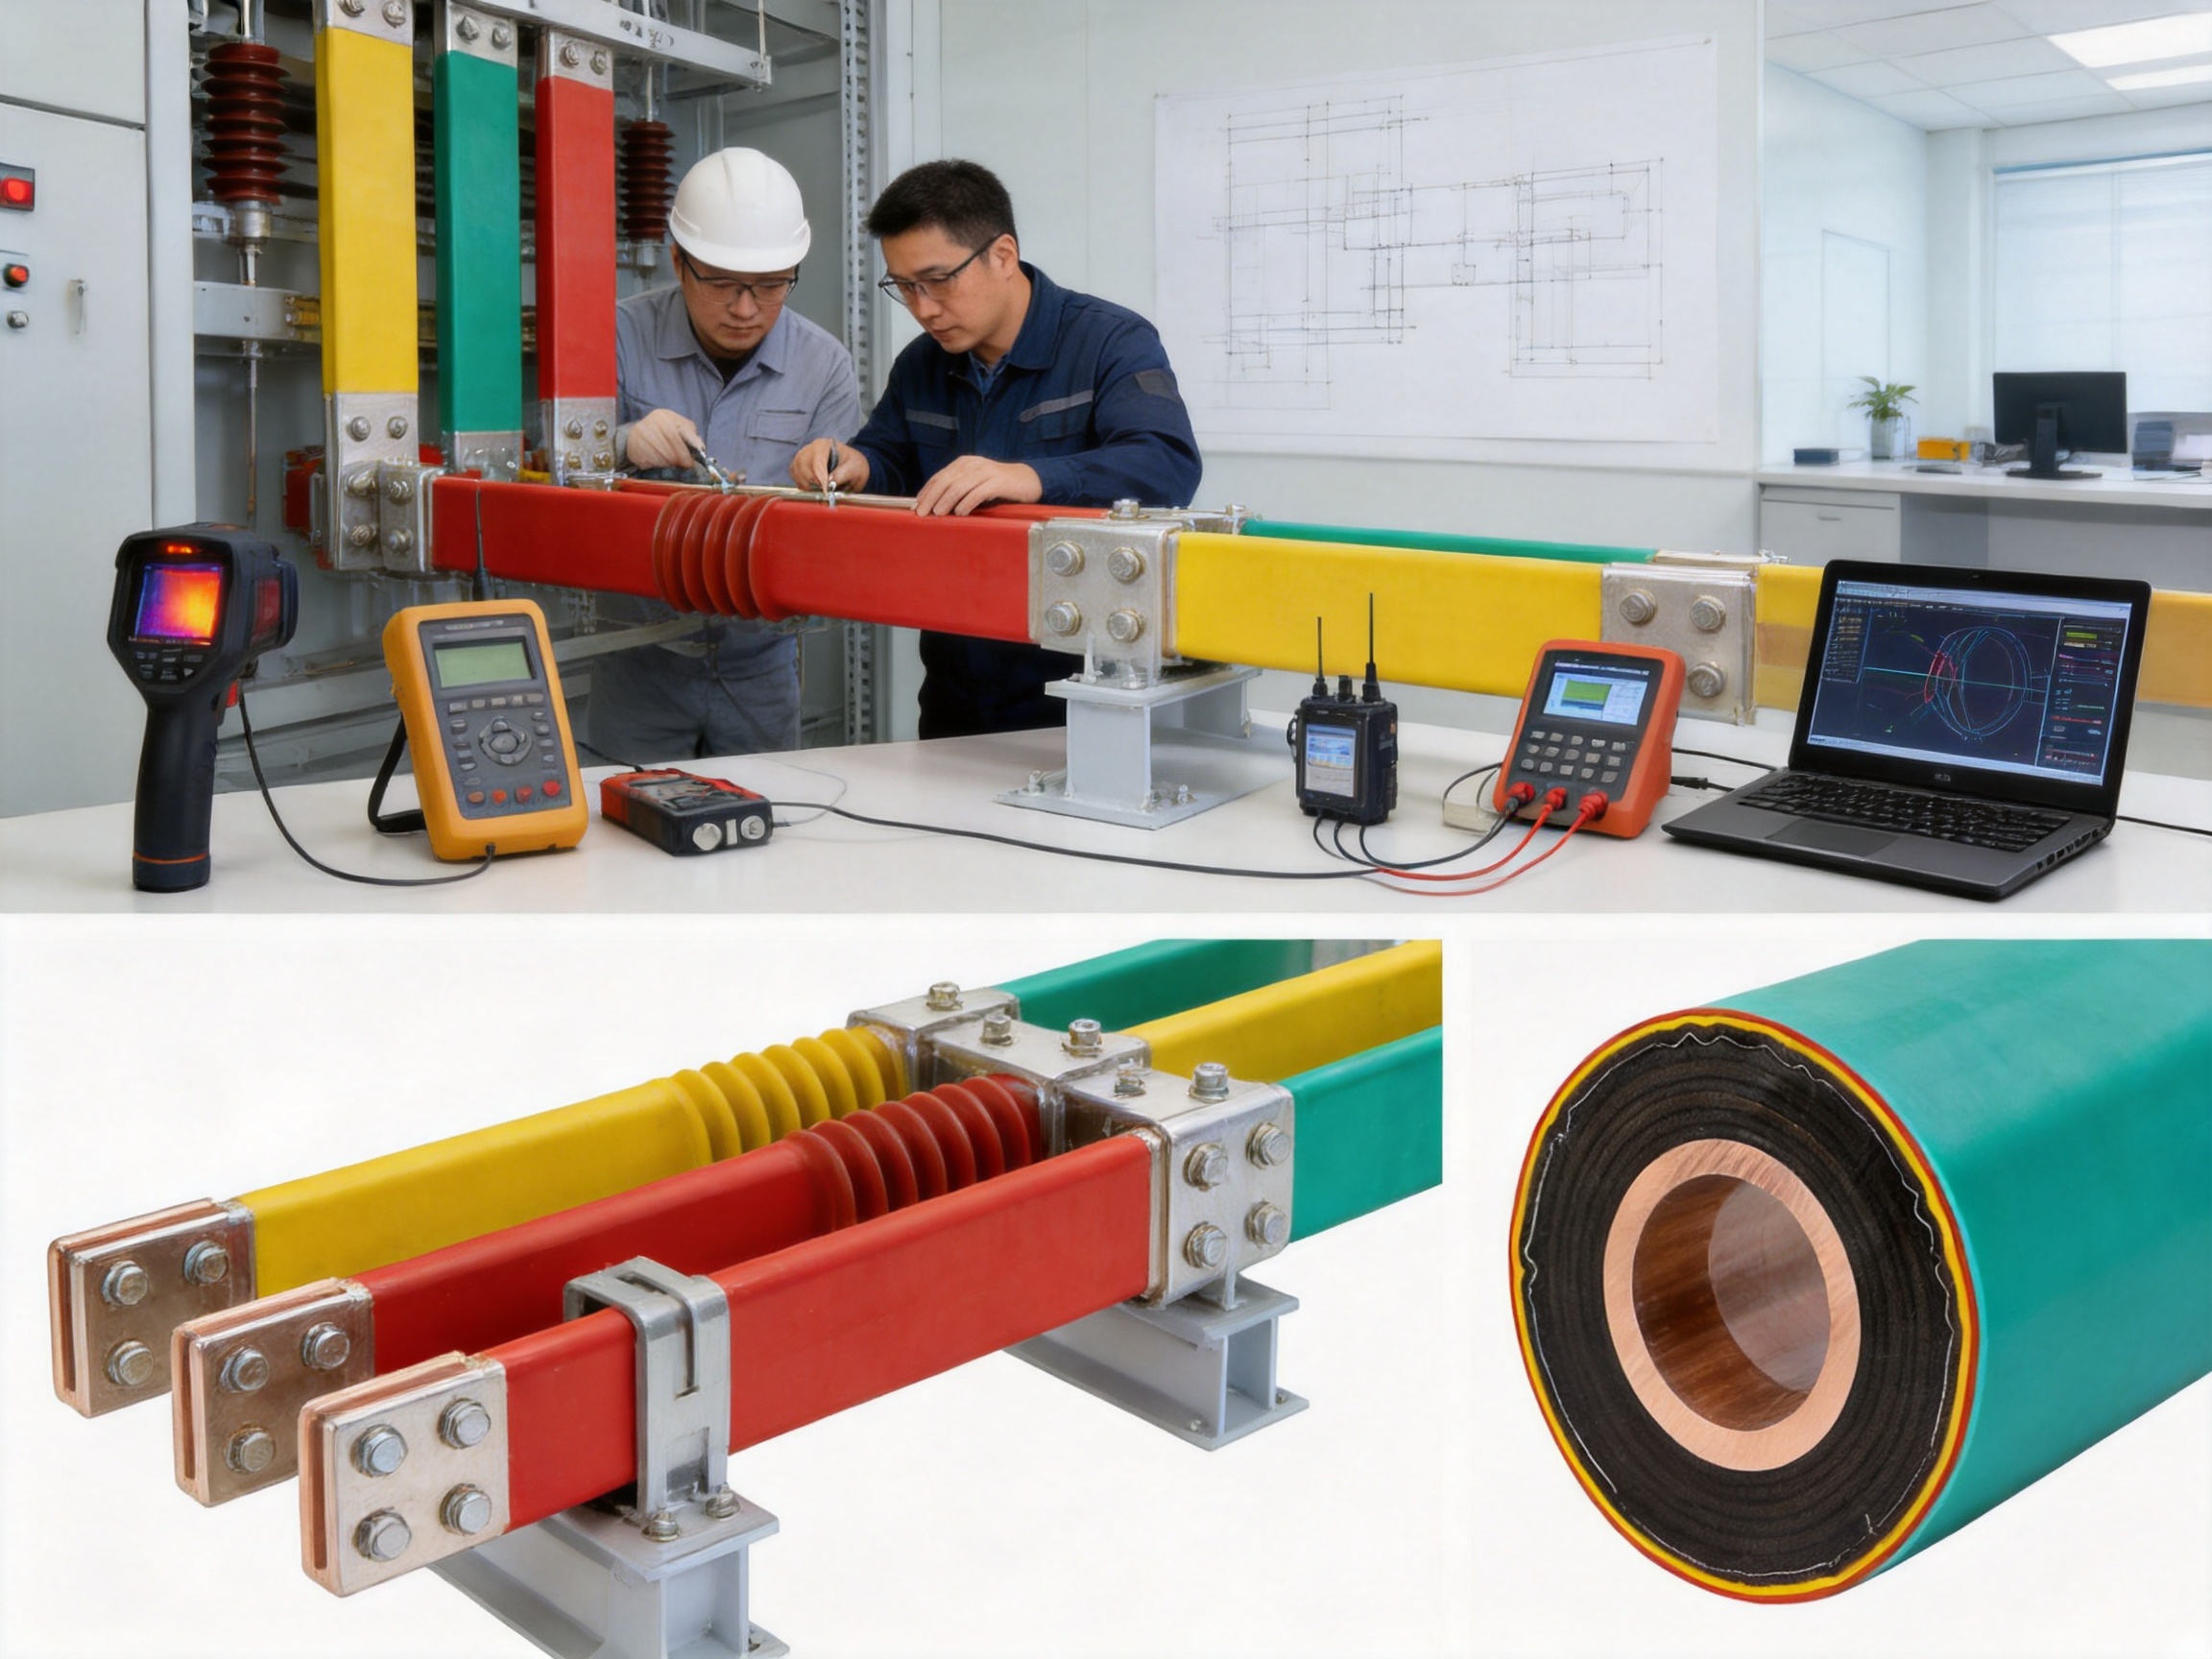
The insulation system normally includes multiple functional layers. These may include an inner shielding layer, semiconductive crepe paper, an outer shielding layer, a metal shielding layer, and an external protective layer. The exact construction depends on the voltage level, insulation coordination, installation environment, connection design, and customer specifications.
Epoxy resin is used because it can be formed into a dense, strong, and electrically stable insulating body. When properly mixed, vacuum-treated, injected, and cured, the resin fills the designed mold around the conductor and other internal layers. The resulting product has fewer air gaps and fewer exposed interfaces than an assembly that depends mainly on separately installed insulation components.
The completed tubular bus bar can be connected to transformers, switchgear, control cabinets, generators, and other equipment using flexible links, bolted connections, terminal joints, and engineered intermediate joints. Depending on the design, it may be installed indoors, in cable trenches, in cable mezzanines, between switch cabinets, or in outdoor sections with suitable environmental protection.
1.1 Integrated Electrical and Mechanical Structure
The main value of the product is not simply the presence of an epoxy insulation layer. Its value comes from the integration of several functions into a single engineered structure. The conductor carries current, the insulation withstands operating voltage, the shielding system controls electric field distribution, the metal shield supports grounding and electromagnetic protection, and the outer layer protects the assembly against physical and environmental stresses.
Because these elements are formed and assembled under controlled manufacturing conditions, the completed bus bar can achieve a consistent geometry along its length. This consistency is important for insulation performance, thermal behavior, mechanical support, and connection accuracy.
1.2 Voltage and Insulation Design
Epoxy resin casting tubular busbars can be designed for different voltage levels. The supplied technical data identifies insulation thicknesses of approximately 10 millimeters for 10 kV, 15 millimeters for 35 kV, 20 millimeters for 66 kV, 30 millimeters for 110 kV, and 45 millimeters for 220 kV applications. These values should be confirmed during project engineering because the final insulation design must also consider working voltage, lightning impulse withstand, switching impulse requirements, altitude, pollution level, creepage distance, partial discharge performance, and the configuration of terminal joints.
For a specific project, the insulation thickness is only one part of the electrical design. The conductor diameter, shielding arrangement, resin formulation, field grading, joint structure, terminal geometry, and grounding arrangement must all be evaluated together.
2. Main Construction of the Product
2.1 Conductive Core
The conductive core is the primary current-carrying component. Copper is widely selected for applications that demand high conductivity, compact dimensions, strong connection performance, and stable thermal characteristics. The specified copper conductor may use TZ7 or a higher grade, with a copper content of at least 99.90 percent for pure copper tube construction.
Aluminum alloy conductors may be selected when reduced weight, easier handling, or material economy is important. Aluminum designs require careful attention to surface treatment, joint preparation, contact resistance, thermal expansion, and corrosion protection. The appropriate conductor material depends on the required current rating, short-circuit withstand, route length, support arrangement, installation method, and equipment interface.
The tubular geometry can improve mechanical rigidity compared with a flat strip of similar application. It also supports a controlled circular or engineered cross-sectional arrangement that is suitable for cast insulation and shielding. At the conductor ends, the connection surface can be silver-plated or tin-plated to reduce contact resistance and improve corrosion resistance.
2.2 Primary Insulation
The epoxy resin insulation layer provides the main dielectric barrier between the conductor and grounded or accessible external surfaces. It is designed to withstand the specified operating voltage and transient electrical stresses while maintaining mechanical integrity.
A properly manufactured cast resin body can resist moisture penetration more effectively than many exposed or loosely wrapped insulation systems. The resin also provides dimensional stability and helps protect internal layers from abrasion, vibration, dust, and accidental contact.
The insulation formulation can be engineered for flame-retardant performance and aging resistance. The supplied product information identifies a designed service life of more than 30 years under appropriate operating conditions. Actual service life depends on loading, ambient temperature, installation quality, ultraviolet exposure, pollution, chemical conditions, mechanical stress, and maintenance practices.
2.3 Semiconductive and Shielding Layers
High-voltage insulated busbars require controlled electric field distribution. Semiconductive layers and shielding components help reduce field concentration around the conductor and at changes in geometry. This is particularly important near terminals, joints, bends, and equipment interfaces.
The product structure may include semiconductive crepe paper, inner and outer shielding layers, and a metal shield. These layers are integrated during the casting and assembly process rather than being left as independent components that can shift during handling or operation.
The metal shielding system may be manufactured from a composite of tinned steel strip and copper strip, or from copper braided tape and copper strip according to the specific design. The metal shield is connected to the grounding system through copper stranded wires or braided copper conductors. Grounding points must be securely bonded to the site grounding network and clearly identified for installation and maintenance.
2.4 External Protective Layer
The external protective layer provides additional resistance to mechanical impact, moisture, dust, and handling damage. It also helps maintain the designed separation between the internal electrical layers and the surrounding environment.
Grounding points require particular protection. Waterproof and moistureproof measures should be applied to prevent water ingress into the grounding connection area. Heat-shrink insulation bushings may be used where appropriate, and phase identification should be clearly visible. Yellow, green, and red phase colors can be applied in accessible and obvious positions to support correct installation and inspection.
2.5 Terminal and Intermediate Joints
Terminal joints are critical because they connect the insulated tubular bus bar to transformers, switchgear, generators, and other equipment. The supplied design uses insulation joints formed in a single molding process and integrated with the copper conductor. This reduces the number of separate interfaces in the terminal area.
Intermediate connections may use embedded stainless steel clamp welding. This method is intended to provide a strong and stable connection while maintaining appropriate electrical and mechanical performance. The stated design objective is for the temperature rise at the terminal joint to remain lower than the temperature rise of the conductor body under specified operating conditions.
Connections between the busbar terminal joint and equipment are made using flexible links and bolted fastening. The flexible connection helps accommodate installation tolerances, vibration, thermal expansion, and relative movement between the tubular busbar and the connected equipment.
All connection surfaces must be properly prepared. The end of the copper tube should be rounded, and the conductor contact surface should be silver-plated or tin-plated when specified. Bolts and screws should use hot-dip galvanized materials or other approved corrosion-resistant finishes. Metal welding completed on site should receive appropriate anti-rust treatment.
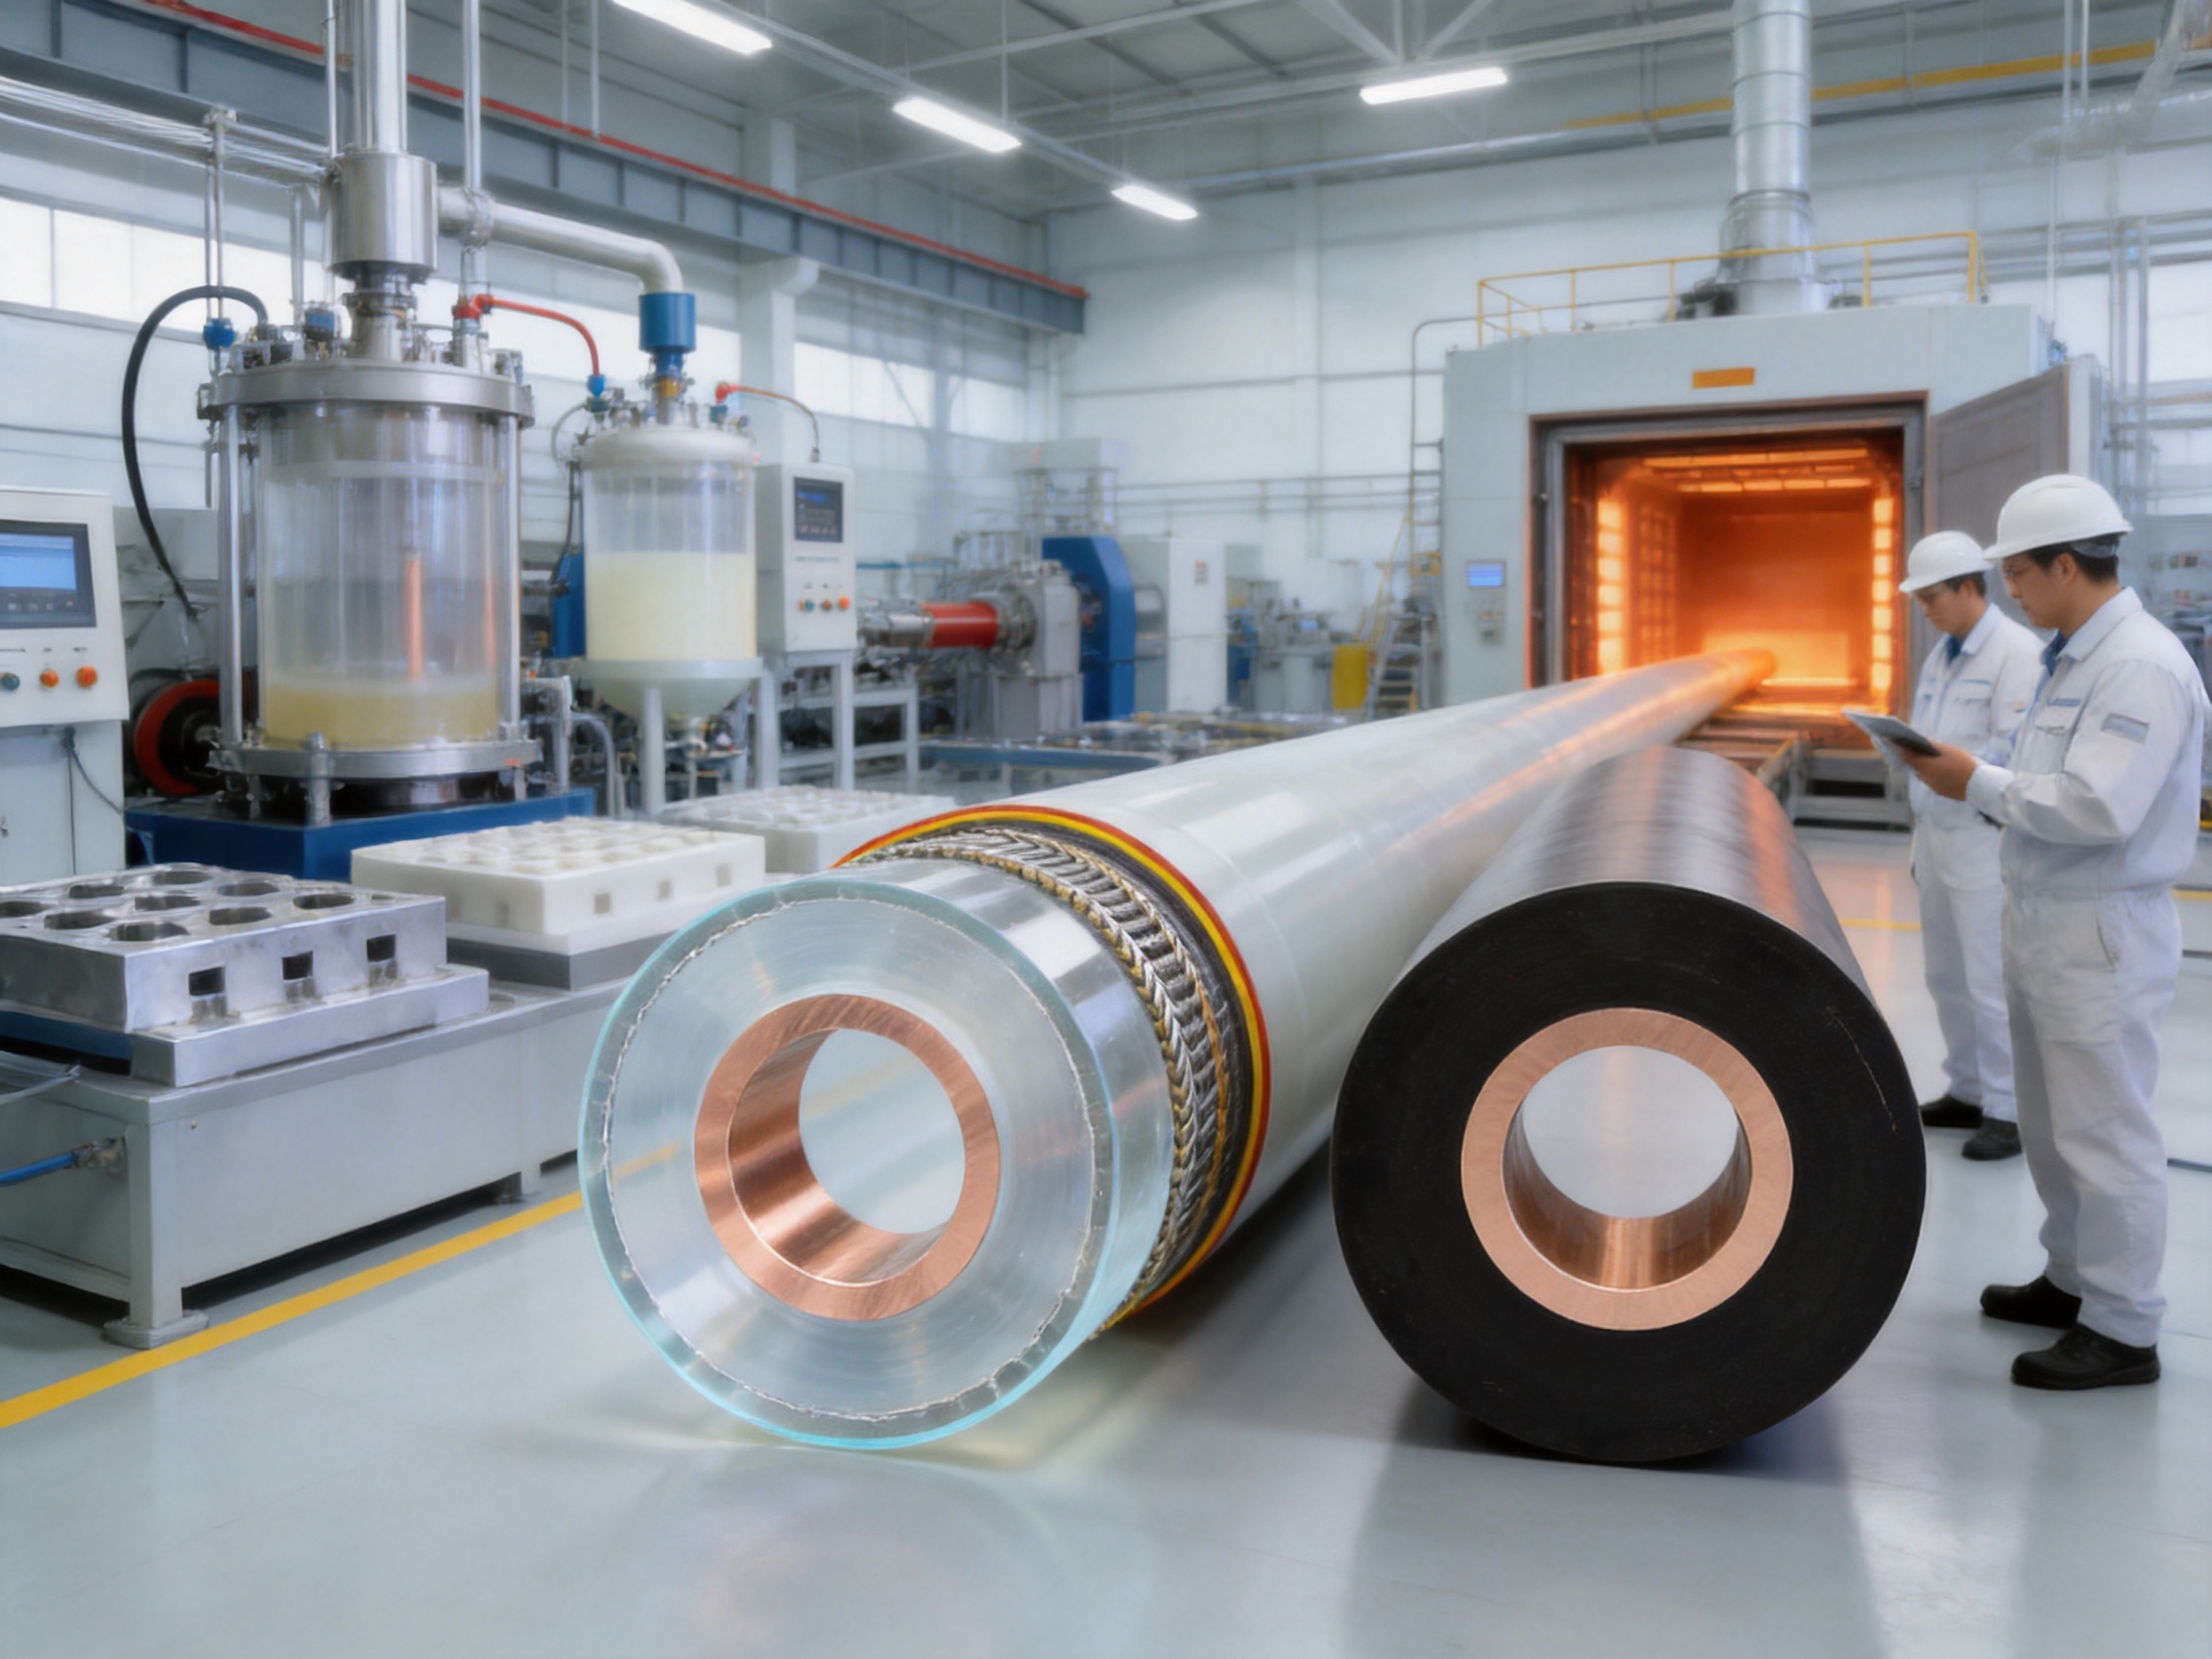
3. Advanced Vacuum Casting and Manufacturing Process
The manufacturing process is central to the performance of an epoxy resin casting tubular bus bar. A high-quality design can only deliver consistent results when the resin system, conductor preparation, mold accuracy, vacuum treatment, injection pressure, curing temperature, and inspection procedures are all controlled.
3.1 Material Preparation
Manufacturing begins with the inspection and preparation of conductive materials, insulation components, shielding materials, resin components, metallic connection parts, and protective accessories. Copper or aluminum conductors are checked for dimensions, surface quality, straightness, conductivity, and compatibility with the project drawings.
Resin and curing-agent components must be stored under controlled conditions. Their batch identification, shelf life, viscosity, mixing ratio, and processing temperature are important factors. Moisture, contamination, incorrect proportioning, or excessive storage time can affect curing behavior and dielectric performance.
Before casting, the conductor surface is cleaned and prepared. Any oxide, oil, dust, burr, or foreign material that could affect bonding or contact resistance must be removed. Shielding layers and grounding components are positioned according to the approved manufacturing drawing.
3.2 Automated Two-Component Mixing
The product is manufactured using an automated two-component vacuum injection molding system. The two resin components are accurately metered and mixed before injection. Automation improves repeatability and reduces the risk of human error in resin proportioning.
The mixing system is designed to produce a uniform resin compound. Consistent mixing is important because localized variations in curing-agent concentration can create differences in hardness, thermal behavior, adhesion, and dielectric strength.
Automated processing also supports production traceability. Key parameters such as material batch, mixing ratio, vacuum level, injection pressure, temperature, curing time, and operator or equipment identification can be recorded for quality management and future reference.
3.3 Vacuum Treatment
Vacuum treatment removes trapped air and volatile substances from the resin and mold assembly. Air voids are undesirable in high-voltage insulation because they can create locations of electrical field concentration and partial discharge. Vacuum processing helps the resin flow into the intended spaces and improves the compactness of the final insulation body.
The conductor and internal layers are positioned in a precision mold before the vacuum process begins. The mold must maintain the correct concentricity, insulation thickness, shielding position, terminal geometry, and dimensional tolerances throughout injection and curing.
Maintaining a stable vacuum is especially important for long tubular products and complex terminal sections. A controlled process reduces the possibility of cavities, incomplete filling, resin-rich areas, resin-starved areas, and defects near connection transitions.
3.4 Pressure Injection
After vacuum treatment, the mixed resin is injected under controlled pressure. Pressure injection promotes complete filling of the mold and helps the resin surround the conductor and shielding layers uniformly.
The injection process must be matched to resin viscosity, mold temperature, product length, conductor geometry, and the location of internal components. Excessive injection speed can lead to turbulence or uneven flow, while insufficient pressure can result in incomplete filling. Advanced equipment enables process engineers to establish repeatable injection parameters for different product specifications.
Pressure injection also supports the formation of an integrated body around the conductor and insulation joints. This one-shot molding approach minimizes separate assembly steps and helps achieve a continuous insulation structure.
3.5 High-Temperature Curing
After injection, the product undergoes controlled high-temperature curing. The curing cycle converts the liquid resin system into a solid thermoset insulation body. Temperature, time, mold condition, and cooling rate must be controlled to reduce internal stress and achieve stable mechanical and electrical properties.
Correct curing is essential for resistance to heat, mechanical vibration, moisture, and long-term aging. Under-cured resin may have inadequate strength or dielectric performance, while excessively rapid or uneven curing may create internal stress, deformation, or cracking.
Once curing is complete, the product is removed from the mold and undergoes dimensional inspection, surface finishing, terminal processing, and electrical testing. The integrated casting process results in a nonseparable structure in which the conductor, insulation, shielding, and protective layers operate as a coordinated assembly.
4. Technical Advantages Compared with Conventional Solutions
4.1 Improved Insulation Integrity
The most important advantage of epoxy resin casting is the formation of a continuous insulation body around the conductor. Conventional arrangements may depend on several separately applied layers, wraps, tapes, supports, or exposed interfaces. Each additional interface can create a potential location for moisture ingress, mechanical movement, installation error, or electrical stress concentration.
A cast resin structure reduces the number of accessible interfaces and helps maintain a stable insulation geometry. The result is particularly valuable in compact substations, industrial plants, and high-current equipment rooms where reliability and space utilization are important.
4.2 Strong Moisture and Pollution Resistance
Moisture and contamination can reduce insulation performance, accelerate surface tracking, and increase maintenance requirements. The dense epoxy exterior and integrated shielding system help protect the conductor from humidity, dust, industrial pollutants, and accidental contact.
This advantage does not eliminate the need for correct installation. Terminals, grounding points, cable entries, joints, and interfaces with external equipment must still be sealed and protected. However, the cast body provides a stronger baseline of environmental protection than an exposed conductor arrangement.
The product information identifies a daily average relative humidity of up to 95 percent and a monthly average relative humidity of up to 90 percent as design environmental conditions. Project-specific verification is required before use in condensation-prone, chemically aggressive, or continuously wet environments.
4.3 Flame-Retardant Performance
Epoxy resin systems can be formulated for flame-retardant performance. This is important in hospitals, data centers, high-rise buildings, transportation facilities, underground installations, and industrial plants where fire safety is a major design consideration.
The supplied technical description identifies flame-retardant characteristics and refers to UL94 V-0 performance in the general product explanation. Final fire classification should always be confirmed through the applicable product test report and the exact resin formulation supplied for the project.
4.4 Mechanical Protection
A cast tubular bus bar provides a mechanically robust external surface. The conductor is protected from accidental impact, abrasion, and handling damage during transportation and installation. The rigid structure can also support controlled routing through difficult areas.
Mechanical strength is especially useful in long vertical routes, cable trenches, power plant equipment rooms, wind turbine towers, and installations subject to vibration. The maximum suspension span for the described product is not more than 5 meters. Actual support spacing should be established through structural calculations that consider product weight, short-circuit forces, wind loading, seismic conditions, and installation orientation.
4.5 Reduced Maintenance Requirements
Because the conductor and insulation are enclosed in an integrated body, routine maintenance can focus on terminal connections, grounding points, support systems, cleanliness of accessible external areas, and periodic electrical inspection. There are fewer exposed insulation surfaces to clean or rewrap than in some conventional systems.
Reduced maintenance does not mean maintenance-free operation. Bolted joints should be inspected for correct torque, signs of overheating, corrosion, or loosening. Grounding continuity should be verified, especially after modifications or maintenance work. Thermal imaging and insulation testing may be included in an appropriate maintenance program.
4.6 Compact and Organized Installation
Tubular busbars can provide a neat and organized alternative to multiple parallel cables. A carefully engineered route can reduce congestion in cable trenches and improve access around switchgear and transformers. The system can also reduce the number of separate cable supports, terminations, and cleats required for a high-current connection.
In applications where visual appearance, access, and clear routing are important, a tubular busbar system can offer advantages over a dense cable installation. It is particularly suitable for direct connections between the low-voltage terminals of a transformer and a switch cabinet.
4.7 Long-Term Design Life
The product is designed for a service life of more than 30 years when operated within specified electrical, thermal, mechanical, and environmental limits. The general product information also describes a potential service life of 30 to 40 years under normal working conditions.
Long-term reliability depends on the complete system, not only on the resin. The conductor must be correctly sized, joints must be properly installed, supports must be adequate, grounding must be reliable, and environmental conditions must remain within the design range. Correct application engineering is therefore essential to realizing the intended service life.
5. Performance Comparison with Other Insulated Bus Bar Systems
Different insulated busbar technologies can be appropriate for different applications. The selection should consider voltage, current, route length, fire requirements, installation environment, maintenance strategy, flexibility, cost, and available space.
| Characteristic | Epoxy Resin Casting Tubular Bus Bar | Silicone Rubber Insulated Bus Bar | PVC Insulated Bus Bar | Conventional Cable Arrangement |
|---|---|---|---|---|
| Insulation structure | Integrated cast resin structure with conductor and shielding layers | Flexible elastomeric insulation system | Polymeric insulation applied around conductors | Multiple individual cables with separate terminations and supports |
| Mechanical rigidity | High | Moderate to high, depending on construction | Moderate | Dependent on cable type and support system |
| Moisture resistance | Excellent when joints and grounding points are properly sealed | Good | Generally lower in demanding high-temperature or harsh environments | Varies significantly with cable jacket and installation method |
| Fire performance | Can be designed for flame-retardant performance, including V-0-rated formulations | Usually good, subject to formulation | Varies by compound and often requires specific fire-rated construction | Varies by cable insulation and sheath materials |
| Protection from contamination | High because the conductor and insulation are enclosed | Good, subject to surface condition and joints | Moderate to good | Depends on enclosure, spacing, and installation environment |
| High-current routing | Suitable for engineered high-current connections | Suitable for selected applications | More limited in demanding high-voltage environments | Possible, but may require many parallel cables |
| Installation appearance | Compact and orderly | Flexible and adaptable | Generally organized | Can become congested with high current ratings |
| Maintenance focus | Terminals, grounding, supports, and routine electrical testing | Surface condition, joints, and supports | Surface condition and aging inspection | Many terminations, cleats, cable surfaces, and support points |
The comparison shows why epoxy resin casting tubular bus bar is attractive for projects that prioritize electrical safety, mechanical protection, compact routing, and long service life. It is not automatically the best choice for every route. Flexible cable systems may be more suitable where frequent movement or complex routing is required, while other insulated busbars may be preferred where low weight or particular installation flexibility is the primary objective.
6. Operating Environmental Conditions
The described tubular bus bar system is designed for demanding environmental conditions when correctly selected and installed. The stated altitude limit is up to 4,000 meters. At high altitude, reduced air density can affect external insulation and heat dissipation, so the final design should include appropriate correction factors and insulation coordination.
The specified ambient air temperature range extends from a minimum of -45°C to a maximum of +60°C, with a maximum daily temperature variation of 35 K. These conditions place demands on resin flexibility, thermal expansion, conductor heating, terminal interfaces, and support structures.
The stated solar radiation intensity is 1,000 W/m², and the maximum wind speed is 40 m/s. For outdoor applications, the enclosure, external surface, terminal protection, and UV resistance should be evaluated in addition to the cast insulation itself.
The product information identifies an ice thickness of up to 20 millimeters and seismic conditions corresponding to an intensity of 8 degrees. The listed ground horizontal acceleration is 0.20 g, vertical acceleration is 0.15 g, and the test frequency is 20 Hz with a sine-wave endurance of three cycles. These values are important for support design, joint flexibility, terminal loading, and structural verification.
A safety factor greater than 1.67 is identified in the technical data. The applicable safety factor for a specific installation should be verified through the project’s structural, electrical, and mechanical calculations.
For heavily polluted outdoor environments, creepage distance and terminal design must be carefully considered. The supplied information refers to a serious pollution design creepage distance of approximately 31 millimeters per kilovolt and a total climbing distance of at least 680 millimeters after installation of an outdoor terminal climbing device. These parameters must be matched to the applicable national and international standards and to the actual site pollution level.
7. Typical Application Solutions
7.1 Transformer-to-Control-Room Connection
One of the most common applications is the direct connection between the low-voltage terminals of a main transformer and the switch cabinet terminals in a control room or distribution room. This arrangement is suitable for high-current transmission and creates a direct, clear, and organized electrical route.
The tubular busbar can be designed as a fully insulated system or, where the engineering conditions permit, a semi-insulated system. A fully insulated configuration provides a higher level of protection against accidental contact, environmental contamination, and installation-area limitations.
7.2 Routing Through a Cable Trench
A tubular busbar can be installed through an underground cable trench or cable mezzanine before connecting to switch cabinets. This method is useful when direct overhead routing is not practical or when the project layout requires equipment separation.
The rigid cast body is well suited to controlled trench routing, provided that support spacing, drainage, access, heat dissipation, and protection against standing water are properly designed. Waterproofing is especially important in underground areas.
7.3 Connections Between Switch Cabinets
In a group of adjacent or separated switch cabinets, tubular busbars can provide a compact connection between sections. The system may be routed through a lower cable connection area, an upper cable connection area, or an intermediate cable mezzanine.
The final connection method should be selected according to cabinet design, phase arrangement, equipment clearances, maintenance access, and the direction of terminal entry. Factory-engineered terminal assemblies can reduce site fabrication work and improve installation consistency.
7.4 Wind Power and Renewable Energy Facilities
Wind turbines and renewable energy facilities often require compact, mechanically robust power transmission systems. Tubular busbars can be adapted for routes in towers, nacelles, substations, and collection systems where space, vibration, and environmental exposure must be considered.
Wind power applications require special attention to vibration, cyclic loading, temperature changes, transport limitations, and installation access. The busbar route and its support structure should be verified as a complete mechanical system.
7.5 Industrial Plants and Large Commercial Buildings
Industrial facilities, petrochemical plants, metallurgical works, hospitals, data centers, and high-rise buildings may require reliable high-current distribution in areas where fire safety, cleanliness, and compact routing are essential.
For these applications, the cast insulation, shielding, grounding, and flame-retardant design can provide advantages over exposed conductors or large groups of parallel cables. The system can also support a more orderly equipment layout and simplify coordination between power distribution rooms.
8. Intelligent Monitoring and Digital Maintenance
Modern busbar systems increasingly incorporate monitoring technologies to improve operational visibility. A tubular bus CNC monitoring system can be configured to monitor multiple technical parameters and support unmanned or remote supervision.
Depending on the project requirements, monitoring may include conductor temperature, joint temperature, load current, insulation condition, grounding continuity, humidity, vibration, and alarm status. Monitoring design must be coordinated with the electrical insulation system so that sensors do not create unacceptable field concentration or compromise sealing.
Temperature monitoring is particularly useful because abnormal heating can indicate overload, increased contact resistance, poor bolting, inadequate ventilation, or an emerging joint defect. Trend analysis can provide an early warning before a visible failure occurs.
Digital monitoring does not replace correct manufacturing, installation, or routine inspection. It complements those activities by providing continuous or periodic data. The most effective maintenance strategy combines factory quality records, commissioning test results, online monitoring, thermal inspection, visual inspection, and scheduled electrical testing.
9. Manufacturing Strengths and Quality Management
9.1 Engineering and Product Development
Jiangsu Wopeng Power Technology Co., Ltd. was founded in 2018 and focuses on the development and manufacture of high- and low-voltage busbar systems. Its product range covers applications from low voltage to 35 kV, as well as selected customized tubular busbar solutions for high-current and critical operating conditions.
The company’s engineering team includes experienced engineers, technical specialists, and production professionals. This combination supports the complete product cycle, including electrical design, mechanical design, material selection, mold development, terminal engineering, production planning, testing, and field application support.
9.2 Modern Production Equipment
Manufacturing facilities include vacuum casting systems, CNC machining equipment, automated assembly technologies, and inspection equipment. Vacuum casting machinery is essential for producing dense, stable, and consistent insulation bodies. CNC processing supports accurate conductor preparation, terminal machining, drilling, and dimensional control.
Automated assembly reduces variation in the positioning of conductors, shielding layers, grounding components, and joint parts. It also supports repeatable production for customized lengths, phase arrangements, connection directions, and installation geometries.
9.3 Standardized Inspection
Each product should undergo defined inspection procedures appropriate to its voltage and current rating. These may include visual inspection, dimensional inspection, conductor resistance measurement, insulation resistance testing, high-voltage withstand testing, partial discharge testing where applicable, mechanical verification, grounding continuity checks, and routine quality inspection.
Mechanical verification is important for long tubular products. It can include checks of support locations, joint strength, terminal alignment, allowable span, and resistance to handling loads. Electrical tests confirm that the completed insulation and conductor system comply with the approved design.
The company also collaborates with third-party testing institutions for independent validation. External testing can support type-test documentation, project approvals, customer qualification procedures, and verification of safety and performance claims.
9.4 Production Traceability
Traceability provides a record of the materials and processes used to manufacture each product. Important records may include conductor batch, resin batch, casting date, mold identification, vacuum level, injection parameters, curing cycle, inspection results, and final product identification.
Traceability is valuable during commissioning, maintenance, warranty evaluation, and future system expansion. It also allows manufacturing teams to identify process trends and improve product consistency over time.
9.5 Project Customization
Power distribution projects rarely have identical requirements. Route length, terminal orientation, phase spacing, connection direction, support points, enclosure dimensions, voltage class, current rating, environmental conditions, and installation access can vary significantly.
A specialized manufacturer can customize tubular busbar systems to match these variables. Custom engineering may include conductor cross-section, copper or aluminum material, insulation thickness, shielding arrangement, terminal joint design, flexible connection, grounding points, phase identification, support hardware, and monitoring provisions.
10. Selection Guidelines for Buyers and Engineers
10.1 Confirm Electrical Requirements
The first step is to establish rated voltage, rated current, frequency, short-circuit current, short-circuit duration, insulation level, power frequency withstand, lightning impulse withstand, and required clearances. The conductor must be sized for continuous current and short-circuit thermal and mechanical stresses.
For high-current systems, the expected load profile should also be reviewed. Continuous operation at maximum rating, cyclic loading, emergency overload, harmonic current, and ambient temperature all affect conductor heating and thermal design.
10.2 Review the Route and Installation Method
The route should be surveyed before final design. Important information includes length, bends, elevation changes, support positions, equipment interfaces, trench dimensions, access restrictions, transportation limitations, and lifting requirements.
The maximum suspension span should not exceed the specified design limit. The support system should prevent excessive deflection and should withstand electromagnetic forces during short-circuit events. Supports must also accommodate thermal expansion and seismic movement where required.
10.3 Evaluate Environmental Conditions
Altitude, minimum and maximum temperature, humidity, pollution, salt exposure, chemical vapors, solar radiation, wind, ice, seismic activity, and flooding risk should be documented. Outdoor terminal components may require additional weatherproofing, UV protection, creepage distance, and climbing devices.
Indoor installation does not automatically mean mild conditions. Industrial dust, condensation, corrosive gases, high humidity, and elevated temperature can be severe inside buildings. The insulation, external protection, terminal seals, and grounding system must be selected accordingly.
10.4 Check Connection Compatibility
The busbar terminal must match the transformer, switchgear, generator, or other equipment interface. Bolted hole patterns, conductor size, phase spacing, terminal height, flexible link length, and available clearance should be confirmed before production.
Improperly aligned or forced connections can place mechanical stress on the busbar and equipment bushing. Flexible links should be designed to absorb reasonable installation tolerances and thermal movement without creating excessive bending or contact pressure.
10.5 Request Technical Documentation
Buyers should request product drawings, technical data sheets, type-test reports, routine test records, installation instructions, grounding diagrams, support details, maintenance recommendations, and material certifications as appropriate.
For critical projects, the supplier should clarify the applicable standards, fire classification, insulation test methods, environmental limitations, partial discharge requirements, short-circuit withstand capability, and field acceptance procedures.
11. Installation and Commissioning Considerations
Installation should be performed by qualified personnel using the approved layout and manufacturer’s instructions. Tubular busbars should be transported and lifted using methods that prevent impact, bending, twisting, and damage to terminal sections.
Before installation, the product should be inspected for cracks, scratches, contamination, moisture, deformation, missing accessories, and damage to protective packaging. Any abnormality should be recorded and evaluated before energization.
Support hardware must be installed at the specified positions. The busbar should not be forced into alignment by tightening equipment bolts. Flexible connections should be installed without excessive bending or torsion.
Grounding points must be securely connected to the site grounding system. The continuity of the metal shield and grounding leads should be verified. Grounding points should remain accessible for inspection where the design permits.
Bolted conductor connections should be cleaned, correctly aligned, and tightened to the specified torque. Contact surfaces must be free of contamination and corrosion. Where silver-plated or tin-plated surfaces are provided, they should not be damaged during installation.
Before energization, the completed system should undergo the required insulation resistance, high-voltage withstand, phase identification, continuity, grounding, contact resistance, and visual inspections. The test voltage and method must follow the approved commissioning procedure and applicable standards.
After energization, the system should be monitored for abnormal noise, odor, temperature rise, vibration, partial discharge indications, and changes in operating current. A baseline thermal image or monitoring record can be valuable for future maintenance comparisons.
12. Frequently Asked Questions
Q1: What is the main advantage of epoxy resin casting tubular bus bar?
The main advantage is its integrated construction. The conductor, insulation, shielding layers, grounding arrangement, and external protection are designed as one coordinated system. This provides strong insulation integrity, mechanical protection, moisture resistance, compact routing, and reduced exposure to contamination compared with many open or loosely assembled conductor arrangements.
Q2: What conductor materials are available?
Copper and aluminum alloy conductors can be considered. Copper is selected when high conductivity, compact dimensions, and strong connection performance are priorities. Aluminum alloy can reduce weight and material cost but requires careful attention to oxide removal, joint preparation, thermal expansion, and corrosion protection.
Q3: What copper quality is specified for the product?
The supplied technical information specifies TZ7 or a higher-grade copper conductor, with pure copper tube copper content of at least 99.90 percent. The exact material certificate and conductor grade should be confirmed for each project.
Q4: How long can the product operate?
The design service life is stated as more than 30 years, and general product information describes 30 to 40 years under normal working conditions. Actual life depends on temperature, load, moisture, pollution, mechanical stress, installation quality, joint condition, and maintenance.
Q5: Can the tubular busbar be used outdoors?
Outdoor use is possible when the product configuration, terminal design, shielding, surface protection, creepage distance, grounding, and sealing are suitable for the site. Outdoor applications must account for solar radiation, rain, wind, ice, pollution, ultraviolet exposure, temperature variation, and seismic conditions.
Q6: What is the maximum suspension span?
The supplied product requirements state that the maximum suspension span should not exceed 5 meters. The actual support spacing must be confirmed through mechanical calculations that consider product weight, short-circuit forces, wind, seismic loading, route orientation, and local installation conditions.
Q7: How are intermediate connections made?
Intermediate connections can use embedded stainless steel clamp welding according to the product design. This connection method is intended to provide mechanical stability and controlled temperature performance. All connection work should follow approved procedures and must receive suitable anti-rust treatment when completed on site.
Q8: How are terminal connections made?
Terminal connections to equipment are made through flexible links and bolted fastening. The flexible link helps accommodate alignment tolerance and movement between the busbar and connected equipment. Contact surfaces may be silver-plated or tin-plated to reduce contact resistance and improve corrosion resistance.
Q9: Is the product suitable for high-humidity environments?
Its cast insulation and protective structure provide strong moisture resistance. The stated design conditions include high relative humidity. However, terminal joints, grounding points, cable entries, and external interfaces must be properly sealed. The system should not be installed in conditions beyond its approved environmental rating without additional engineering measures.
Q10: What tests should be performed before energization?
Typical commissioning checks include visual inspection, dimensional and phase verification, insulation resistance, high-voltage withstand, grounding continuity, contact resistance, terminal torque verification, and mechanical inspection. The exact test program should follow the approved project specification and applicable standards.
Q11: Can the product be customized?
Yes. Customization may include conductor material and size, voltage level, insulation thickness, route length, terminal orientation, phase arrangement, connection pattern, flexible links, grounding points, support hardware, protective accessories, and monitoring functions.
Q12: What makes an experienced manufacturer important?
An experienced manufacturer can coordinate electrical design, mechanical design, resin formulation, vacuum casting, conductor preparation, terminal machining, assembly, testing, and documentation. This integrated capability reduces design conflicts and supports consistent quality for customized power transmission projects.
13. Why Choose a Specialized Tubular Busbar Manufacturer?
A tubular busbar is not simply a conductor placed inside an insulating tube. It is a coordinated electrical, mechanical, thermal, and environmental system. The manufacturer must understand conductor sizing, field control, resin chemistry, vacuum processing, joint design, grounding, support structures, and equipment interfaces.
A specialized manufacturer can identify risks before production begins. For example, a terminal design that is electrically acceptable may create excessive mechanical stress, while a mechanically convenient support arrangement may restrict thermal expansion. An experienced engineering team evaluates these interactions during the design stage.
Manufacturing depth is also important for repeatability. Automated vacuum injection, controlled two-component mixing, high-temperature curing, CNC processing, and standardized inspection create a more consistent production environment than manual casting and uncontrolled assembly.
Jiangsu Wopeng Power Technology Co., Ltd. supports projects through product development, manufacturing, testing, and application engineering. Its products have been used across more than 17 provinces and in multiple sectors, including power generation, substations, wind energy, industrial manufacturing, rail transit, and large commercial facilities.
The company’s product portfolio allows customers to evaluate different busbar solutions within one technical supply platform. Options include epoxy resin vacuum-cast tubular busbars, low-voltage epoxy-cast busbar trunking, copper and aluminum tubular busbars, wind power tube busbars, compact busbar systems, and sliding contact line systems.
14. Conclusion
Epoxy resin casting tubular bus bar provides a reliable solution for power transmission applications that require high insulation integrity, mechanical strength, environmental resistance, compact routing, and long service life. Its integrated structure combines a high-quality copper or aluminum conductor with cast epoxy insulation, semiconductive layers, metal shielding, grounding components, and external protection.
The use of automated two-component vacuum injection, pressure casting, and high-temperature curing supports the production of a dense and stable insulation body. One-shot molding of insulation joints and conductor components reduces separate interfaces, while embedded stainless steel connection technology helps maintain dependable intermediate joints.
Compared with exposed conductors, conventional cable groups, and some separately assembled insulated busbar solutions, the product can offer advantages in fire performance, moisture resistance, mechanical protection, cleanliness, appearance, maintenance, and high-current routing. Its suitability is particularly strong in substations, transformer connections, switchgear rooms, industrial plants, wind power facilities, data centers, hospitals, high-rise buildings, and other critical infrastructure.
Successful application depends on correct electrical sizing, mechanical support, environmental evaluation, grounding, terminal design, installation, and testing. When these elements are coordinated by an experienced manufacturer, epoxy resin casting tubular bus bar can provide a safe, efficient, and durable foundation for modern power distribution systems.
References
1. Jiangsu Wopeng Power Technology Co., Ltd., Technical Data for Epoxy Resin Vacuum-Cast Tubular Busbar Systems.
2. Jiangsu Wopeng Power Technology Co., Ltd., Product Structure, Environmental Conditions, and Installation Requirements for Insulated Tubular Busbars.
3. IEC 60071 Series, Insulation Coordination.
4. IEC 62271 Series, High-Voltage Switchgear and Controlgear.
5. IEC 61439 Series, Low-Voltage Switchgear and Controlgear Assemblies.
6. IEC 60243 Series, Electric Strength of Insulating Materials.
7. IEC 60587, Electrical Insulating Materials Used Under Severe Ambient Conditions.
8. UL 94, Tests for Flammability of Plastic Materials for Parts in Devices and Appliances.
9. GB/T 5582, External Insulation Pollution Classification and Related Creepage Design Principles.
10. General principles of high-voltage busbar design, electrical insulation coordination, grounding engineering, thermal verification, and mechanical support calculation.
Product: Epoxy Resin Casting Tubular Bus Bar


-
 +86-180 3625 3000
-
 admin@wpbusbar.com
-
 No. 8, Yanjin Road, Chengxi Industrial Park, Shanyang Town, Baoying County, Yangzhou City, Jiangsu Province, China
Copyright © Jiangsu Wopeng Power Technology Co., Ltd.
All Rights Reserved.
 Custom Insulated Bus Bar Manufacturer
Tubular Busbar System Factory